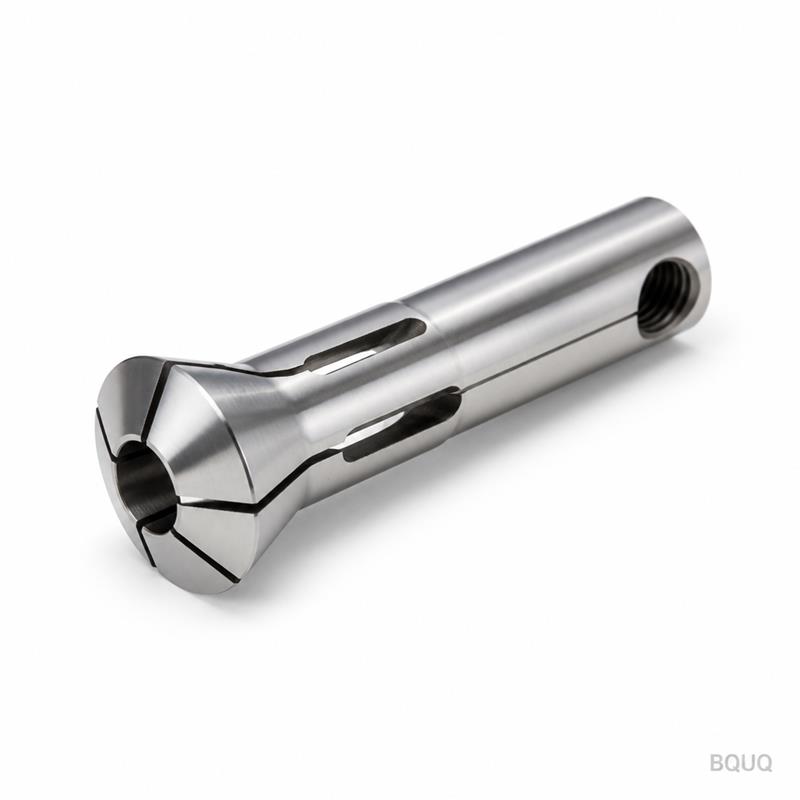
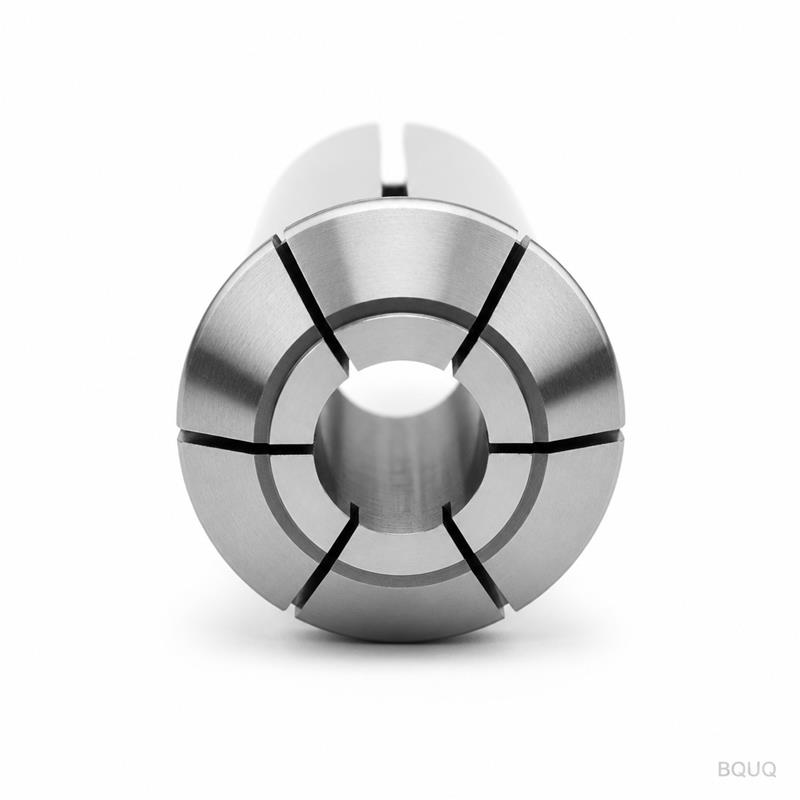
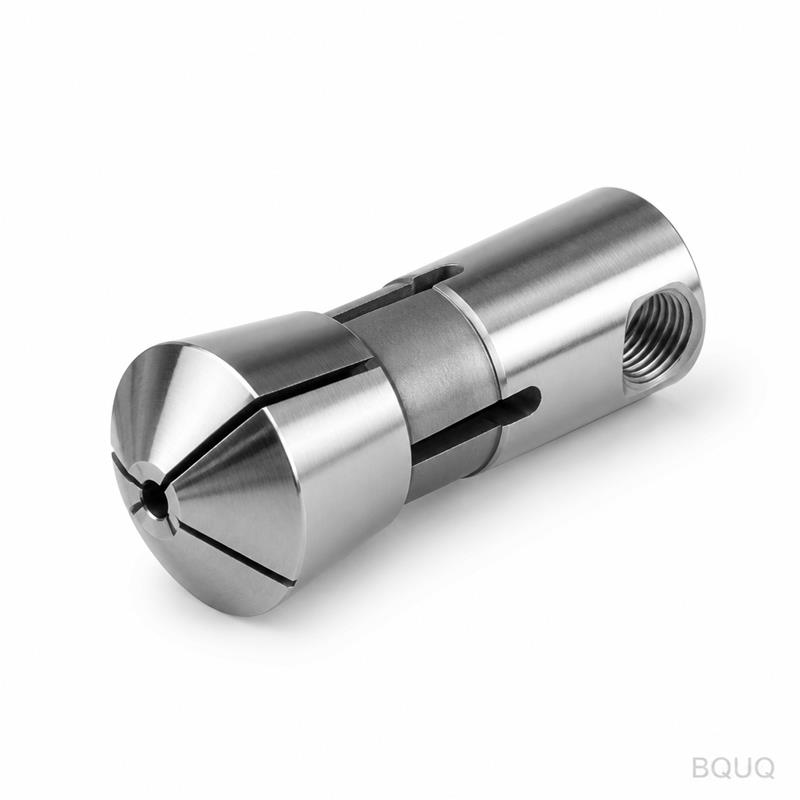
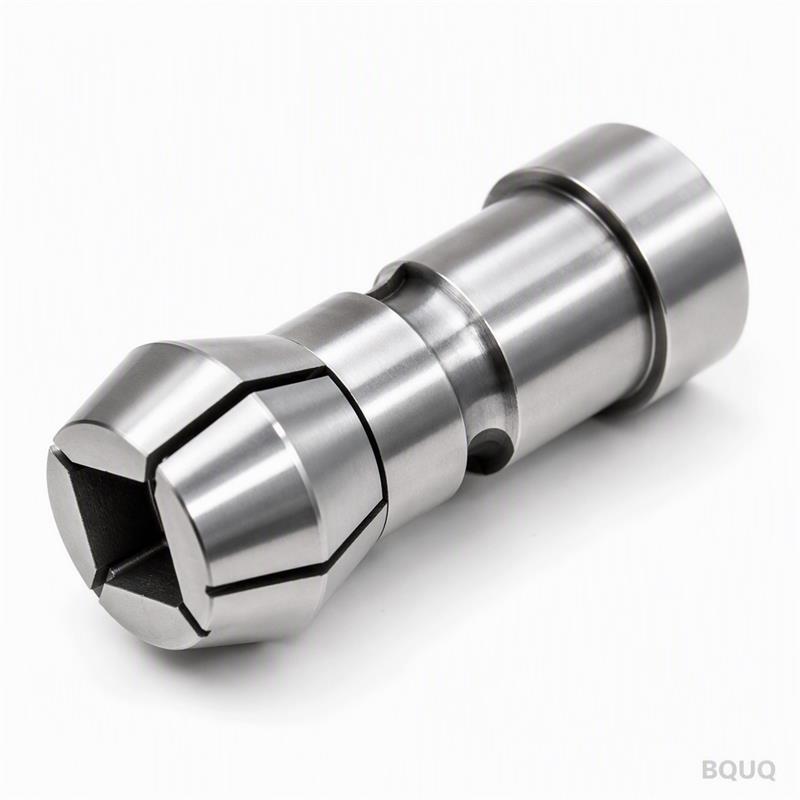
OpeningThis is a 15 Type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every dimension is cut, measured, and verified bef
Custom CNC Collet Chuck 15 Type Round Bore Extended Collet
OpeningThis is a 15 Type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every dimension is cut, measured, and verified before shipment. If the
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a 15 Type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every dimension is cut, measured, and verified before shipment. If the print says ±0.005 mm, we hold ±0.005 mm.
At a glance: Tolerance down to ±0.005 mm, lead time 7–12 working days, no MOQ, material certs included.
Specifications
We run these on CNC Swiss-type lathes and multi-spindle automatics. The extended nose length gives you deeper reach into the workpiece bore without sacrificing grip concentricity. Hardened and ground where the print calls for it.
Parameter
Value
Material
AISI 4140, 8620, 12L14, or per your spec
Hardness
58–62 HRC (case-hardened) or 40–45 HRC (through-hardened)
Process
CNC turning, milling, internal grinding, wire EDM for slots
Tolerance
±0.005 mm on bore ID, ±0.01 mm on outer diameter
Surface finish
Ra 0.4 µm on bore, Ra 0.8 µm on taper
Concentricity
≤0.005 mm TIR between bore and taper
Batch size
1 piece to 10,000 pieces, no MOQ
Lead time
7 working days for prototypes, 12 days for production
Inspection
100% dimensional check, CMM report per batch
Marking
Laser etched part number and heat code
We grind the taper after heat treatment. That is the only way to keep the seating angle accurate. We do not skip this step, even for prototypes.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Each batch gets a unique heat code. We record material lot, machine operator, tool wear data, and inspection results. If you have a problem six months later, we can trace it back to the exact shift that made it. This is not paperwork for show. It is how we find and fix root causes fast.
2. Inspection report per batch. You get a full dimensional report with every shipment. Not a generic certificate—actual measured values for critical features like bore ID, taper angle, and concentricity. We use a CMM and air gauges, not calipers. If a dimension is out, we reject the part before it reaches you.
3. One factory for CNC machining, stamping, springs, and heat sinks. Your collet chuck often sits inside a larger assembly. You might need a stamped retainer, a spring for the ejector, or a heat sink for the spindle motor. We make all of those in the same building. You send one drawing package, get one quote, and receive one consolidated shipment. Fewer suppliers, fewer handoffs, fewer excuses.
Where these parts are used
A 15 Type extended collet is not a generic tool. It is used where standard collets cannot reach or cannot grip without interference.
Swiss-type screw machines: Extended nose clears the guide bushing and reaches into deep counterbores on small turned parts.
Automatic lathe spindles: Round bore grips round stock from Ø3 mm to Ø15 mm, common for brass and aluminum valve components.
Medical device machining: Small bone screws and implant drivers require concentric grip with minimal runout. The extended nose reduces vibration at the cutting tip.
Hydraulic fittings: Extended collets hold the hex or round blank while the back end is drilled and threaded. The longer grip prevents part pushback under high feed rates.
Aerospace fasteners: Titanium and Inconel blanks need rigid support. The hardened bore resists wear from abrasive materials.
If your part has a deep bore, a thin wall, or a tight concentricity callout, this collet design is likely what you need.
Q: What is your MOQ?
A: No MOQ. We make one prototype or a million pieces. The unit price drops with quantity, but the setup cost is the same. For a single piece, expect a higher price per part. For 500 pieces, the price per part drops significantly.
Q: How do you guarantee tolerance and concentricity?
A: We grind the taper and bore in the same setup after heat treatment. This eliminates the error from re-chucking. We then measure every part with an air gauge for the bore and a CMM for the taper. The inspection report shows the actual values, not just a pass/fail mark.
Q: What is your lead time for a custom collet?
A: 7 working days for a prototype with standard material. Production batches of 1000 pieces take 12 working days. If you need faster, we can expedite for a 20% surcharge, subject to material availability.
Q: Do you provide material certificates?
A: Yes. We supply a mill test certificate from the original steel mill, plus our own heat treatment report. If you need third-party testing, we can arrange it at cost. We do not substitute material without your written approval.
Send your drawing
Email your PDF or STEP file to sc@bquq.com. We reply with a firm quote within 12 hours. Include your target quantity and material preference. If you are not sure about the material, we will recommend one based on your application.
For urgent inquiries, WhatsApp +86 13713157787. We are in Dongguan, China, and we answer within the hour during working hours.
Your drawing is the starting point. We handle the rest—precision manufacturing, inspection, and shipment. No MOQ, no surprises. Send it now.