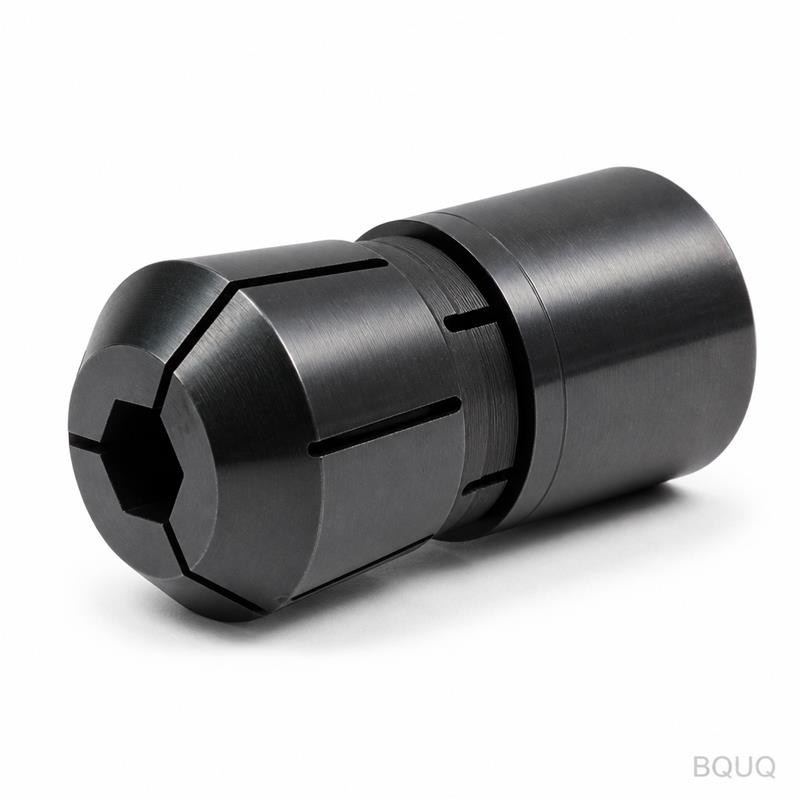
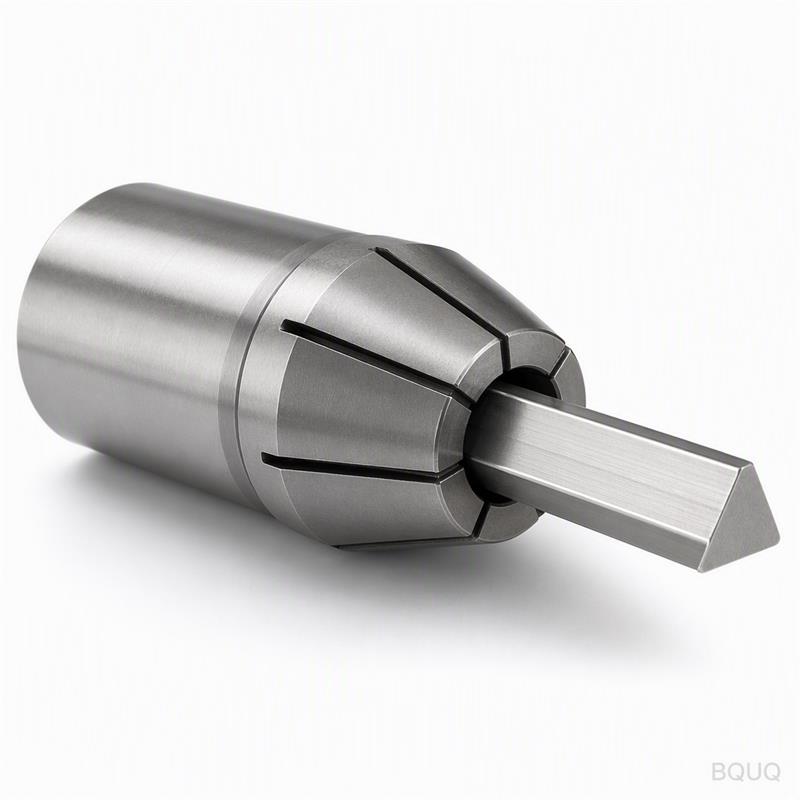
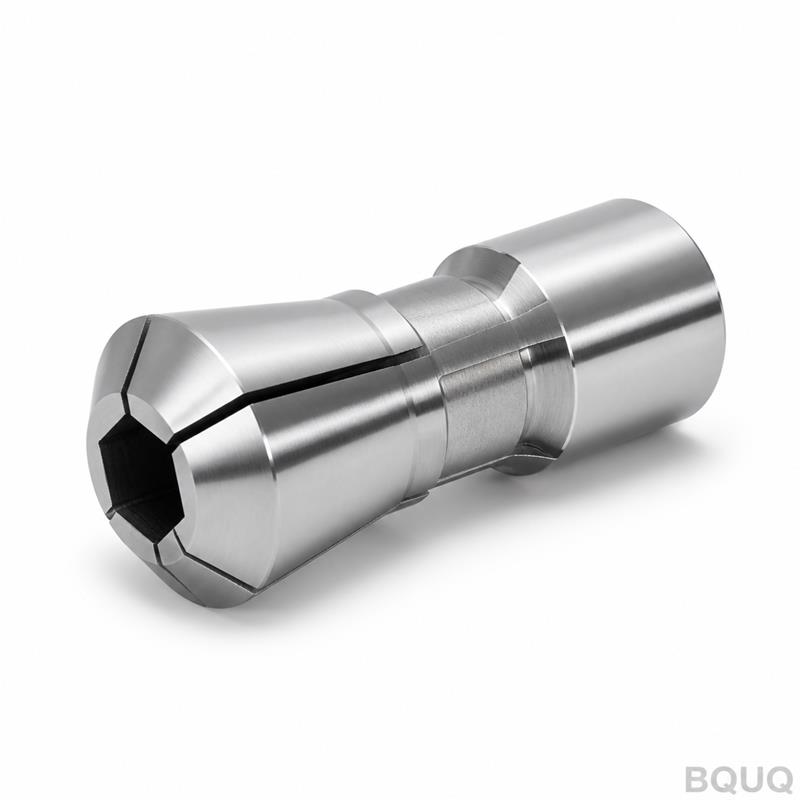
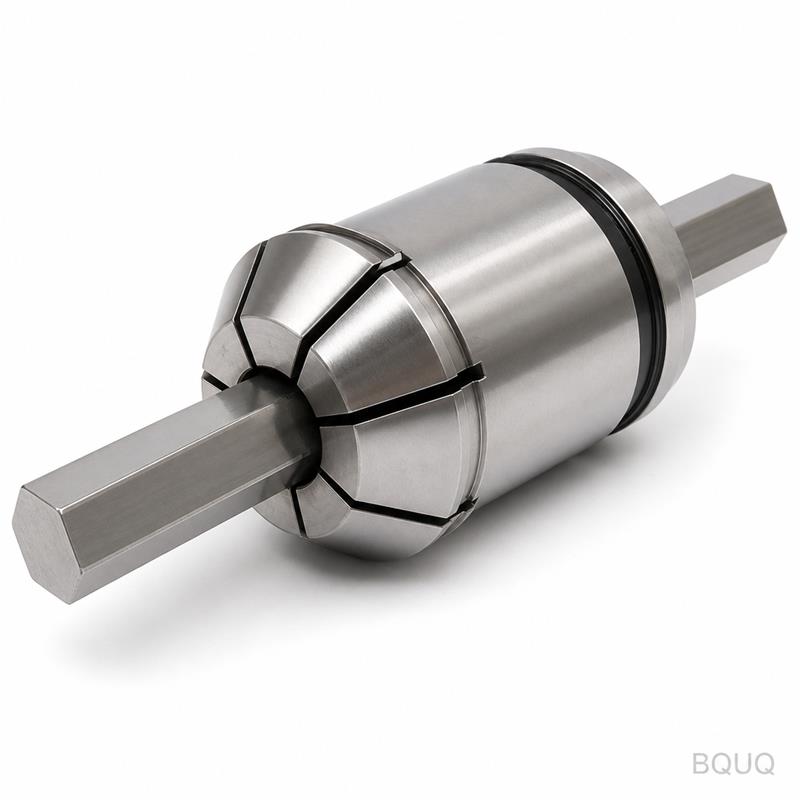
OpeningThis is a 36-type hex bore collet, machined to your drawing, not a stock item. We cut, heat-treat, and grind it in our Dongguan factory. Every bore is verified with a go/no-
Custom CNC Collet Chuck 36 Type Hex Bore Quenched Collet
OpeningThis is a 36-type hex bore collet, machined to your drawing, not a stock item. We cut, heat-treat, and grind it in our Dongguan factory. Every bore is verified with a go/no-go gauge before ship
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a 36-type hex bore collet, machined to your drawing, not a stock item. We cut, heat-treat, and grind it in our Dongguan factory. Every bore is verified with a go/no-go gauge before shipment. You get a collet that holds hex stock without marking it, even at high spindle speeds.
At a glance: Tolerance ±0.005 mm on bore, concentricity ≤0.01 mm, lead time 7–12 working days, no MOQ. One piece or one thousand, same process.
Specifications
Parameter
Value
Material
20CrMnTi or 8620 steel, case-hardened to 58–62 HRC
Bore shape
Hexagonal, 6-point, to your drawing (e.g., 6.35 mm, 8 mm, 10 mm across flats)
Hardness
Quenched and tempered, surface 58–62 HRC, core 35–40 HRC
Tolerance
Bore ±0.005 mm, outer diameter ±0.01 mm, length ±0.02 mm
Vacuum carburizing + gas quenching, no decarburization
Batch size
1 to 5,000 pieces, no MOQ
Inspection
100% bore check, 30% taper check, CMM report on request
Lead time
7 days for prototypes, 12 days for production batches
We use 20CrMnTi for its toughness after quenching. The hex bore is broached or wire-cut, then ground with a diamond wheel. The taper is ground to match your spindle, not a generic angle. If you need a through-hole or a slot for coolant, we add it in the same setup.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Each collet gets a heat-treatment batch number stamped on the face. If you have a problem in the field, we trace it back to the furnace cycle and the grinding operator. No guesswork.
2. Inspection report per batch. You get a dimensional report with every shipment. It lists bore size, hardness, concentricity, and surface finish. We also include a micrograph of the case depth if you ask. This is not a generic certificate; it is your actual parts measured on our CMM.
3. One factory for CNC + stamping + springs + heat sinks. You send us one drawing package, and we handle the collet chuck, the spring that holds it, the stamped retainer ring, and the heat sink if your spindle runs hot. One purchase order, one shipping date, one quality standard. No juggling three suppliers in three time zones.
Where these parts are used
Swiss-type lathe spindles for hex brass or steel stock in watch and connector manufacturing. The quenched bore holds hex bar without slipping at 8,000 RPM.
Automatic screw machines producing hex nuts, fittings, and valve cores. The collet grips the hex OD while the tool cuts the thread or chamfer.
Hydraulic and pneumatic fittings where the hex is the wrenching surface. The collet must not deform the hex corners, so our bore is ground to a sharp internal corner, not a radius.
Medical device components like bone screws and dental implants, where hex drive ends need repeatable positioning. The ≤0.01 mm concentricity keeps the cut concentric to the hex.
Aerospace fasteners in titanium or Inconel. The quenched collet resists wear from abrasive alloys, and the batch traceability satisfies your QA audit.
Q: What is your MOQ?
A: No MOQ. We run one piece for a prototype or 5,000 for production. The per-piece price drops at 100 and 500 pieces, but we do not force you to buy more than you need.
Q: How do you guarantee the bore tolerance?
A: We grind the hex bore with a diamond wheel on a CNC internal grinder. Then we check every piece with a calibrated hex plug gauge. The CMM report shows actual values, not just a pass/fail. If the bore is out, we reject it before it goes to the quench line.
Q: What is your lead time for a custom collet?
A: 7 working days for a prototype after drawing approval. Production batches of 100–1,000 pieces take 10–12 working days. Heat treatment adds 2 days because we run a full vacuum cycle, not a short batch.
Q: Can you provide material certificates?
A: Yes. We supply a mill certificate for the steel, a heat-treatment report with hardness and case depth, and a dimensional inspection report. All are in English and traceable to our ISO 9001:2015 system.
Send your drawing
Send us your 2D or 3D drawing. We check the hex size, the taper angle, and the hardness spec. You get a firm quote in 12 hours, with a lead time and a price per piece. No hidden tooling fees, no surprise setup charges.
Email: sc@bquq.com
WhatsApp: +86 13713157787
We are a precision manufacturing factory in Dongguan, China, with 20 years in CNC machining, stamping, springs, and heat sinks. Your custom CNC collet chuck is made in China, but with the inspection rigor you expect from a German or Japanese supplier. Send the drawing, and we will prove it.