OpeningYour drawing defines the part. We machine it. Every collet is made to your exact dimensions, not a stock approximation. Before shipment, each unit is verified against your f
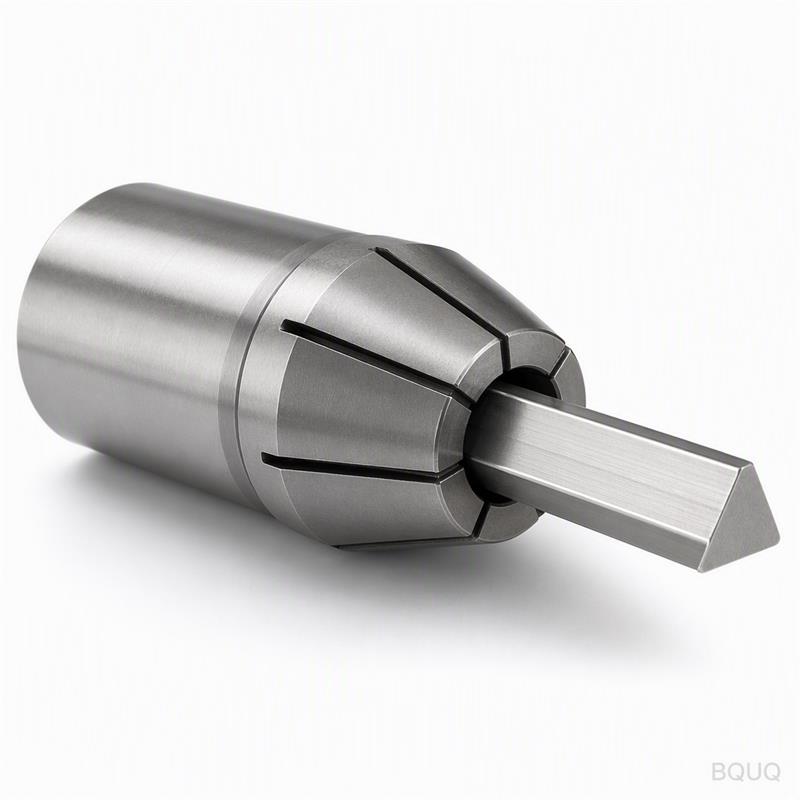
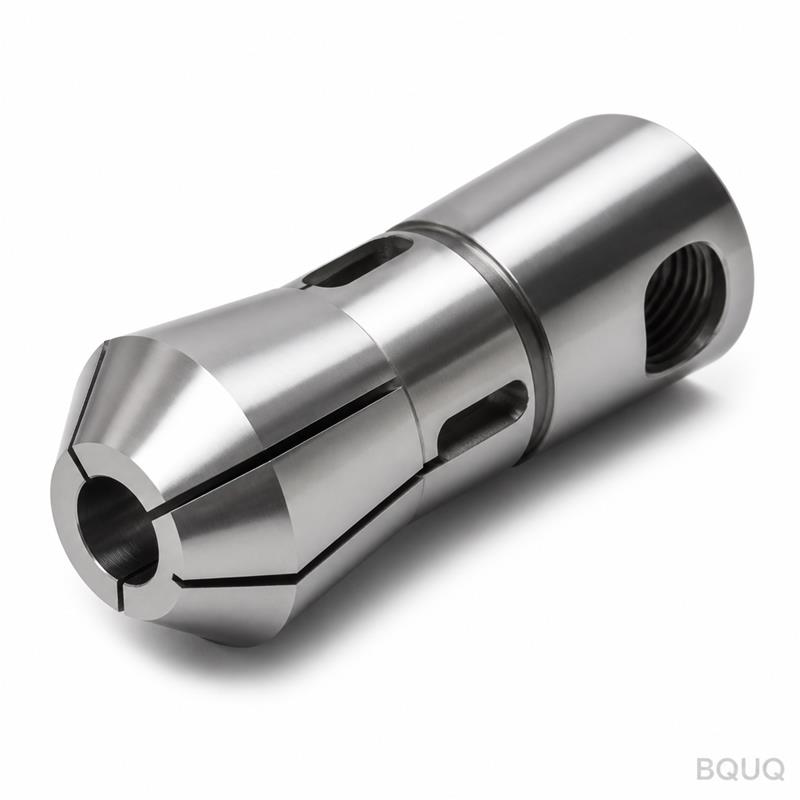
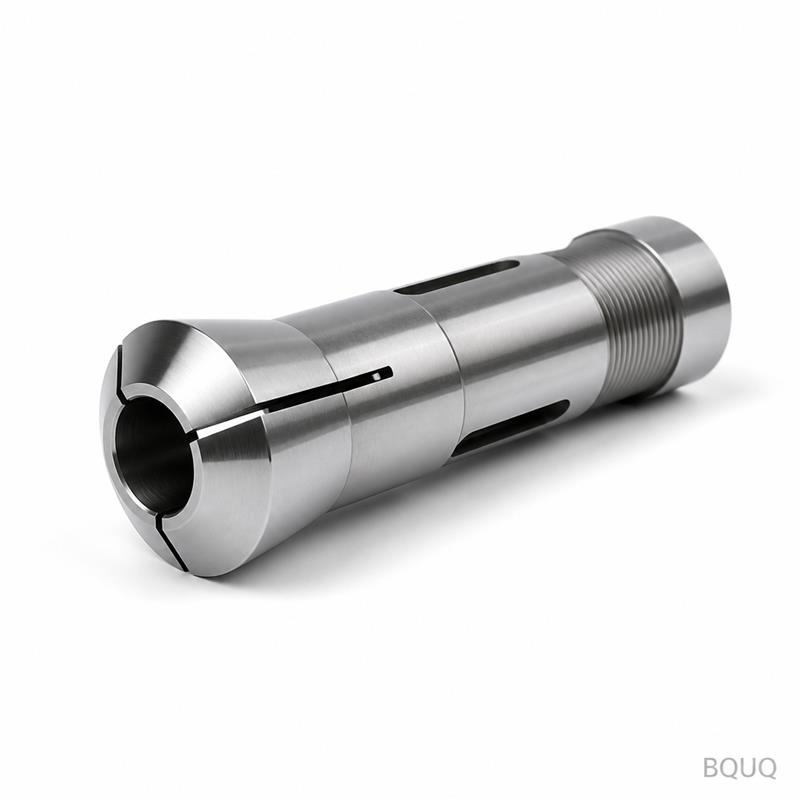
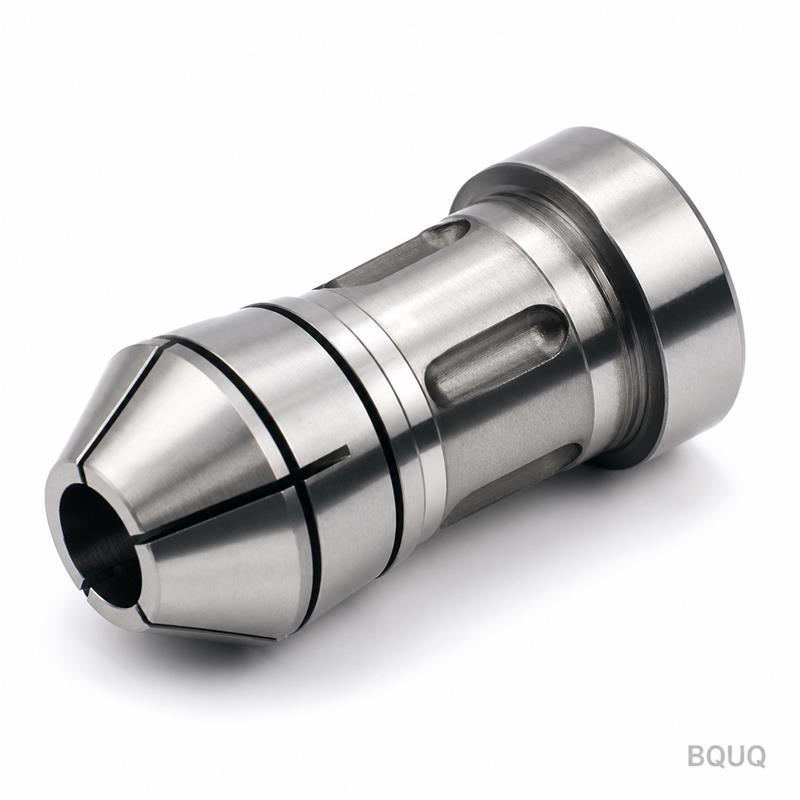
Custom CNC Collet Chuck Auto Lathe 25 Type Triangle Bar Stock
OpeningYour drawing defines the part. We machine it. Every collet is made to your exact dimensions, not a stock approximation. Before shipment, each unit is verified against your file with a CMM repor
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your drawing defines the part. We machine it. Every collet is made to your exact dimensions, not a stock approximation. Before shipment, each unit is verified against your file with a CMM report. You get a part that fits your spindle and holds your triangle bar stock without chatter.
Tolerance: ±0.005 mm on bore and slot width
Lead time: 7–10 working days for prototypes, 15 days for production runs
No MOQ — order one piece or one thousand
Material: 20CrMnTi or 40Cr, case-hardened to HRC 58–62
This is a 25-type collet for auto lathes, designed for feeding triangle (hexagonal or square) bar stock. The internal profile matches your stock geometry. The external taper matches your spindle nose. We cut it, heat-treat it, and grind it in one facility.
Specifications
Parameter
Value
Notes
Type
25-type auto lathe collet
Fits standard 25 mm spindle taper
Stock shape
Triangle, hex, square
Custom profile per drawing
Material
20CrMnTi, 40Cr, or 65Mn
Case-hardened or through-hardened
Hardness
HRC 58–62
Case depth 0.3–0.8 mm
Bore tolerance
±0.005 mm
Ground after heat treatment
Slot width
±0.01 mm
EDM wire-cut, burr-free
Taper angle
±0.02°
Verified with optical comparator
Surface finish
Ra 0.4 µm on bore, Ra 0.8 µm on taper
No grinding burns
Balancing
G2.5 at 6000 rpm
Available on request
Batch size
1–10,000 pieces
No MOQ, tooling cost shared
Inspection
100% dimensional check
CMM report per batch
Lead time
7 days prototype, 15 days production
Faster for repeat orders
Process: CNC turning of the blank, milling the slot, heat treatment, then centerless grinding of the OD and internal grinding of the bore. We do not outsource any critical step. This keeps tolerances tight and traceability simple.
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Each batch gets a unique heat number and a dimensional report. If you need to trace a part back to its raw material lot, we have the records. No mixing of batches, no guessing which heat treatment cycle a part went through. This matters when a collet fails at 8000 rpm — you want to know exactly why.
2. Inspection report per batch.
You do not have to trust us. We send a CMM inspection report with every shipment. It lists bore diameter, slot width, taper angle, and hardness for each sampled unit. For critical orders, we do 100% inspection and mark each collet with a serial number. You can verify everything on your end.
3. One factory for CNC + stamping + spring + heatsink.
Your collet is not the only part you need. If your assembly also uses a stamped retainer, a compression spring, or a heatsink for a motor driver, we make all of them under one roof. You get one supplier, one quality system, one shipping invoice. Fewer vendors means fewer delays and less paperwork.
Where these parts are used
Swiss-type and automatic lathes — feeding triangle bar stock for high-volume screw machining. The collet grips the stock firmly, preventing rotation during drilling and tapping.
Pneumatic and hydraulic collet chucks — used in secondary operations like slotting or cross-drilling on pre-formed parts. The triangle profile prevents the part from slipping under torque.
Medical device manufacturing — small titanium or stainless steel components where surface finish and dimensional repeatability are critical. A loose collet causes chatter marks that fail inspection.
Automotive fuel injector bodies — these require tight concentricity between the bore and the outer profile. Our collets hold the stock within 0.005 mm, so the machined part stays in spec.
Fastener and fitting production — hex and triangle stock for nuts, fittings, and valve components. The collet must open and close millions of cycles without fatigue cracking. We test our collets to 500,000 cycles before release.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototyping or 10,000 for production. Tooling cost is quoted separately and amortized over your order volume. For repeat orders, tooling is free after the first batch.
Q: How do you guarantee tolerance on the bore and slot?
A: We grind the bore after heat treatment, not before. This removes distortion from hardening. The slot is wire-cut after grinding, so it does not affect the bore geometry. Every part is measured with a CMM and the report is included in the shipment.
Q: What is your lead time?
A: Prototypes ship in 7–10 working days. Production runs of 500+ pieces ship in 15 working days. If you need faster, we can split the batch and ship partial orders. We keep common materials like 20CrMnTi in stock.
Q: Can you provide material certificates?
A: Yes. We supply mill certificates for raw material, heat treatment reports, and hardness test results. For aerospace or medical applications, we can provide full traceability with batch numbers and chemical composition analysis.
Send your drawing
Send us your PDF or STEP file. We will check the taper angle, bore profile, and slot width against our standard tooling. If we need a custom grinding wheel or wire electrode, we will tell you the cost before you commit. You get a firm quote within 12 hours.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, with no MOQ and verified quality. Your drawing, our machines, your parts.