OpeningYou need a collet chuck that holds tight at 6,000 RPM and repeats within microns. We machine it from your drawing, verify every critical dimension before shipment, and ship
Custom CNC Collet Chuck Auto Lathe 45 Type Round Bore | BQUQ
OpeningYou need a collet chuck that holds tight at 6,000 RPM and repeats within microns. We machine it from your drawing, verify every critical dimension before shipment, and ship it with a report you
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
You need a collet chuck that holds tight at 6,000 RPM and repeats within microns. We machine it from your drawing, verify every critical dimension before shipment, and ship it with a report you can file.
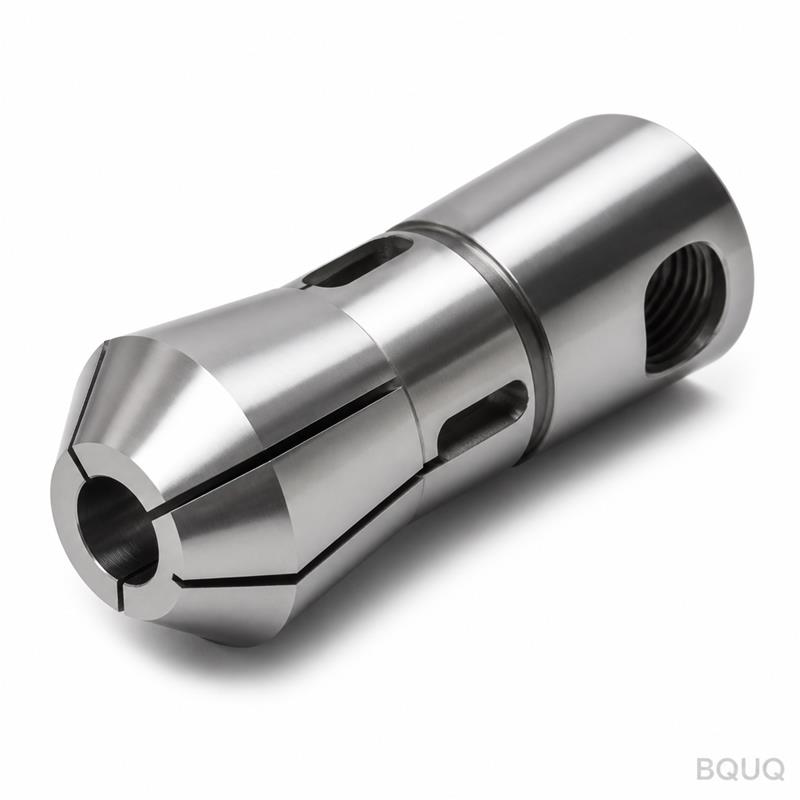
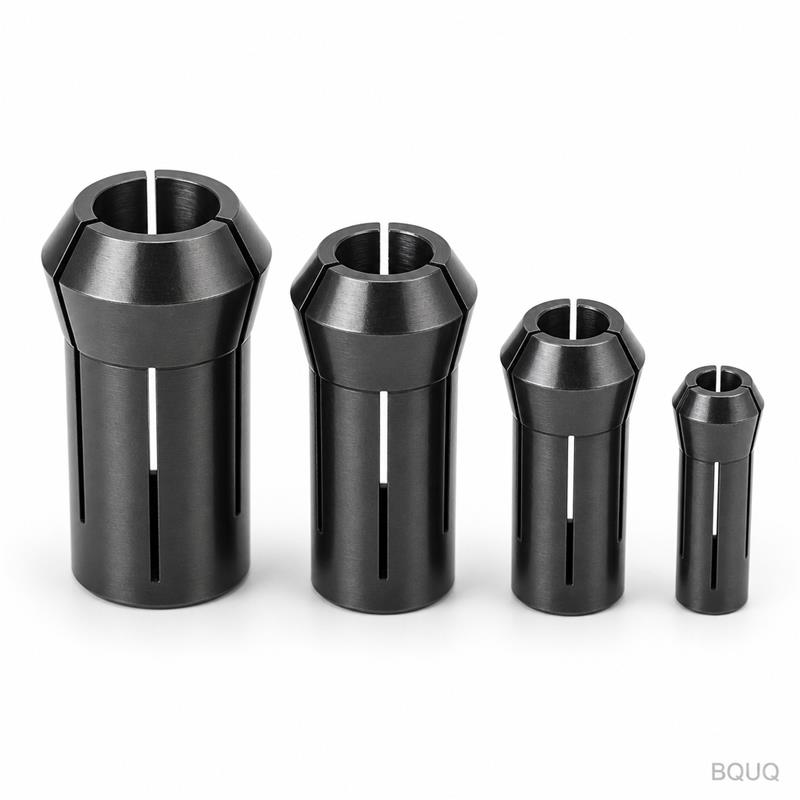
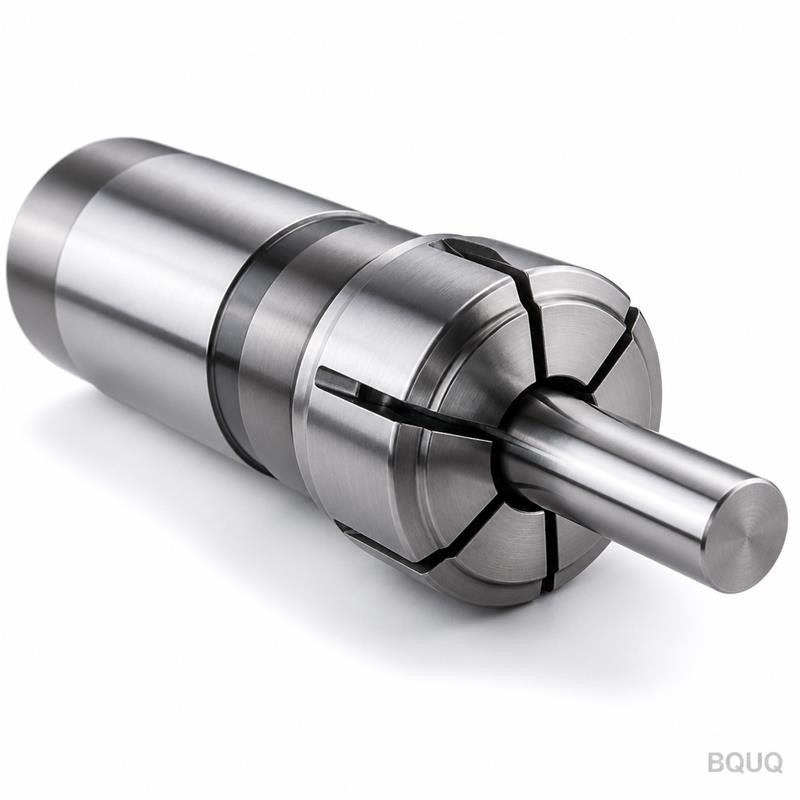
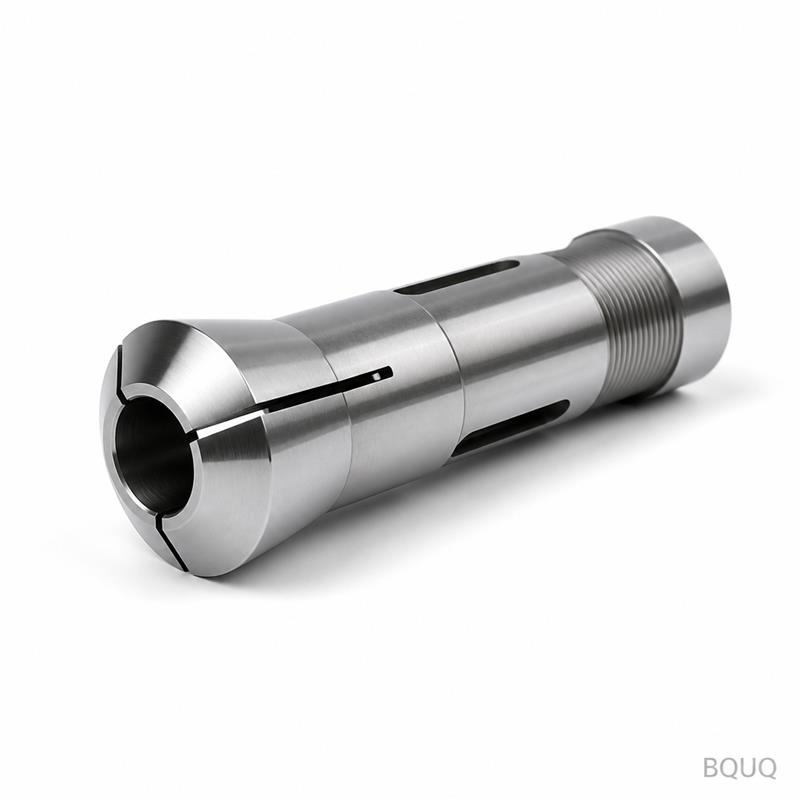
This is a 45-type round bore spring collet chuck for auto lathes. We make it to your print—bore diameter, taper angle, slot width, pullback force—not from a stock catalog.
Tolerance: ±0.005 mm on bore and taper
Lead time: 7–12 days for prototypes, 15–20 days for production runs
No MOQ—send one drawing or one thousand
Material certs and full inspection report included with every batch
If you are tired of chasing runout on your Swiss or sliding-head lathe, this is the part that fixes it.
Specifications
Parameter
Value
Type
45-type round bore spring collet chuck
Bore diameter range
3 mm – 45 mm (custom per drawing)
Taper angle
30° standard, custom angles available
Material options
65Mn spring steel, 60Si2Mn, 9Cr18 stainless, 20CrMnTi carburized
Hardness
HRC 45–52 (spring temper), case-hardened to HRC 58–62 on request
Surface finish
Ra 0.4 µm on bore and taper, black oxide or phosphate coating
±0.005 mm on bore, ±0.01 mm on slot width, concentricity ≤0.01 mm
Balancing
Dynamic balanced to G2.5 grade at 6,000 RPM
Batch size
1 piece to 10,000 pieces per order
Inspection
100% dimensional check on bore and taper; CMM report per batch
All collets are machined on Citizen and Tsugami CNC lathes, then ground on Studer cylindrical grinders. Slots are cut with wire EDM—no burrs, no heat-affected zones. We control the full process in one factory, from raw bar stock to final inspection.
Three reasons buyers send us their drawings
1. Batch-traceable quality, not a gamble.
Every collet gets a unique serial number. We record heat treatment batch, grinding wheel used, and inspector ID. If a problem shows up in your production line, you trace it back to the exact heat and shift. No guesswork.
2. Inspection report per batch, not a generic certificate.
You get a CMM report with actual measured values for bore, taper, and concentricity—not a "certificate of conformance" with no numbers. We also include hardness test results and material mill certificates. Your QA team can file these without re-verifying.
3. One factory for CNC machining, stamping, springs, and heat sinks.
Your collet chuck is not an isolated part. If your assembly needs a stamped retainer ring, a compression spring for the release mechanism, or a heat sink for the spindle drive, we make them under the same roof. One purchase order, one quality system, one shipping date. Fewer vendors, fewer excuses.
Where these parts are used
Swiss-type automatic lathes (Citizen, Star, Tsugami) for medical screw and implant production—where runout below 0.01 mm is non-negotiable.
Sliding-headstock lathes machining brass valve bodies and stainless fittings in high-volume runs.
Multi-spindle automatics in automotive fuel injector nozzle production, holding round stock at 8,000 RPM with coolant flood.
In-house job shops doing short-run precision turning, where quick changeover between bar diameters matters more than batch size.
Aerospace fastener lines making titanium bolts and pins, where material certs and traceability are audited by the customer.
In every case, the collet chuck is the last interface between the machine spindle and the workpiece. If it flexes, your part scrap. We design and grind it so it does not.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype validation at the same tolerance as a 10,000-piece run. The per-piece price is higher for single units, but the quality standard is identical.
Q: How do you guarantee tolerance and quality?
A: We grind the bore and taper on a Studer cylindrical grinder, then measure on a CMM with 0.001 mm resolution. Every collet is checked for concentricity and slot width. The inspection report is included with your shipment. If any dimension is out of spec, we remake the part at no cost.
Q: What is your lead time?
A: Prototypes (1–5 pieces): 7–12 days. Production runs (50+ pieces): 15–20 days. For urgent breakdowns, we can expedite a single piece in 72 hours at a 30% surcharge. We ship via DHL or FedEx, door to door.
Q: Do you provide material certificates?
A: Yes. Every batch ships with a mill certificate for the raw material, heat treatment records, and hardness test results. For aerospace or medical applications, we can provide full traceability to the melt origin.
Send your drawing
Stop guessing whether a stock collet will hold your bar stock. Send us your drawing and get a firm quote in 12 hours.
We are a precision manufacturing factory in Dongguan, China, with 20 years of experience in CNC machining, stamping, springs, and heat sinks. Your custom CNC collet chuck is made in China, but inspected to German and Japanese standards.
Email your PDF or STEP file to sc@bquq.com
WhatsApp: +86 13713157787 (we reply within one business hour, 8:00–20:00 Beijing time)
Include your bore size, taper angle, and target runout. We will reply with a price, lead time, and a technical review of your design—free of charge.