OpeningYour spindle deserves a tool holder that holds true. We machine BT30 ER collet chucks to your exact drawing, not from stock blanks. Every unit is verified before shipment. N
Custom CNC Collet Chuck Tool Holder | Precision BT30 ER Made in China
OpeningYour spindle deserves a tool holder that holds true. We machine BT30 ER collet chucks to your exact drawing, not from stock blanks. Every unit is verified before shipment. No surprises at your
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
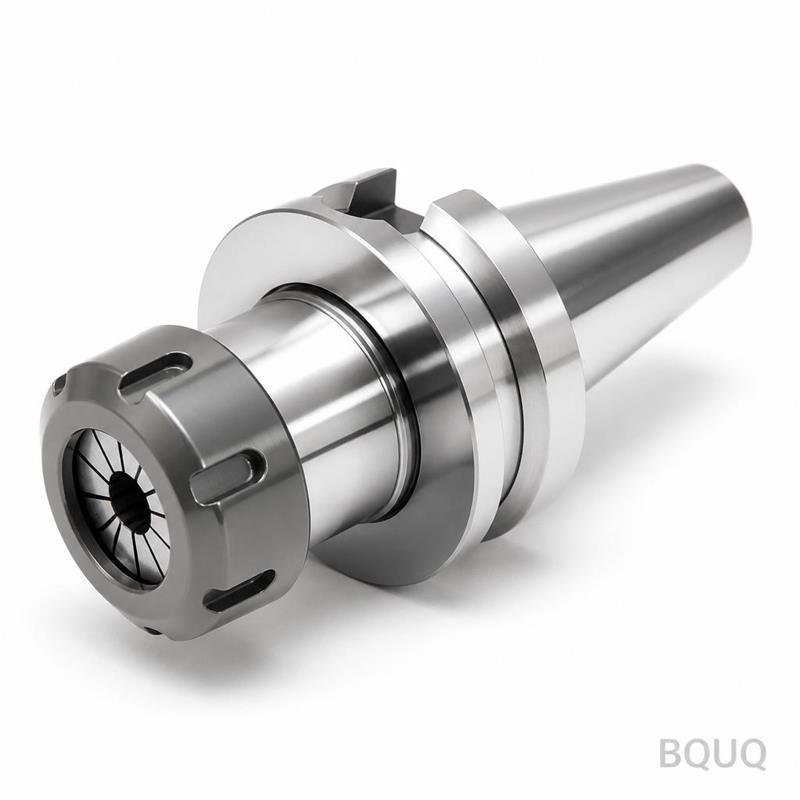
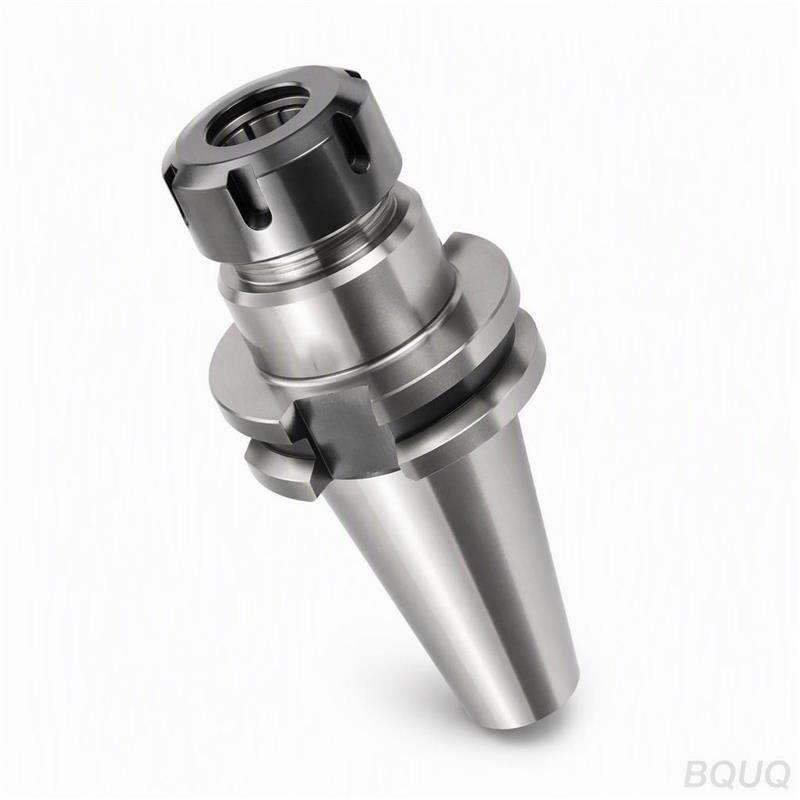
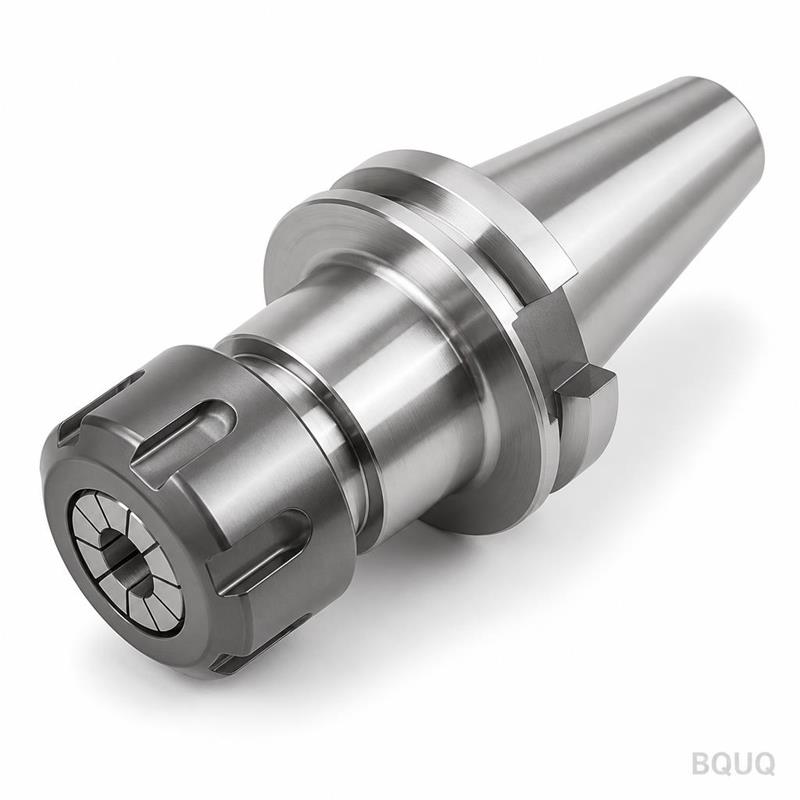
Your spindle deserves a tool holder that holds true. We machine BT30 ER collet chucks to your exact drawing, not from stock blanks. Every unit is verified before shipment. No surprises at your incoming inspection.
At a glance: Runout within 0.005 mm TIR at the nose, taper angle AT3 or better, lead time 15-20 working days, no MOQ. One part or one thousand, same process control.
Specifications
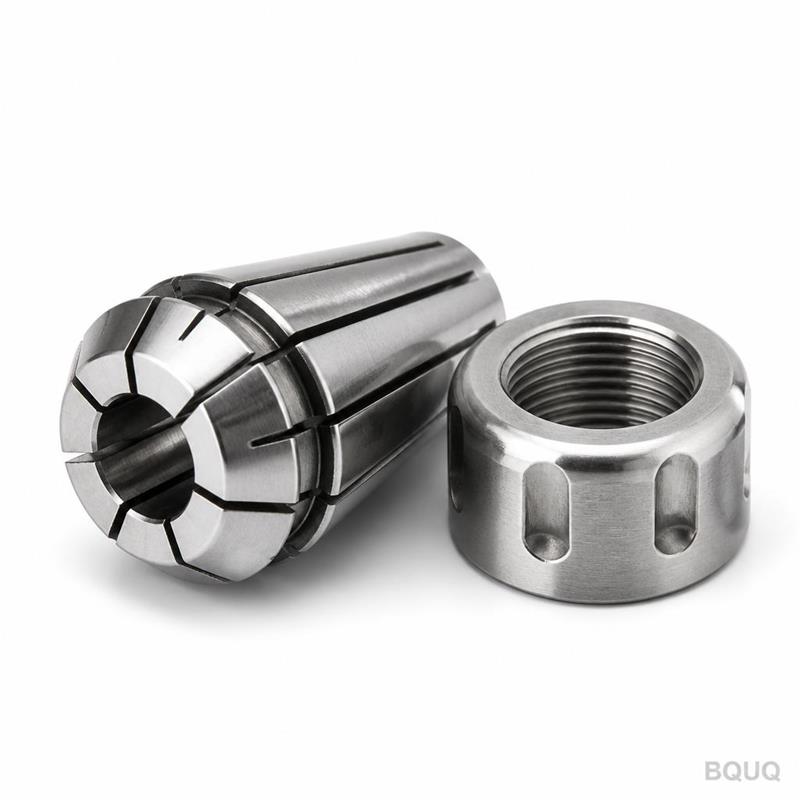
We run a dedicated CNC turning and grinding cell for collet chucks. The taper is ground, not turned. The thread is cut, not rolled. Here is what you get when you send us your print.
Parameter
Value
Available tapers
BT30, BT40, BT50 (CAT/DIN on request)
Collet type
ER11, ER16, ER20, ER25, ER32, ER40
Material
20CrMnTi or 8620 steel, case-hardened to 58-62 HRC
Taper accuracy
AT3 per ISO 1947, ground finish Ra 0.2 µm
Runout (TIR)
≤ 0.005 mm at nose, ≤ 0.010 mm at 4×D
Thread accuracy
6H internal, ground after heat treat
Surface finish
Black oxide, electroless nickel, or TiN coating
Balancing
G2.5 at 15,000 rpm standard, G1.0 optional
Inspection
100% dimensional check, CMM report per batch
Batch size
1 to 5,000 pieces, no MOQ
Lead time
15 days for prototypes, 20 days for production
Origin
Made in China, Dongguan factory
The grinding wheel is dressed before every batch. The CMM is calibrated weekly. We do not skip steps to hit a price.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality. Each collet chuck gets a unique serial number. We record heat treat lot, grinding wheel ID, and operator initials. If a problem appears in your toolroom, we trace it to the exact heat treat batch and machining shift. You get a corrective action report, not excuses.
2. Inspection report per batch. You receive a full dimensional report with every shipment. Taper angle, runout, thread pitch, hardness — measured values, not nominal values. Our QC team uses a Zeiss CMM and a Taylor Hobson roundness tester. The report is signed and archived for 5 years.
3. One factory for CNC, stamping, springs, and heat sinks. Your tool holder is not our only line. We run CNC machining, metal stamping, spring coiling, and heat sink fabrication under one roof. That means one purchase order for a complete assembly. One logistics contact. One quality system. If your project needs a spring-loaded collet mechanism or a stamped retention knob, we make it in-house.
Where These Parts Are Used
A BT30 ER collet chuck is not a shelf item. It is a working component in high-torque, high-speed machining. Here is where our customers use them.
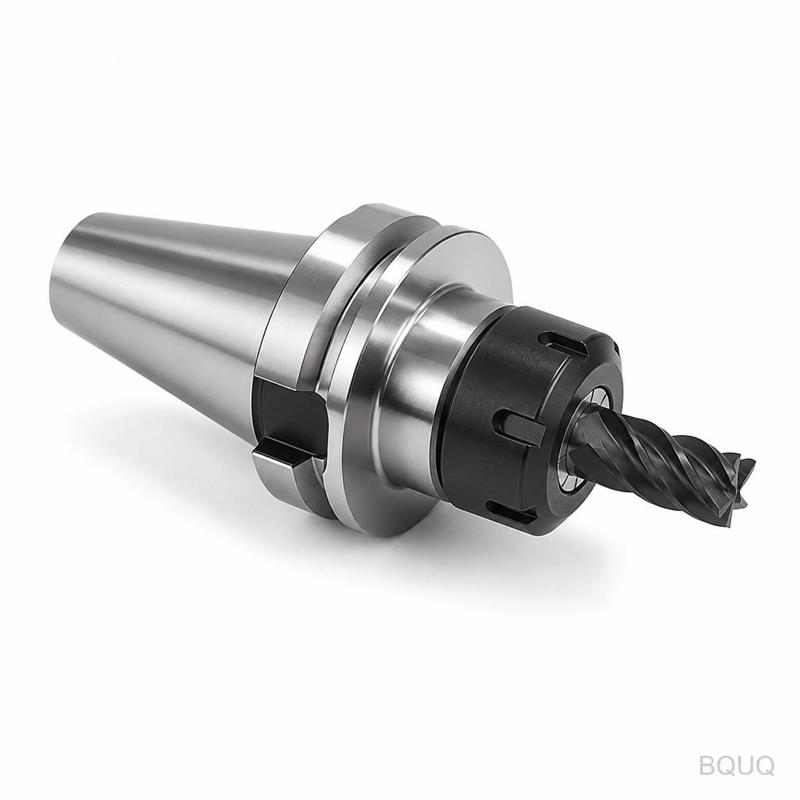
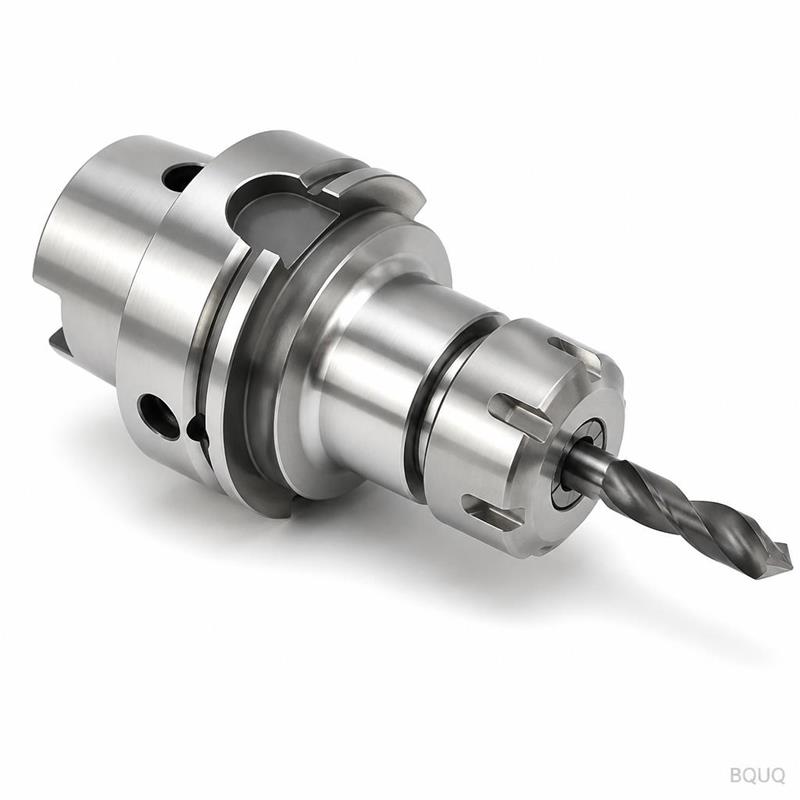
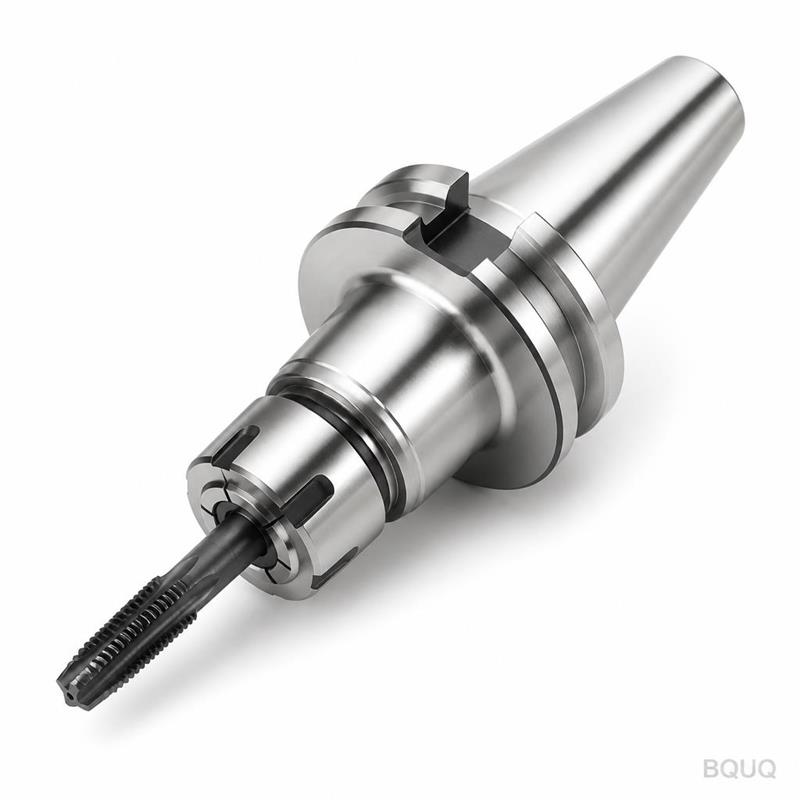
CNC machining centers — vertical and horizontal spindles for milling, drilling, and tapping. The ER collet holds drills and end mills from 1 mm to 26 mm.
Automotive production lines — transfer lines and machining cells for engine blocks and transmission housings. These run 24/7. Our chucks hold tolerance through 10,000+ tool changes.
Aerospace structural parts — aluminum and titanium machining where runout directly affects surface finish and tool life. A 0.005 mm TIR chuck extends tool life by up to 30% compared to a standard holder.
Die and mold shops — finishing passes on hardened steel. The ER collet's clamping force and concentricity reduce chatter marks.
Robotic deburring cells — where the tool holder must survive lateral forces without pulling the collet loose.
If your spindle takes a BT30 taper, we can make the chuck. If it takes something else, ask. We have made odd tapers for special spindles before.
Q: What is your MOQ?
A: No MOQ. We accept one piece for prototype validation. The setup cost is quoted separately for small batches, but the unit price drops significantly at 50 pieces and again at 200 pieces.
Q: How do you guarantee tolerance and quality?
A: We grind the taper and bore on the same setup to minimize error. Every chuck is checked for runout at the nose and at 4×D. The CMM report is included in the shipment. If any dimension is out of spec, we replace the part at no cost.
Q: What is the lead time for a custom BT30 ER collet chuck?
A: 15 working days for prototypes after drawing approval. Production batches of 100+ pieces take 20 working days. We can expedite to 10 days for an additional fee if your line is down.
Q: Do you provide material certificates and heat treat reports?
A: Yes. We supply mill certificates for the raw steel, heat treat curves, and hardness test reports. All documents are in English and stamped by our QC manager.
Send Your Drawing
Stop comparing generic catalogs. Send us your print and get a firm quote in 12 hours. We will confirm the taper, the collet size, and the runout spec before we quote. No hidden costs, no vague promises.
Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We reply within one business hour, Monday to Saturday. Precision manufacturing is our only business. Let us prove it with your part.