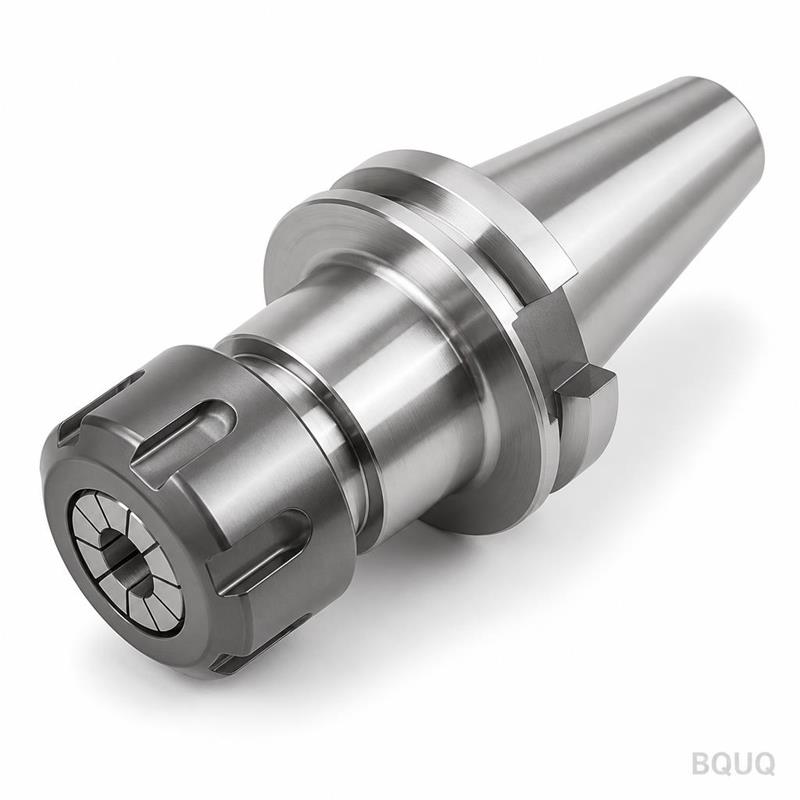
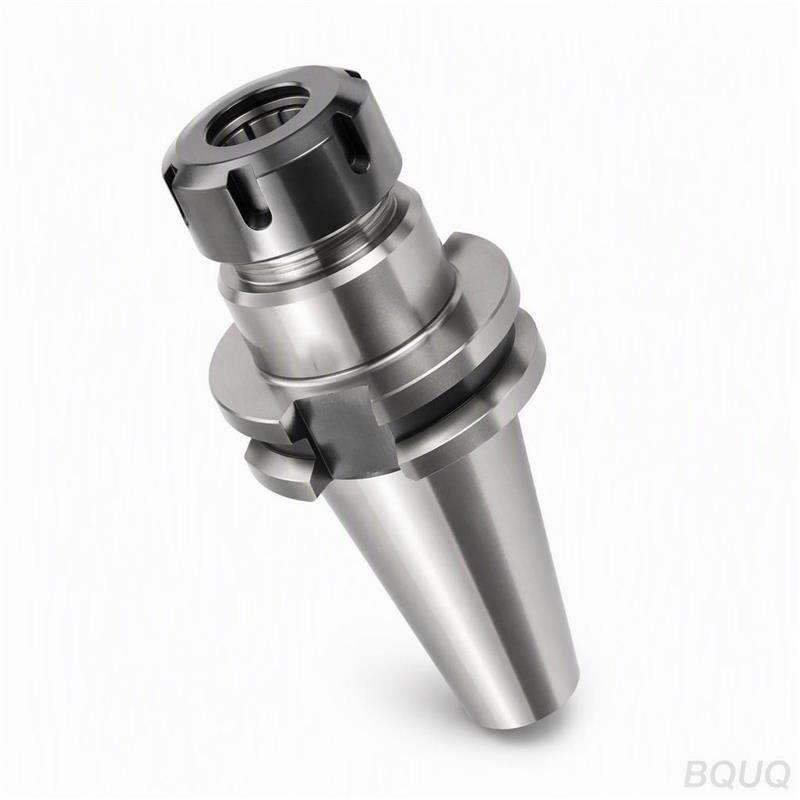
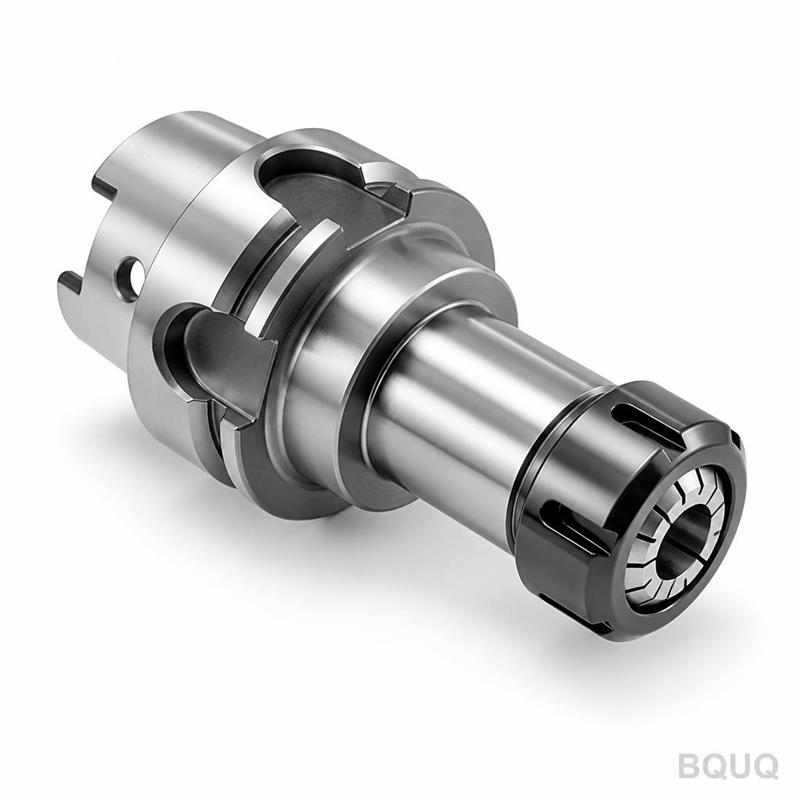
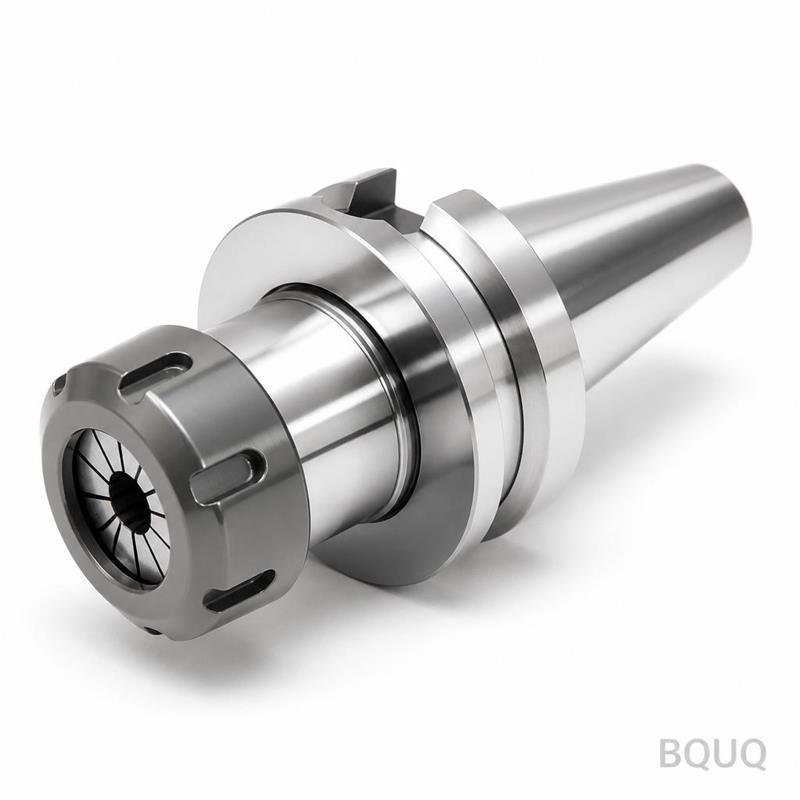
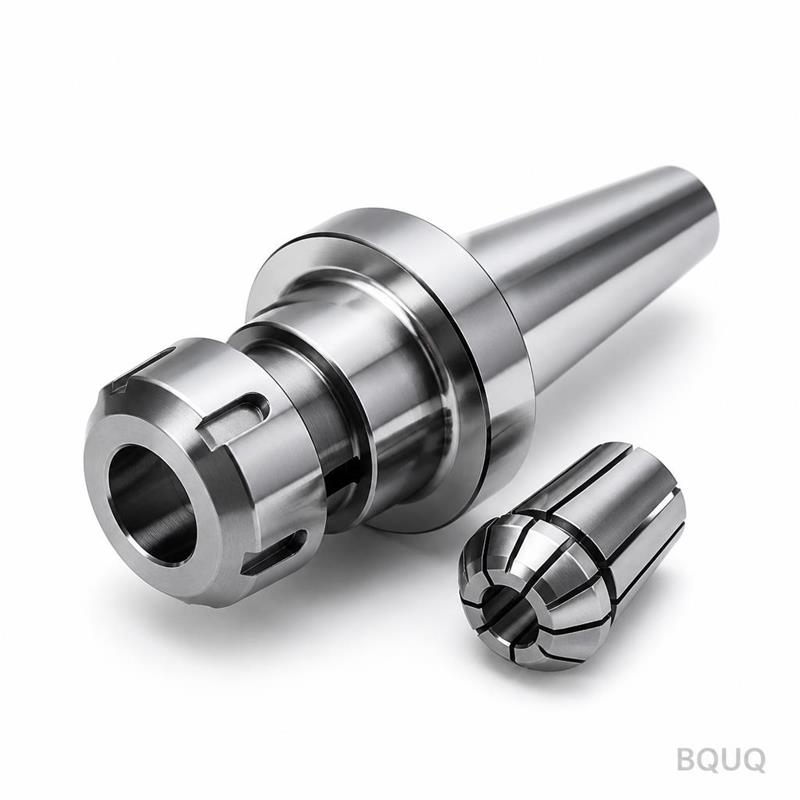
OpeningYour BT50 ER32 collet chuck starts as raw steel or alloy and ends as a precision tool holder verified on our own CMM before it ships. We machine the taper, the thread, and t
OpeningYour BT50 ER32 collet chuck starts as raw steel or alloy and ends as a precision tool holder verified on our own CMM before it ships. We machine the taper, the thread, and the collet seat in on
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your BT50 ER32 collet chuck starts as raw steel or alloy and ends as a precision tool holder verified on our own CMM before it ships. We machine the taper, the thread, and the collet seat in one setup to hold concentricity under 0.005 mm. Every unit is checked for runout and hardness, not sampled. Send us your drawing, and we will confirm the geometry, material, and coating within 12 hours.
At a glance: BT50 taper, ER32 collet seat, runout ≤ 0.005 mm, surface finish Ra 0.4, lead time 15–20 working days, no MOQ.
Specifications
We run a dedicated CNC turning and milling line for tool holders. The process is stable because we control the heat treatment and grinding in-house. Below are the standard parameters we hold for custom CNC collet chuck orders.
Parameter
Value
Material options
20CrMnTi, 40Cr, 42CrMo, 65Mn (or per drawing)
Hardness
58–62 HRC (carburized case depth 0.8–1.2 mm)
Taper accuracy
AT3 or better (BT50)
Runout (taper to collet seat)
≤ 0.005 mm
Surface finish
Ra 0.4 on taper, Ra 0.8 on body
Thread class
6H (ER32 collet nut thread)
Balancing
G2.5 at 15,000 rpm (optional)
Coating
TiN, TiAlN, or black oxide (optional)
Inspection
100% runout check, CMM report per batch
Lead time
15–20 working days after drawing approval
Batch size
1 piece to 5,000 pieces, no MOQ
We use CNC lathes with live tooling and cylindrical grinders for the final taper. The collet seat is ground after heat treatment to remove distortion. If you need a custom flange, coolant holes, or a special pull stud thread, we can add those features without changing the core process.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Each heat number and each batch gets a unique code. We keep records for 10 years. If you have a problem on your line, we can trace the material certificate, the machine operator, and the inspection data for that specific chuck. This is standard for our precision manufacturing work, not a paid extra.
2. Inspection report per batch. You get a dimensional report with actual measured values for taper angle, runout, hardness, and surface finish. We do not send a generic "passed" sheet. The report lists the CMM results for every critical dimension on your drawing. This saves your incoming QC time.
3. One factory for CNC, stamping, springs, and heat sinks. Your tool holder is not a standalone part. You might need a spring for the collet, a stamped retainer, or a heat sink for a nearby electronic module. We make all of those in the same building. You deal with one quality system, one shipping desk, and one invoice. This cuts your supplier management cost.
Where these parts are used
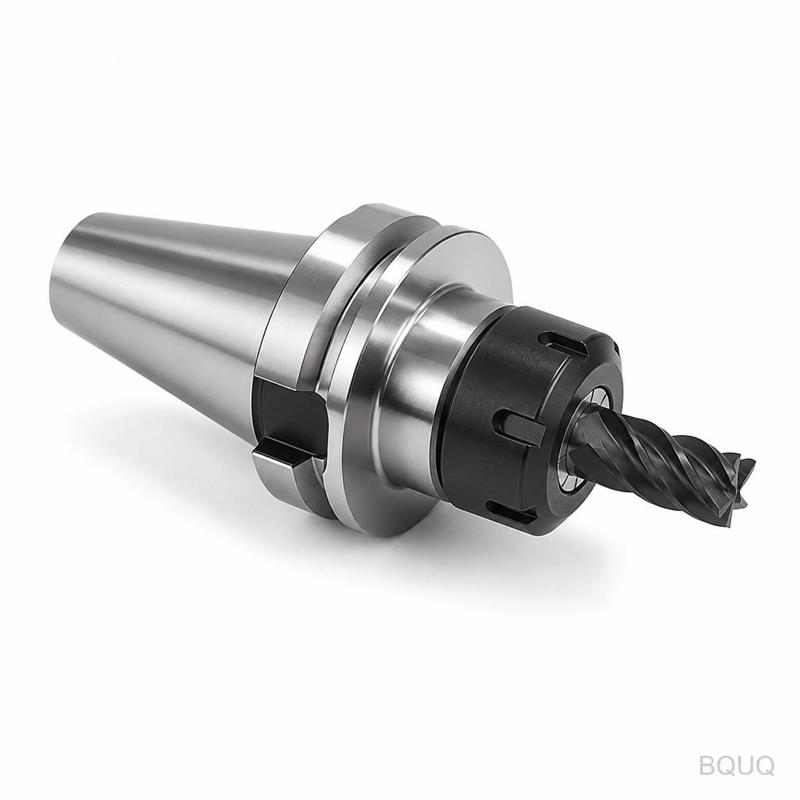
A heavy duty BT50 ER32 collet chuck is not a light-duty accessory. You will find it in CNC machining centers and milling machines that remove metal at high torque. Typical applications include:
Automotive powertrain machining: Boring and milling engine blocks, cylinder heads, and transmission housings where rigidity is critical.
Mold and die shops: Finishing hardened steel cavities where any runout shows up as a visible mismatch on the polished surface.
Aerospace structural parts: Aluminum and titanium frame components that require long reach and stable clamping at high spindle speeds.
Heavy equipment manufacturing: Hydraulic valve bodies, gear housings, and large bracket milling where the tool holder must absorb vibration.
General job shops: Replacing worn or low-cost holders with a custom unit that matches your exact pull stud length and projection.
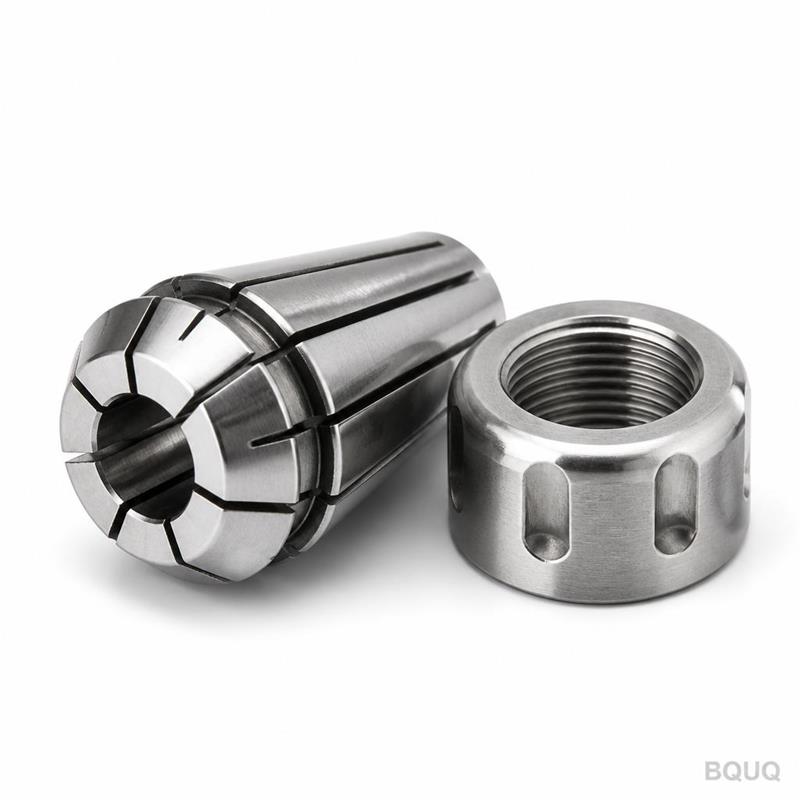
The ER32 collet system gives you a clamping range of 2 mm to 20 mm. Combined with a BT50 shank, it is a common choice for machines with 50-taper spindles that need a rigid but flexible toolholding solution.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype validation or 5,000 pieces for production. The unit price drops with quantity, but the quality process is identical.
Q: How do you guarantee tolerance and runout?
A: We grind the BT50 taper and the ER32 seat in the same clamping setup. Every chuck is measured on a CMM for taper angle and runout. We reject any unit above 0.005 mm runout, and we include the measured values in your batch report.
Q: What is your lead time for a custom design?
A: Standard lead time is 15–20 working days after you approve the drawing and we confirm material. If you need a sample quickly, we can rush a single piece in 7 working days for an additional fee. We will quote both options.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply mill certificates for the raw material, a hardness test report, and a heat treatment batch record. All documents are in English and can be notarized if your customer requires it.
Send your drawing
We give firm quotes within 12 hours. Send us your drawing in STEP, IGES, PDF, or even a hand sketch with dimensions. We will confirm the material, tolerances, coating, and price. No MOQ, no hidden tooling charges.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Your custom CNC collet chuck, made in China with full traceability, is one message away.