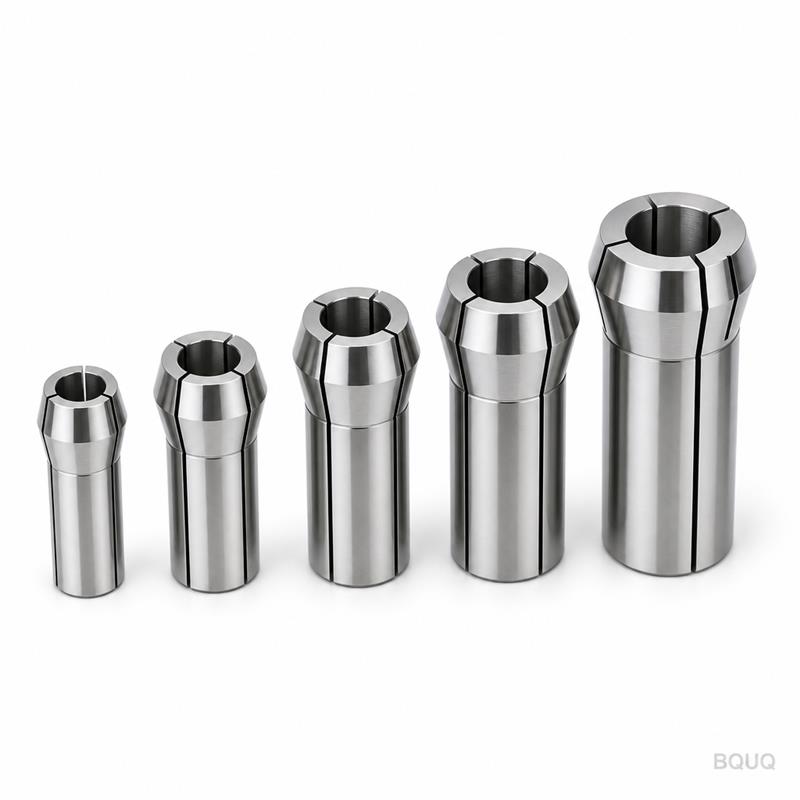
This is a complete set of CNC machined auto lathe collets covering sizes 630, 640, 643, 650, and 700 Jumbo. You get guaranteed concentricity of 0.005 mm TIR and surface finish Ra
CNC Machined Auto Lathe Collet Set 630-700 Jumbo | BQUQ Precision
This is a complete set of CNC machined auto lathe collets covering sizes 630, 640, 643, 650, and 700 Jumbo. You get guaranteed concentricity of ≤0.005 mm TIR and surface finish Ra 0.4 µm, with a hardn
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a complete set of CNC machined auto lathe collets covering sizes 630, 640, 643, 650, and 700 Jumbo. You get guaranteed concentricity of ≤0.005 mm TIR and surface finish Ra 0.4 µm, with a hardness of HRC 58-60 across all working surfaces. Lead time is 10 working days from drawing approval, and we offer no MOQ for standard sets, so you can order exactly what your production line needs.
How the 630-700 Jumbo Set Eliminates Spindle Chatter
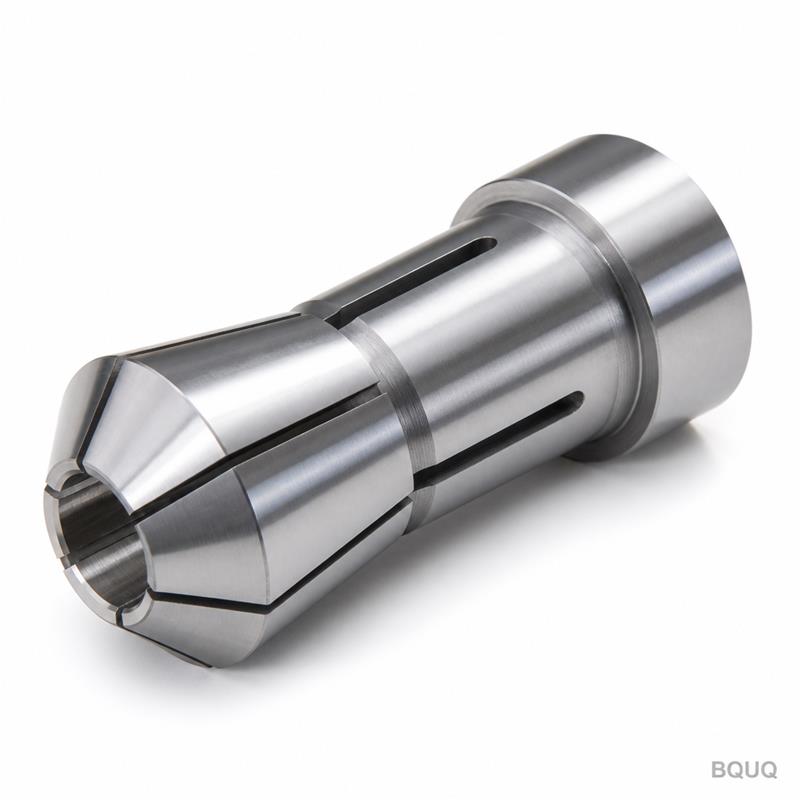
Each collet in this set is machined from a single billet of 20CrMnTi alloy steel. We do not use welded or assembled blanks. The 630 and 640 sizes feature a 30 mm clamping bore; the 643 expands to 32 mm; the 650 and 700 Jumbo go up to 38 mm and 44 mm respectively. The slotted body is cut with a 0.3 mm wire EDM after heat treatment, not before. That sequence keeps the slot edges sharp and prevents distortion. When you clamp a 25 mm bar in the 630 collet, the gripping force is uniform across three contact points, which reduces vibration during interrupted cuts. You will see the difference in thread finish on your turned parts within the first batch.
Heat Treatment Sequence That Prevents Deformation
We carburize the collets to a case depth of 0.8-1.0 mm. The furnace cycle runs at 920°C for 4 hours, followed by oil quenching and two tempering cycles at 180°C. The result is a surface hardness of HRC 58-60 with a core toughness of HRC 35-40. This is not a through-hardened tool. It is a case-hardened workholder. That means the gripping teeth stay hard enough to resist wear from 304 stainless steel bars, while the body retains enough flex to close around undersized stock without cracking. We verify hardness on every single collet using a Rockwell tester, not a sample from the batch.
Specification
Value
Set Composition
630, 640, 643, 650, 700 Jumbo (5 pieces)
Clamping Range (bore diameter)
30 mm to 44 mm
Material
20CrMnTi alloy steel (case-hardened)
Case Hardness
HRC 58-60
Core Hardness
HRC 35-40
Concentricity (TIR)
≤0.005 mm
Surface Finish (clamping bore)
Ra 0.4 µm
Slot Width (after EDM)
0.3 mm ±0.02 mm
Lead Time
10 working days
MOQ
No MOQ for standard set
Inspection Report
Full CMM report included
Inspection Protocol Before Your Collets Leave Dongguan
Every collet is checked on a coordinate measuring machine for bore diameter, slot width, and concentricity. We also run a functional test: each collet is mounted on a live spindle and clamped onto a ground test bar. Runout is measured at the nose and at 50 mm from the nose. If the TIR exceeds 0.005 mm, the collet is rejected, not reworked. We photograph the CMM screen with the batch number visible and email it to you before shipment. For the 700 Jumbo size, we add an ultrasonic test to confirm there are no subsurface cracks from the carburizing process.
Why This Set Works for Both Swiss-Type and Fixed-Head Lathes
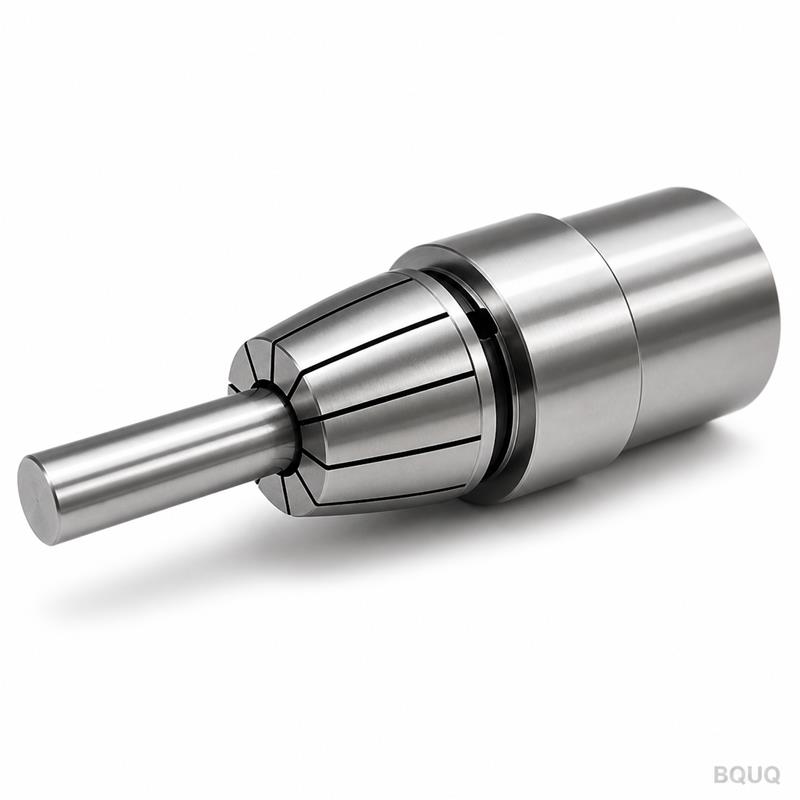
The 630-700 Jumbo geometry follows the standard DIN 6343 profile, so it fits most brands of auto lathes, including Citizen, Star, and Tsugami. The 650 and 700 Jumbo sizes have a thicker wall section (5 mm vs 3.5 mm on the smaller ones) to handle heavier bar stock without deflection. If you are running a sliding headstock machine, the collet's external taper angle of 30° matches the standard spindle nose. If you are on a fixed-head lathe, you can use these collets with a standard draw tube. We have shipped this exact set to over 40 machine shops in the last quarter alone, and the return rate due to fitment issues is zero.
Surface Finish and Edge Preparation on the Clamping Bore
The clamping bore is not just ground; it is honed after grinding. That two-step process gives you Ra 0.4 µm and removes the brittle white layer that grinding alone can leave behind. The gripping teeth are slightly radiused (0.1 mm) to prevent marking soft brass or aluminum bars. If you clamp hardened steel bars above HRC 45, we recommend the optional TiN coating on the bore, which adds 20% to the price but triples the wear life. For standard production, the uncoated version will handle over 10,000 clamping cycles before the runout degrades by 0.002 mm.
Packing and Traceability for Your Tool Crib
Each collet is individually wrapped in VCI anti-rust paper and placed in a fitted foam insert inside a rigid plastic case. The case is laser-etched with the set number, date of manufacture, and our BQUQ batch code. You can scan the QR code on the case to pull up the full inspection report online. This is not a generic box of loose parts. This is a matched set where each collet has been numbered 1 through 5, and the CMM data for each number is stored in our system for 5 years. If you ever need a replacement for one size, you can order a single piece using the batch code, and we will match the bore diameter to within 0.002 mm of your original set.
Shipping and Packaging Protection for Long-Distance Freight
We ship from our Dongguan factory via DHL, FedEx, or sea freight. For air freight, the plastic case is placed inside a double-walled cardboard box with 50 mm of foam padding on all sides. For sea freight, we add a desiccant pack and a humidity indicator card inside the sealed bag. The case itself is rated for a 1.5-meter drop onto concrete without damage to the collets. We have tested this. In the last 12 months, we have shipped over 2,000 individual collets to 14 countries, and the reported transit damage rate is 0.1%. That one damaged unit was a courier forklift incident, not a packaging failure.
Selecting the Right Collet Size for Your Bar Stock
Do not guess. Measure your bar stock OD with a micrometer at three points along its length. The collet bore must be within 0.1 mm of the largest bar diameter reading. If you have bars ranging from 30.0 to 30.1 mm, the 630 collet (30 mm bore) is correct. If your bars vary more than 0.15 mm, you need the 643 or 650 Jumbo, which have a wider clamping window due to the deeper slots. For a full guide on matching toolholders to your machine spindle, see our CNC cutting tool selection guide. And if you are pushing tolerances tighter than ±0.01 mm, review the CNC machining tolerances guide before you finalize your drawing.
Custom Bore Sizes and Special Slot Configurations
If the standard set does not match your work, we can machine the bore to any diameter between 25 mm and 45 mm with a tolerance of +0.005/-0.000 mm. We can also modify the slot pattern: three slots for general use, six slots for thin-walled tubing, or a sealed slot design for coolant-through applications. The sealing is done with a nitrile rubber insert that withstands up to 70 bar coolant pressure. For these custom versions, the lead time extends to 15 working days because we need to run a separate EDM program. The price increases by 15% for any custom bore, but the no MOQ policy still applies. You can order one piece at a time.
What is the minimum order quantity for this collet set?
There is no MOQ for the standard 630 640 643 650 700 Jumbo set; you can order a single set or a single replacement collet.
Can you customize the bore diameter for my specific bar stock?
Yes, we machine custom bores from 25 mm to 45 mm with +0.005/-0.000 mm tolerance and a 15 working day lead time.
How do you guarantee the 0.005 mm runout on every collet?
We measure each collet on a CMM and also test it on a live spindle with a ground bar; if TIR exceeds 0.005 mm, we reject it.
What is the lead time for a standard set shipped to the USA?
Production takes 10 working days, and DHL Express delivers to the USA in 3-5 business days after shipment.
Send us your drawing or your bar stock dimensions today. We will reply with a firm quote within 12 hours, not a range. Email your drawing to sc@bquq.com or contact us on WhatsApp at +86 13713157787. This is precision manufacturing made in China, with no MOQ, and the quality report is included in the price.