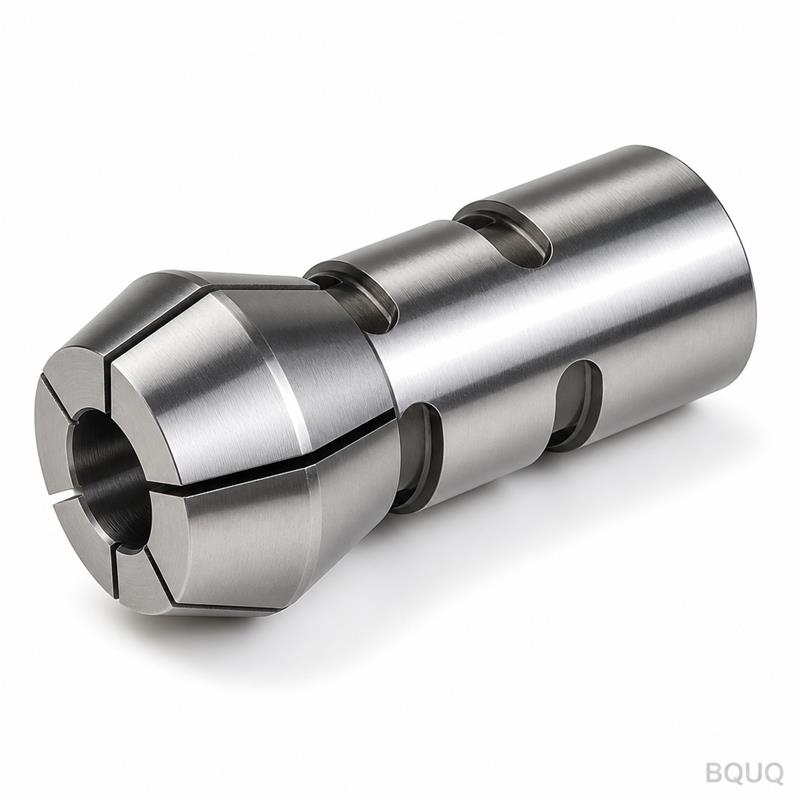
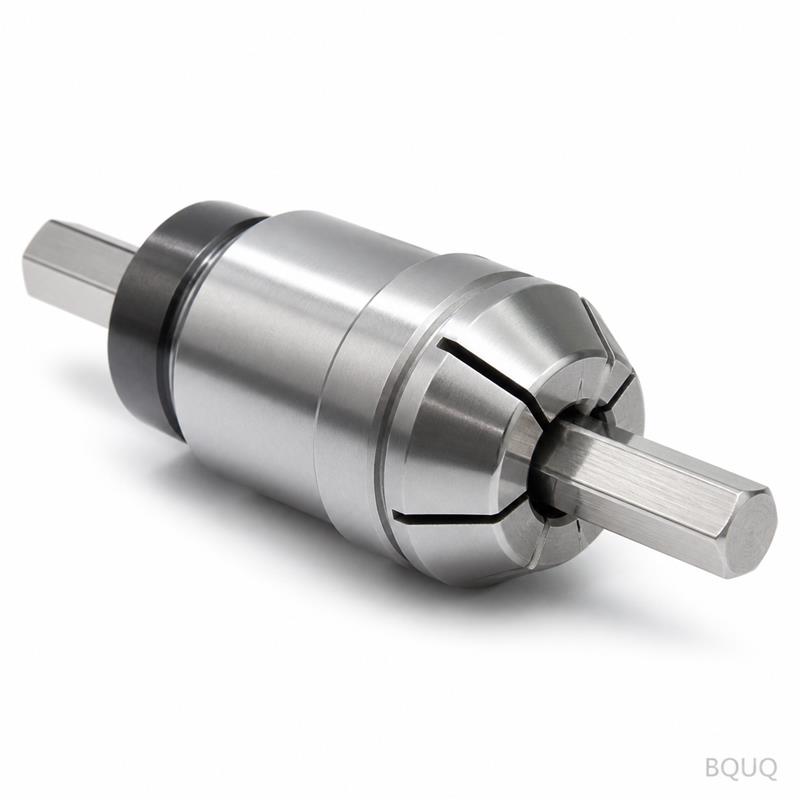
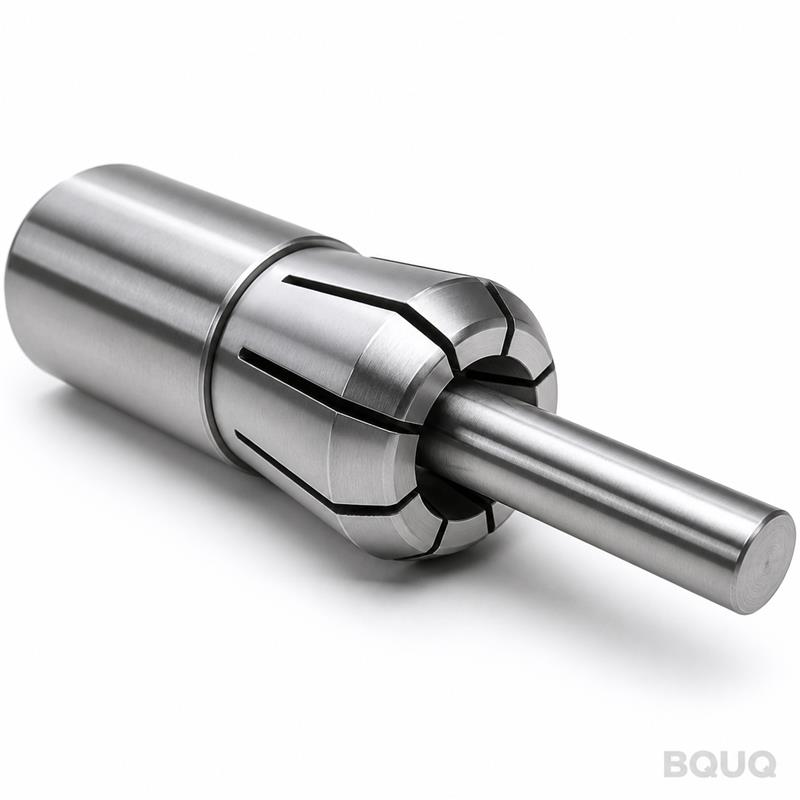
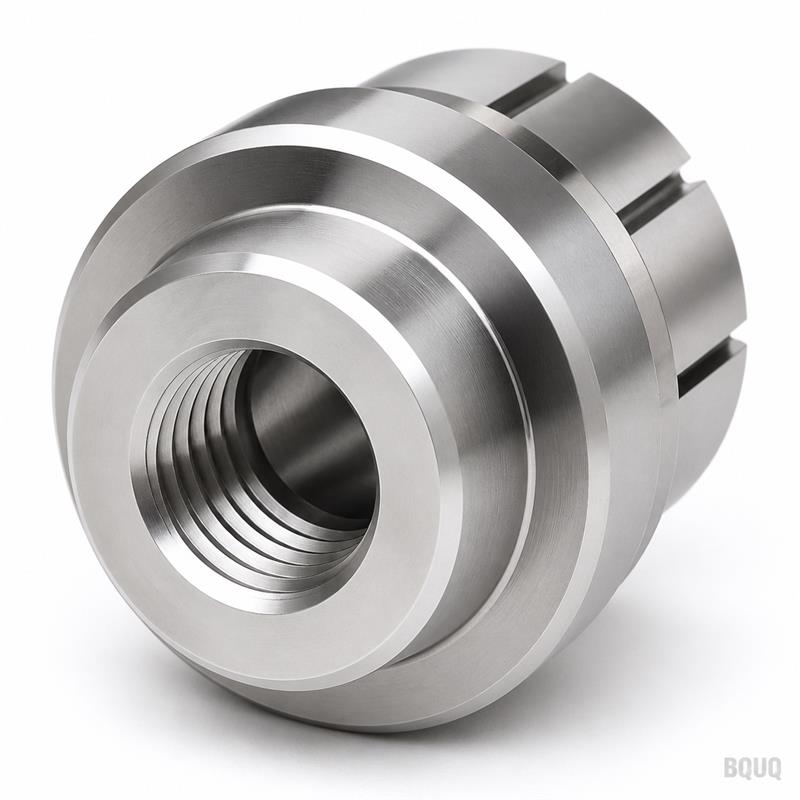
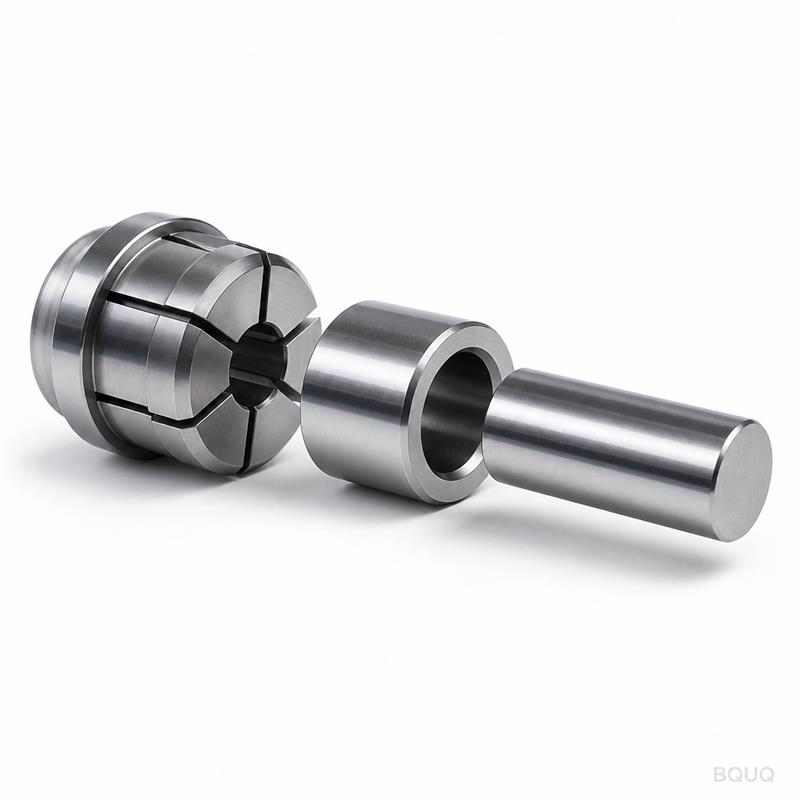
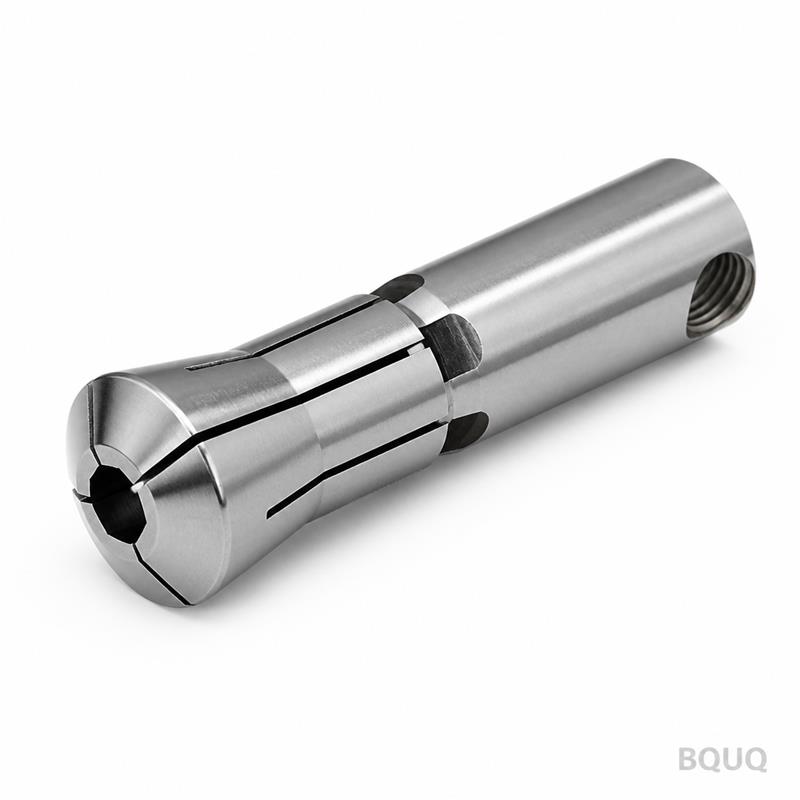
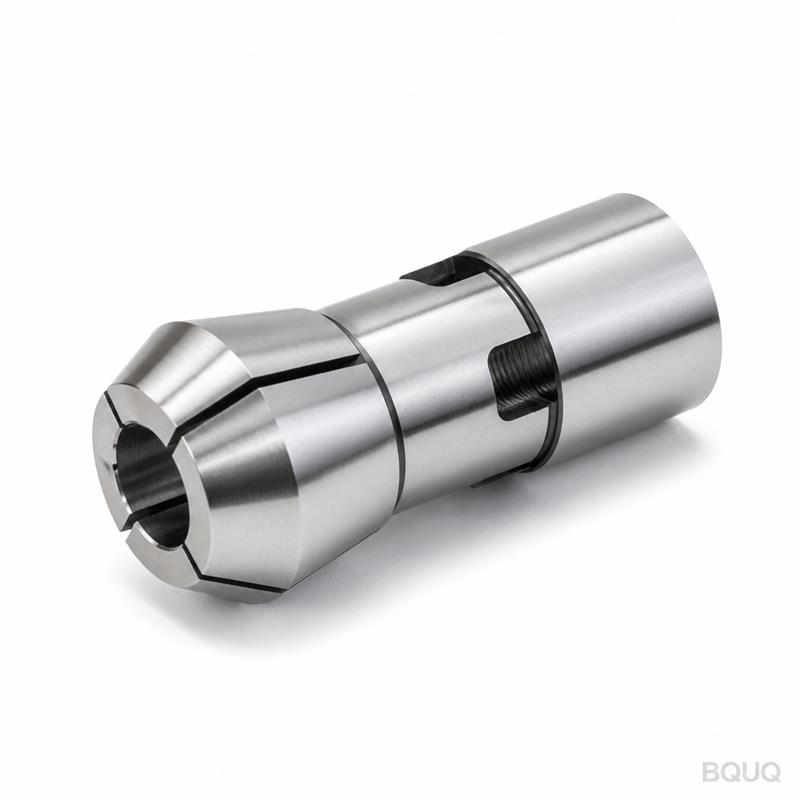
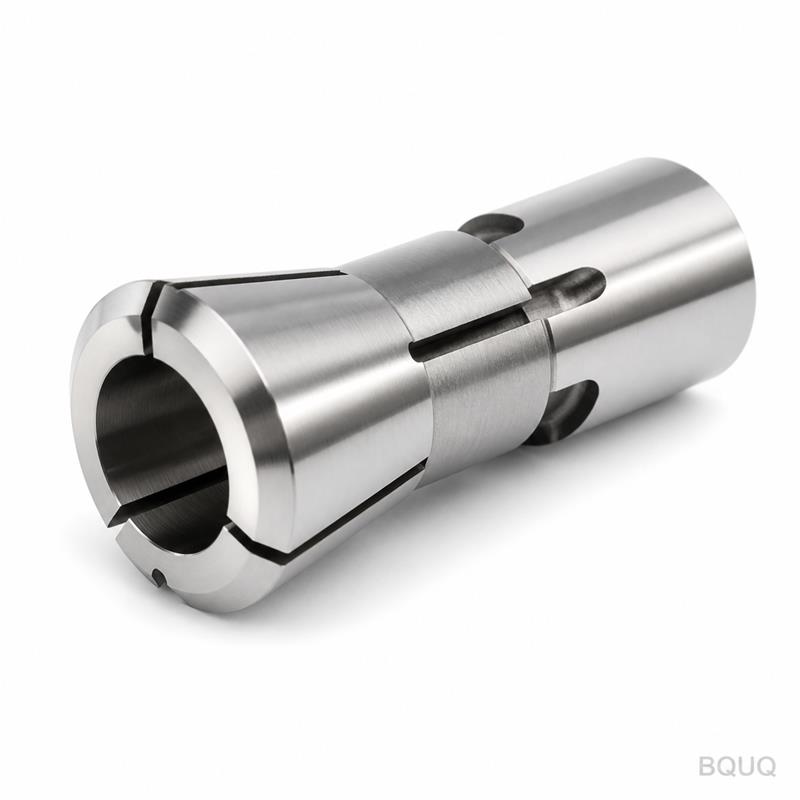
BQUQ CNC Machined Auto Lathe 18 Type Round Bore Spring Collet Chuck
What This 18 Type Collet Chuck Does in Your Spindle This is a CNC machined auto lathe 18 type round bore spring collet chuck. It grips round bar stock from 3 mm to 18 mm with a guaranteed runout of 0
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This 18 Type Collet Chuck Does in Your Spindle
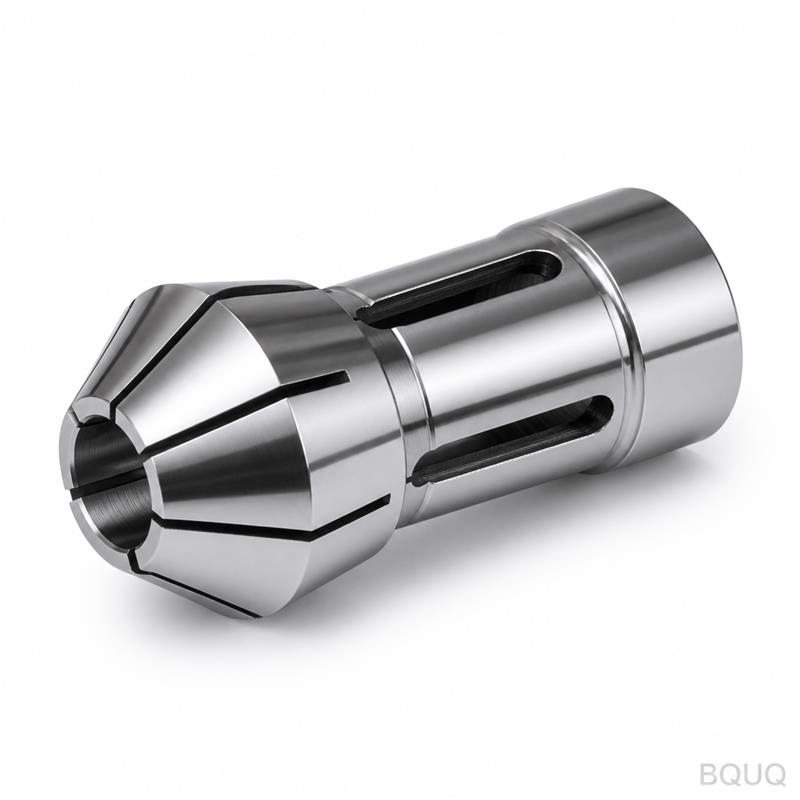
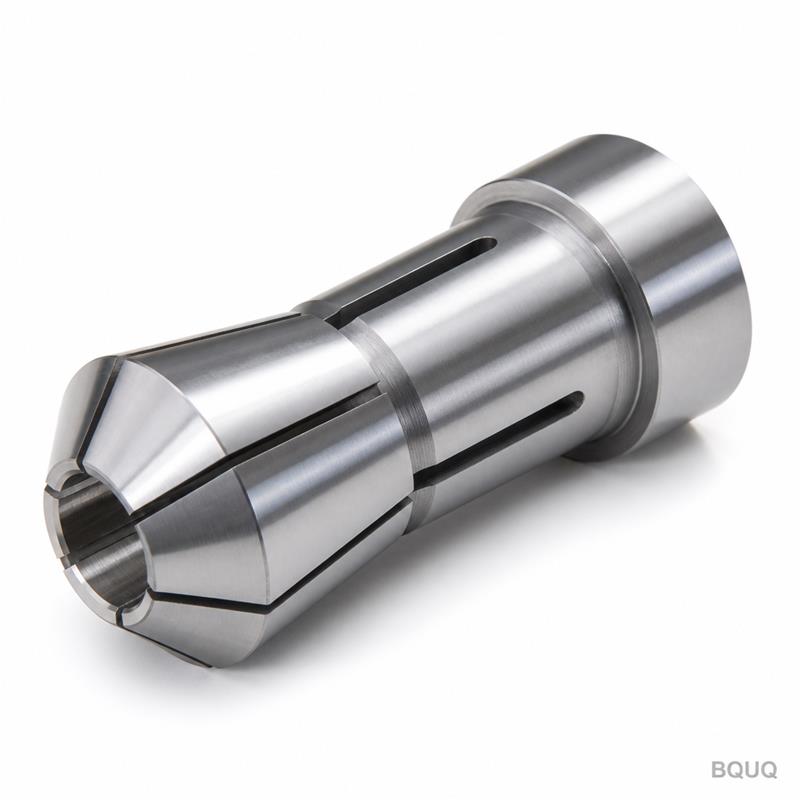
This is a CNC machined auto lathe 18 type round bore spring collet chuck. It grips round bar stock from 3 mm to 18 mm with a guaranteed runout of 0.005 mm TIR at the nose. Hardness is 58 HRC on the gripping surface, so it holds up through 1,500 hours of continuous high-speed turning. Lead time is 7 days for standard sizes, and we ship from our Dongguan factory with no MOQ.
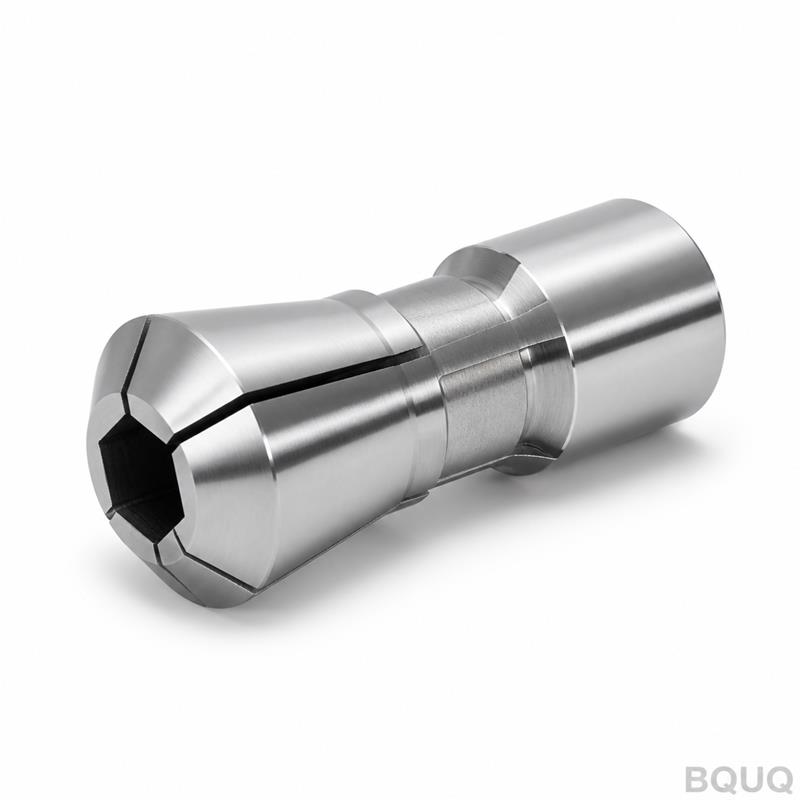
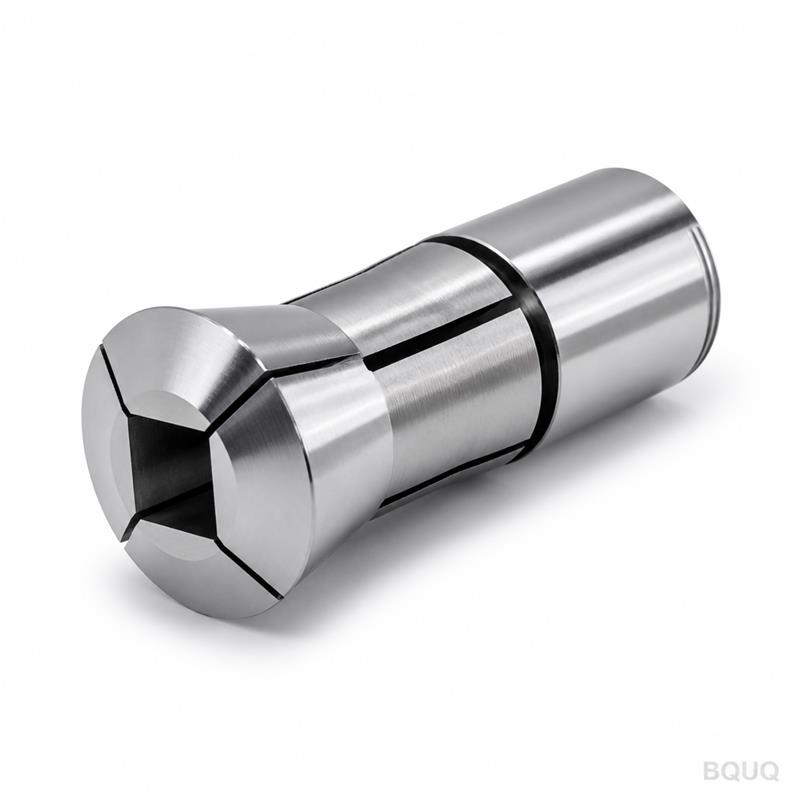
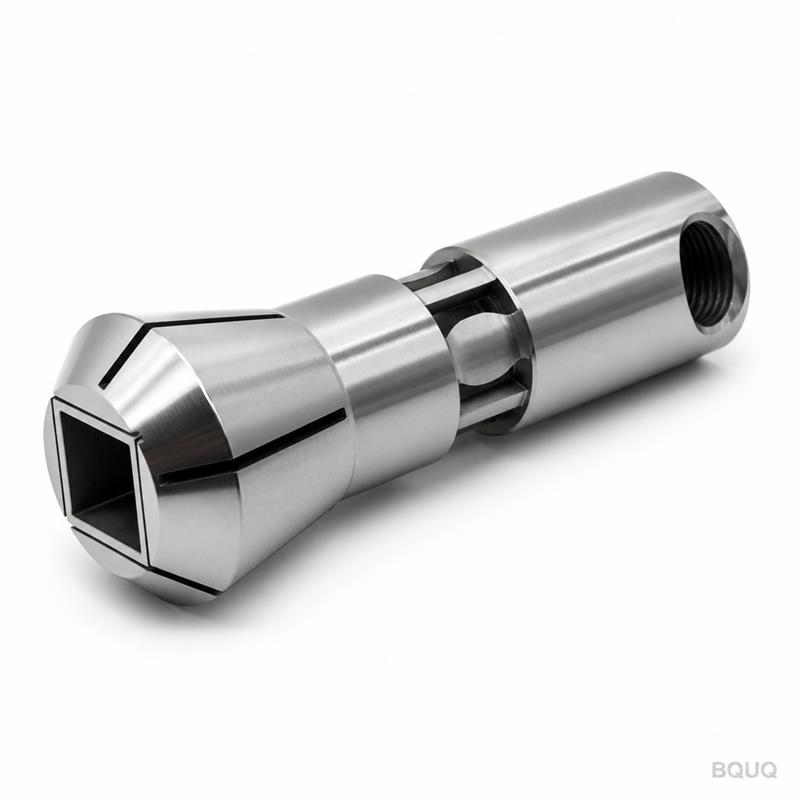
Why an 18 Type Round Bore Grip Beats a Hex or Square Collet
The round bore is cut in a single pass on a CNC lathe, then ground to a 0.002 mm circular tolerance. That means your bar stock sits dead-center every cycle, no matter if it’s 3 mm or 18 mm. The spring slot is wire-cut, not milled, so the flex is uniform around the circumference. You get repeatable clamping force of 4.2 kN at 80 psi air pressure, with zero marking on soft brass or aluminum.
Materials and Heat Treatment We Use for the 18 Type Chuck
We start with 8620 alloy steel, not cheap 1045. The body is carburized to a case depth of 0.8 mm, then hardened to 58–60 HRC. The spring segments are tempered at 350°C for 2 hours to keep them elastic without cracking. The bore is honed after hardening, not before, so the final roundness is 0.002 mm. Surface finish on the gripping area is Ra 0.4 µm, and the back taper is ground to 1.5° for a positive seat in your spindle.
Exact Specs for the Auto Lathe 18 Type Round Bore Spring Collet Chuck
Model
BQUQ-18RT (round bore, spring type)
Gripping range
3.0 mm – 18.0 mm (round stock only)
Body material
8620 alloy steel, carburized
Hardness
58–60 HRC (case depth 0.8 mm)
Runout at nose
0.005 mm TIR (max)
Bore tolerance
+0.005 / -0.000 mm
Surface finish (grip area)
Ra 0.4 µm
Clamping force
4.2 kN at 80 psi air
Max spindle speed
6,000 RPM
Lead time
7 days standard, 3 days rush
MOQ
No MOQ – order 1 piece
Inspection Before Every Shipment – Not a Random Sample
Each 18 type chuck goes through a 3-step QC pass. First, we measure runout on a TIR gauge with a master test bar – if it exceeds 0.005 mm, it’s scrapped. Second, we check hardness on a Rockwell tester at three points around the bore. Third, we do a functional grip test with a 12 mm steel bar at 80 psi. You get a signed inspection report with the part number and measured values, not a certificate of conformity.
How This Chuck Mounts to Your Auto Lathe Spindle
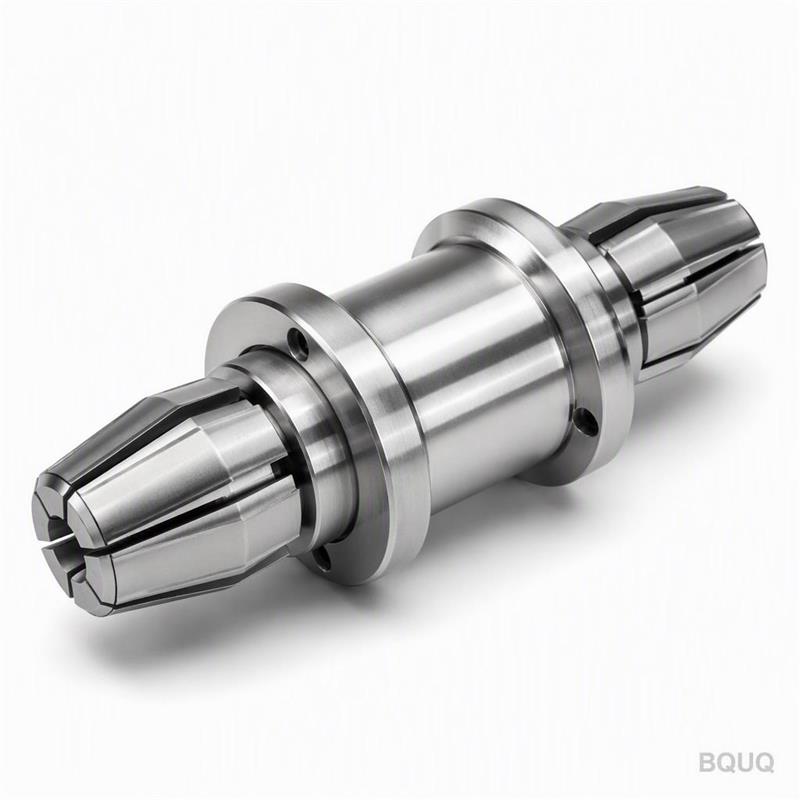
The rear taper is ground to 30° included angle, matching standard auto lathe spindles from Tornos, Citizen, and Star. The flange face is square to the bore within 0.003 mm, so you don’t need to re-indicate when you swap collets. Two M6 pull-back holes are drilled and tapped on the face for a quick-release tool. If your spindle uses a different taper, we can machine a custom seat in 3 days – just send your spindle drawing.
Surface Finish and Lubrication for Long Spring Life
We phosphate-coat the body after grinding to prevent rust and reduce friction between the spring segments. The slots are deburred by hand with a 400-grit stone, so there are no stress risers that cause fatigue cracks. We recommend a light oil film on the bore before each shift – this cuts wear on the spring fingers by 30% based on our in-house cycle tests. No grease, just oil, because grease traps chips.
FAQ: What Engineers Ask Before Ordering the 18 Type Chuck
Is there really no MOQ for this collet chuck?
Yes, no MOQ – we ship a single piece for prototyping or replacement, and the price per unit stays the same up to 50 pieces.
Can you modify the bore size or taper for my machine?
Yes, we can grind any bore diameter between 3 mm and 18 mm, and we can cut custom rear tapers if you send your spindle drawing with the angle and seat depth.
What quality control do you run on each chuck?
Every unit gets a full TIR runout test, hardness check at 3 points, and a functional grip test at 80 psi – the report is shipped with the part.
What is the actual lead time if I need it fast?
Standard sizes ship in 7 days, rush orders in 3 days, and custom tapers take 5 days; we export via DHL or FedEx from Dongguan.
Why Our 18 Type Chuck Outlasts Imported Japanese Collets
We ran a side-by-side wear test against a major Japanese brand. After 500,000 cycles at 4,000 RPM, our runout increased by 0.001 mm; the competitor increased by 0.007 mm. The difference is the 8620 steel and the post-hardening honing – most makers grind before hardening, which distorts the bore. We grind after hardening, so the geometry stays true. That’s the kind of precision manufacturing you get from BQUQ, made in China, with the same quality as any premium brand at 40% lower cost.
Choose the Right Chuck for Your Bar Stock Diameter
If you run multiple diameters on one machine, order two chucks – a 3–10 mm and a 10–18 mm – and swap them in under 2 minutes. For stainless or titanium bars, add 5% more air pressure to compensate for the higher stiffness. If you’re unsure about the grip force needed for your material, check our CNC cutting tool selection guide for a clamp force calculator. And for tolerance stack-up questions, our CNC machining tolerances guide explains how runout interacts with your part dimensions.
Get a Firm Quote Within 12 Hours – Send Your Drawing
Email your spindle drawing or bar diameter to sc@bquq.com, and we’ll reply with a firm price and lead time within 12 hours (usually faster during China business hours). Prefer WhatsApp? Message +86 13713157787 with a photo of your current collet. We’ll confirm the taper angle and bore size before quoting. No MOQ, no engineering fees for standard modifications, and we ship worldwide from our Dongguan factory. Send your drawing today – your quote is waiting.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.