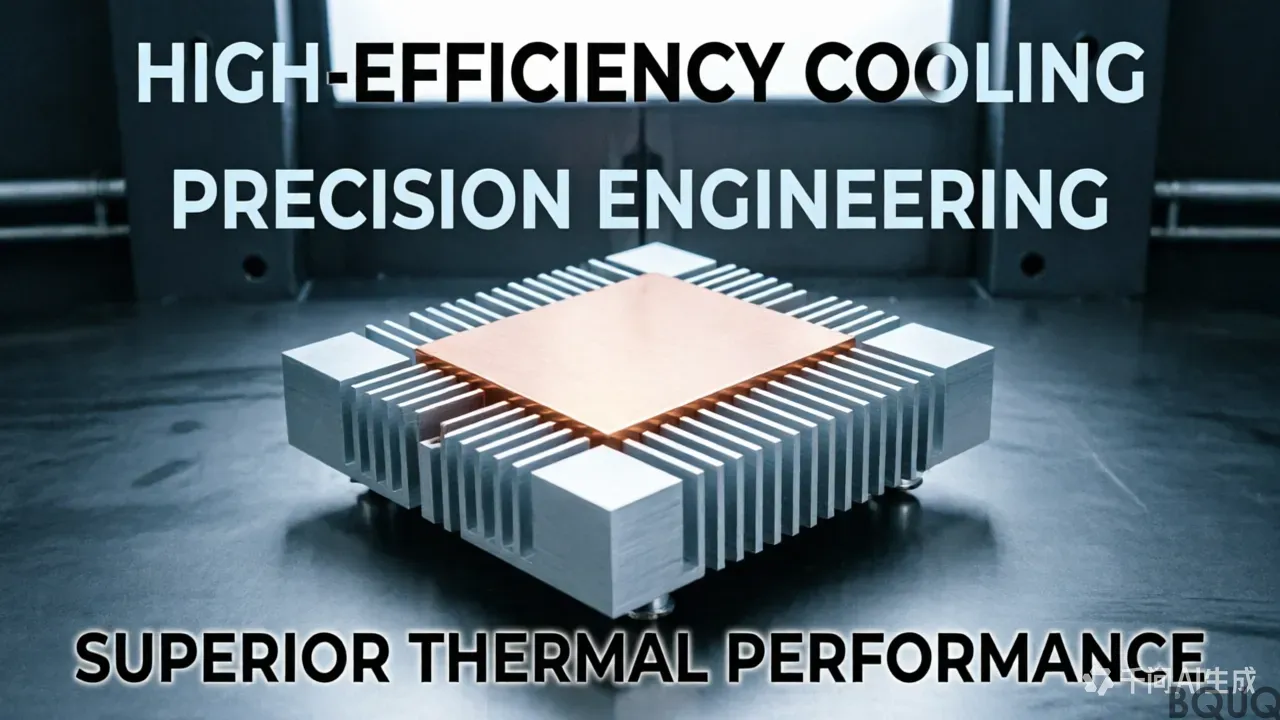
nvme heat sink: 6061-T6 aluminium, tolerance 0.10 mm, surface sandblast + epoxy powder coating RAL 9005, lead time 20 working days, MOQ 1000 pcs. Capacity 50,000 pcs for LED high bay lighting. Drawing review and first-article report included.
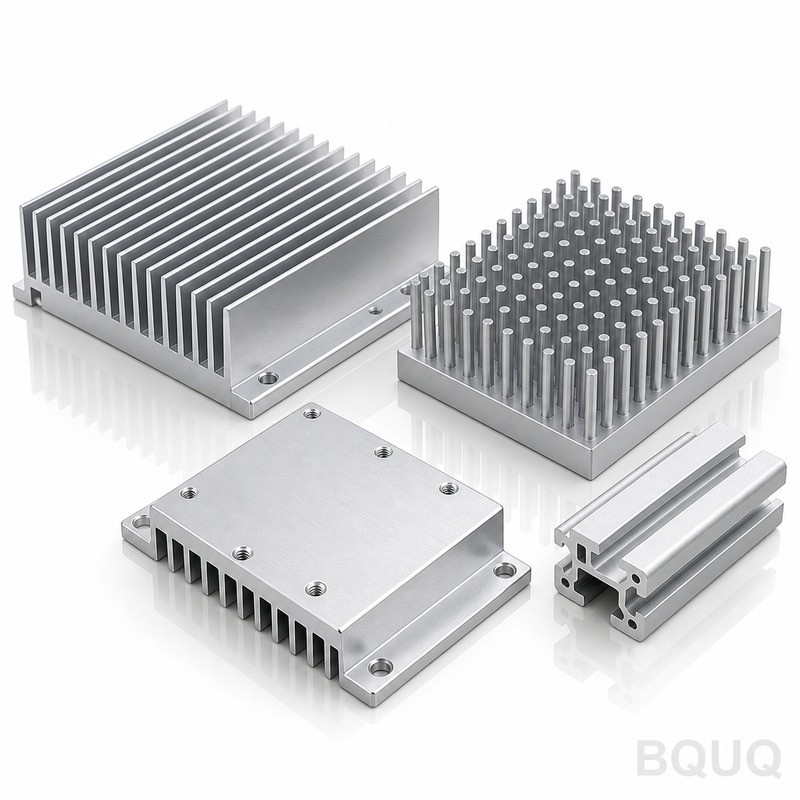
nvme heat sink
Key Takeaway
nvme heat sink manufacturing at BQUQ uses 6063-T5 aluminium with 0.5 mm fin thickness and 3.0 mm fin pitch, delivering 1.10 K/W thermal resistance. General tolerance is ±0.20 mm, set by tooling geometry rather than inspection filtering. Hard anodize Type III at 25-40 µm extends service life. Lead time is 20 working days, with capacity documented at 800,000 pcs for qualified LED high bay lighting programs.
Related reading: Vacuum Fixtures for Thin Parts: When They Win.
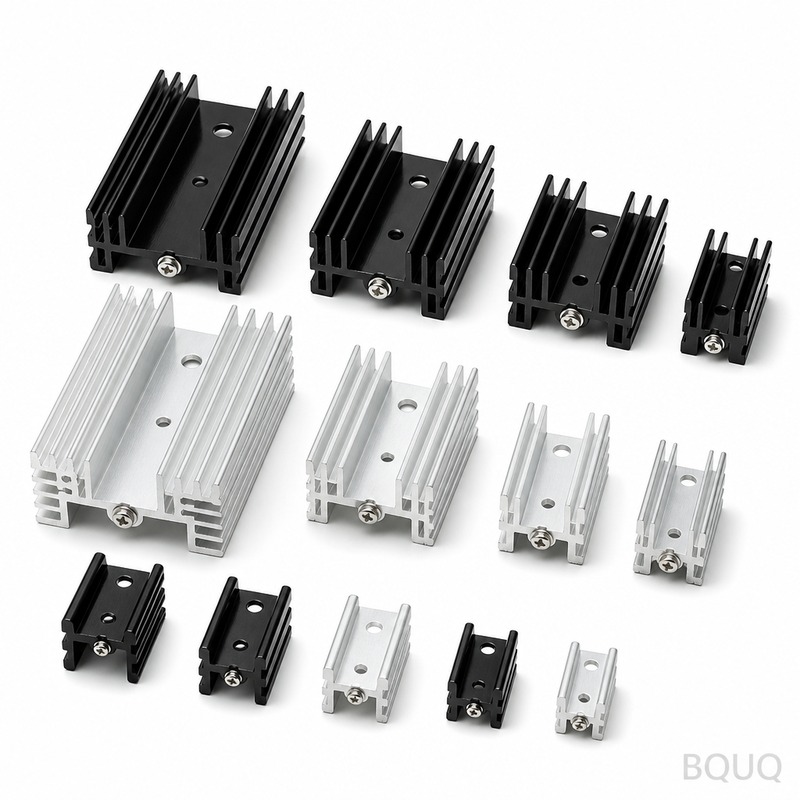
Key Takeaway
nvme heat sink manufacturing at BQUQ uses 6063-T5 aluminium with 0.5 mm fin thickness and 3.0 mm fin pitch, delivering 1.10 K/W thermal resistance. General tolerance is ±0.20 mm, set by tooling geometry rather than inspection filtering. Hard anodize Type III at 25-40 µm extends service life. Lead time is 20 working days, with capacity documented at 800,000 pcs for qualified LED high bay lighting programs.
See also: BQUQ CNC Machined Auto Lathe Synchronized Collet Chuck Precision Runout 0.005mm.
There is no shortage of suppliers who can quote nvme heat sink. The shortage is in suppliers who can explain why ±0.20 mm was chosen, what hard anodize Type III, 25-40 µm does to service life, and how 20 working days is protected when tooling needs repair.
Learn more about Why Do Stamped Parts Have Tooling Marks and Is That Normal?.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 6063-T5 aluminium |
| Fin thickness | 0.5 mm |
| Fin pitch | 3.0 mm |
| Thermal resistance | 1.10 K/W |
| Surface finish | hard anodize Type III, 25-40 µm |
| General tolerance | ±0.20 mm |
Market and Technical Context
Demand in LED high bay lighting has shifted from single-source standard parts toward qualified custom parts, which pushes documentation requirements upstream. Material certificates, first-article reports, and PPAP-style records are now requested at 5000 pcs rather than at mass production.
Further technical detail: heat sink compound thermal paste.
Consolidation among LED high bay lighting buyers means fewer, larger programs. That rewards suppliers who can document process capability at 800,000 pcs rather than those who win on a single sample.
Recommended reading: BQUQ Cnc Machined Auto Lathe Full Series 25 To 700 Collet Collection.
How We Manufacture It
Tooling is designed around the measured capability of the process, so ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. That is why 20 working days is realistic instead of optimistic.
In production, nvme heat sink runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.20 mm.
Compare it with BQUQ Stainless Steel Touch Springs Collection 02.
Deburring and edge conditioning are specified on the drawing for nvme heat sink. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Material and Surface Finish
Material condition matters as much as grade. 6063-T5 aluminium supplied in the wrong temper will drift after machining, which is why nvme heat sink is stress-relieved before finishing when the geometry is asymmetric.
Surface specification for nvme heat sink is hard anodize Type III, 25-40 µm, chosen for the service environment in LED high bay lighting. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Where nvme heat sink sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Related reading: How to Calculate Heat Sink Size for Your Electronic Enclosure.
Tolerance and Inspection
General dimensions on nvme heat sink are held to ±0.20 mm; critical features are identified on the drawing and controlled separately with a tighter band.
See also: BQUQ Bonded Fin Aluminum Heatsink.
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so nvme heat sink drawings state how each critical dimension is verified.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on nvme heat sink, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Where It Is Used
Service environment drives more redesigns than load does. nvme heat sink in outdoor or washdown service needs hard anodize Type III, 25-40 µm and sealing considered at design stage, not added later.
Learn more about Computer heat sink.
Retrofit requests are common: an existing assembly needs nvme heat sink in a slightly different size. Because the process window is already known, 20 working days on a retrofit is usually shorter than on a new part.
What to Confirm Before Ordering
Packaging is part of the specification. Parts arriving with edge damage or mixed lots cost more than the packaging difference, especially for nvme heat sink with finished surfaces.
Confirm the reorder path. If nvme heat sink is documented with tooling drawings and a first-article report on file, a repeat order years later reproduces the original part instead of approximating it.
FAQ: Your Questions Before Ordering
What tolerance can you hold on nvme heat sink?
General dimensions are held to ±0.20 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
What is the minimum order quantity for nvme heat sink?
Prototype quantities start well below production minimums. Production runs for nvme heat sink start at 5000 pcs, which is where the process window is proven and unit cost stabilises.
How long does production take for nvme heat sink?
Yes. Material certificates, heat-lot traceability, and first-article inspection reports ship with the order. If your LED high bay lighting customer requires additional documentation, specify it at quote stage.
Can you work from our existing drawing?
hard anodize Type III, 25-40 µm is standard for nvme heat sink. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
What surface finishes are available for nvme heat sink?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of nvme heat sink remains usable.
If nvme heat sink is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
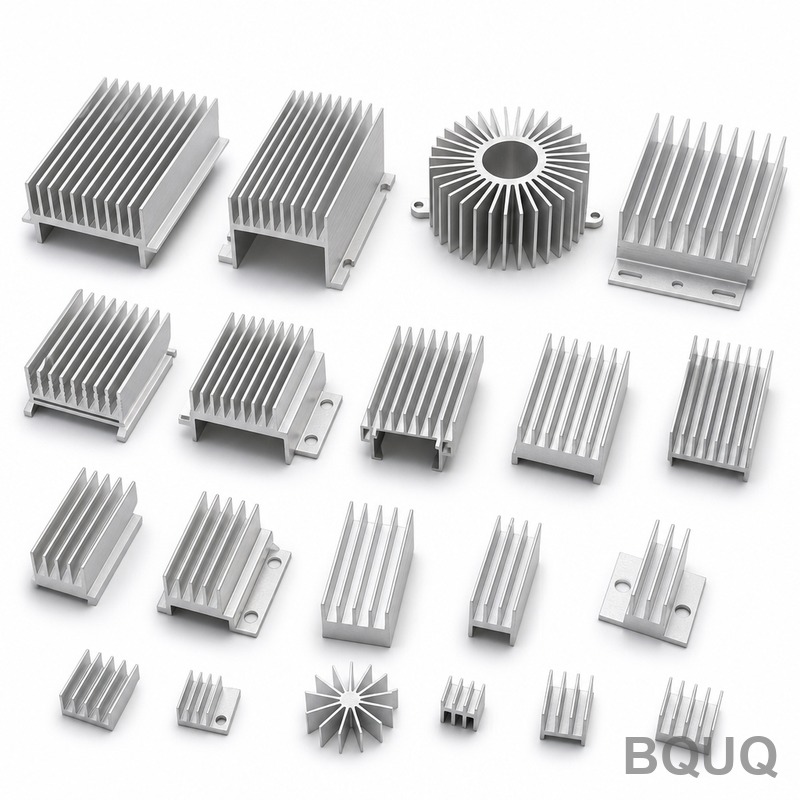
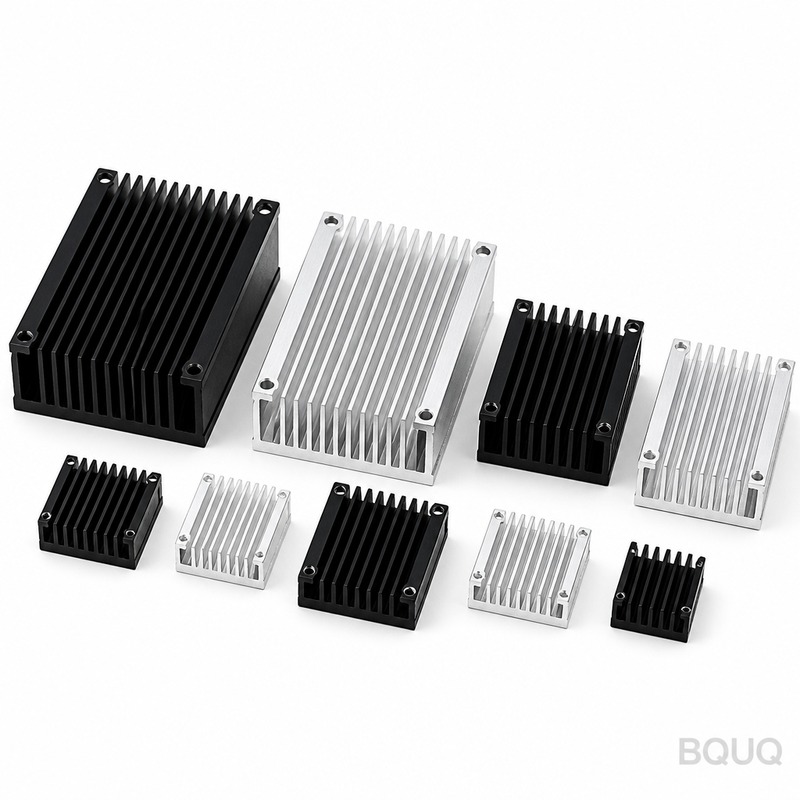
Further technical detail: Custom Copper Skived Fin Heatsinks.
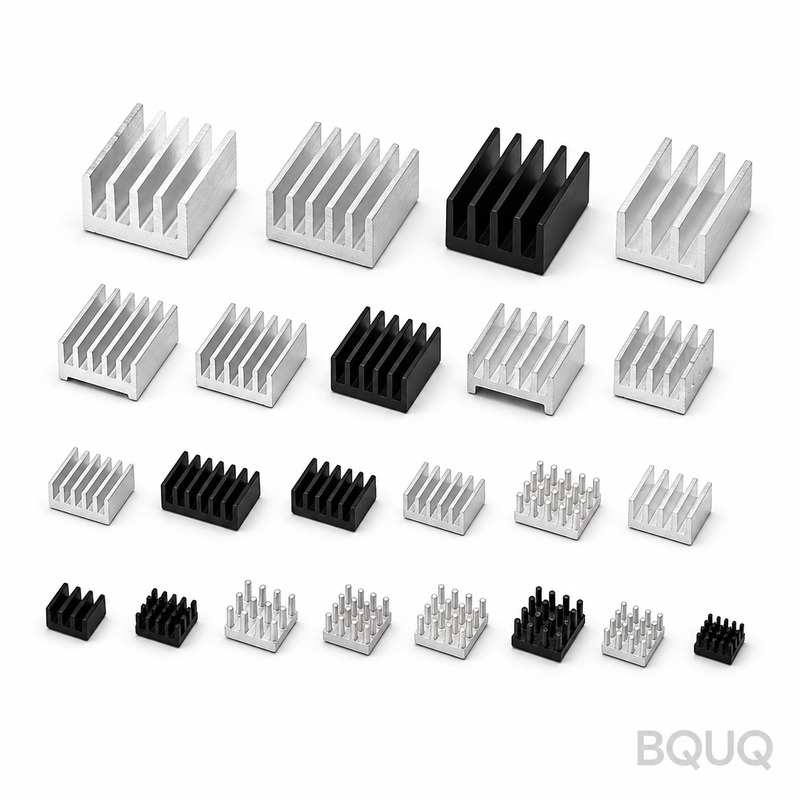
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6063-T5 aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 20 working days |
| MOQ | 5000 pcs for documented programs |
| Capacity | 800,000 pcs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard single-source part | Low-volume or non-critical LED high bay lighting | Limited documentation; not qualified for larger programs |
| Qualified custom part | Programs requiring material certificates, first-article reports, and PPAP-style records | Higher upfront documentation and tooling validation effort |
| 6063-T5 aluminium with hard anodize Type III, 25-40 µm | Applications needing 1.10 K/W thermal resistance and extended service life | Higher cost than bare or thinner coatings |
| ±0.20 mm tooling-based tolerance | Repeatable production at 800,000 pcs | Requires tooling repair planning to protect 20 working days lead time |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Tooling design | Geometry set around measured process capability for ±0.20 mm | Tooling design and capability study |
| Incoming material | 6063-T5 aluminium verification | Material certificates |
| First article | Dimensional and thermal performance check | First-article report |
| Production | Process capability at 800,000 pcs | PPAP-style records |
| Final inspection | General tolerance ±0.20 mm and surface finish hard anodize Type III, 25-40 µm | Inspection report |
Frequently Asked Questions
What is the thermal resistance of this nvme heat sink?
The thermal resistance is 1.10 K/W with 6063-T5 aluminium, 0.5 mm fin thickness, and 3.0 mm fin pitch. This combination supports LED high bay lighting programs requiring qualified custom parts and documented process capability at 800,000 pcs.
Why is the general tolerance ±0.20 mm?
±0.20 mm is a consequence of tooling geometry designed around measured process capability, not an inspection filter. This supports repeatable production and helps protect the 20 working day lead time when tooling needs repair.
What does hard anodize Type III, 25-40 µm do for service life?
Hard anodize Type III at 25-40 µm increases surface hardness and wear resistance, extending service life in demanding LED high bay lighting environments. It is applied to 6063-T5 aluminium parts with 0.5 mm fin thickness and 3.0 mm fin pitch.
What is the lead time and how is it protected?
Lead time is 20 working days. It is protected by designing tooling around measured process capability for ±0.20 mm, planning tooling repair, and documenting process capability at 800,000 pcs rather than relying on a single sample.
What documentation is available at 5000 pcs?
At 5000 pcs, material certificates, first-article reports, and PPAP-style records are available. These support qualified custom parts for LED high bay lighting buyers who require documentation upstream rather than at mass production.
What material and finish are used?
Material is 6063-T5 aluminium with 0.5 mm fin thickness and 3.0 mm fin pitch. Surface finish is hard anodize Type III, 25-40 µm. General tolerance is ±0.20 mm, and thermal resistance is 1.10 K/W.
Recommended reading: aluminum heat sink 300x140x20.
What should I confirm before ordering?
Confirm material certificates, first-article reports, and PPAP-style records at 5000 pcs. Verify ±0.20 mm tolerance, hard anodize Type III 25-40 µm, 1.10 K/W thermal resistance, 20 working day lead time, and capacity at 800,000 pcs.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6063-T5 aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 20 working days |
| MOQ | Not specified in excerpt |
| Capacity | 800,000 pcs for qualified LED high bay lighting programs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard nvme heat sink | Single-source standard parts | Less documentation, may not meet custom thermal or fit requirements |
| Custom nvme heat sink | Qualified custom parts in LED high bay lighting | Higher documentation requirements (material certificates, first-article reports, PPAP-style records) |
| 6063-T5 aluminium with hard anodize Type III | Applications needing 1.10 K/W thermal resistance and extended service life | Higher cost and longer lead time than bare aluminium |
| 0.5 mm fin thickness and 3.0 mm fin pitch | Balancing thermal performance and manufacturability | Tooling geometry sets ±0.20 mm tolerance, limiting tighter tolerances without new tooling |
Frequently Asked Questions
What material and finish are used for the nvme heat sink?
The nvme heat sink uses 6063-T5 aluminium with hard anodize Type III at 25-40 µm. This combination provides 1.10 K/W thermal resistance and extends service life. The material and finish are standard for BQUQ manufacturing and are documented with material certificates.
What is the general tolerance and how is it set?
General tolerance is ±0.20 mm. It is set by tooling geometry rather than inspection filtering. This means the tooling determines the achievable tolerance, and inspection verifies it. For tighter tolerances, new tooling may be required.
What is the lead time and capacity for the nvme heat sink?
Lead time is 20 working days. Capacity is documented at 800,000 pcs for qualified LED high bay lighting programs. This capacity reflects the production scale for qualified custom parts with full documentation.
What documentation is available for qualified orders?
For qualified orders, documentation includes material certificates, first-article reports, and PPAP-style records. These are requested at 5000 pcs rather than at mass production. This supports the shift from single-source standard parts to qualified custom parts.
How does hard anodize Type III affect service life?
Hard anodize Type III at 25-40 µm extends service life by providing a durable, corrosion-resistant surface. It is applied to the 6063-T5 aluminium nvme heat sink. This finish helps maintain thermal performance over time.
Compare it with aluminum heat sink for seeed studio xiao.
What is the thermal resistance of the nvme heat sink?
Thermal resistance is 1.10 K/W. This is achieved with 6063-T5 aluminium, 0.5 mm fin thickness, and 3.0 mm fin pitch. The design balances thermal performance with manufacturability and tooling geometry.
What should I confirm before ordering a custom nvme heat sink?
Confirm the required documentation level, such as material certificates, first-article reports, and PPAP-style records at 5000 pcs. Also confirm tolerance needs, since ±0.20 mm is set by tooling geometry. Lead time is 20 working days, and capacity is 800,000 pcs for qualified programs.