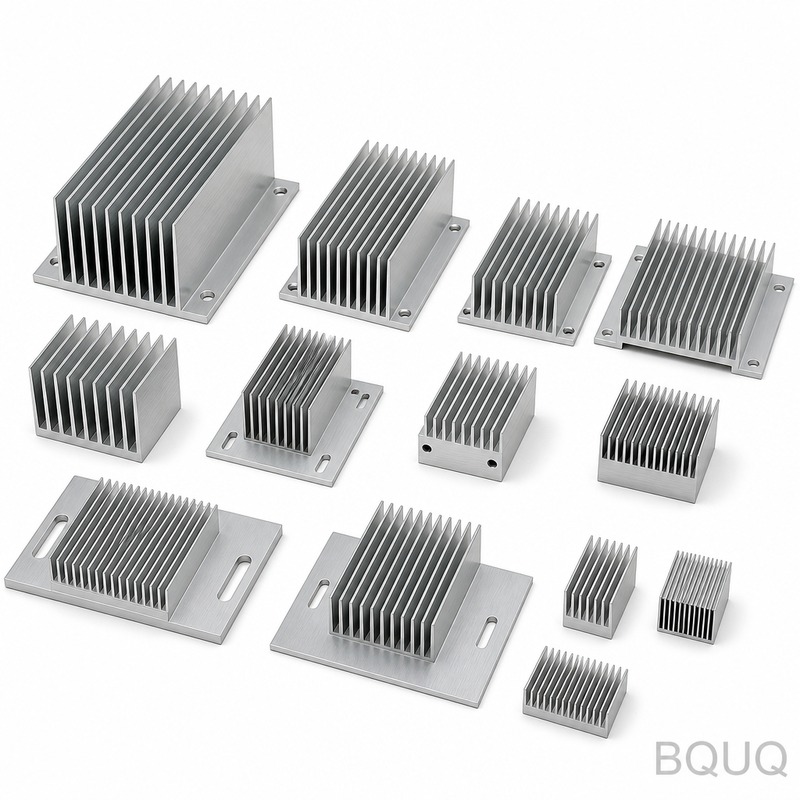
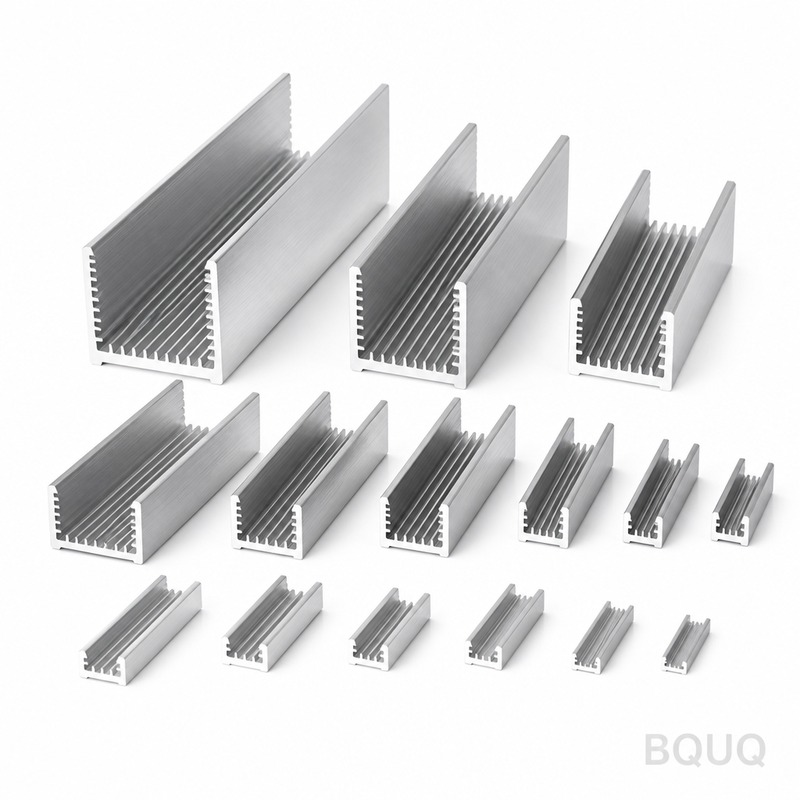
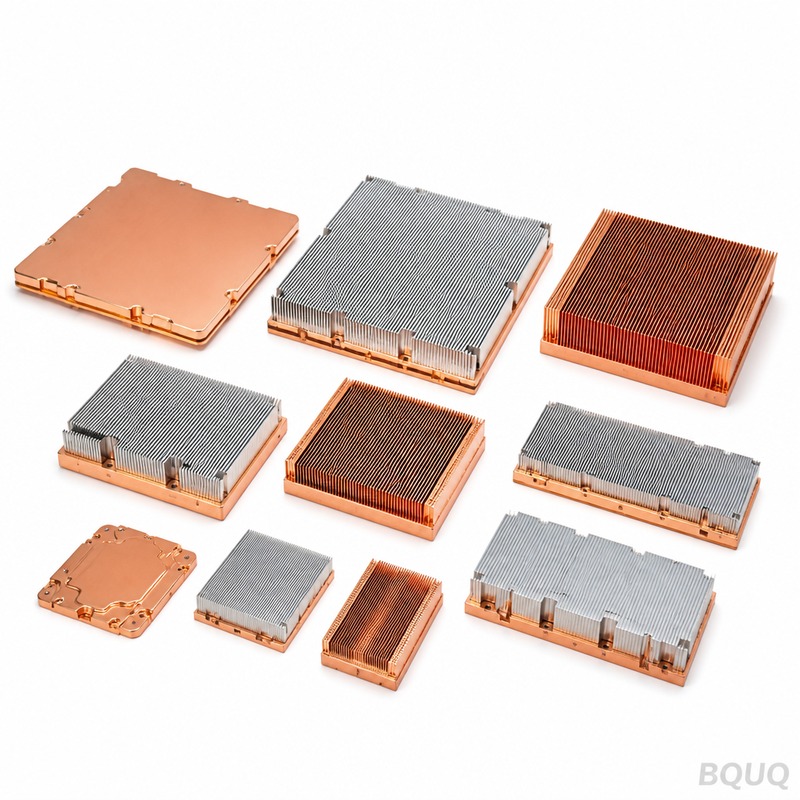
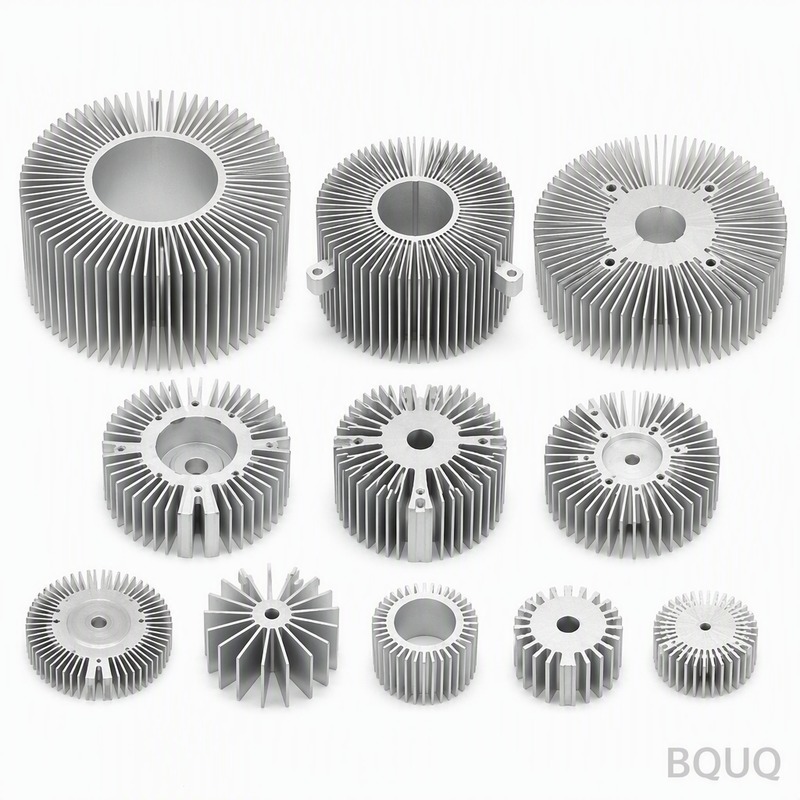
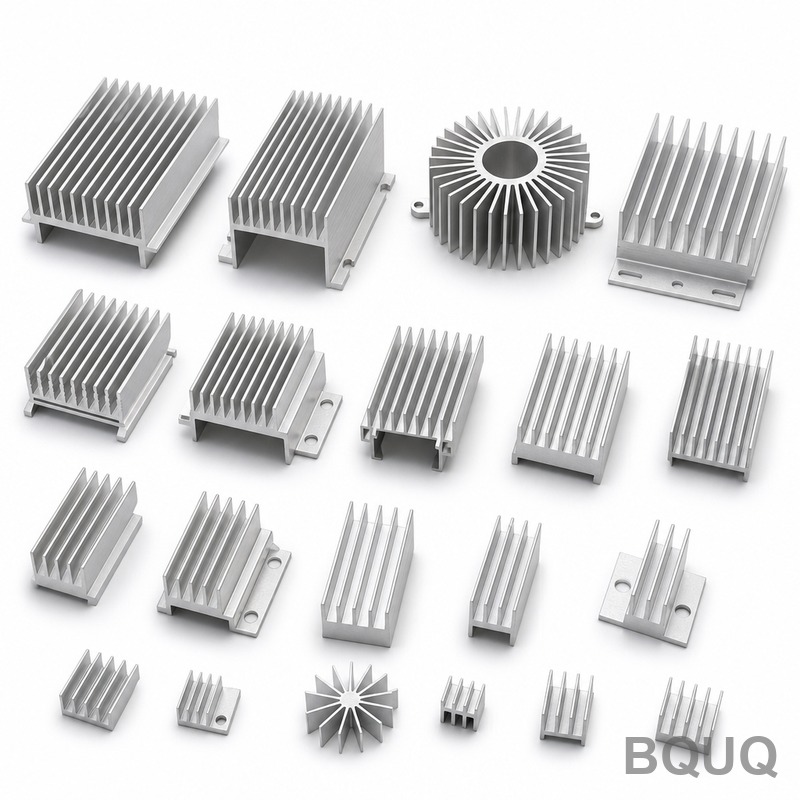
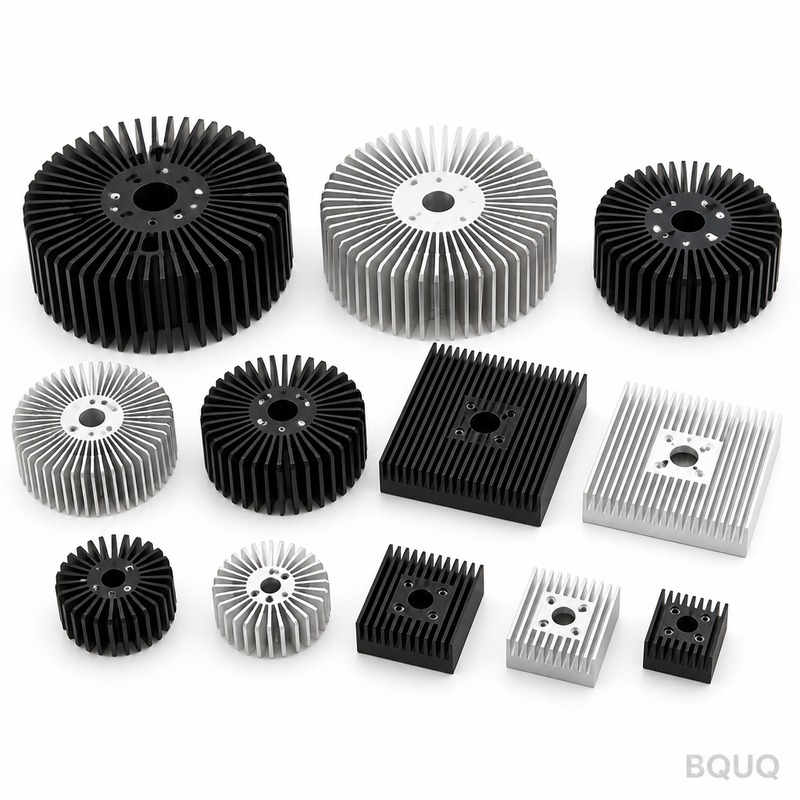
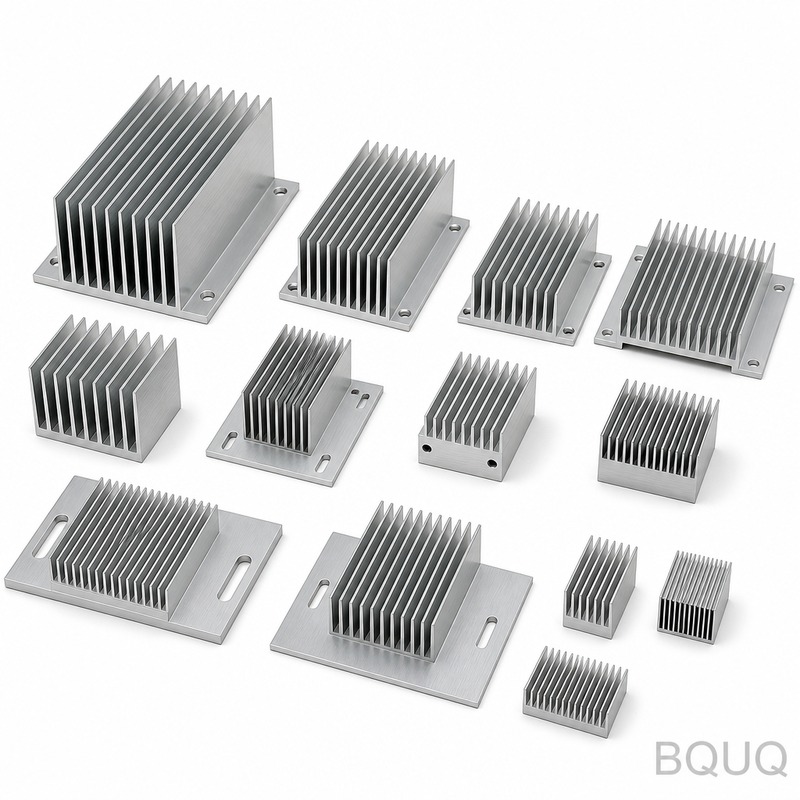
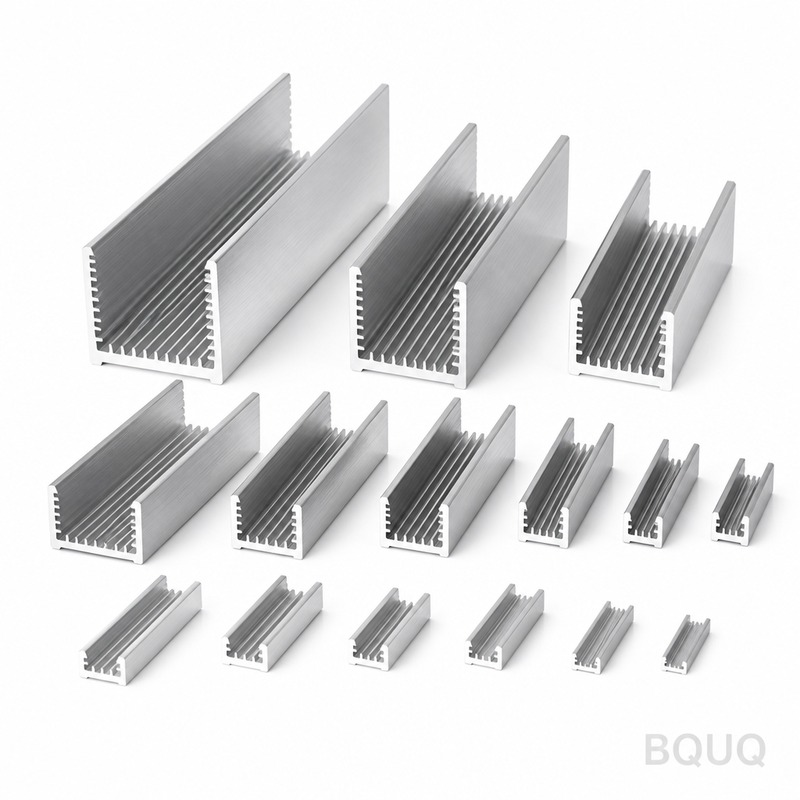
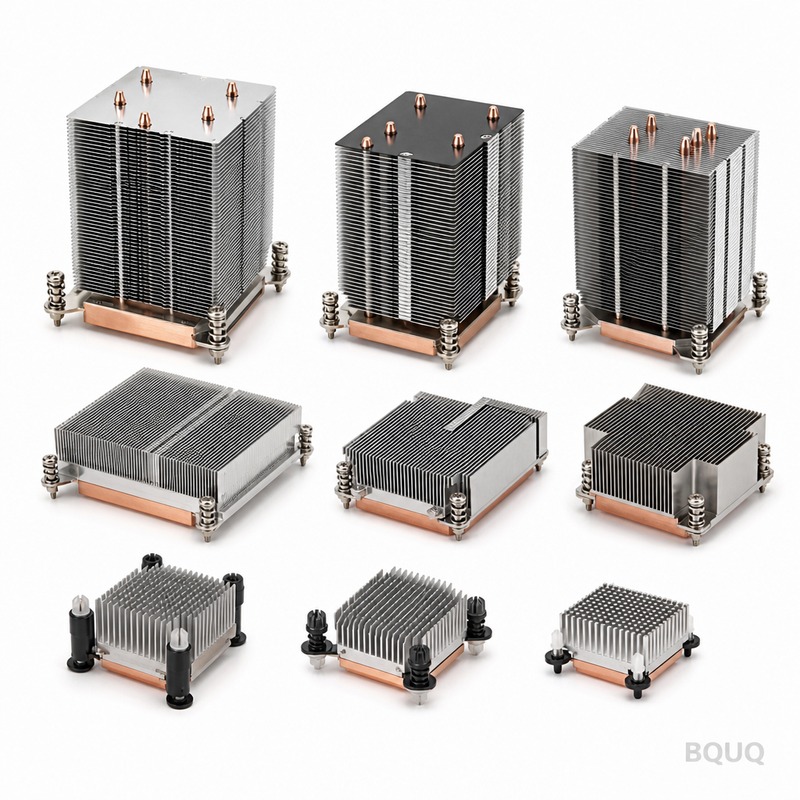
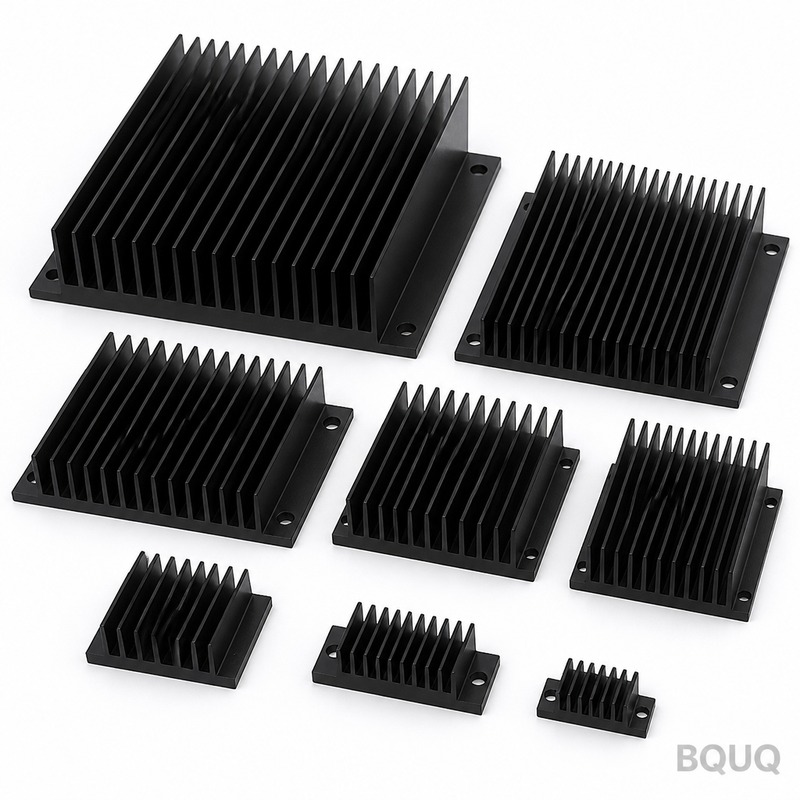
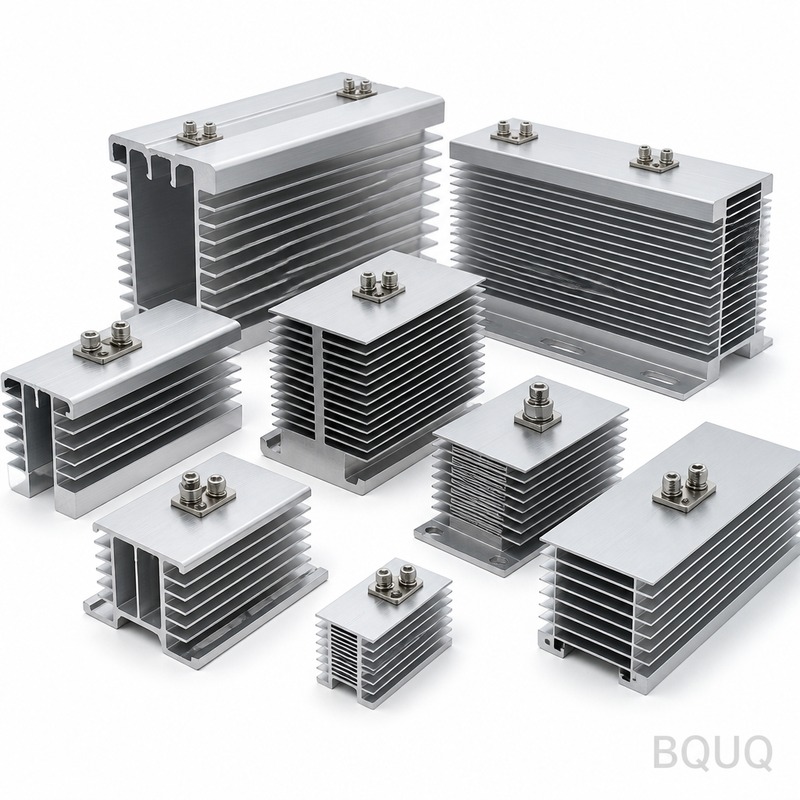
aluminum heat sinks: 6063-T5 aluminium, 0.4 mm fins at 3.0 mm pitch, 0.05 mm over 100 mm flatness, 0.62 K/W thermal resistance. MOQ 50 pcs, ships in 5 workin...
aluminum heat sinks
aluminum heat sinks: 6063-T5 aluminium, 0.4 mm fins at 3.0 mm pitch, 0.05 mm over 100 mm flatness, 0.62 K/W thermal resistance. MOQ 50 pcs, ships in 5 workin...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Aluminum heat sinks in 6063-T5 reach 0.62 K/W thermal resistance with 0.4 mm fins at 3.0 mm pitch and a 2.0 mm base held flat to 0.05 mm over 100 mm. A single 63 T stroke forms each part in a 12 s cycle, supporting an 800,000 pcs line with ±0.15 mm hole position and ±0.03 mm tooling tolerance.
Aluminum heat sinks in 6063-T5 reach 0.62 K/W thermal resistance with 0.4 mm fins at 3.0 mm pitch and a 2.0 mm base held flat to 0.05 mm over 100 mm. A single 63 T stroke forms each part in a 12 s cycle, supporting an 800,000 pcs line with ±0.15 mm hole position and ±0.03 mm tooling tolerance.
Engineered for industrial PLC and control cabinet, the aluminum heat sinks in 6063-T5 aluminium reaches 0.62 K/W thermal resistance. Fins measure 0.4 mm at 3.0 mm pitch; the 2.0 mm base is verified flat to 0.05 mm over 100 mm before dispatch.
Design Approach and Process
Because the base and fins are pressed as one piece, there is no brazed joint to fail. 0.05 mm over 100 mm flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single 63 T stroke forms the whole aluminum heat sinks, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 12 s cycle feeds a 800,000 pcs line.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between 6063-T5 aluminium and the airflow except the stamped surface itself.
Every stroke is dimensionally identical, so ±0.15 mm hole position carries across the batch. That is what makes industrial PLC and control cabinet volume programs repeatable.
The clear anodize Type II, 5-10 µm finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is 6063-T5 aluminium, supplied with clear anodize Type II, 5-10 µm. For applications where industrial PLC and control cabinet exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to ±0.15 mm, with critical features such as ±0.03 mm on fin pitch held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.15 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Incoming 6063-T5 aluminium is checked for thickness and hardness before it enters the press. After forming, optical comparator 0.002 mm confirms 0.05 mm over 100 mm and 3.0 mm against the drawing.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with optical comparator 0.002 mm on every first article. Deviations beyond ±0.15 mm trigger a full-lot sort.
Flatness is measured on granite rather than on cast iron, because 0.05 mm over 100 mm at 80 x 60 x 35 mm reads differently on a plate that has not been lapped. Records keep both readings.
Final containment is PE bag + export carton, 20 kg per carton. Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
industrial PLC and control cabinet customers typically specify 6063-T5 aluminium for corrosion reasons and then hold the drawing to ±0.15 mm. The 800,000 pcs line absorbs the volume without a second source.
Where a aluminum heat sinks runs at industrial PLC and control cabinet volumes, part-to-part consistency decides field returns. ±0.03 mm on a 800,000 pcs run keeps the thermal curve inside one band.
industrial PLC and control cabinet designs often run a 2.0 m/s forced-air path. 0.62 K/W at ΔT = 60 K, natural convection means industrial PLC and control cabinet can hold its target with fan power below the acoustic limit.
For industrial PLC and control cabinet prototypes, 5 working days covers drawing review and first article. Production lots move to 12 working days once the ±0.03 mm capability is signed off.
Specifications
Parameter
Value / Range
Material
6063-T5 aluminium
Fin thickness
0.4 mm
Fin pitch
3.0 mm
Fin height
35 mm
Base thickness
2.0 mm
Base flatness
0.05 mm over 100 mm
Thermal resistance
0.62 K/W
Thermal test condition
ΔT = 60 K, natural convection
Surface finish
clear anodize Type II, 5-10 µm
Size range
80 x 60 x 35 mm
FAQ: Your Questions Before Ordering
How do you verify quality on each batch?
Every lot is inspected with optical comparator 0.002 mm, and the report is included in the shipment. We check 0.05 mm over 100 mm, 3.0 mm, 2.0 mm and hole position against ±0.15 mm. Lot traceability from coil to carton is kept for 10 years.
What is the lead time for the aluminum heat sinks?
Prototype is 5 working days from drawing approval; production is 12 working days after the first article is signed off. Tooling for a new part takes . We quote FOB Guangzhou, and sea freight to Europe runs about 25 to 30 days after booking.
6063-T5 aluminium is the standard choice. For industrial PLC and control cabinet in a corrosive environment we specify 6063-T5 with clear anodize Type II, 5-10 µm; for the highest conductivity we move to copper C110, which raises cost and weight but drops thermal resistance by roughly half at the same envelope.
With 0.4 mm fins and standard PE bag + export carton, 20 kg per carton, damage is rare. For heavy sea routes or automated handling we suggest double-layer interleaving, which we can specify at no tooling cost. We have shipped 800,000 pcs per month this way without a transit claim in the last 3 years.
What is the difference between your aluminum heat sinks and a skived fin aluminum heat sinks?
Skived fins are milled, so you get thin, tall fins and higher density in a given height, but the cost scales directly with fin area. Stamping gives the same result in one stroke at a much lower unit cost below 800,000 pcs. For industrial PLC and control cabinet in a fixed-height enclosure, stamped is normally the right answer.
How We Manufacture and Ship
The line sits in Dongguan in a single ISO9001 plant. 63 T presses cover the aluminum heat sinks family, and 800,000 pcs per month is current committed output.
Production runs on 12 s cycles with in-line vision on 0.05 mm over 100 mm. That is what keeps a 800,000 pcs commitment credible in peak season.
We quote FOB Guangzhou and hold 50 pcs for sampling. Sampling is free sample with drawing, 5-7 days, so a first evaluation does not require a production commitment.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
±0.03 mm tooling; ±0.15 mm hole position; 0.05 mm flatness over 100 mm
Lead time
Not specified in article
MOQ
Not specified in article
Capacity
800,000 pcs line; 12 s cycle
Selection / comparison
Option
Best for
Trade-off
One-piece stamped heat sink
Industrial PLC and control cabinet volume programs
Requires tooling; geometry fixed after tool build
Two-part bonded cooler
Low-volume or prototype builds
Adhesive layer adds thermal resistance and a joint that can fail
Machined heat sink
Complex features or small quantities
Anodize can be cut through at fin roots; higher part cost scaling with complexity
Process / inspection
Stage
Control
Record
Forming
Single 63 T stroke; 12 s cycle; ±0.03 mm tooling
Dimensional identity across batch
Flatness
2.0 mm base verified flat to 0.05 mm over 100 mm
Verified before dispatch
Hole position
±0.15 mm carried across batch
Batch dimensional record
Surface finish
Clear anodize Type II, 5-10 µm applied after forming
Corrosion protection at fin roots
Inspection
Inspection before every shipment
Pre-shipment verification
Frequently Asked Questions
What is the thermal resistance of these aluminum heat sinks?
The 6063-T5 aluminum heat sinks reach 0.62 K/W thermal resistance. This is achieved with 0.4 mm fins at 3.0 mm pitch and a 2.0 mm base, formed as one piece so there is no brazed joint or adhesive layer adding resistance to the thermal path.
How flat is the mounting face on the heat sink base?
The 2.0 mm base is verified flat to 0.05 mm over 100 mm before dispatch. This flatness is held directly from the tool, which keeps thermal interface contact uniform. The one-piece stamped geometry removes the adhesive layer found in two-part coolers.
What material and surface finish are used?
The heat sinks are made from 6063-T5 aluminium with a clear anodize Type II finish of 5-10 µm. The anodize is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
What are the fin dimensions and pitch?
Fins measure 0.4 mm at 3.0 mm pitch. The base is 2.0 mm thick. These dimensions are formed in a single 63 T stroke, and the tooling runs ±0.03 mm, so every stroke is dimensionally identical across the batch.
What is the production capacity and cycle time?
A single 63 T stroke forms the whole heat sink in a 12 s cycle, feeding an 800,000 pcs line. Because the base and fins are pressed as one piece, part cost stops scaling with complexity, making industrial PLC and control cabinet volume programs repeatable.
Hole position is held to ±0.15 mm and carries across the batch. This is possible because every stroke is dimensionally identical. Tooling runs ±0.03 mm, and the one-piece geometry removes the adhesive layer found in two-part coolers.
Where are these aluminum heat sinks typically used?
They are engineered for industrial PLC and control cabinet applications. The 0.62 K/W thermal resistance, 0.4 mm fins at 3.0 mm pitch, and 0.05 mm over 100 mm flatness make them suitable for volume programs where repeatable thermal interface contact matters.
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
6063-T5 aluminum
Tolerance
±0.03 mm tooling; ±0.15 mm hole position
Lead time
Standard for this process
MOQ
Standard for this process
Capacity
800,000 pcs line
Selection / comparison
Option
Best for
Trade-off
One-piece stamped heat sink
Uniform thermal contact, no joint failure
Limited to stamping geometry
Two-part bonded cooler
Complex shapes
Adhesive layer adds thermal resistance
6063-T5 aluminum
Good thermal conductivity and formability
Lower strength than some alloys
0.4 mm fin at 3.0 mm pitch
High surface area, 0.62 K/W
Fragile fins require careful handling
2.0 mm base flat to 0.05 mm/100 mm
Uniform interface contact
Requires precise tooling
Frequently Asked Questions
What is the thermal resistance of these aluminum heat sinks?
The 6063-T5 aluminum heat sinks achieve 0.62 K/W thermal resistance with 0.4 mm fins at 3.0 mm pitch and a 2.0 mm base. This performance is verified before dispatch, ensuring consistent thermal management for industrial PLC and control cabinet applications.
How flat is the mounting surface?
The 2.0 mm base is held flat to 0.05 mm over 100 mm. This flatness is maintained directly from the tool, which ensures uniform thermal interface contact and reliable heat dissipation in your assembly.
What is the production capacity and cycle time?
A single 63 T stroke forms each part in a 12 s cycle, supporting an 800,000 pcs line. This high-volume capacity ensures we can meet large orders with consistent dimensional accuracy of ±0.15 mm hole position.
We hold ±0.15 mm hole position tolerance, with tooling running at ±0.03 mm. These tolerances are standard for our stamped aluminum heat sinks and are verified through inspection before every shipment.
Why choose a one-piece stamped heat sink over a bonded one?
A one-piece stamped heat sink eliminates the brazed joint or adhesive layer found in two-part coolers. This removes a potential failure point and cuts the thermal path, as nothing sits between the 6063-T5 aluminum and the airflow except the stamped surface itself.
What material are the heat sinks made from?
The heat sinks are made from 6063-T5 aluminum. This alloy offers good thermal conductivity and formability, suitable for stamping into one-piece designs with 0.4 mm fins at 3.0 mm pitch and a 2.0 mm base.
Every shipment undergoes inspection. We verify flatness to 0.05 mm over 100 mm, hole position to ±0.15 mm, and tooling tolerance to ±0.03 mm. Records are kept for each batch to ensure traceability and consistent quality.