OpeningYour 15 type collet with pin slot, machined exactly to your drawing. We do not stock generic blanks and modify them. We start from raw bar stock and cut every feature—bore,
Custom CNC Collet Chuck 15 Type with Pin Slot | Made in China
OpeningYour 15 type collet with pin slot, machined exactly to your drawing. We do not stock generic blanks and modify them. We start from raw bar stock and cut every feature—bore, slot, thread, and pi
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
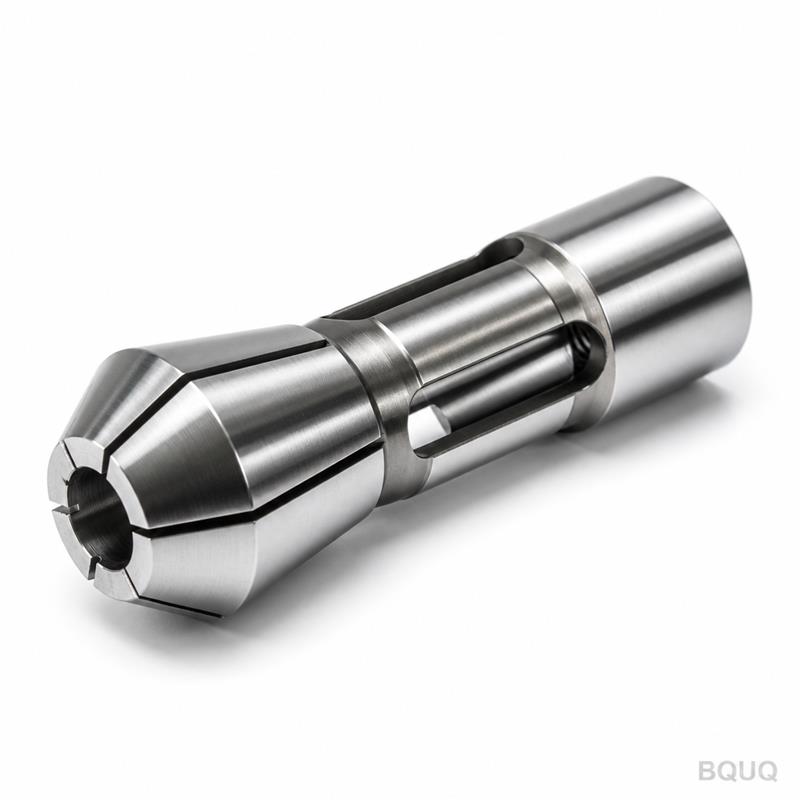
Your 15 type collet with pin slot, machined exactly to your drawing. We do not stock generic blanks and modify them. We start from raw bar stock and cut every feature—bore, slot, thread, and pin relief—to your specified tolerances. Before shipment, each collet is checked on a CMM and a test run in a spindle. If it does not grip true, it does not ship.
At a glance: Tolerance ±0.005 mm on bore and slot width, surface finish Ra 0.4, lead time 7–10 working days, no MOQ. One piece or one thousand, same process.
Specifications
Parameter
Value
Material options
65Mn spring steel, 40CrMo, 20CrMnTi, or per your spec
Hardness
HRC 45–52 (through-hardened) or HRC 58–62 (case-hardened)
Machining process
CNC Swiss-type lathe, 5-axis milling for slot and pin relief
Bore tolerance
±0.005 mm
Slot width tolerance
±0.01 mm
Concentricity
≤0.008 mm TIR to shank
Surface finish
Ra 0.4 on bore, Ra 0.8 on outer diameter
Heat treatment
Vacuum hardening, no decarb layer
Batch size
1 to 10,000 pieces, no MOQ
Inspection
100% critical dimensions, CMM report per batch
Lead time
7–10 working days for standard materials
We use CNC Swiss-type lathes for the outer profile and bore, then a 5-axis machining center for the pin slot and any cross holes. This avoids secondary handwork. The slot edges are deburred and micro-blasted. If you need a specific coating—TiN, black oxide, or phosphate—we apply it after heat treatment so the coating does not close up the slot tolerance.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every heat lot gets a unique code. We record raw material cert, machine parameters, and operator ID for each batch. If a problem appears in your assembly line, we can trace back to the exact bar stock and tool path. No guesswork.
2. Inspection report per batch. You do not have to ask for it. Every shipment includes a dimensional report with actual measured values for bore, slot, and concentricity. For critical collets, we also send a video of the test grip in a live spindle. This is standard, not a paid extra.
3. One factory for CNC machining, stamping, springs, and heat sinks. Your collet might need a spring pusher, a stamped retainer plate, or a heat sink for the spindle housing. We make all of them under one roof. You get one purchase order, one quality system, and one shipping date. Fewer suppliers means fewer tolerance stack-up problems.
Where these parts are used
A 15 type collet with a pin slot is not a general-purpose tool. It is designed for a specific spindle nose or a custom fixture. Common applications we see:
Swiss-type lathe guide bushings – the pin slot locks the collet against rotation during high-speed bar feeding.
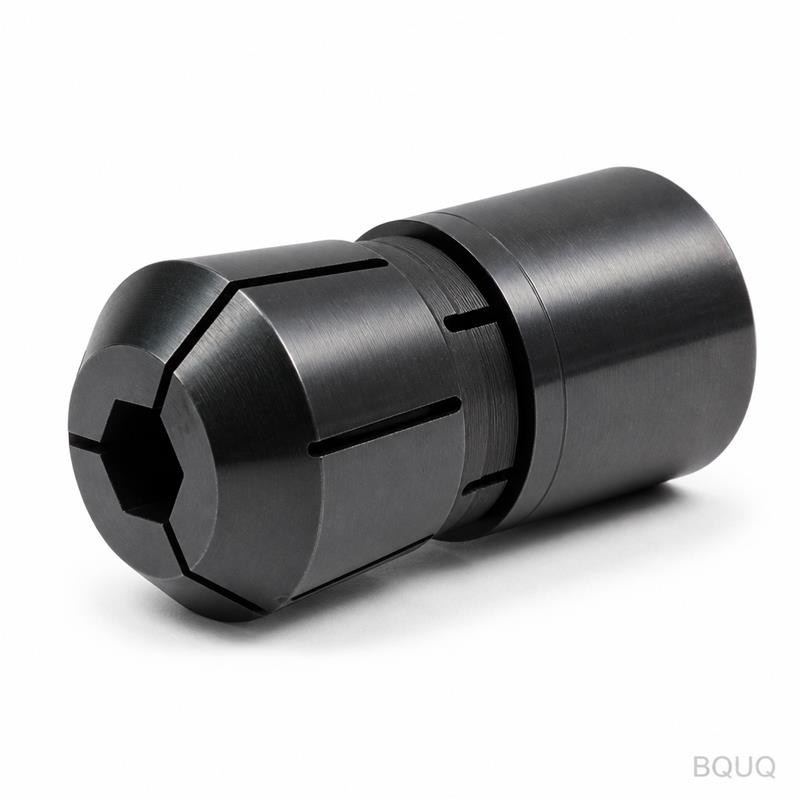
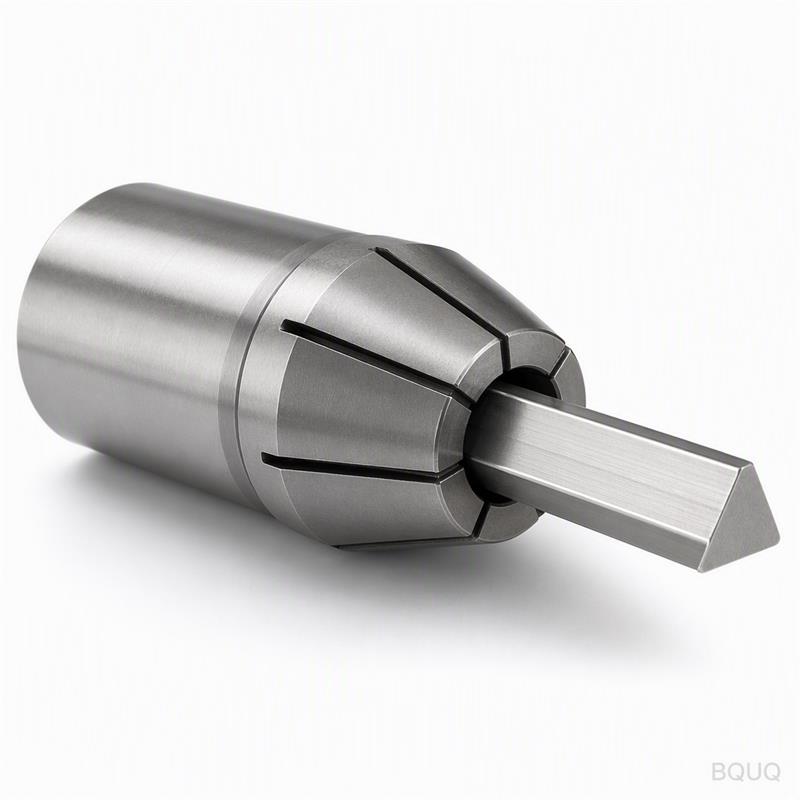
Automatic lathe workholding – for hex, square, or round bar stock where the pin indexes the collet to a fixed orientation.
Sub-spindle pick-off operations – the pin slot prevents the collet from spinning when gripping a part with a milled flat.
Custom fixture chucks – for medical device or aerospace parts that need a non-standard bore profile and a positive angular stop.
Replacement collets for aging machines – when the original manufacturer stopped production, we reverse-engineer from your worn sample and improve the material.
If your application is different, send the drawing. We have machined collets for watchmaking, dental tools, and automotive fuel injectors. The geometry changes, the process does not.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype testing at the same tolerance as a production run. The price per piece is higher for one, but the process is identical. You can order 5 pieces to validate, then scale up.
Q: How do you guarantee tolerance on the slot and bore?
A: We machine the bore and slot in the same setup where possible. After heat treatment, we grind the bore to final size. The slot is milled after grinding, so the pin slot position is referenced to the finished bore, not the raw stock. CMM report confirms it.
Q: What is your lead time for a custom collet?
A: Standard materials (65Mn, 40CrMo) and simple slot geometry: 7–10 working days. If you need case hardening or a special coating, add 3–5 days. For urgent orders, we can do 5 days on a single-piece basis. Tell us your deadline at the quote stage.
Q: Do you provide material certificates?
A: Yes, for every batch. We supply a mill test certificate from the steel mill and our own hardness test report. If you require third-party testing (SGS or equivalent), we arrange it at cost. No hidden fees.
Send your drawing
We quote from the drawing, not from a photo. Send your PDF or STEP file. Include the material grade, required hardness, and any coating. If you only have a worn sample, ship it to us and we will measure and quote.
Firm quote in 12 hours. We do not send a range. You get a fixed price per piece, tooling cost (if any), and a confirmed delivery date.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, with a paper trail you can audit. Your custom CNC collet chuck, built to your numbers, verified before it leaves our floor.