OpeningWe machine this 42 Type hex bore spring collet to your exact drawing. Not from stock. Not from a catalog. From your dimensions, your tolerances, your material callout.Every
Custom CNC Machined Auto Lathe 42 Type Hex Bore Spring Collet
OpeningWe machine this 42 Type hex bore spring collet to your exact drawing. Not from stock. Not from a catalog. From your dimensions, your tolerances, your material callout.Every collet is verified b
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
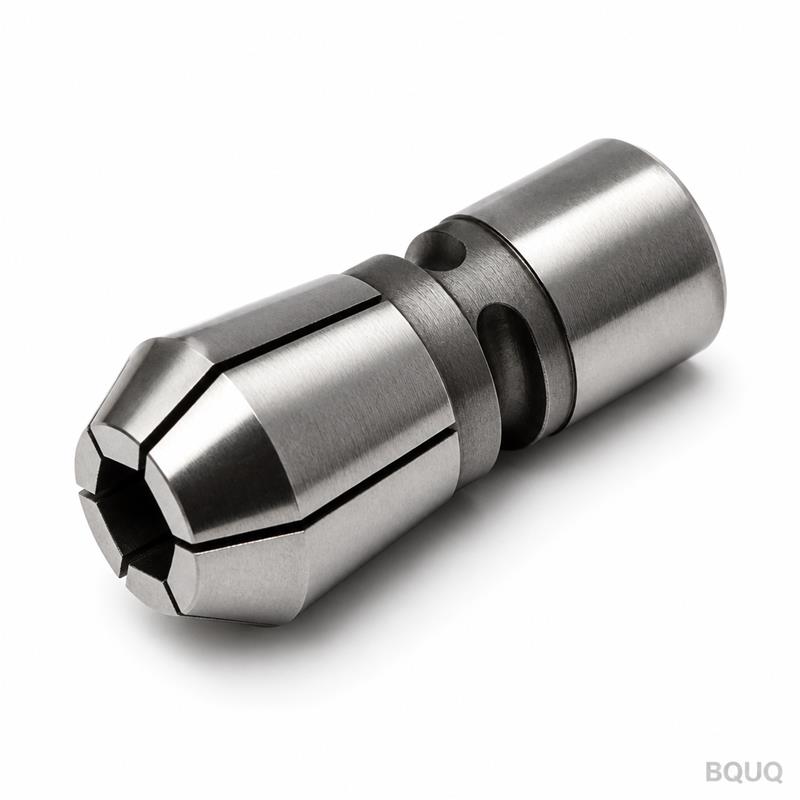
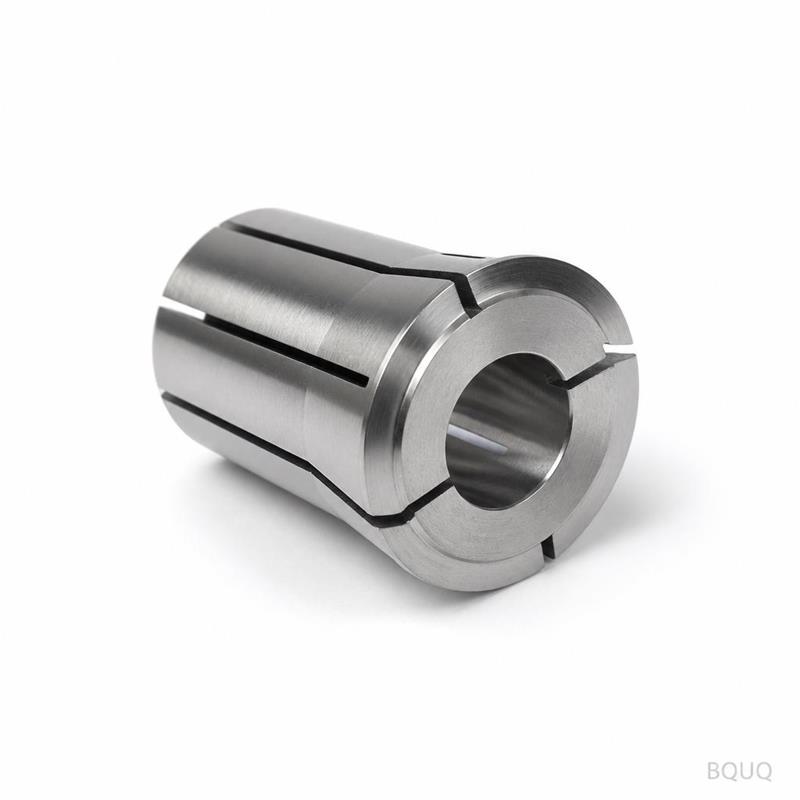
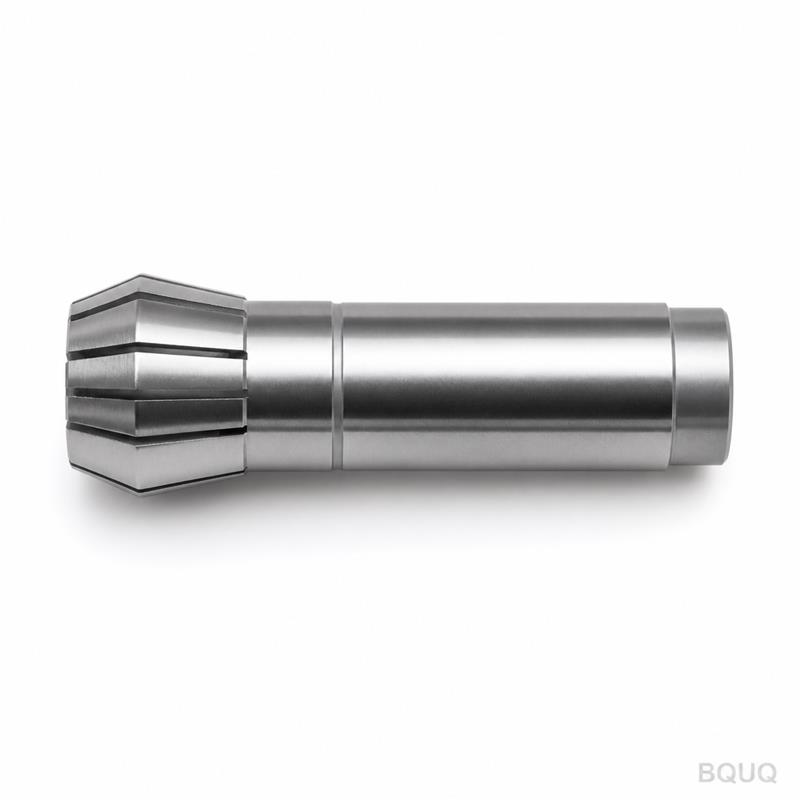
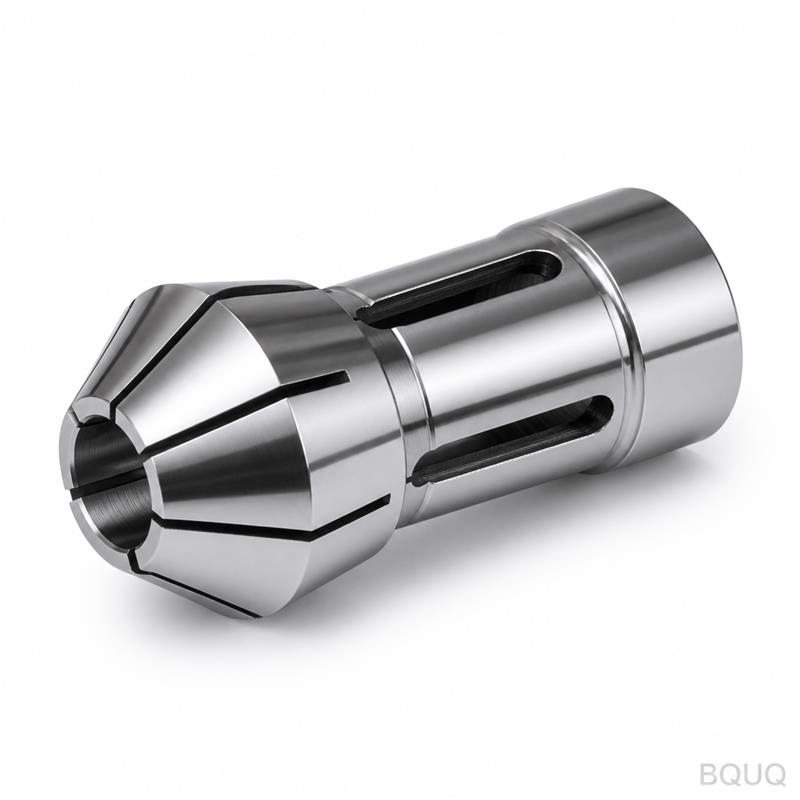
We machine this 42 Type hex bore spring collet to your exact drawing. Not from stock. Not from a catalog. From your dimensions, your tolerances, your material callout.
Every collet is verified before shipment. We check the hex bore size, the spring slot width, the concentricity, and the hardness. If it does not match your print, it does not ship.
This is a precision part. A collet that runs out by a few microns will ruin your workpiece tolerance, wear your spindle, and scrap your batch. We do not let that happen.
Tolerance: ±0.005 mm on bore and OD
Lead time: 7–12 days for prototypes, 15–20 days for production runs
No MOQ: order one piece or ten thousand
Material: 42CrMo, 65Mn, or your specified alloy
Surface: black oxide, phosphate, or as-machined
Inspection report included with every batch
Specifications
Parameter
Value
Type
Auto Lathe 42 Type Hex Bore Spring Collet
Bore shape
Hexagonal, per your drawing (e.g., 8 mm across flats)
Outer diameter
42 mm (standard 42 Type)
Length
60–80 mm, per drawing
Material options
42CrMo (quenched and tempered), 65Mn (spring steel), 9SiCr, or customer-specified
Hardness
HRC 45–52 for 42CrMo, HRC 48–55 for 65Mn
Tolerance
±0.005 mm on bore and OD, ±0.01 mm on slot width
Concentricity
≤0.005 mm TIR between bore and OD
Surface finish
Ra 0.4 µm on bore, Ra 0.8 µm on OD
Surface treatment
Black oxide, phosphate, or as-machined
Machining process
CNC turning, CNC milling, wire EDM for slots, heat treatment
Inspection
100% dimensional check, hardness test, concentricity test per batch
Batch size
1 to 100,000+ pieces
Lead time
7–12 days prototype, 15–20 days production
We use CNC lathes with live tooling for the OD and bore, then wire EDM for the spring slots. Heat treatment is done in-house in a controlled atmosphere furnace. Hardness is verified with a Rockwell tester on every batch, not just the first piece.
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Each batch gets a unique heat number and work order. We record material lot, machine operator, tooling used, and inspection results. If a problem shows up in your assembly line, we can trace it back to the exact heat and shift. This is not common for collet suppliers. We do it as standard.
2. Inspection report per batch.
You get a dimensional report with actual measured values, not just a pass/fail checkbox. We measure hex bore across flats, OD, length, slot width, and concentricity. Hardness values are included. The report is signed by our QC lead and sent with the shipment. Your incoming inspection can verify against our numbers in minutes.
3. One factory for CNC, stamping, springs, and heat sinks.
We are not a trading company. We run CNC machining, metal stamping, spring making, and heat sink fabrication under one roof in Dongguan. If your collet assembly needs a spring, a stamped retainer, or a heat sink for the spindle drive, we make those too. One purchase order, one quality system, one shipping point. Fewer suppliers, fewer delays, fewer arguments about who is responsible for a bad part.
Where these parts are used
The 42 Type hex bore spring collet is a workholding component for automatic lathes, especially Swiss-type and sliding headstock machines. The hex bore grips hexagonal bar stock or hex-headed workpieces for secondary operations.
Typical applications include:
Automotive fuel injector bodies – hex stock held for drilling and threading
Hydraulic fittings – hex bar stock machined into connectors and adapters
Fastener manufacturing – hex blanks held for slotting or head forming
Electrical terminals – hex brass or copper stock machined into contact pins
Medical device components – small hex shafts for surgical instruments, where concentricity is critical
Aerospace fasteners – hex stock in titanium or Inconel, where tool wear and runout are constant problems
In each case, the collet must hold the hex stock without marking it, without slipping under load, and without losing grip after thousands of cycles. That is why material, heat treatment, and slot geometry matter. We machine the slots to your width and depth so the spring action is consistent over the life of the collet.
Q: What is your MOQ?
A: No MOQ. We make one piece for prototype validation or a thousand for production. The unit price drops with quantity, but we do not force you to over-order.
Q: How do you control tolerance and quality?
A: We machine to ±0.005 mm on critical dimensions. Each batch is 100% dimensionally checked, and we test hardness and concentricity per batch. You receive a signed inspection report with actual values. If we miss a tolerance, we remake the parts at our cost.
Q: What is your lead time?
A: Prototypes ship in 7–12 days after drawing approval. Production runs of 500+ pieces ship in 15–20 days. Heat treatment and surface treatment are included in that time. For urgent orders, we can split the batch and ship the first part faster.
Q: Can you provide material certificates?
A: Yes. We supply mill certificates for the raw material with every batch, including chemical composition and mechanical properties. If you need third-party testing, we can arrange it at cost.
Send your drawing
Send us your drawing. We will review the material, tolerances, and quantity, and come back with a firm quote in 12 hours. No vague estimates, no hidden tooling charges.
Email your PDF or STEP file to sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, with no MOQ and batch-traceable quality. Your custom CNC collet chuck starts with a drawing. Send it today.