OpeningYour part. Your drawing. Our machines. That is how we work at BQUQ.We machine the CNC Auto Lathe 42 Type Round Bore Spring Collet Chuck to your exact geometry. Not a catalog
Custom CNC Collet Chuck Auto Lathe 42 Type Round Bore Precision
OpeningYour part. Your drawing. Our machines. That is how we work at BQUQ.We machine the CNC Auto Lathe 42 Type Round Bore Spring Collet Chuck to your exact geometry. Not a catalog copy. Not a modifie
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your part. Your drawing. Our machines. That is how we work at BQUQ.
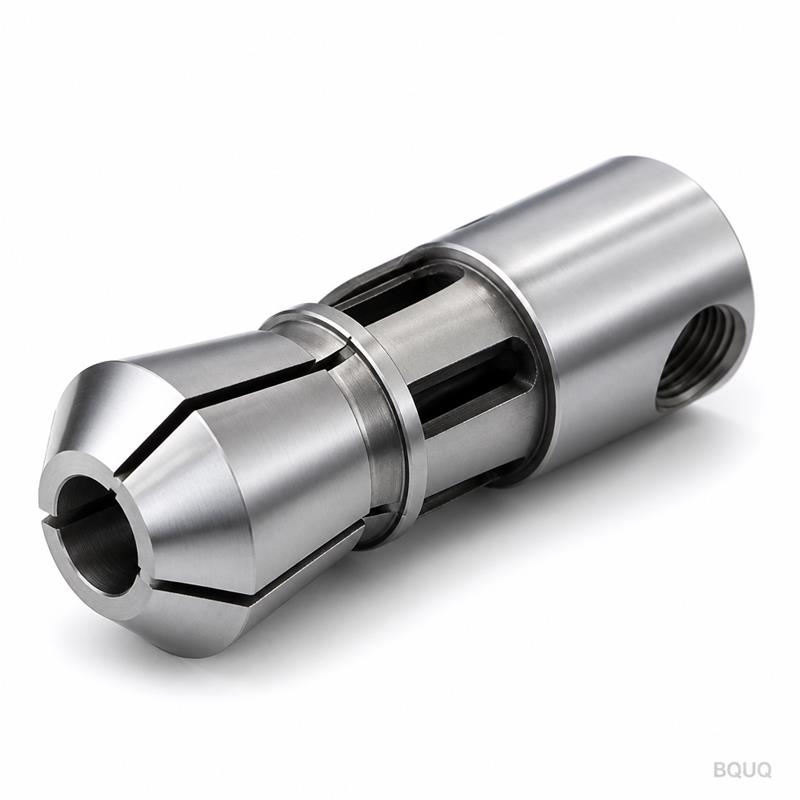
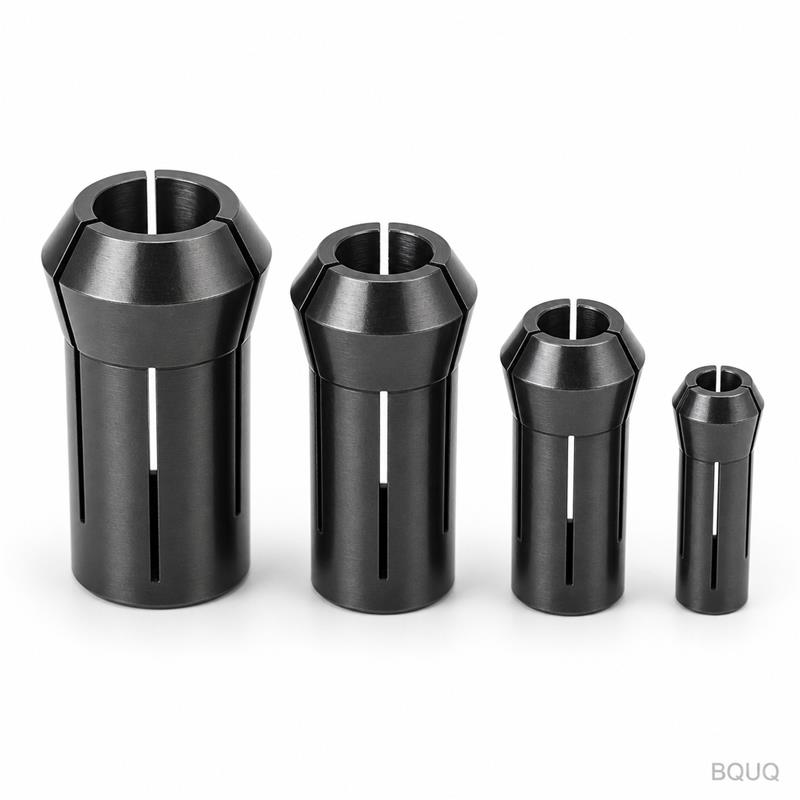
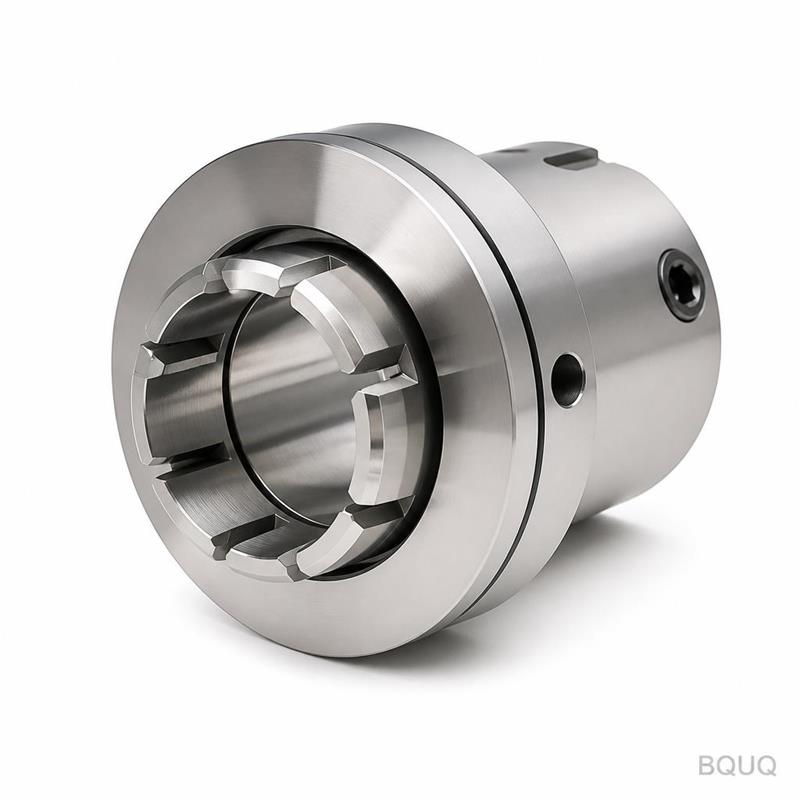
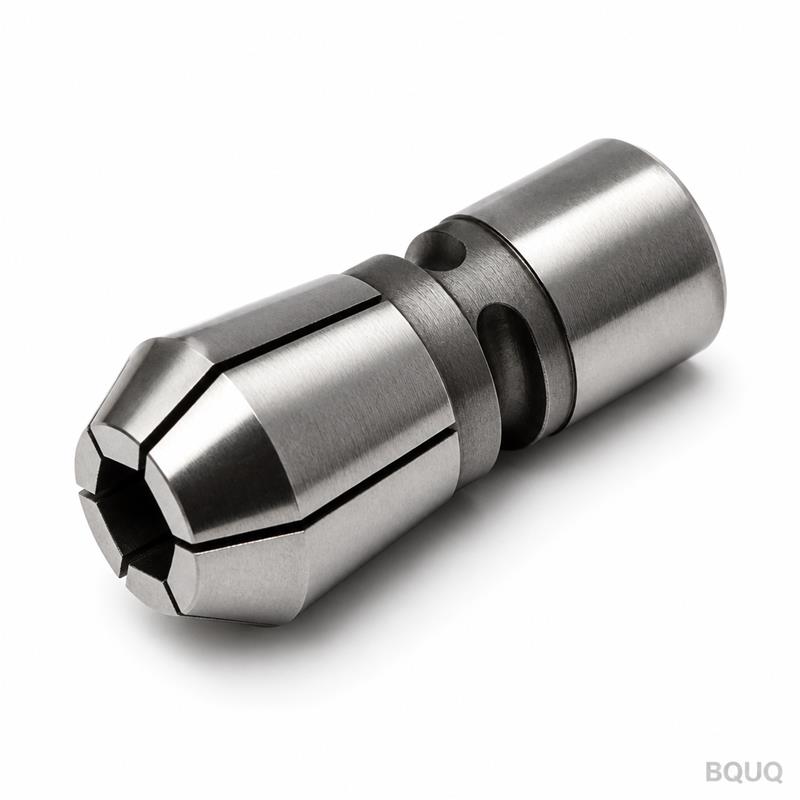
We machine the CNC Auto Lathe 42 Type Round Bore Spring Collet Chuck to your exact geometry. Not a catalog copy. Not a modified standard. Your drawing becomes the master. Every dimension is verified before shipment. We use CMM inspection and a hard gauge for the bore and taper.
At a glance: Tolerance ±0.005 mm on the bore, concentricity ≤0.01 mm TIR, lead time 15-20 working days, no MOQ. One piece or one thousand, the price per unit stays fair. We are a precision manufacturing factory in Dongguan, China, with 20 years of experience on CNC lathes and grinding machines.
Specifications
We do not outsource critical steps. The collet chuck body, the slots, and the spring tempering are all done in-house. This gives us control over the final fit and the clamping force repeatability.
Parameter
Value
Material options
65Mn spring steel, 60Si2MnA, 42CrMo (hardened), or per your spec
Hardness (spring collet)
HRC 42-48 after heat treatment
Hardness (body)
HRC 38-42
Bore diameter range
Ø3 mm to Ø42 mm (round bore type)
Concentricity (bore to taper)
≤0.01 mm TIR
Tolerance on bore diameter
+0.005 / -0.005 mm
Surface finish (bore)
Ra 0.4 µm (ground)
Surface finish (slots)
Ra 1.6 µm (wire-cut, no burr)
Slots
3-slot or 6-slot design, laser-cut or wire-cut
Taper angle
16° or 20° per your machine spindle
Keyway / drive slots
Per DIN 6343 or your drawing
Batch size
1 piece to 10,000 pieces, no MOQ
Inspection
100% dimensional check on critical features, CMM report included
Lead time
15 working days for prototypes, 20 days for production batches
We use CNC turning centers for the body, internal grinding for the bore, and wire EDM for the slots. The spring fingers are heat-treated in a vacuum furnace to prevent scale and decarburization. This is how we keep the clamping force consistent across a batch.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every collet chuck gets a unique serial number. We record the heat treatment lot, the grinding wheel used, and the inspector's name. If you have a problem on your line, we can trace it back to the exact batch and the exact machine. You get a full inspection report per batch, not a generic certificate.
2. Inspection report per batch. We do not just say "it's good." We send you the data. For every batch, you receive a dimensional report with actual measured values for the bore, the taper, and the concentricity. We also include a hardness test report. You can verify the part before you even put it on your spindle.
3. One factory for CNC + stamping + spring + heatsink. Your collet chuck is not an island. It works with springs, washers, and sometimes a stamped retainer plate. We make all of those in the same building. You send us one drawing package, we coordinate the whole assembly. Fewer suppliers, fewer logistics headaches, one responsible party.
Where these parts are used
The Auto Lathe 42 Type Round Bore Spring Collet Chuck is a workhorse in high-volume turning shops. You will find it in:
Swiss-type and automatic lathe spindles for bar stock feeding and gripping.
Fastener production lines making screws, bolts, and rivets from round bar.
Automotive component machining for valve guides, injector pins, and small shafts.
Medical device manufacturing for bone screws and surgical pins where concentricity is critical.
Connector and electronic pin production where the round bore grips small diameter brass or stainless steel.
The 42 type refers to the maximum bar capacity. It fits standard 42 mm spindle liners. The round bore design is for gripping round stock only. If you need hex or square bores, we can machine those too, but the round type is the most common.
Q: What is your MOQ?
A: No MOQ. We machine one piece for prototypes and small runs. The unit price for one piece is higher due to setup time, but we do not force you to buy 100 pieces to test a design.
Q: How do you guarantee tolerance and quality?
A: We grind the bore after heat treatment. That is the only way to hold ±0.005 mm. We inspect 100% of the critical dimensions on a CMM. The inspection report is included with the shipment. If a part fails your incoming inspection, we replace it at no cost.
Q: What is the lead time for a custom CNC collet chuck?
A: 15 working days for a prototype after drawing approval. Production batches of 100+ pieces take 20 working days. If you need it faster, we can expedite for an additional charge, but we will not skip inspection to save time.
Q: Do you provide material certificates and heat treatment reports?
A: Yes. We provide a mill certificate for the raw material (65Mn or your specified grade) and a heat treatment report with the actual hardness values per batch. All documents are in English and can be notarized if required.
Send your drawing
We are a made-in-China precision manufacturing partner that answers fast.
Send us your 2D drawing (PDF or DWG) and your 3D model (STEP or IGES). We will check the geometry, the tolerances, and the material spec. You will receive a firm quote within 12 hours. No hidden costs, no vague estimates.
Email: sc@bquq.com
WhatsApp: +86 13713157787
We speak engineer. We machine to your drawing. Let's get your collet chuck into production.