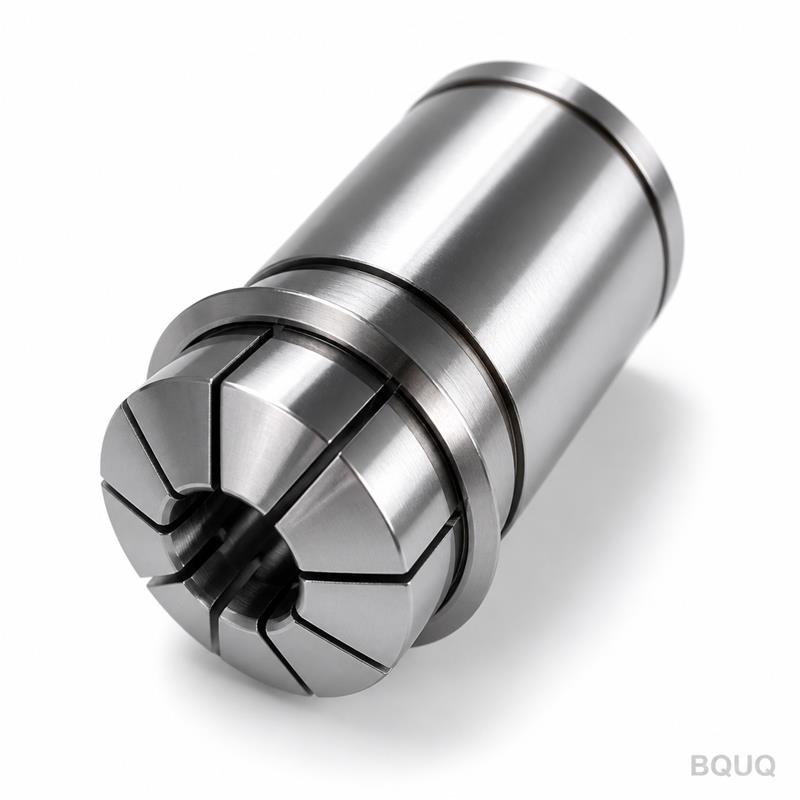
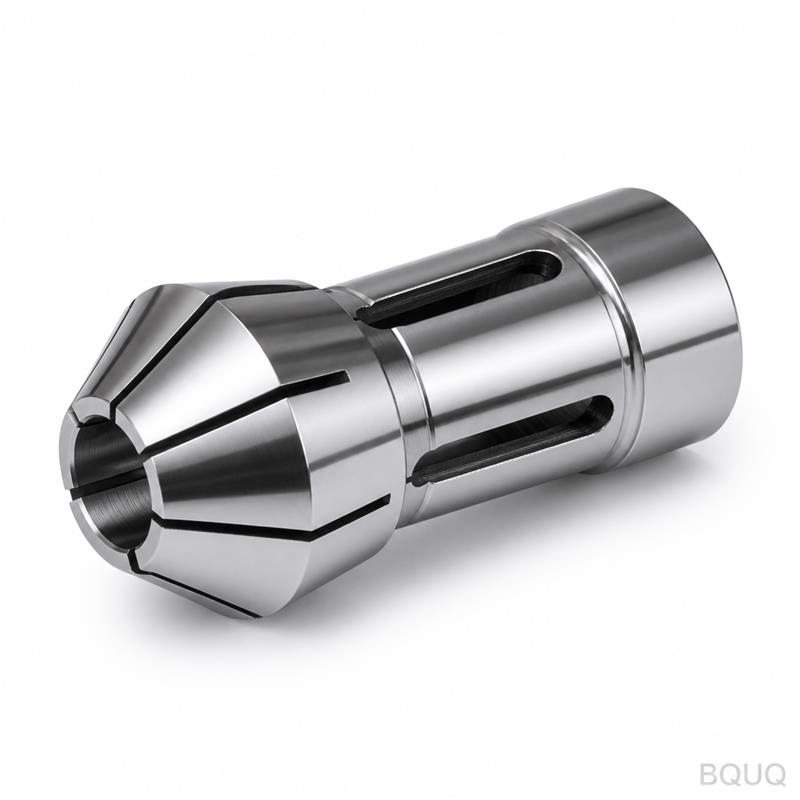
OpeningThis is a closeup of a 46-type collet chuck body, machined for an auto lathe spindle. The taper slot is cut to your exact drawing. We do not stock generic blanks. Every unit
Custom CNC Collet Chuck Auto Lathe 46 Type Taper Slot Closeup
OpeningThis is a closeup of a 46-type collet chuck body, machined for an auto lathe spindle. The taper slot is cut to your exact drawing. We do not stock generic blanks. Every unit is made from your C
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a closeup of a 46-type collet chuck body, machined for an auto lathe spindle. The taper slot is cut to your exact drawing. We do not stock generic blanks. Every unit is made from your CAD file, verified with a CMM before shipment.
At a glance: Tolerance ±0.005 mm on the taper angle, surface finish Ra 0.4, lead time 15 working days, no MOQ. One part or one thousand, same process control.
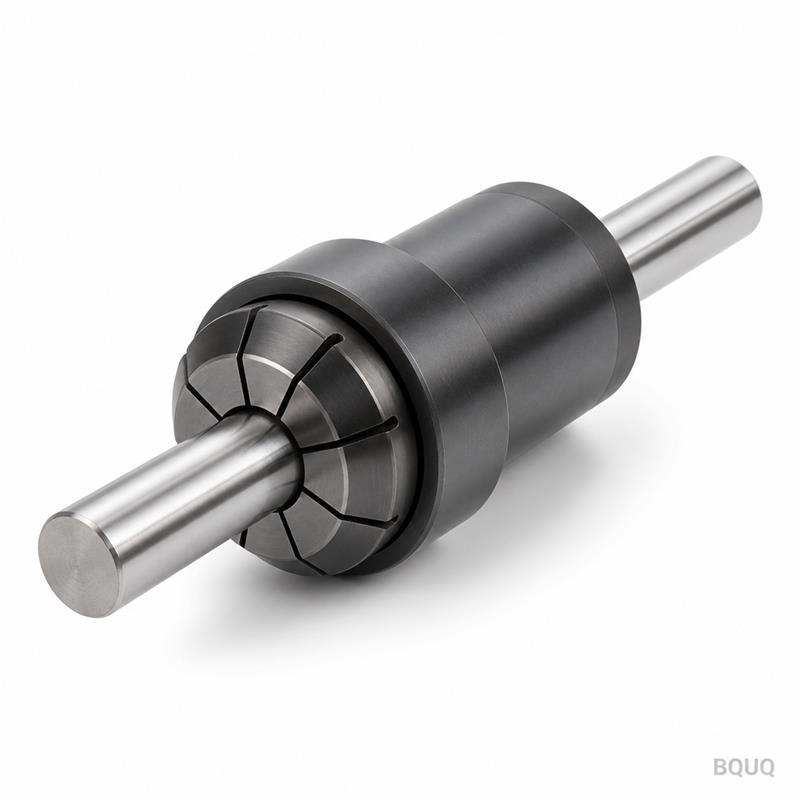
You send the drawing. We machine the collet. You receive a part that seats true on the spindle nose and grips the bar stock without runout.
Specifications
Parameter
Value
Material
20CrMnTi (case-hardened), 42CrMo, or 9Cr18 (stainless)
Hardness
58–62 HRC (case depth 0.8–1.2 mm)
Taper angle tolerance
±0.005 mm (measured on CMM)
Concentricity (ID to taper)
≤0.005 mm TIR
Surface finish
Ra 0.4 on taper, Ra 0.8 on slots
Slot width tolerance
±0.01 mm
Key process
CNC turning, CNC milling, wire EDM for slot relief
Heat treatment
Vacuum carburizing + gas quenching
Inspection
100% dimensional check, CMM report per batch
Batch size
1–500 pcs, no MOQ
Lead time
15 working days for first article, 10 days for repeat
Country of origin
Made in China, Dongguan factory
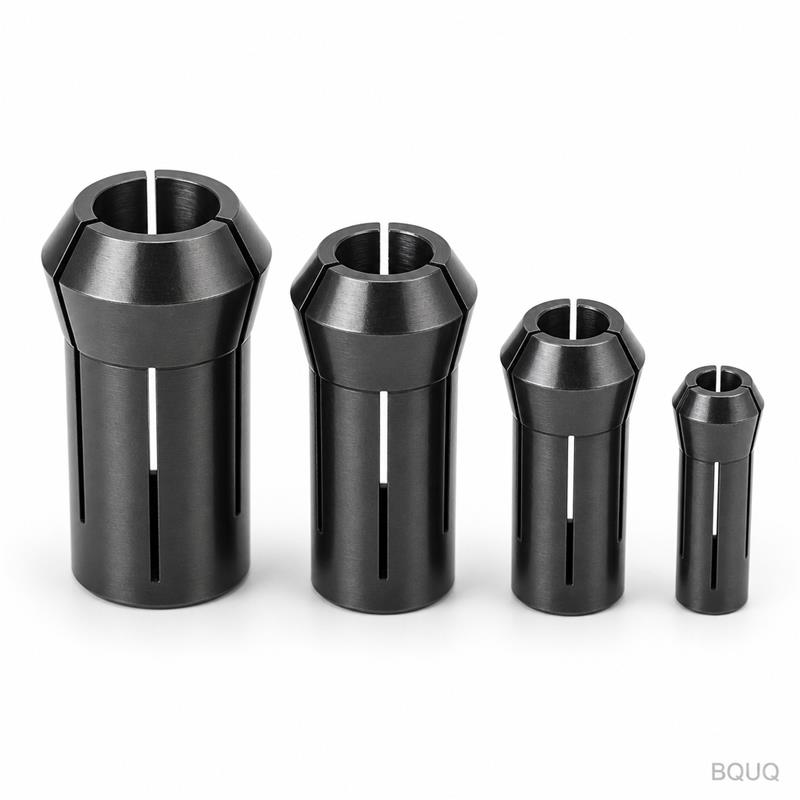
The 46-type collet is a standard auto lathe size, but the taper slot geometry is not standard. That slot controls the collapse and grip force. We cut it with a wire EDM after heat treatment, so the edges stay sharp and the slot width holds even after hardening.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality. Each heat lot gets a unique number. We record material batch, machine operator, heat treatment furnace log, and CMM results. If a part fails in your spindle, we trace it back to the exact ingot. No guessing.
2. Inspection report per batch. You get a dimensional report with every shipment. Not a generic certificate—actual measured values for taper angle, slot width, concentricity, and hardness. We sign it. We stand behind it.
3. One factory for CNC, stamping, springs, and heat sinks. Your collet chuck might need a spring for the release mechanism, a stamped retainer plate, or a heat sink for a high-speed spindle motor. We make all of them under one roof. One purchase order, one quality system, one shipping address. Fewer suppliers, fewer delays.
Where These Parts Are Used
A 46-type collet chuck with a precision taper slot is not a shelf item. It goes into:
Swiss-type auto lathes for medical screw machining—the slot must collapse evenly to hold 0.5 mm diameter wire without marking it.
Multi-spindle automatics in automotive fuel injector production. Cycle times are seconds, so the collet opens and closes millions of times. The slot edges take the wear.
High-speed CNC lathes for brass valve bodies. The taper seat must be true to the spindle nose, or you get chatter marks on the part.
Retrofit spindles on older cam-operated machines. Buyers send us the spindle nose drawing, and we match the taper to their existing holder.
In every case, the slot is the failure point. A worn slot means grip loss, part slippage, and scrap. Our slot is cut after hardening, so the grain structure is not disturbed. It stays sharp longer.
Q: What is the MOQ?
No MOQ. We run one piece for prototype validation, or 500 pieces for production. The per-piece price drops at 50 and 200 pieces, but the quality process is identical.
Q: How do you guarantee the taper tolerance?
We machine the taper on a CNC lathe with a live tooling turret, then measure it on a CMM with a 0.0001 mm resolution probe. If the angle is off by more than 0.005 mm, the part is scrapped. We do not blend or hand-fit.
Q: What is the standard lead time?
First article: 15 working days after drawing approval. Repeat orders: 10 working days. For urgent prototypes, we can do 7 days with a 20% surcharge. We do not quote faster than we can deliver.
Q: Do you provide material certificates?
Yes. Each batch ships with a mill certificate for the raw material, a heat treatment report, and our CMM inspection report. If you need third-party testing (SGS or TUV), we arrange it at cost.
Send Your Drawing
Stop guessing whether a stock collet will fit your spindle. Send us your drawing and we will quote the exact part.
Firm quote in 12 hours. We reply with a price, lead time, and a technical review of any critical tolerances. If we see a problem, we tell you before you order.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing is not a slogan. It is the CMM report we send with every batch. Send your drawing and see the difference.