OpeningYour ER11 collet chuck starts as a drawing, not a stock item. We machine it to your exact dimensions, verify it on a CMM, and ship it with a report. If it doesn‘t match your
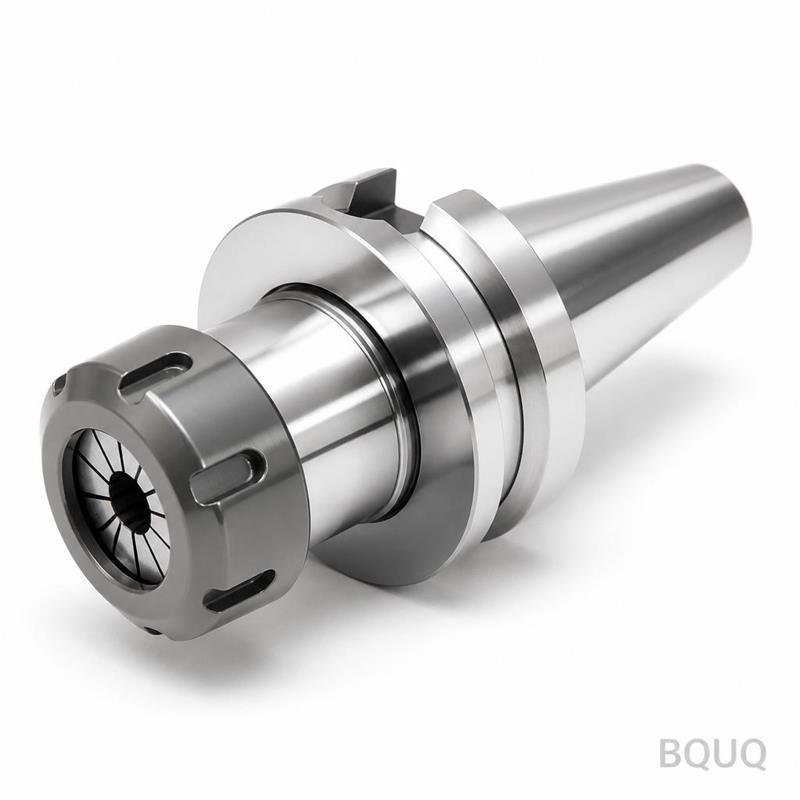
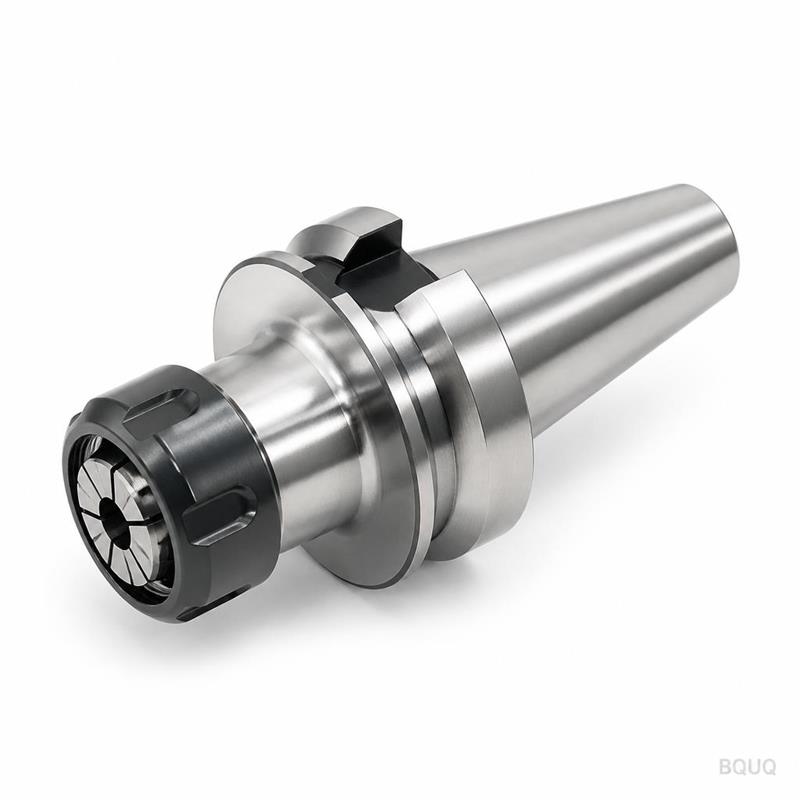
Custom CNC Collet Chuck ER11 | Precision Manufacturing Made in China
OpeningYour ER11 collet chuck starts as a drawing, not a stock item. We machine it to your exact dimensions, verify it on a CMM, and ship it with a report. If it doesn't match your print, you don't pa
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
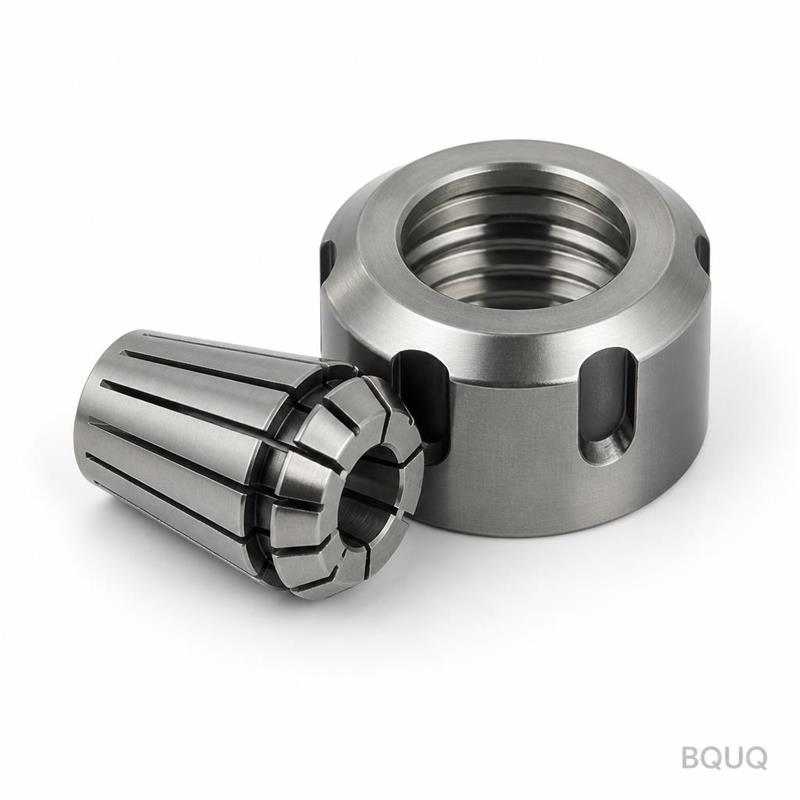
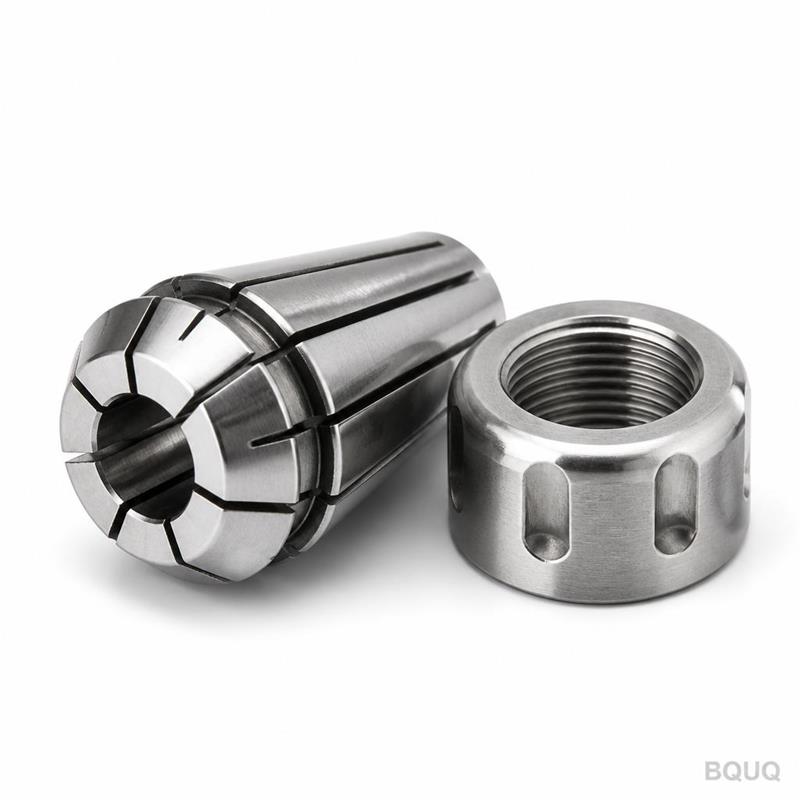
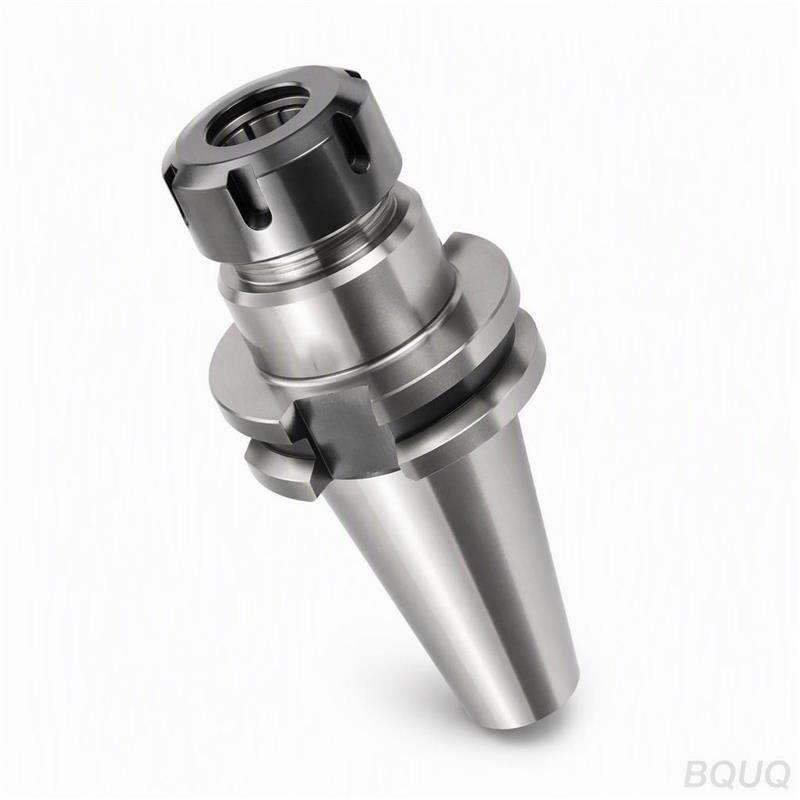
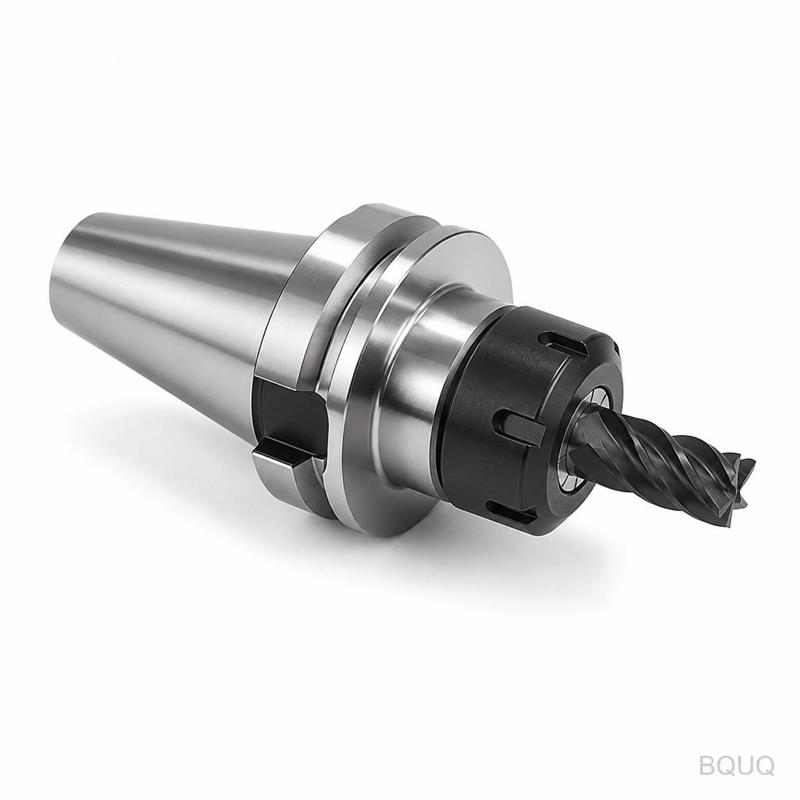
Your ER11 collet chuck starts as a drawing, not a stock item. We machine it to your exact dimensions, verify it on a CMM, and ship it with a report. If it doesn't match your print, you don't pay.
At a glance: Runout ≤ 0.005 mm TIR, hardness 58–62 HRC, lead time 7–12 days, no MOQ.
Specifications
Parameter
Value
Material options
20CrMnTi, 40Cr, 65Mn, or customer-specified steel
Heat treatment
Carburized or induction hardened, 58–62 HRC
Surface finish
Ra 0.4 μm on taper, Ra 0.8 μm on OD
Runout (TIR)
≤ 0.005 mm at nose, ≤ 0.01 mm at 50 mm from nose
Taper accuracy
AT3 per DIN 6499 / ISO 15488
Thread form
ER11 collet nut thread, M14 x 0.75 or per drawing
Keyed slots
Broached or wire-cut, ±0.02 mm
Coating option
Black oxide, TiN, or no coating
Inspection
100% dimensional check, CMM report included
Batch size
1 piece to 10,000 pieces
Lead time
7 days for prototypes, 12 days for production
MOQ
None
Machining is done on 5-axis CNC lathes and machining centers. We hold tolerances down to ±0.005 mm where your print requires it. Each part is deburred, cleaned, and rust-protected before packing.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Every heat number and batch is logged. If a material issue appears six months later, we trace it to the exact melt. You get a part number, not a guess.
2. Inspection report per batch. You receive a dimensional report with actual measured values, not just a pass/fail stamp. We measure taper angle, thread pitch, and runout on every piece. No random sampling.
3. One factory for CNC + stamping + spring + heatsink. Your collet chuck might need a spring for the collet retention or a stamped washer for the nut. We make all of it under one roof. Fewer vendors, fewer handoffs, fewer tolerance stack-ups.
Where these parts are used
ER11 collet chucks are the workhorse for small-diameter toolholding. Common applications include:
Engraving machines — holding 1–7 mm end mills and gravers
CNC routers — wood, aluminum, and plastic cutting
Automated tool changers — where repeatable clamping force matters
Medical device machining — small drills and reamers in tight spaces
Jewelry and watchmaking — precision micro-machining operations
If your machine uses ER11 collets, you need a chuck that seats the collet perfectly. A poor taper means runout, and runout means broken tools and bad finishes.
Q: What is your minimum order quantity?
A: No MOQ. We make one prototype or ten thousand production parts. Prototype pricing is slightly higher per piece, but production pricing drops at 100, 500, and 1,000 pieces.
Q: How do you guarantee tolerance and quality?
A: We inspect 100% of parts. Runout is measured on a precision spindle with a dial indicator. Taper angle is checked with a calibrated gauge. You get the CMM report with your shipment.
Q: What is your lead time?
A: 7 days for prototypes, 12 days for production batches. If you need faster, we can split the batch and ship partial quantities. Air freight is available.
Q: Can you provide material certificates?
A: Yes. We provide mill certificates for the raw material and heat treatment reports. Material grade is traceable to the original melt.
Send your drawing
Send us your PDF, STEP, or IGES file. We will review the geometry, check for manufacturability, and send a firm quote within 12 hours. No hidden costs, no surprises.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing made in China — with the paperwork to prove it.