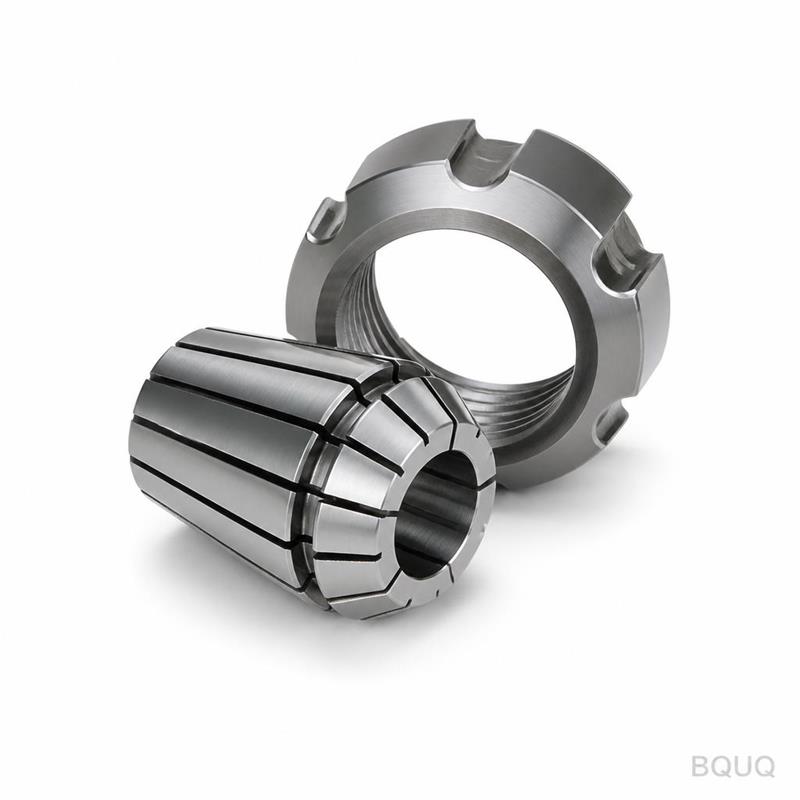
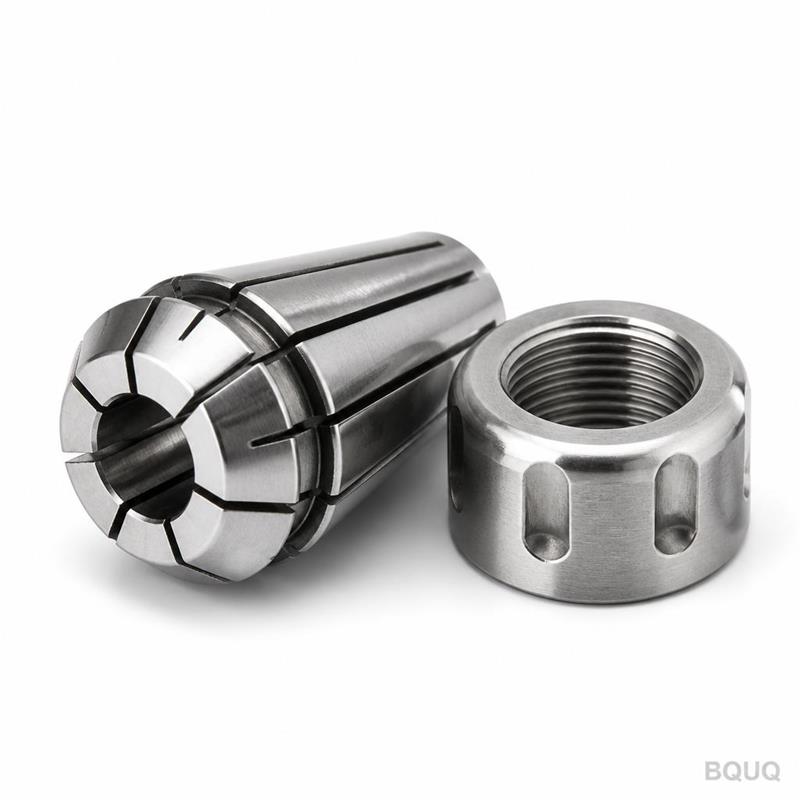
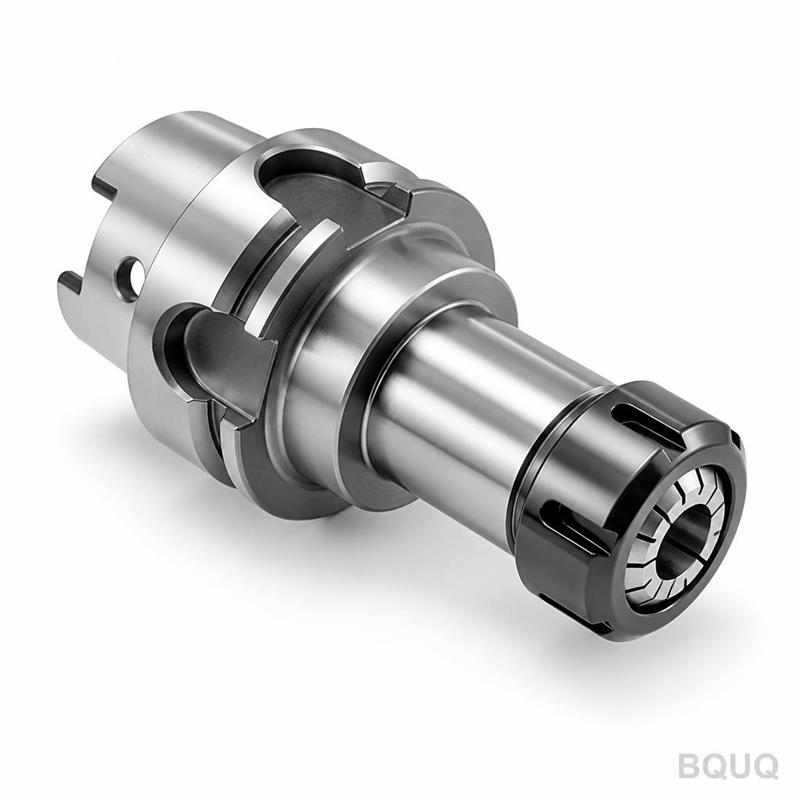
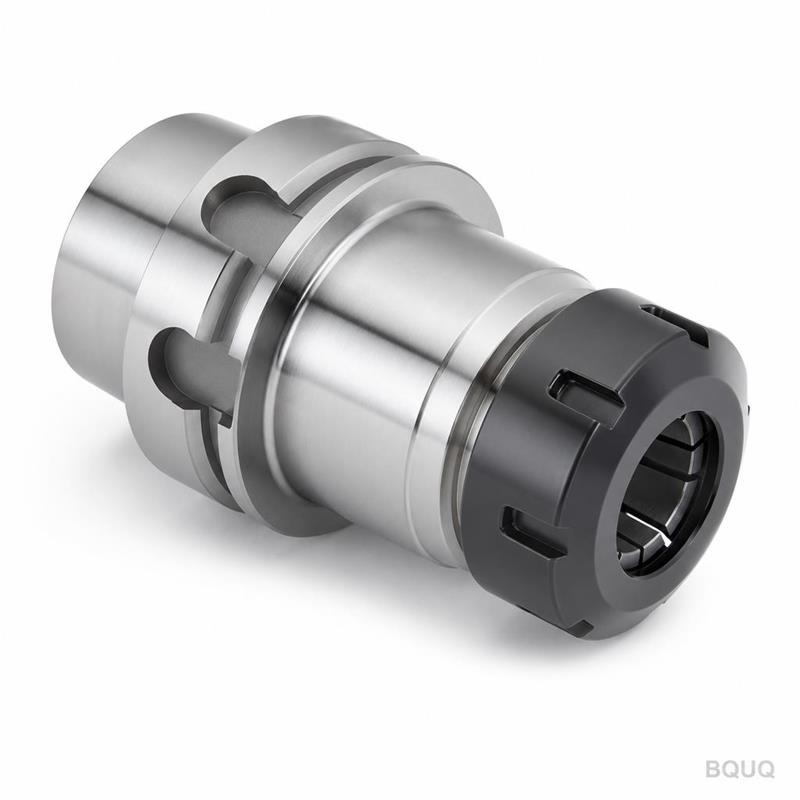
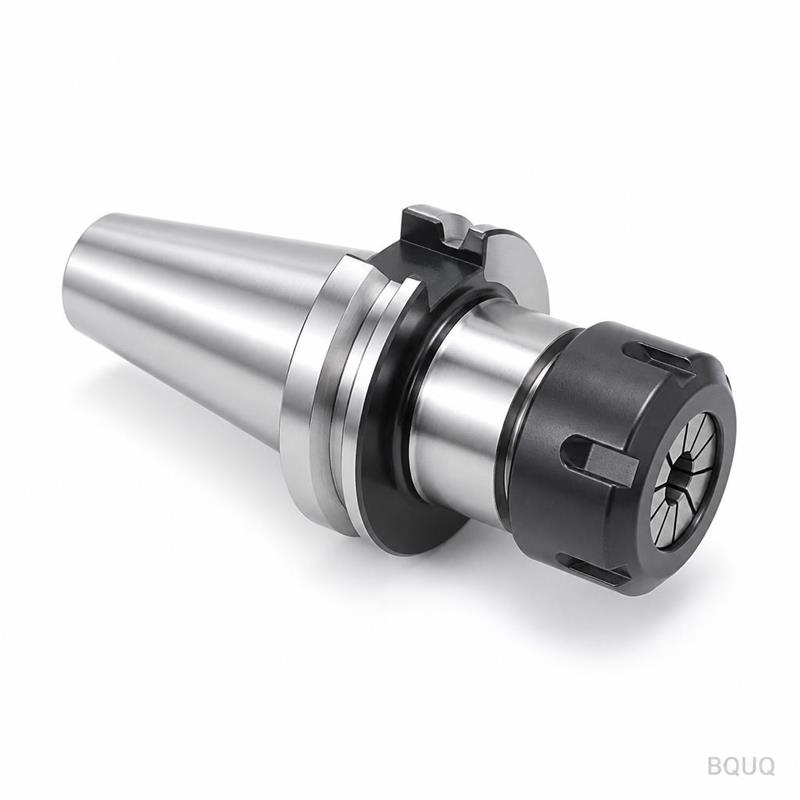
OpeningYour ER16 collet chuck starts as a raw bar of alloy steel. We machine it to your drawing, not a stock catalog part. Every thread, every taper, every concentricity callout is
Custom CNC Machined ER16 Collet Chuck & Nut | Precision Made in China
OpeningYour ER16 collet chuck starts as a raw bar of alloy steel. We machine it to your drawing, not a stock catalog part. Every thread, every taper, every concentricity callout is verified before shi
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your ER16 collet chuck starts as a raw bar of alloy steel. We machine it to your drawing, not a stock catalog part. Every thread, every taper, every concentricity callout is verified before shipment. You get a tool holder that runs true on your spindle, not a gamble.
Tolerance: ±0.005 mm on critical diameters (ER16 taper and thread)
Lead time: 7–12 days for custom batches
No MOQ: order 1 piece or 1,000
Material: AISI 4140 or 8620, hardened to HRC 52–56
Made in China, inspected per batch, shipped with a report
Specifications
Parameter
Value
Notes
Material
AISI 4140 / 8620 / 12L14
Customer-specified alloys accepted
Hardness
HRC 52–56 (through-hardened)
Surface hardness for wear resistance
Taper accuracy
AT3 or better
ER16 taper angle 8° per side
Thread accuracy
6H (internal) / 6g (external)
M16x1.5 or M18x1.5 per drawing
Concentricity
≤0.005 mm TIR
Measured at nose, with test bar
Surface finish
Ra 0.4 µm on taper, Ra 0.8 µm elsewhere
Black oxide or plain finish
Machining process
CNC turning, milling, grinding
5-axis available for complex slots
Inspection
CMM + thread gauges + taper gauge
100% critical dimensions checked
Batch size
1–10,000 pieces
No MOQ, tooling amortized per order
Lead time
7 days for prototypes, 12 days for production
Air freight available
We grind the ER taper on a dedicated internal grinder. We do not just turn it. That is the difference between a chuck that holds a tool once and one that holds it the same way every time. Threads are cut with single-point inserts, then rolled if you need higher fatigue life.
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Every batch gets a heat number. Every part gets a serial number laser-marked on the body. If a problem shows up on your spindle, we trace it back to the exact bar, the exact machine, the exact operator. That is not common in this industry.
2. Inspection report per batch.
You do not have to ask for it. Each shipment includes a dimensional report: taper angle, thread pitch diameter, concentricity, hardness. We use a CMM and calibrated gauges. The report is signed by the QC lead. If you need a full PPAP or material certs, we provide those too.
3. One factory for CNC + stamping + springs + heat sinks.
Your collet chuck is not the only part you buy. We also run presses for stampings, CNC lathes for springs, and dedicated lines for heat sinks. Send us a full assembly drawing. We quote the chuck, the nut, the retention knob, and the spring collet in one email. One supplier, one freight bill, one quality standard.
Where these parts are used
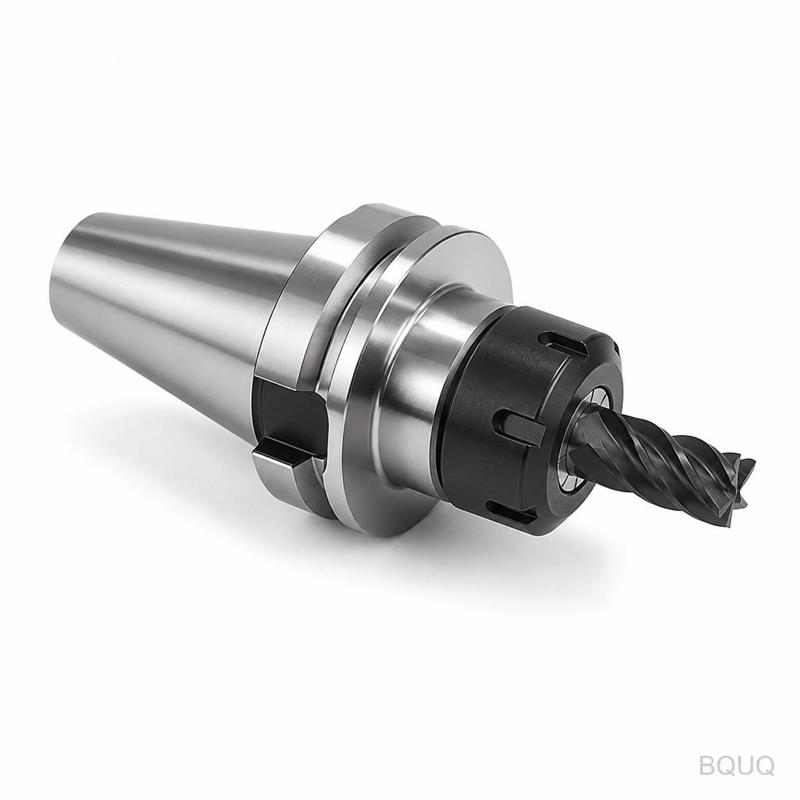
ER16 collet chucks are not just for hobby mills. They hold end mills, drills, and reamers in production environments where tool change time is money.
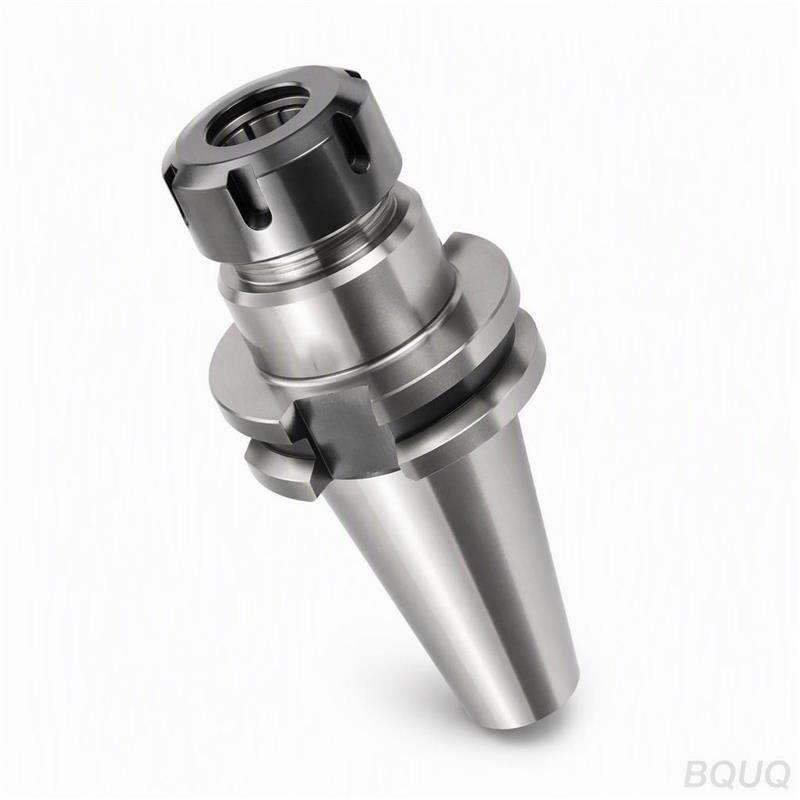
CNC machining centers: Used in BT30, BT40, and HSK spindles for light to medium milling. The ER16 size handles tool shanks from 1 mm to 10 mm.
Swiss-type lathes: The compact body fits in tight tool positions. We make short versions for sliding headstocks.
Automotive line tooling: High-volume drilling and tapping stations use ER16 chucks for quick changeover. Our hardened nuts survive thousands of cycles.
Aerospace fixture work: When you need to hold a 3 mm end mill at 15,000 RPM without runout, the ER16 taper and thread accuracy matter.
Medical device machining: Small diameter tools, high precision, no room for chatter. Our chucks are balanced for low vibration at high speed.
We also make custom variants: extended noses, through-coolant holes, and special thread pitches for non-standard spindles. If your drawing calls for it, we machine it.
Q: What is your MOQ?
Zero. We make one piece for a prototype or 5,000 for production. The price per piece drops with quantity, but we do not force you to buy more than you need. No MOQ is a policy, not a marketing line.
Q: How do you guarantee tolerance and quality?
We grind the taper and thread, not just turn them. Every part is checked with a CMM and a calibrated ER taper gauge. Concentricity is measured with a test bar in a V-block. We ship a per-batch inspection report. If a part is out of spec, we replace it at our cost.
Q: What is the lead time?
Prototypes (1–5 pieces) ship in 7 days. Production runs (50+ pieces) ship in 10–12 days. We have standard blanks in stock for ER16 bodies and nuts. If you need faster, we can expedite with air freight, but we do not skip inspection to save a day.
Q: Do you provide material certificates?
Yes. We provide mill certificates for the raw material (ASTM or DIN equivalent) and a heat treatment certificate if you harden the part. These are included free with every batch. Third-party testing is available at cost.
Send your drawing
Send us your PDF or STEP file. We reply with a firm quote in 12 hours. The quote includes unit price, tooling cost (if any), lead time, and shipping options. We do not ask for a minimum order. We do not ask for a commitment. We just ask for the drawing.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing is not a slogan. It is a set of measurements. Send us yours.