OpeningYour drawing defines the part. Our machines do the rest. We machine SK40 ER32 collet chucks to your exact print, then verify every critical dimension before the crate leaves
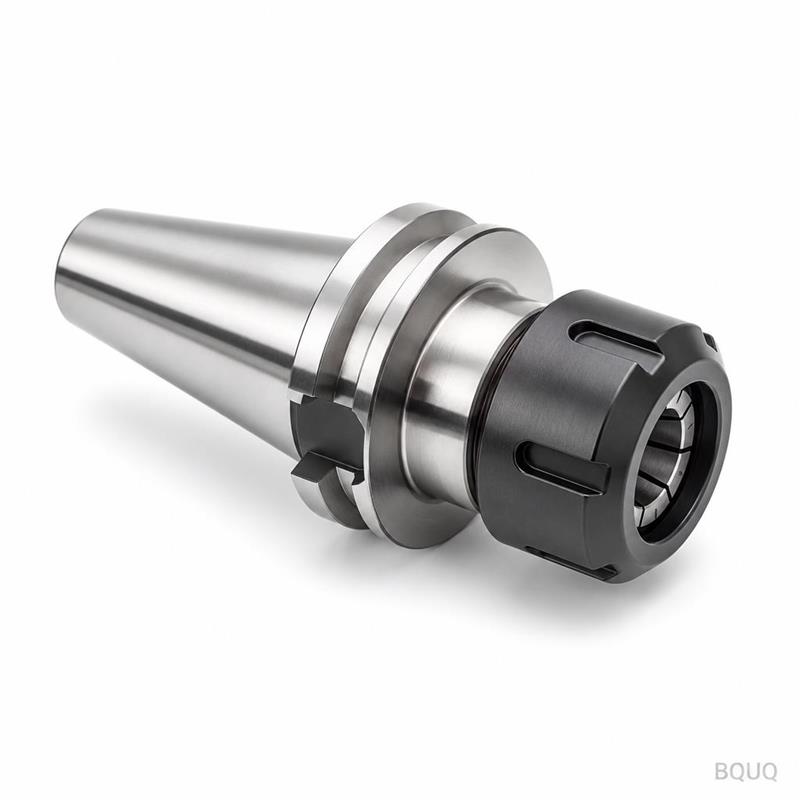
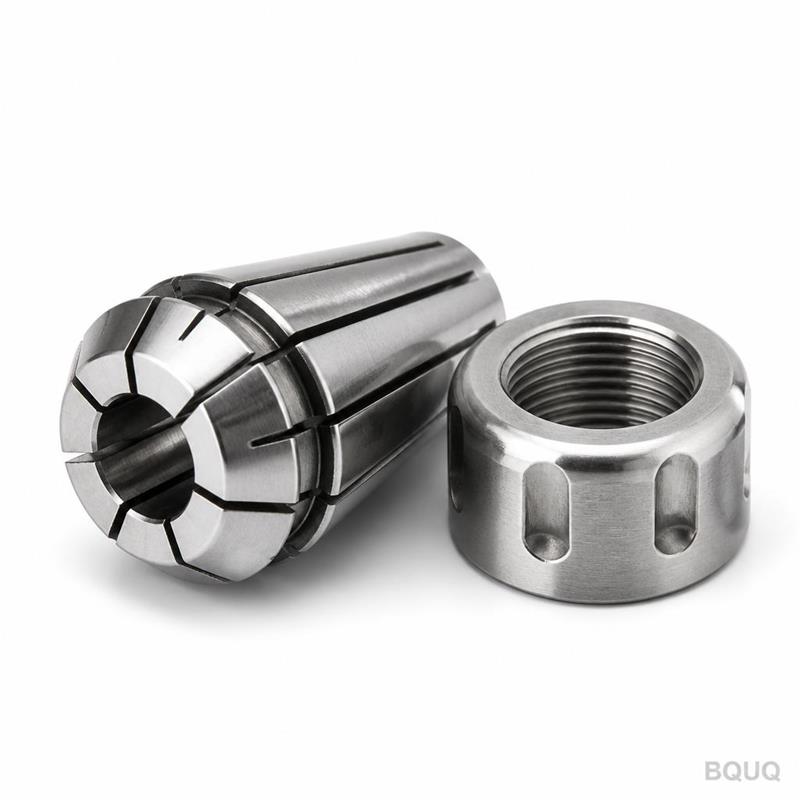
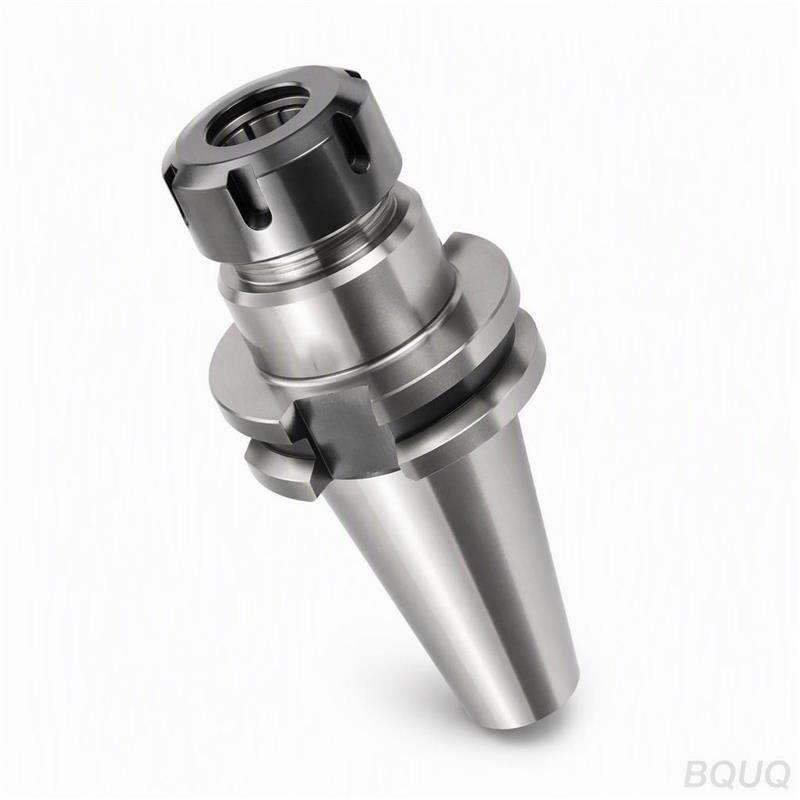
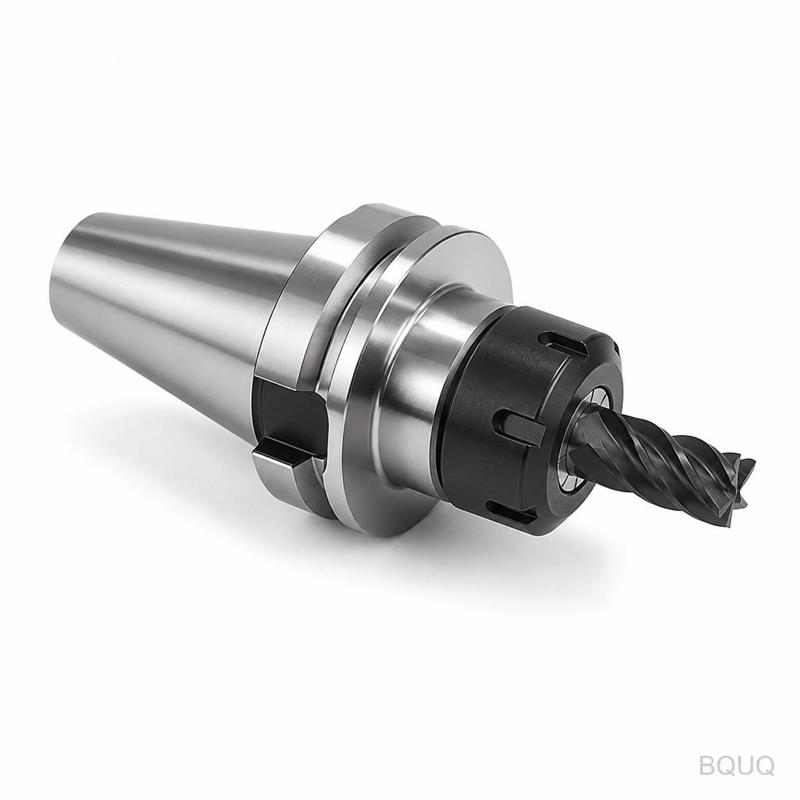
Custom CNC Collet Chuck Tool Holder SK40 ER32 Precision Made in China
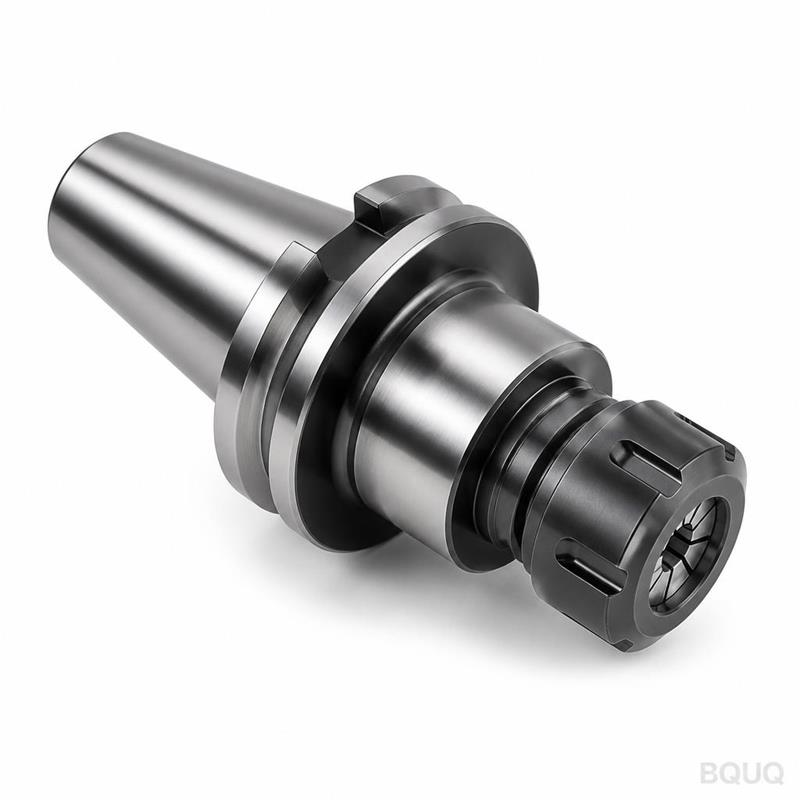
OpeningYour drawing defines the part. Our machines do the rest. We machine SK40 ER32 collet chucks to your exact print, then verify every critical dimension before the crate leaves our Dongguan floor.
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
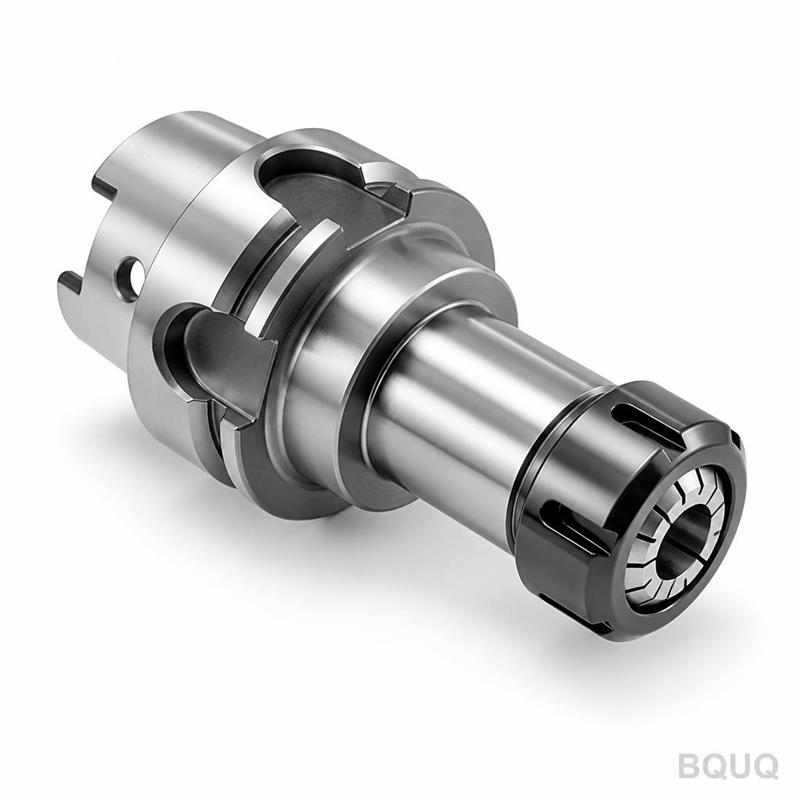
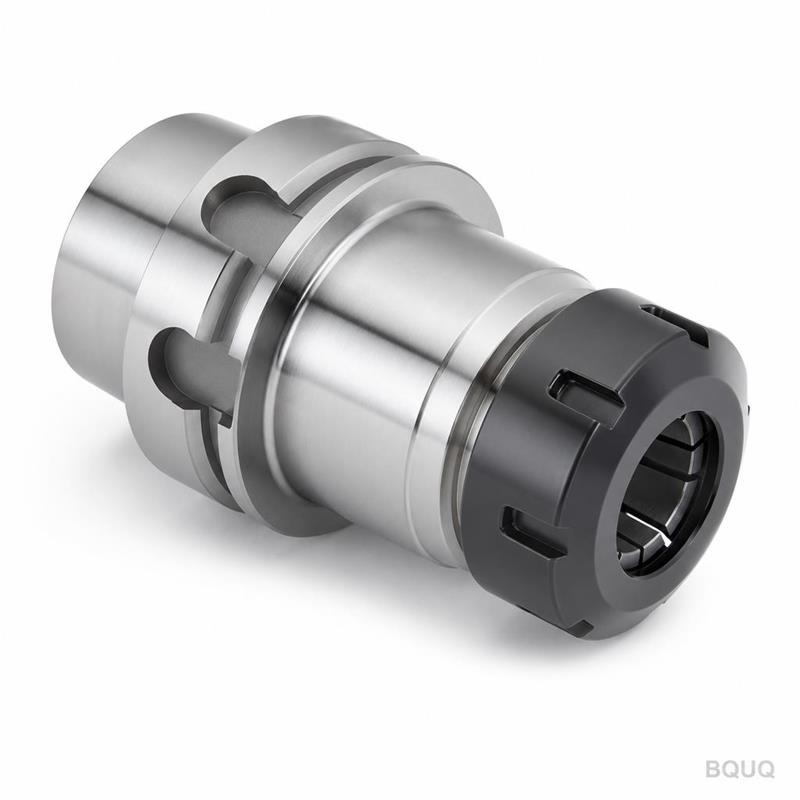
Your drawing defines the part. Our machines do the rest. We machine SK40 ER32 collet chucks to your exact print, then verify every critical dimension before the crate leaves our Dongguan floor. This is not a stock item. It is a custom part, built for your spindle, your tooling, and your tolerance stack-up.
At a glance: Runout accuracy within 0.005 mm TIR at the nose. Material options include 20CrMnTi or 42CrMo4. Lead time 15-20 working days after drawing approval. No MOQ—order one prototype or a thousand pieces.
Specifications
We treat a collet chuck as a precision instrument, not a weldment. The table below shows our standard capabilities for this product family. If your print calls for something tighter, we will quote it—our machining center holds ±0.003 mm when required.
Parameter
Value
Material
20CrMnTi (case-hardened), 42CrMo4 (quenched & tempered), or per your spec
≤ 0.005 mm at nose, ≤ 0.010 mm at 100 mm from nose
Surface Finish
Ra 0.4 µm on taper, Ra 0.8 µm on body
Coating
Black oxide, electroless nickel, or TiN (optional)
Inspection
100% dimensional check, CMM report included per batch
Batch Size
1 piece to 5,000 pieces
Lead Time
15 working days for prototype, 20 days for production
We grind the internal taper after heat treatment. That step is non-negotiable. It is the only way to hold the runout number we promise. We also balance the chuck body to G2.5 grade if your application runs above 8,000 RPM.
Three Reasons Buyers Send Us Their Drawings
1. Batch-traceable quality. Every chuck gets a heat number and a work order number. If a problem shows up in your toolroom six months later, we can trace it back to the heat-treat batch, the grinding wheel, and the operator. No guesswork. No "maybe it was another supplier."
2. Inspection report per batch. You get a CMM report with actual measured values, not a checkbox. We measure taper angle, runout at three axial positions, and hardness at two points. The report ships with the parts. Your incoming QC can verify in 10 minutes instead of 2 hours.
3. One factory for CNC + stamping + springs + heat sinks. You send us the collet chuck drawing. We machine it. But if your assembly also needs a stamped cover plate, a compression spring for the release mechanism, or a heat sink for the spindle drive, we make those too. One purchase order, one shipping dock, one quality standard. Fewer vendors, fewer arguments.
Where These Parts Are Used
SK40 ER32 collet chucks are not exotic. They are workhorses. We see them in these real applications:
Vertical machining centers holding end mills for die and mold work. The 0.005 mm runout keeps finishing passes clean.
CNC lathes with live tooling where an ER32 collet grips a drill or a tap for secondary operations.
Automotive transfer lines that run 24/7. The case-hardened 20CrMnTi version survives millions of cycles without wear on the taper.
Aerospace fixture work where a machinist needs to swap tools quickly between aluminum and titanium parts. The SK40 taper seats repeatably, and the ER32 nut gives a positive grip.
Prototype shops that need one-off chucks modified for non-standard shank lengths. We cut the pocket depth to your drawing, not a catalog standard.
If your spindle takes an SK40 pull stud, this chuck will fit. We machine the pull stud groove to DIN 69872 or MAS BT, depending on your machine.
Q: What is your MOQ?
A: No MOQ. We machine one piece for a prototype or a repair. The per-piece price is higher for a single unit, but the engineering and setup are the same. For production runs, we offer tiered pricing at 50, 200, and 500 pieces.
Q: How do you guarantee tolerance and quality?
A: We inspect 100% of critical dimensions on every part. The taper is measured with an air gauge, not a caliper. Runout is checked on a precision mandrel with a 0.001 mm indicator. You receive the CMM report with the shipment. If a part fails your incoming inspection, we replace it and pay the freight.
Q: What is your lead time?
A: Prototype (1-5 pieces): 15 working days after drawing approval. Production (50+ pieces): 20 working days. Heat treatment adds 3-4 days. We can expedite to 10 days for an additional charge if your spindle is down.
Q: Do you provide material certificates?
A: Yes. We supply mill certificates for the raw material (EN 10204 3.1) and a heat-treatment report showing hardness and case depth. If you need a full traceability package with chemical composition, we include it at no extra cost.
Send Your Drawing
Stop guessing. Send us your PDF or STEP file. We will review the geometry, check the tolerance against our machine capability, and come back with a firm quote in 12 hours. No vague estimates. No "maybe we can do it."
We are a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining experience. Your custom CNC collet chuck will be made in China, but it will meet or exceed the quality of any European or Japanese source—at a fraction of the cost.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Send the drawing. Get the quote. We will handle the rest.