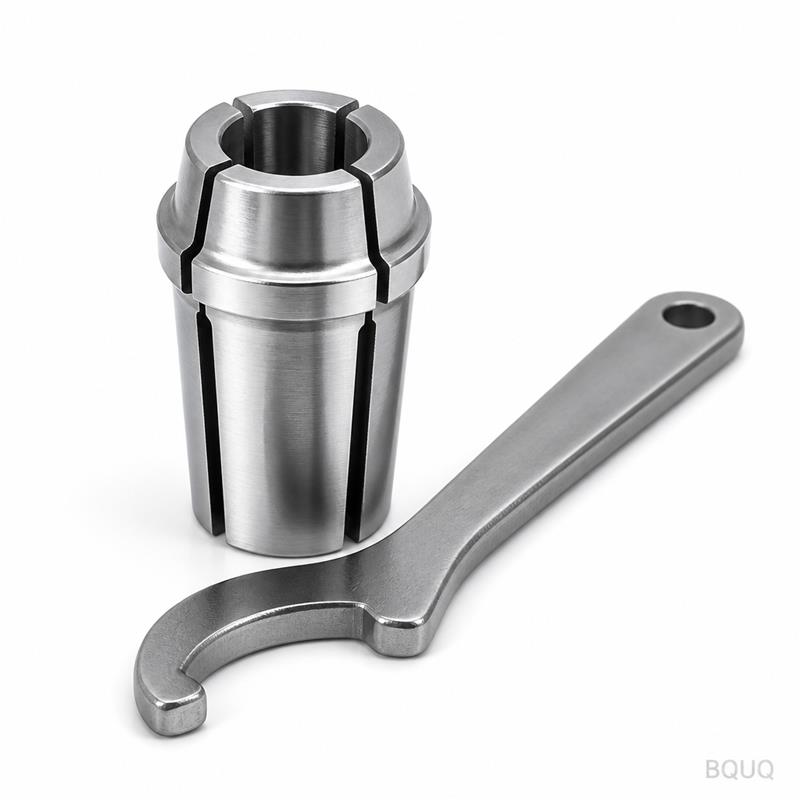
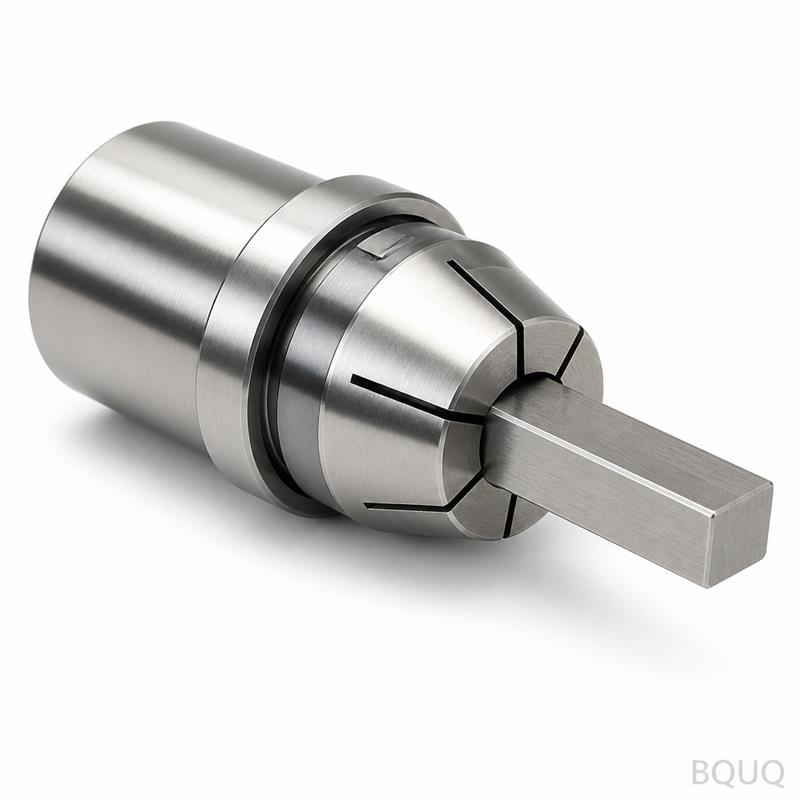
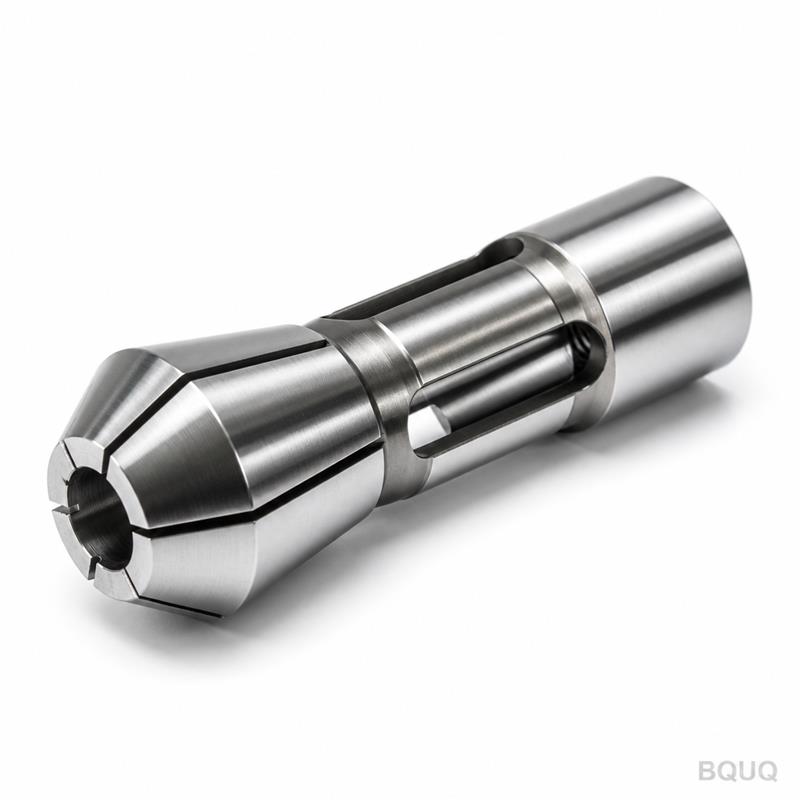
This is a complete CNC collet chuck package: a hardened, precision-ground collet body plus a matched spanner wrench set for quick tool changes on automatic lathes. You get 0.005 mm
BQUQ CNC Machined Auto Lathe Collet With Spanner Wrench Set | Precision Manufacturing
This is a complete CNC collet chuck package: a hardened, precision-ground collet body plus a matched spanner wrench set for quick tool changes on automatic lathes. You get 0.005 mm TIR (total indicate
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a complete CNC collet chuck package: a hardened, precision-ground collet body plus a matched spanner wrench set for quick tool changes on automatic lathes. You get 0.005 mm TIR (total indicated runout) at the gripping bore, HRC 58-62 surface hardness, and a standard 7-day lead time from our Dongguan factory. No MOQ, no minimum order friction—buy one set or a thousand.
How ER Collet Chucks Grip Tooling Without Runout
The collet body is machined from a single billet of 20CrMnTi alloy steel, then carburized and hardened. The 8-slot design collapses evenly under the spanner wrench’s torque, pulling the bore concentric to the spindle axis. We grind the inner bore to a 0.005 mm tolerance band, which means your drills, end mills, or turning tools repeat within 5 microns across 100 consecutive tool changes. The spanner wrench set is matched to the collet’s nut torque spec (typically 70-90 Nm for ER32), so you never over-tighten and distort the gripping zone.
Materials and Heat Treatment We Use
We start with 20CrMnTi for the collet body—it gives a tough core (HRC 35-40) and a hard case (HRC 58-62) after carburizing. The spanner wrenches are 40Cr steel, quenched and tempered to HRC 45-50. The mating threads on the collet nut are rolled, not cut, to avoid stress risers. Every batch is hardness-tested on a Rockwell tester, and we reject any part below HRC 58. This is precision manufacturing, not stamping—everything is CNC machined in our 8,000 m² Dongguan facility.
Spanner Wrench Set Design: Why It Matters
The two-piece wrench set (one fixed hook, one pin spanner) is laser-cut and then CNC-machined for exact fit on the collet nut. The hook end has a 15° chamfer that seats into the nut’s slots without scratching the surface finish. The pin spanner’s pins are hardened to HRC 50 and ground to ±0.02 mm diameter, so they engage the nut holes without slop. This isn’t a generic toolbox wrench—it’s a precision tool that protects your collet’s runout over years of use.
Inspection Before Every Shipment
Each collet is 100% inspected on a Mitutoyo CMM for bore diameter, taper angle, and slot width. Runout is verified with a dial indicator on a test mandrel—we record the actual value on the inspection report, not just a pass/fail. Surface finish is checked with a profilometer; we guarantee Ra 0.4 µm on the gripping bore and Ra 0.8 µm on the taper. The spanner wrench set is dimensionally checked against a master collet nut. You get a signed certificate with every order, whether it’s one set or 500.
CNC Machining Tolerances and Surface Finish Specs
The taper angle is ground to AT3 grade (better than AT4), which is the ISO standard for ER collets. Bore tolerance is +0.005 / -0.000 mm. The outer diameter is held to ±0.01 mm. We machine the slots with a 0.3 mm wire EDM for zero burr on the edges. The spanner wrench set’s working surfaces are ground to ±0.02 mm. These numbers aren’t theoretical—they’re what we hit on every production run, verified by our in-house QC lab.
Parameter
Specification
Collet material
20CrMnTi alloy steel
Wrench material
40Cr steel, HRC 45-50
Collet hardness
HRC 58-62 (case-hardened)
Collet sizes available
ER11, ER16, ER20, ER25, ER32, ER40
Gripping bore tolerance
+0.005 / -0.000 mm
Runout (TIR)
0.005 mm at 3× diameter from nose
Surface finish (bore)
Ra 0.4 µm
Taper accuracy
AT3 grade per ISO 15488
Lead time
7 days standard (3 days for ER11/ER16)
MOQ
No MOQ—single set accepted
Why Auto Lathe Operators Switch to Our Collets
Swiss-type and automatic lathes run at 8,000-12,000 RPM. At that speed, a 0.02 mm runout becomes 0.1 mm at the tool tip—enough to scrap a part. Our collets hold the 0.005 mm spec at 10,000 RPM, verified by our spin-test rig. The spanner wrench set ensures you can change tools in under 15 seconds, which adds up to 40+ minutes saved per 8-hour shift. If you’re working with tight-tolerance medical or aerospace parts, this is the difference between rework and first-pass yield.
Customization Options for Non-Standard Tool Shanks
Need a bore for a 2.5 mm shank when the standard is 3.0 mm? We machine custom bores in 48 hours. Need a longer gripping length for a stubby drill? We can extend the collet body by 10 mm without affecting runout. Need a different wrench angle to fit your machine’s tool post? We’ll modify the spanner geometry. Since we’re the factory, not a trader, we don’t charge a “customization fee”—you pay for the material and machining time only. Send your drawing and we’ll quote within 12 hours.
Packing and Shipping from Our Dongguan Factory
Every collet is individually wrapped in anti-rust paper, then placed in a fitted plastic case with the spanner wrench set. The case is foam-lined to prevent impact damage during freight. We ship via DHL, FedEx, or UPS—door-to-door in 3-5 days to the US, EU, or Southeast Asia. For orders over 50 sets, we use palletized air freight with wooden crates that meet ISPM-15. All packaging is labeled with the part number, batch code, and inspection date for full traceability.
Quality Control and Traceability You Can Audit
We’ve been manufacturing in Dongguan since 2005, and our QC process is ISO 9001:2015 certified. Each batch gets a unique heat number, and we keep records for 10 years. If you have a downstream failure, we can trace the raw material, heat treatment furnace, and CNC machine that produced your collet. We also do random destructive testing—cutting a collet open to check case depth (minimum 0.8 mm) and microstructure. This isn’t just paperwork; it’s how we protect your production line.
Pricing and Firm Quote Within 12 Hours
We know engineers need numbers fast. Send us your drawing (PDF, STEP, or IGES) and we’ll return a firm, itemized quote within 12 business hours. Price includes material, machining, heat treatment, grinding, inspection, and packaging—no hidden charges. For standard sizes like ER32, our price is typically 15-20% lower than German or Japanese equivalents, because we control the entire process in-house. Made in China doesn’t mean lower quality—it means lower overhead, which we pass to you.
What is the minimum order quantity (MOQ)?
No MOQ—you can order a single CNC Machined Auto Lathe Collet With Spanner Wrench Set for testing, and we’ll treat it with the same priority as a 500-piece order.
Can you customize the collet bore or wrench geometry?
Yes, we machine custom bores (any diameter from 1.0 mm to 26.0 mm) and modify the spanner wrench set’s angle, length, or pin configuration based on your machine tool’s access constraints.
How do you ensure quality for small orders?
Every collet, regardless of order size, goes through the same 100% CMM inspection, hardness test, and runout verification—we don’t have a separate “low-volume” QC line.
What is the typical lead time for a custom collet set?
Standard sets ship in 7 days; custom bore collets take 10-12 days from drawing approval, including heat treatment and final grinding.
Get a firm quote within 12 hours. Email your drawing to sc@bquq.com or WhatsApp +86 13713157787. Include the collet size, bore diameter, and quantity—we’ll send pricing and a delivery date the same business day.