BQUQ CNC Machined Precision Flanges Couplings | Zero-Runout Hubs, 24h Lead Time
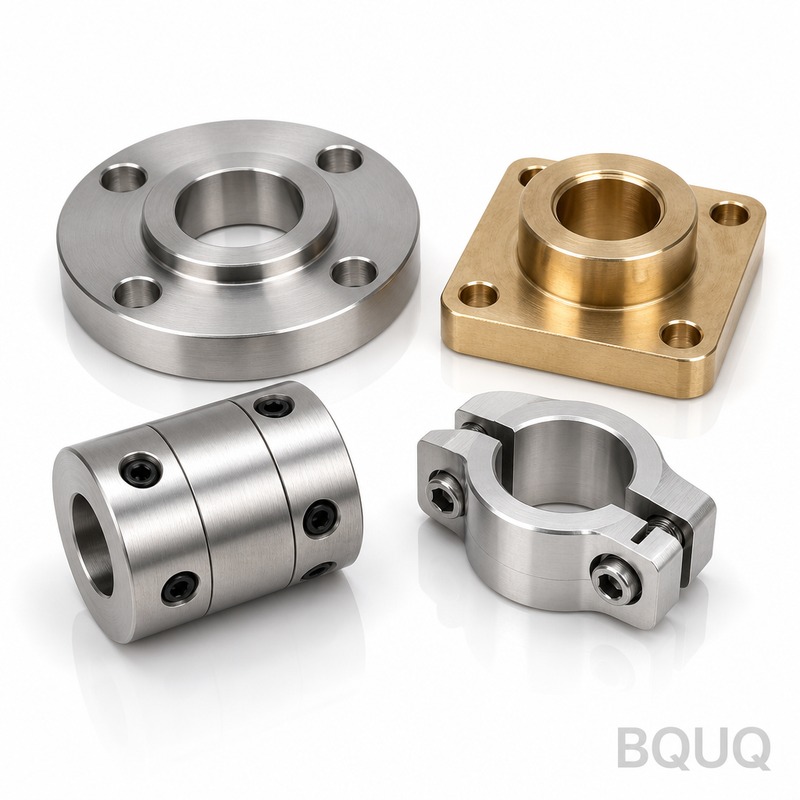
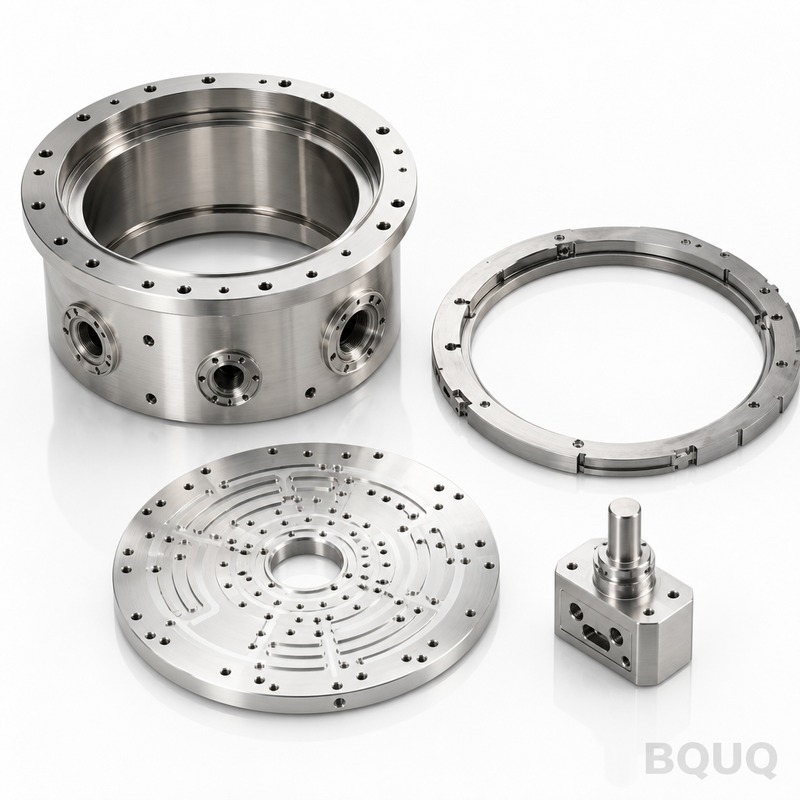
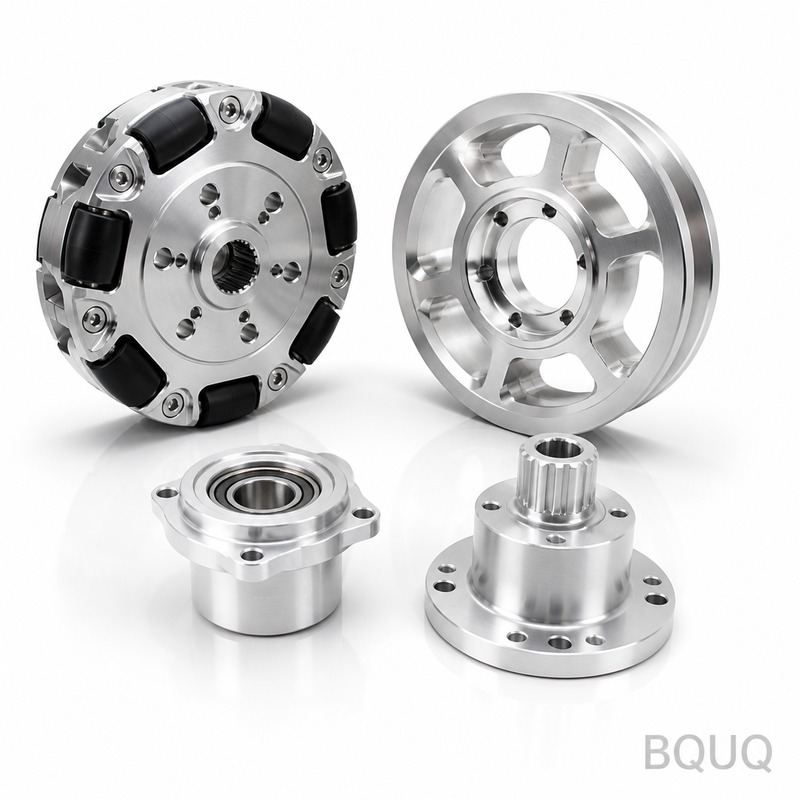
These are CNC machined flanges and couplings used to transfer torque between shafts, mount chucks, or locate fixtures—all machined in one setup at our Dongguan factory. We hold radial runout to 5 µm
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
These are CNC machined flanges and couplings used to transfer torque between shafts, mount chucks, or locate fixtures—all machined in one setup at our Dongguan factory. We hold radial runout to 5 µm and bore tolerances to ±0.005 mm, with hardness up to 58 HRC on request. Typical lead time is 7 days for small batches, and we offer no MOQ for standard blank sizes.
How We Eliminate Runout on the Pilot Bore and Flange Face
Runout kills tool life and spoils part concentricity. We machine the pilot bore and the flange face in the same clamping operation on our Mazak 5-axis mills. That means the datum features are cut without re-chucking, so the geometric relationship is not dependent on operator skill. For critical couplings, we add a final skiving pass with a CBN insert—this removes the work-hardened layer from roughing and brings surface finish to Ra 0.4 µm. Our inspection reports show actual runout values, not just "within spec" statements.
Materials and Heat Treatment We Use for Flanges and Couplings
We stock 1045, 4140, 4340, and 17-4PH stainless steel in round bar and plate. For standard flanges, we use 1045 in the normalized condition (HB 170-210) and hard turn the mating faces. If you need wear resistance, we offer through-hardening of 4140 to 28-32 HRC, or induction hardening of the bore and keyway to 50-55 HRC. For corrosive environments, 17-4PH is provided in H1025 condition (33-38 HRC). We also machine aluminum 6061-T6 and 7075-T6 flanges for servo motor mounts where weight is critical.
Bore Finishing: Honing vs. Fine Boring vs. Internal Grinding
The bore is where most coupling failures start. For bores under 25 mm, we fine bore with a PCD insert, holding H7 tolerance and a 0.8 µm Ra finish. For bores 25-80 mm, we switch to Sunnen honing—this gives a cross-hatch pattern that retains lubricant and reduces fretting on keyed shafts. For bores over 80 mm or those requiring hardened surfaces above 45 HRC, we internally grind with a CBN wheel. We do not use reamers for final bores; reamers copy the existing hole position error. Boring or grinding corrects it.
Balancing and Keyway Standards for High-Speed Rotation
If your coupling spins above 3,000 RPM, unbalance vibration will damage bearings. We dynamically balance every flange above 150 mm diameter to G2.5 grade per ISO 1940-1. For keyways, we cut to DIN 6885 or ANSI B17.1 with a broach, not an end mill. A broached keyway has parallel sides and a flat bottom—an end mill leaves a radius that reduces the effective shear area by up to 15%. We also offer involute splines (DIN 5480) on request. Each balanced part is marked with the residual unbalance value on the flange face.
Inspection Before Every Shipment: CMM and Hardness Reports
Every flange coupling leaves with three documents: a dimensional report from our Zeiss CMM (accuracy ±1.5 µm), a surface finish trace printout, and a material certificate with heat number. We do not do batch sampling—we measure 100% of critical dimensions on 100% of parts. For runout, we use a Talyrond roundness machine, not a V-block and dial indicator. The difference matters: a V-block test can miss lobing errors. If the part has a keyway, we verify the keyway position with an optical comparator before deburring.
Surface Finish Options: From Machined to Black Oxide to Electroless Nickel
Bare machined steel will rust within a week in humid air. We offer three standard finishes. Black oxide (MIL-DTL-13924) for indoor use, giving 0.5 µm thickness and good oil retention. Electroless nickel (AMS 2404) at 25 µm for corrosion resistance—this is what we recommend for washdown environments. For aluminum flanges, we hard anodize to 60 HRC equivalent (per MIL-A-8625 Type III) with a 50 µm coating. We do not offer zinc plating by default because it hydrogen embrittles high-strength steels above 40 HRC unless baked—we can do it but we will ask you to sign a waiver.
Flange Coupling Design Checks Before Quoting
Send us your drawing, but first check three things. One: the pilot bore should be the datum, not the bolt circle. Two: if the flange OD exceeds 200 mm, tell us the required balance grade—G2.5 adds one hour of machining time. Three: specify the thread class for any tapped holes (2B is standard, 3B for high-vibration). We will flag the same issues in your drawing review. Our engineers will call out any missing GD&T callouts within 4 hours of receiving your file. We machine to ISO 2768-mK for undimensioned features, but we prefer you dimension everything.
No MOQ—we machine single prototypes and million-piece production runs with the same quality system.
Can you modify a standard flange drawing for my existing motor mount?
Yes, we accept DXF, STEP, or PDF and will redraw your bolt pattern and pilot bore to match the motor flange within 24 hours.
How do you guarantee the 5 µm runout on every piece?
We measure 100% of parts on a Talyrond roundness machine and include the numerical report in the shipment, not a pass/fail certificate.
What is the fastest lead time for a rush order of 10 couplings?
If the material is in stock (1045 or 6061-T6), we can ship in 3 days by air freight from our Dongguan plant.
Get a firm quote within 12 hours. Email your drawing to sc@bquq.com or send it to us on WhatsApp at +86 13713157787. We will reply with a unit price, lead time, and a design review checklist—no generic sales pitch. This is precision manufacturing from a 20-year-old Chinese factory that treats your tolerance as a contract, not a suggestion.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.