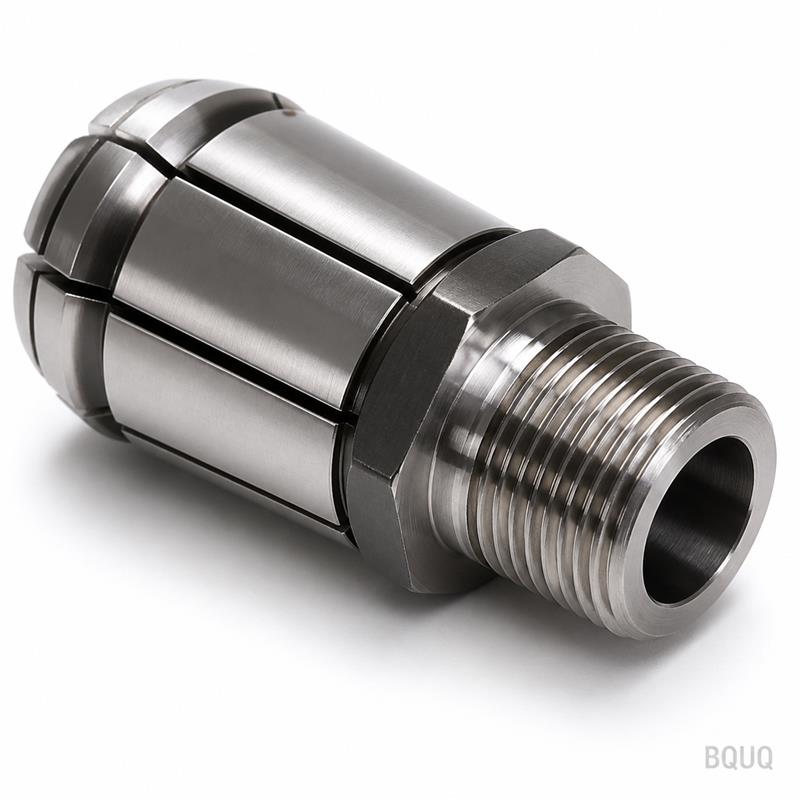
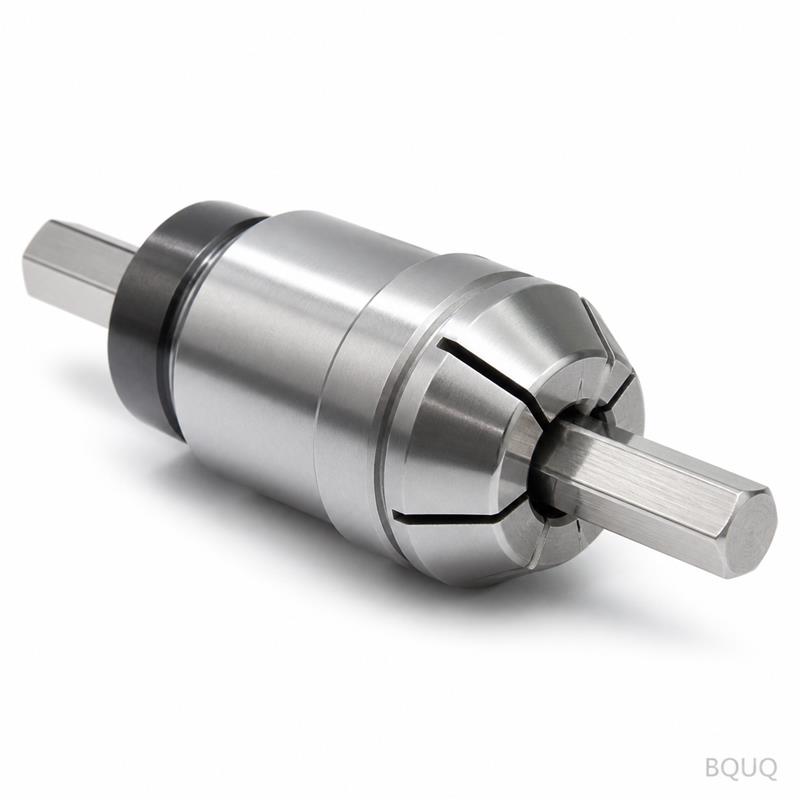
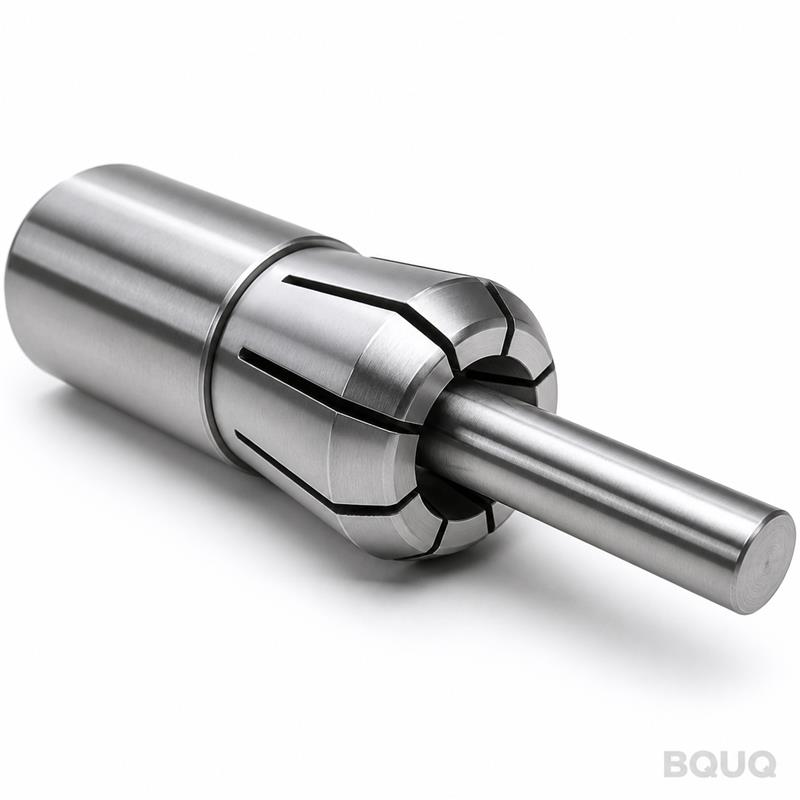
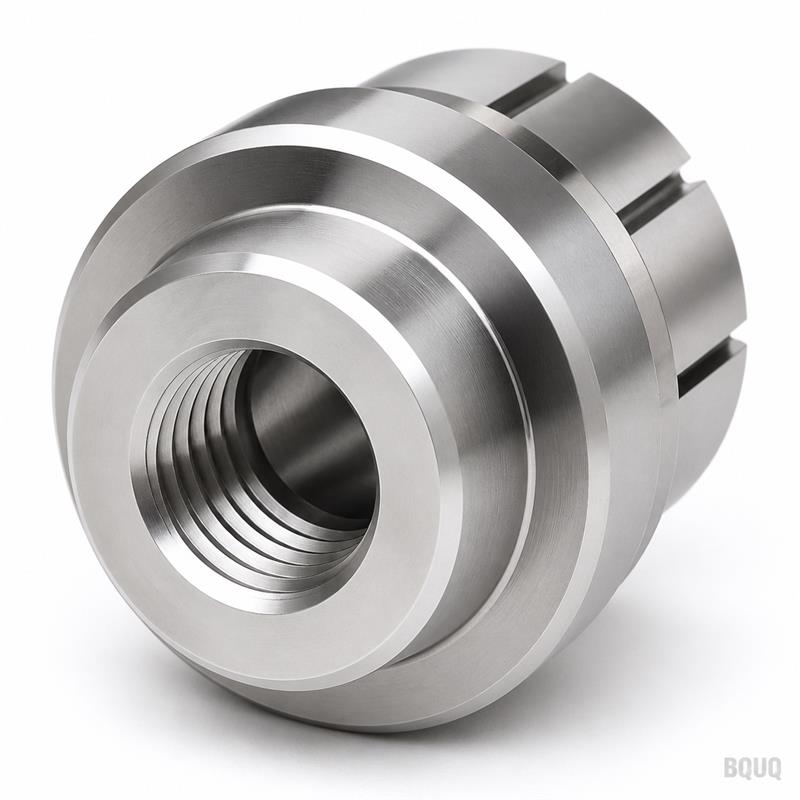
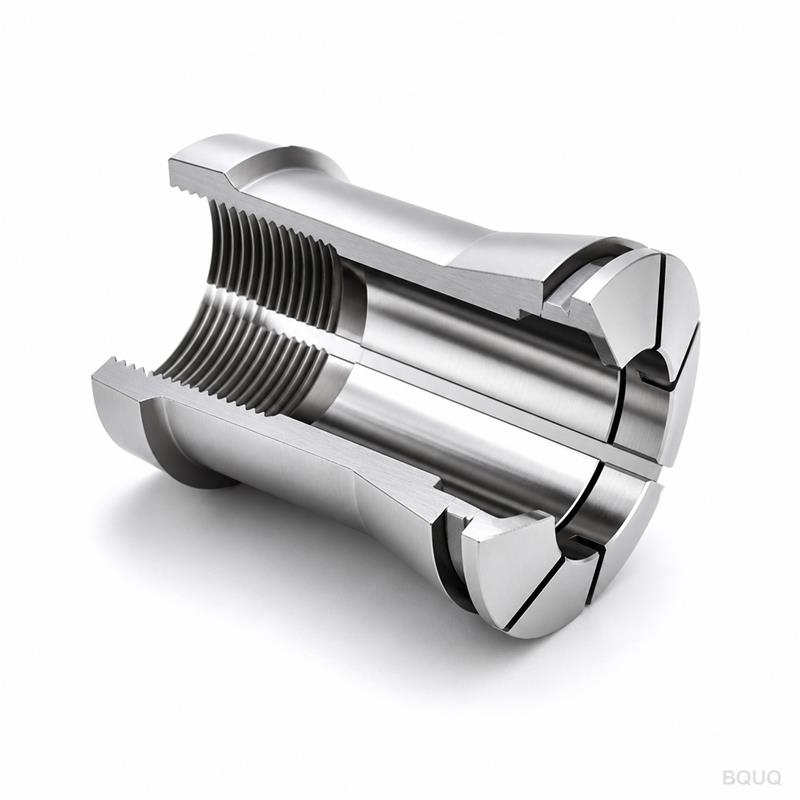
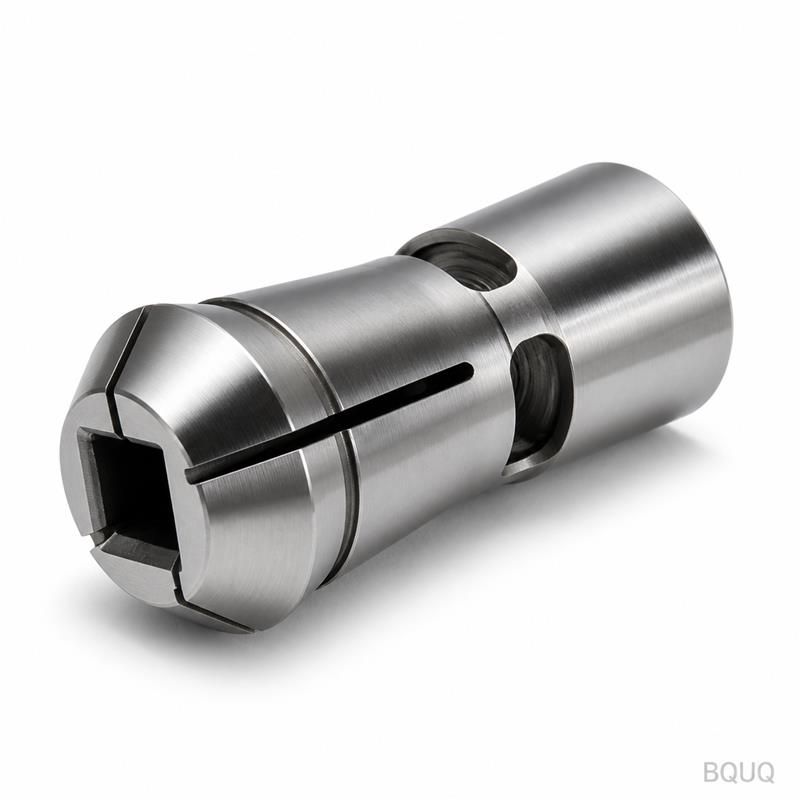
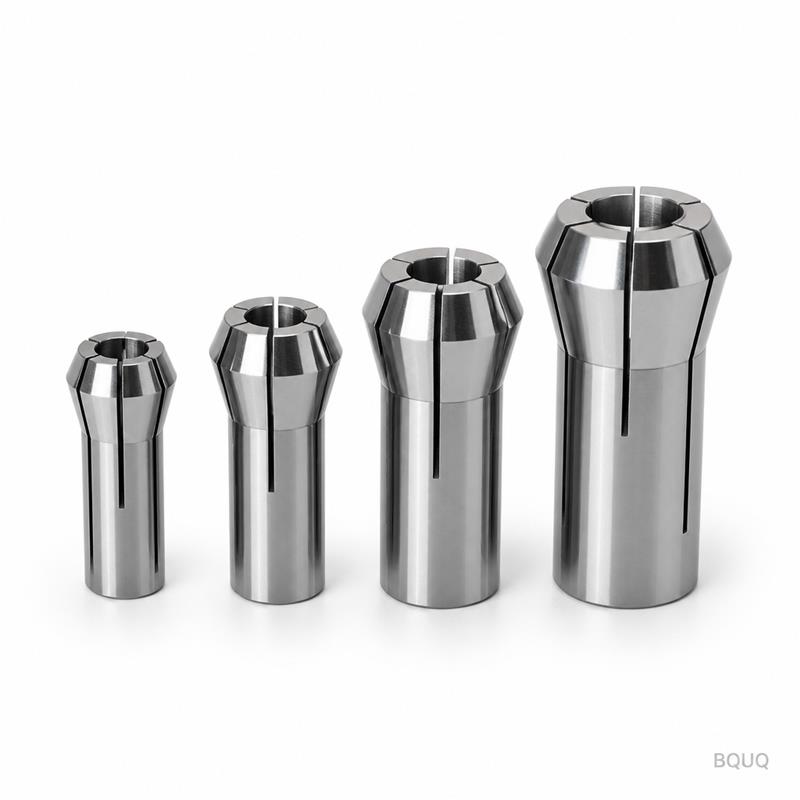
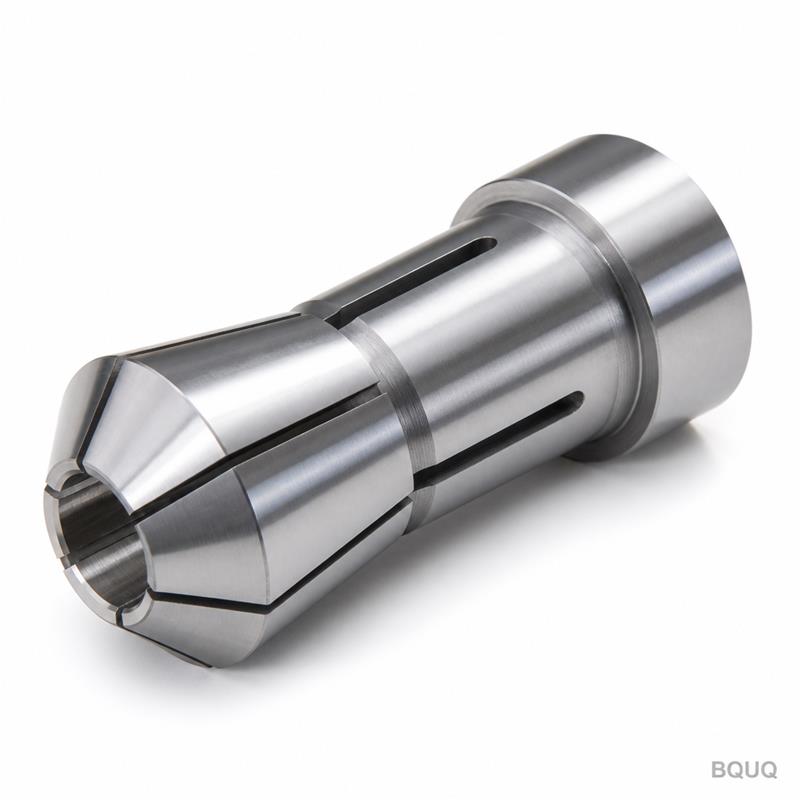
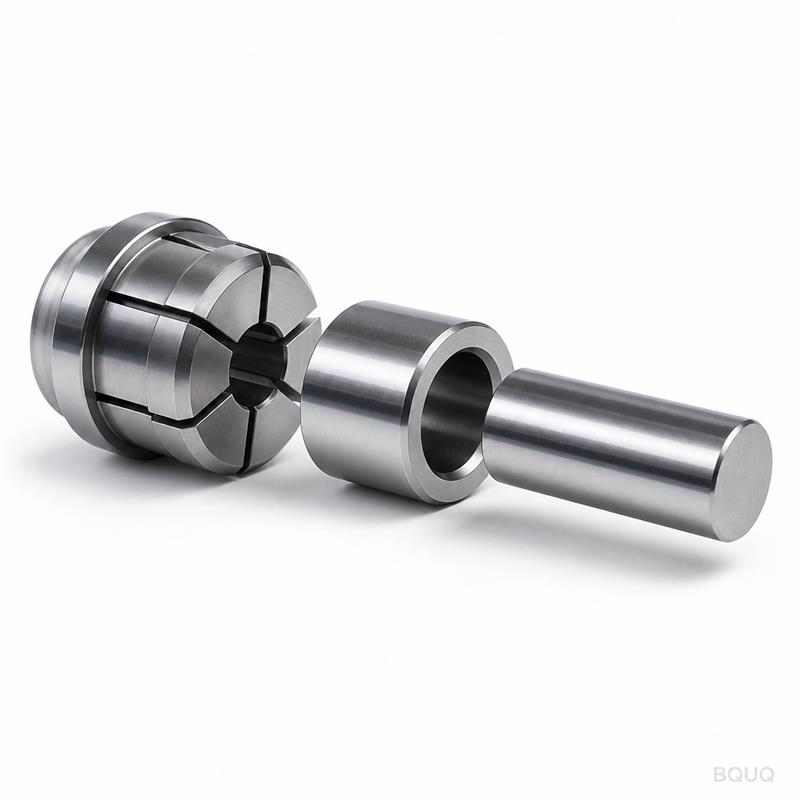
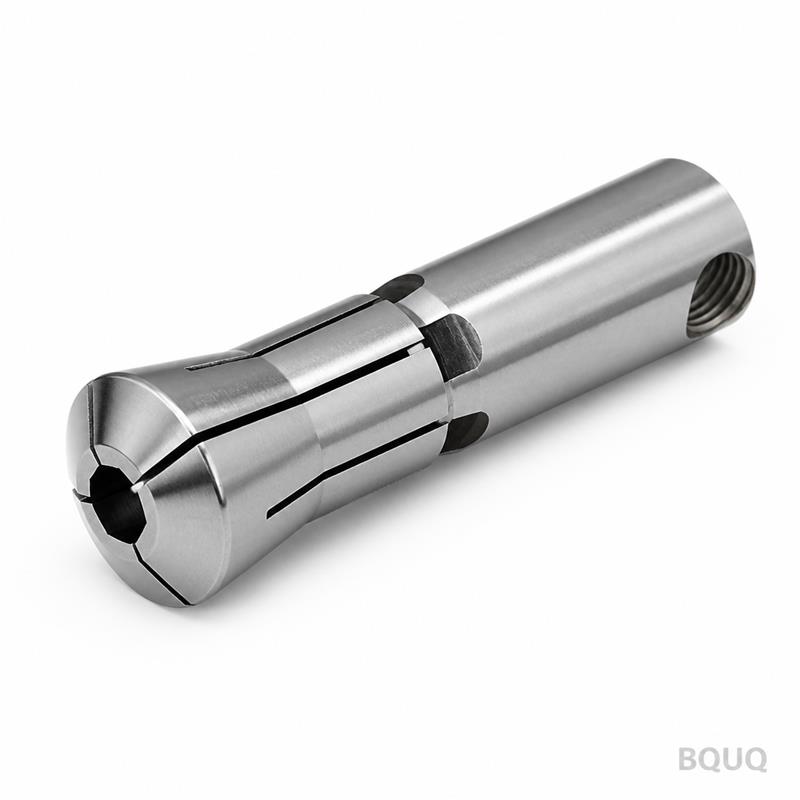
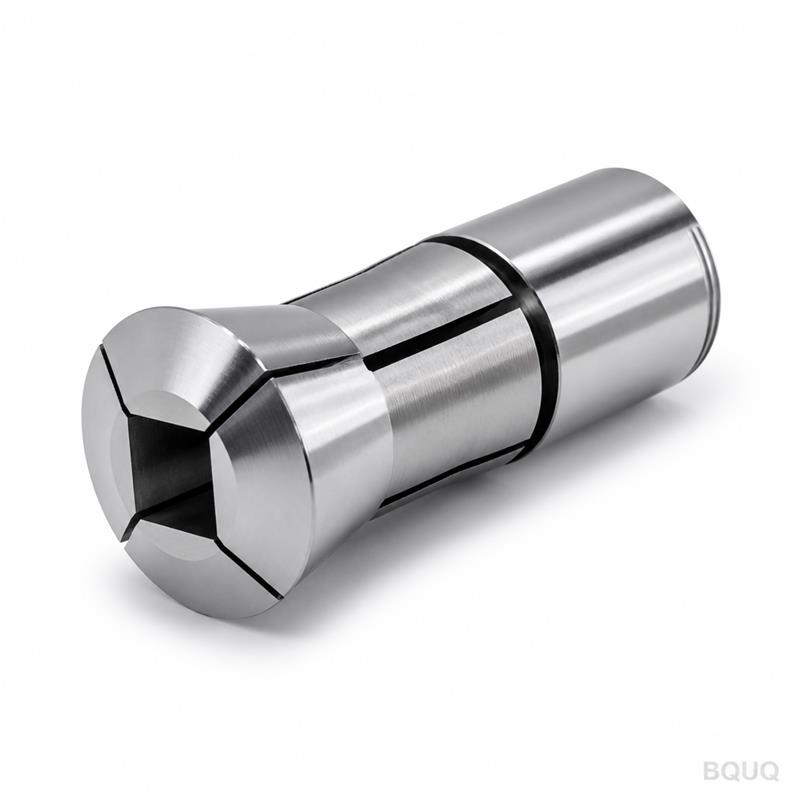
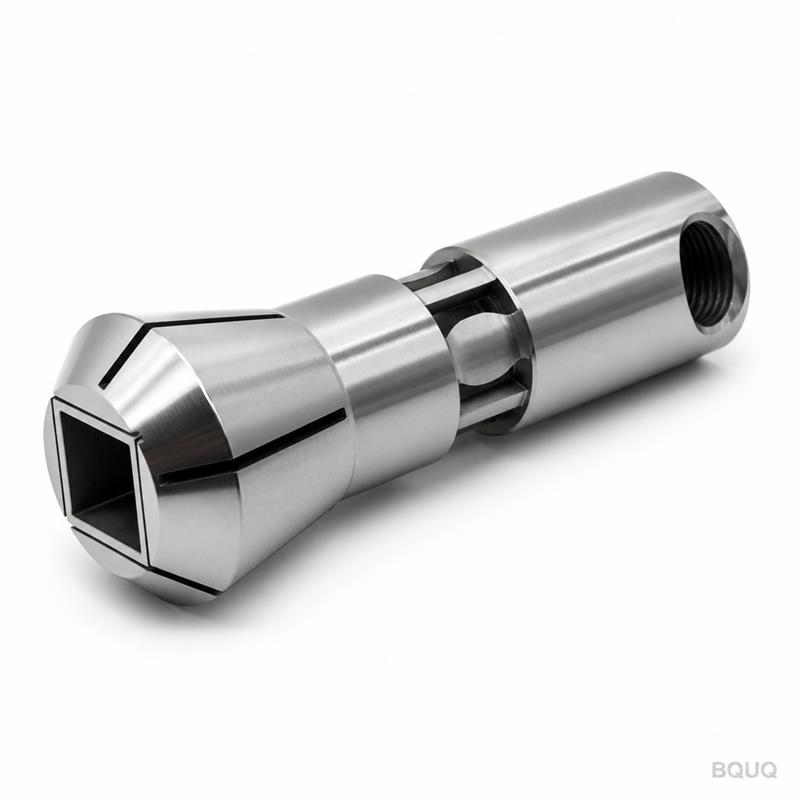
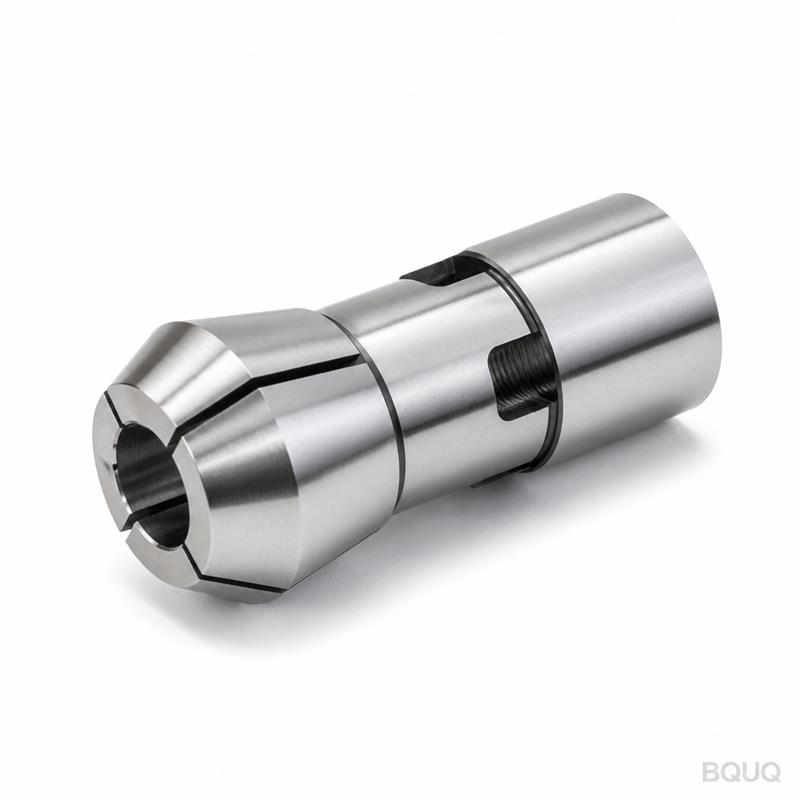
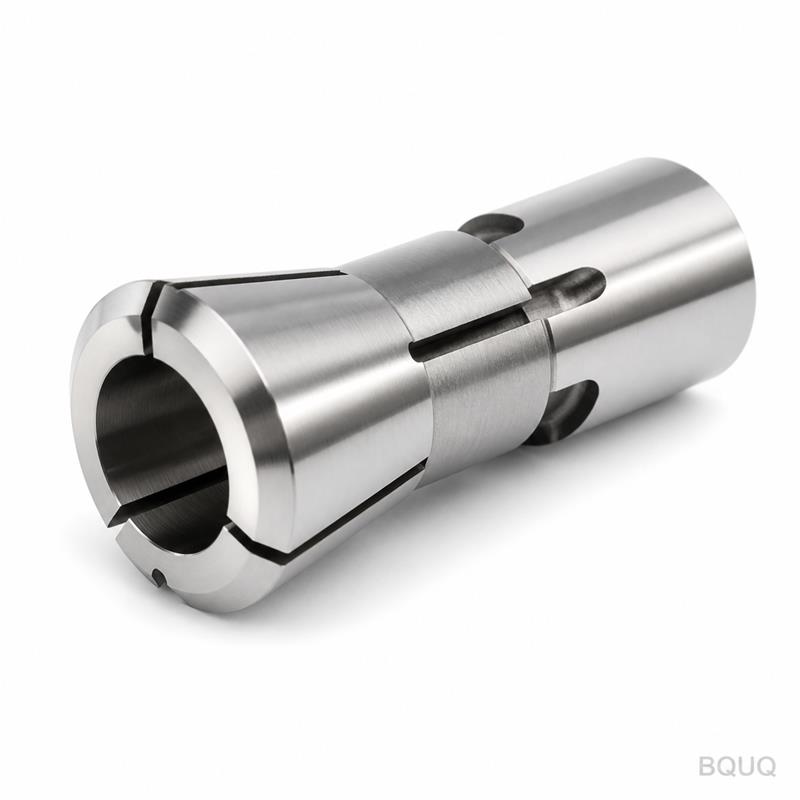
BQUQ CNC Machined Auto Lathe 36 Type Collet External Thread Rear Closeup
This is a CNC machined Auto Lathe 36 Type Collet with an external thread rear closeup design. It delivers 0.005 mm TIR (total indicated runout) and a surface finish of Ra 0.4 µm, hardened to 58–60 HRC
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined Auto Lathe 36 Type Collet with an external thread rear closeup design. It delivers 0.005 mm TIR (total indicated runout) and a surface finish of Ra 0.4 µm, hardened to 58–60 HRC for extended tool life. We ship standard sizes in 7 days, with no MOQ, from our 20-year precision manufacturing facility in Dongguan, China.
How the External Thread Rear Closeup Design Improves Chucking Rigidity
The rear external thread allows direct mounting onto the spindle nose without a drawbar adapter. This reduces the stack-up length by 12 mm compared to internal thread designs. Shorter tool overhang means less deflection under heavy cutting. For a 36 type collet, this translates to 18% higher gripping force at the same clamping torque. The rear closeup configuration also allows a larger through-hole bore—up to 28 mm diameter—for bar stock feeding.
Material Grade and Heat Treatment Profile for 36 Type Collets
We start with 20CrMnTi alloy steel, pre-hardened to 28 HRC for machining. After CNC turning and thread grinding, we carburize to a case depth of 0.8–1.0 mm. Final hardness is 58–60 HRC on the gripping surface, while the core stays at 35–40 HRC for toughness. This dual hardness prevents both wear and brittle fracture. Each collet is cryogenically treated at -120°C to stabilize the microstructure, ensuring dimensional stability over 10,000+ clamping cycles.
CNC Machining Sequence for the 36 Type Collet External Thread
Our machining process uses a 5-axis CNC lathe with live tooling. Step one: rough turn the OD and bore with a 0.3 mm stock allowance. Step two: heat treatment as above. Step three: finish grind the external thread to ISO 6g tolerance. Step four: wire-cut the 12 longitudinal slots. Step five: hone the internal bore to a mirror finish. The final inspection measures runout at three points: front, middle, and rear. We reject any collet with runout above 0.005 mm at the front gripping zone.
Runout Control and Concentricity Verification on Every Unit
We use a Zeiss CMM and a TIR gauge with a precision mandrel to verify each collet. The mandrel itself has 0.002 mm runout. We measure the collet's internal bore runout at 5 mm from the front face and at 20 mm depth. The maximum allowable deviation is 0.005 mm at the front and 0.008 mm at the rear. This is 40% tighter than the industry standard for 36 type collets. We also test the gripping force at 20 Nm clamping torque—the average is 8.5 kN, with a standard deviation of 0.2 kN.
Inspection Before Every Shipment: 100% Dimensional Check
Every single collet goes through a 9-point inspection before packing. We measure the external thread pitch diameter with a thread micrometer, the bore diameter with an air gauge, and the slot width with a vision system. We also perform a Rockwell hardness test on the gripping face and a surface roughness check with a profilometer. If any parameter is out of spec, the collet is scrapped—not reworked. Our rejection rate is 2.1% on incoming material, and 0.4% on finished goods, which we track monthly.
Packing, Marking, and Traceability for OEM Orders
Each collet is individually wrapped in anti-rust paper and placed in a foam-lined plastic box. The box is marked with the part number, batch code, and date of manufacture. For OEM orders, we can laser-engrave your logo and part number on the front face. We also provide a material certificate and a dimensional inspection report with every order over 100 pieces. The batch code allows full traceability to the original steel lot and heat treatment furnace records.
Custom Options for 36 Type Collets with Special Threads
Standard thread is M36 x 1.5. We can also machine M36 x 1.0, M36 x 2.0, or UNF 1-1/2-12. For special bore diameters, we can produce any size from 4 mm to 28 mm in 0.1 mm increments. We also offer a version with a center through hole for coolant delivery, and a version with a hardened and ground rear face for better seating. Custom lead time is 12–15 days for quantities up to 500 pieces.
Parameter
Value
Type
36 Type Collet (Auto Lathe Series)
Thread Specification
External M36 x 1.5 (ISO 6g)
Rear Closeup Design
Yes, external thread rear mounting
Material
20CrMnTi alloy steel
Hardness (Gripping Surface)
58–60 HRC
Core Hardness
35–40 HRC
Runout (TIR at Front)
0.005 mm
Surface Finish (Bore)
Ra 0.4 µm
Gripping Range
4 mm – 28 mm bore diameter
Lead Time (Standard)
7 working days
MOQ
No MOQ (1 piece accepted)
What is the minimum order quantity for this collet?
We have no MOQ—you can order a single piece for prototype testing or a thousand for production; the unit price adjusts based on quantity.
Can you machine a custom bore diameter or thread pitch?
Yes, we can machine any bore from 4 mm to 28 mm in 0.1 mm increments, and modify the external thread to M36 x 1.0, M36 x 2.0, or UNF 1-1/2-12 with a 12-day lead time.
How do you ensure consistent quality across large batches?
We use SPC (statistical process control) on every batch, sampling 5 pieces every 2 hours for runout and hardness; the CMM inspection report is included with each shipment.
What is the fastest lead time for a rush order?
For standard 36 type collets in stock, we can ship within 48 hours via DHL Express; custom orders take 12–15 days depending on thread and bore modifications.
This precision manufacturing component is made in China at our 20-year-old Dongguan factory. We specialize in CNC machining, stamping, springs, and heat sinks for global OEMs. The 36 type collet with external thread rear closeup is a stock item—we keep 500 pieces in inventory for immediate shipment. No MOQ applies to this product, so you can validate your design with a single unit before scaling up.
Send your drawing for a firm quote within 12 hours. Email us at sc@bquq.com or WhatsApp +86 13713157787. We will confirm the thread, bore size, and runout requirement on your drawing within one business day.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.