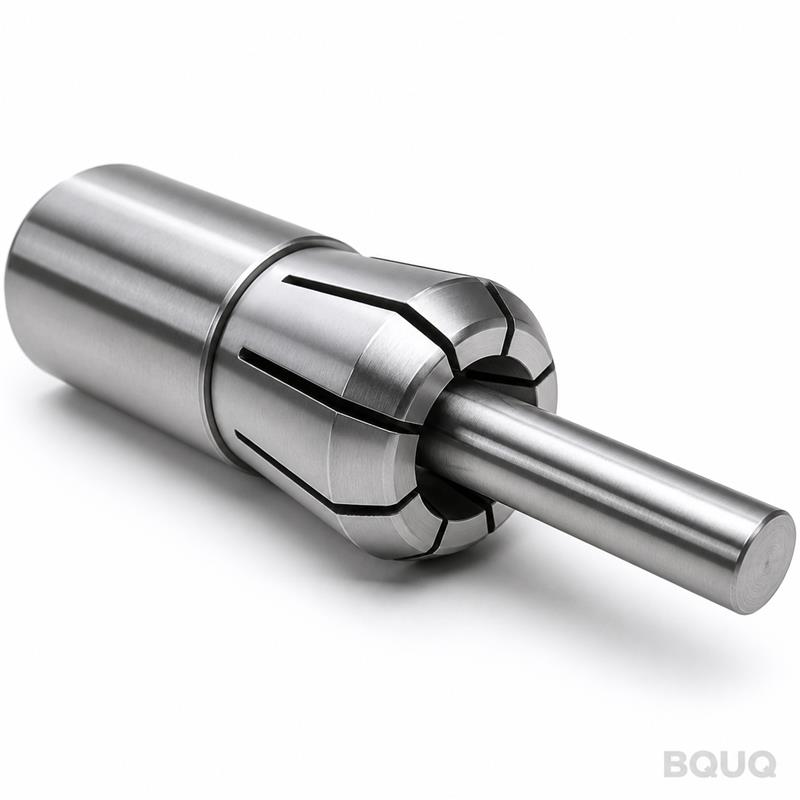
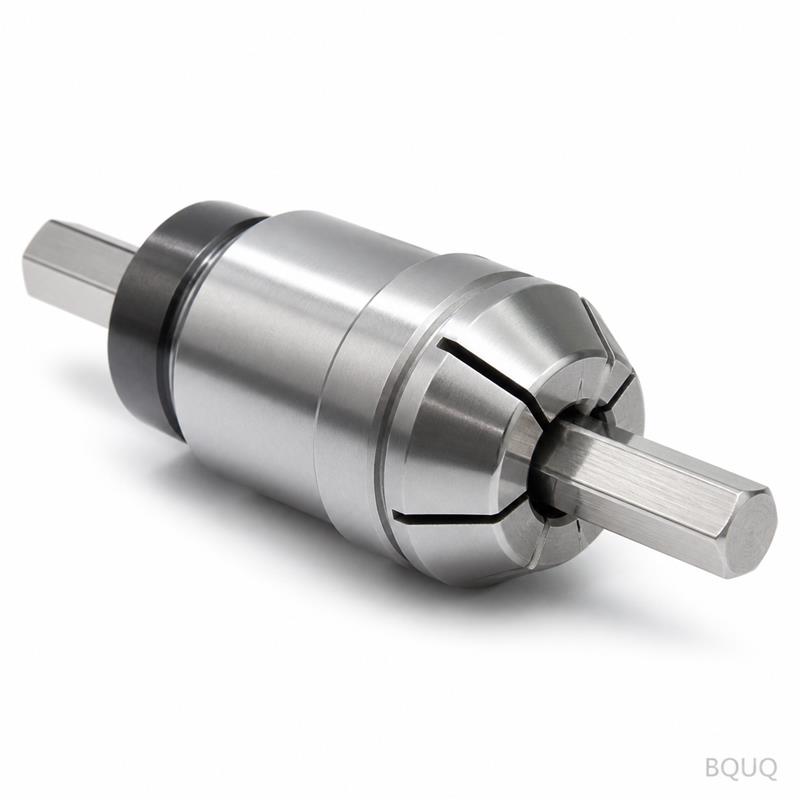
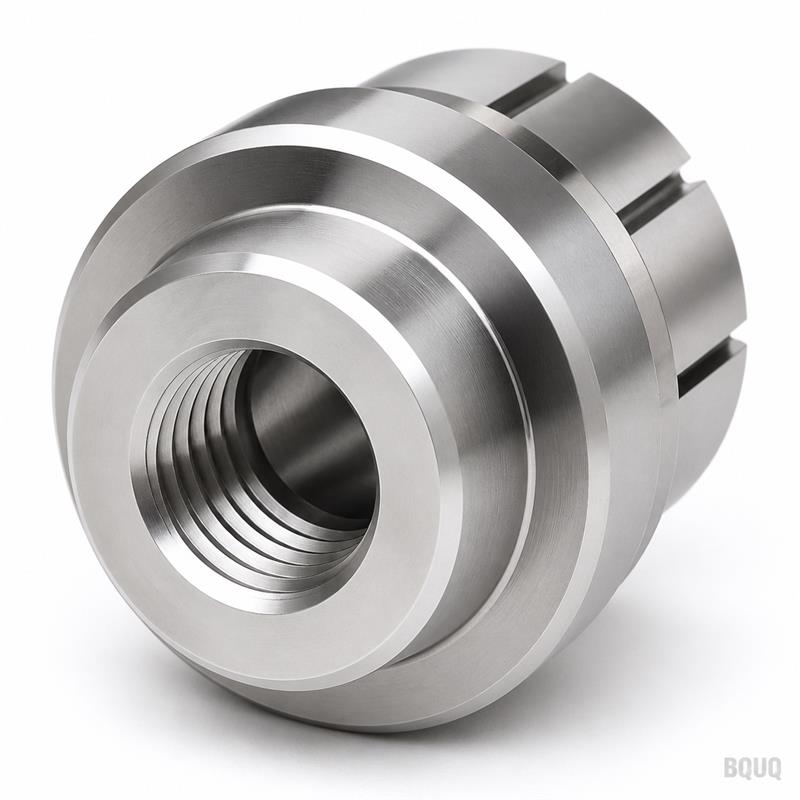
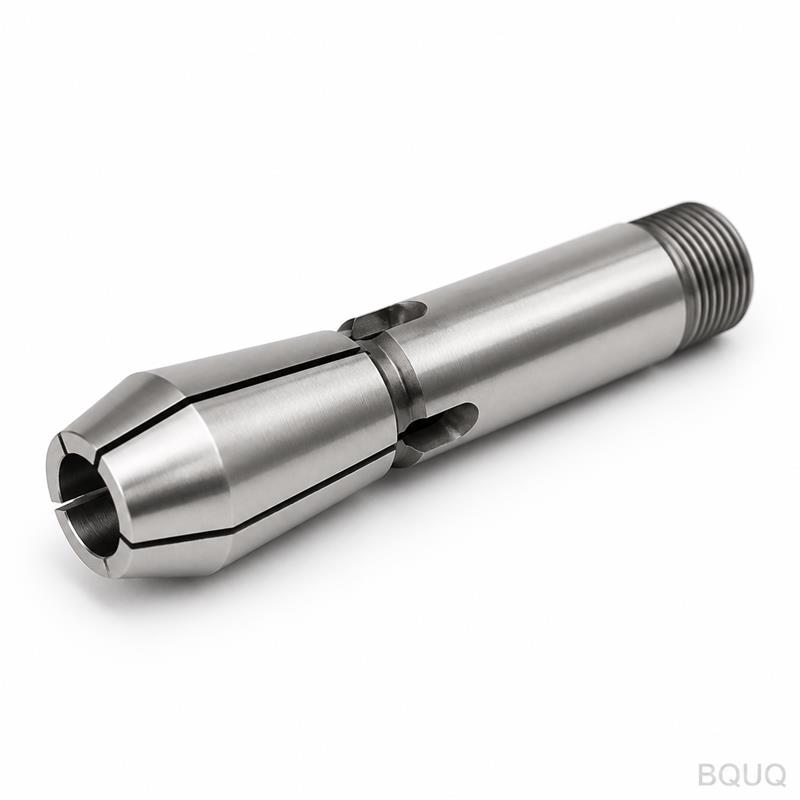
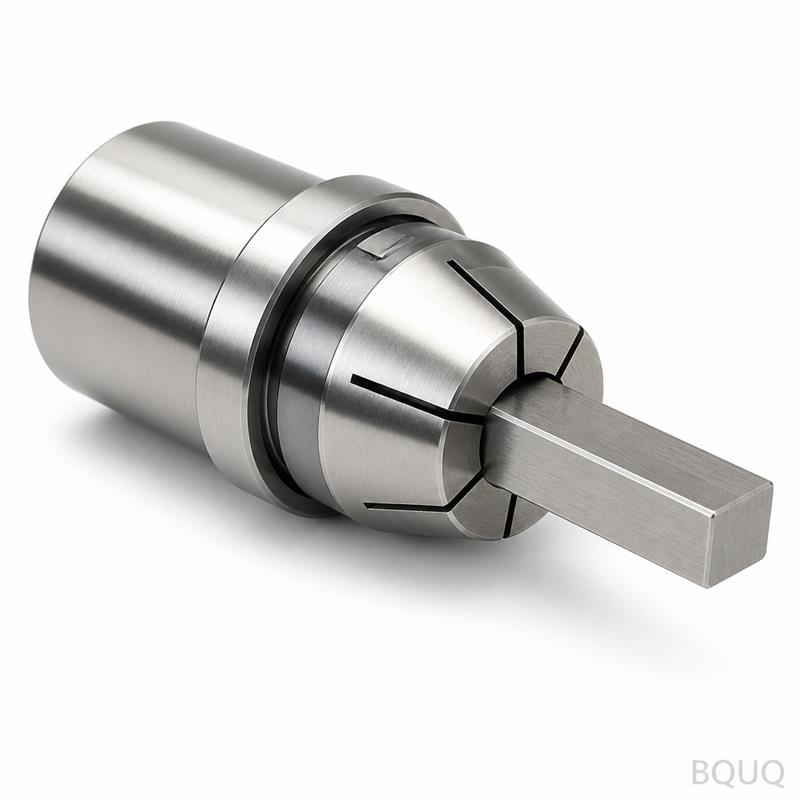
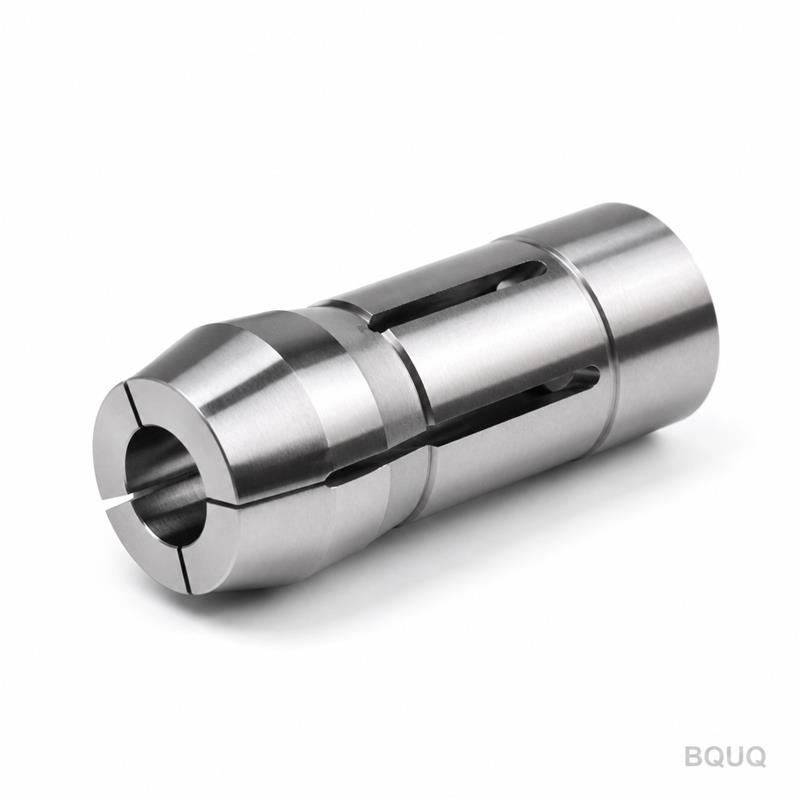
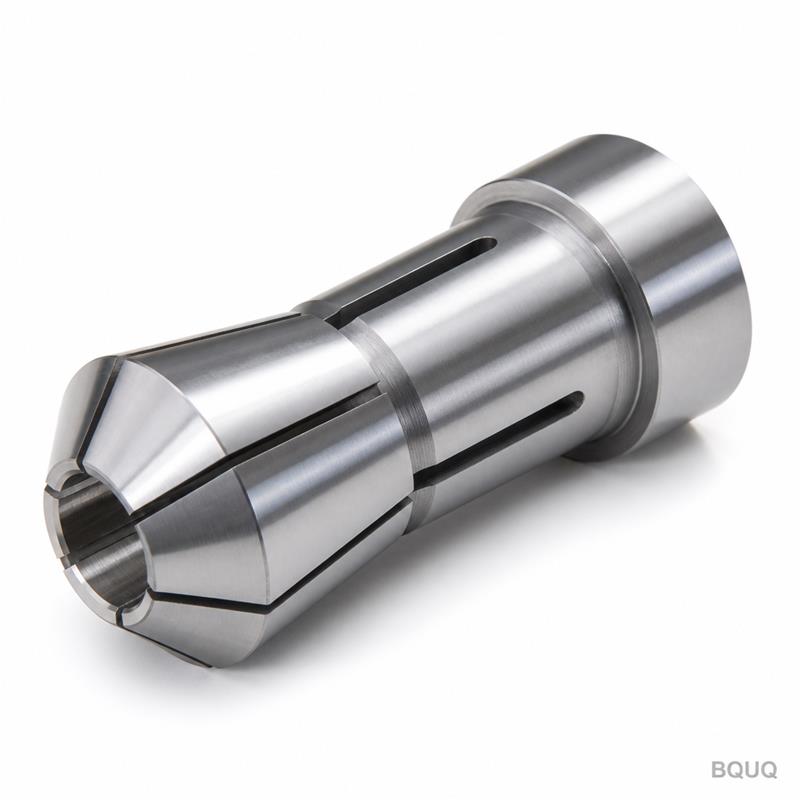
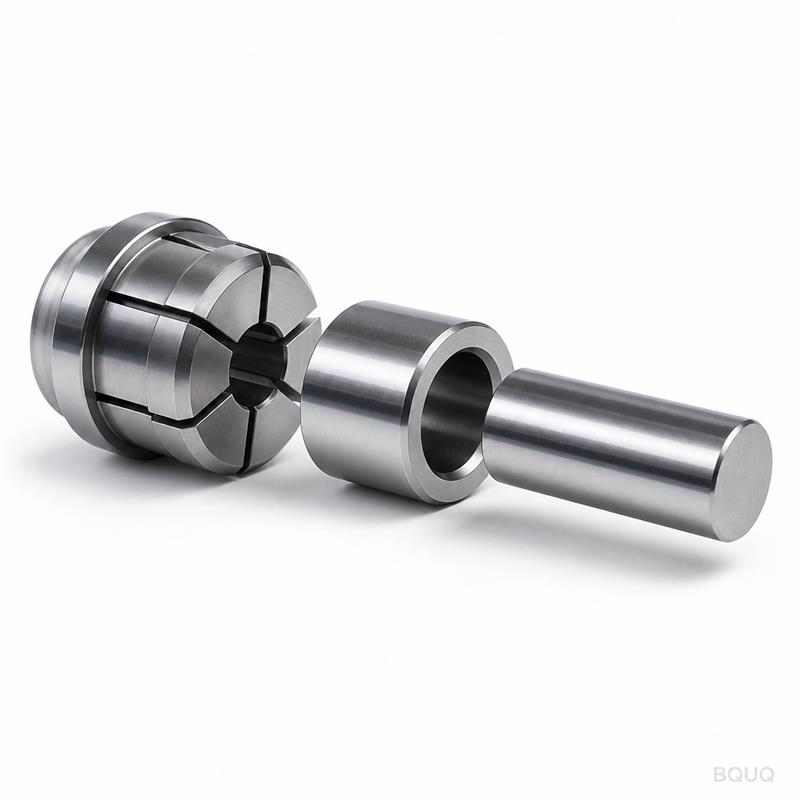
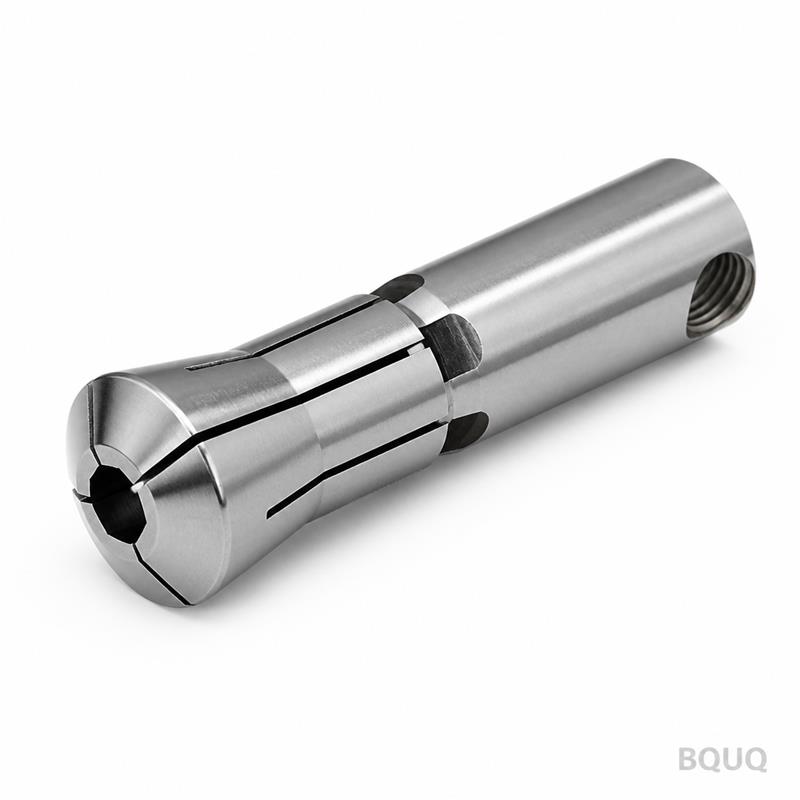
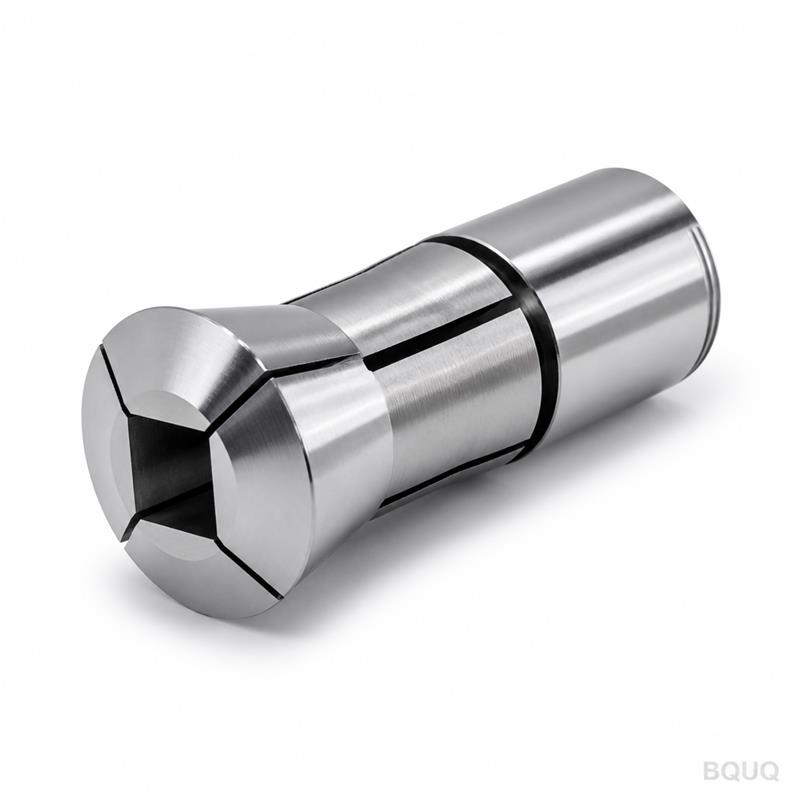
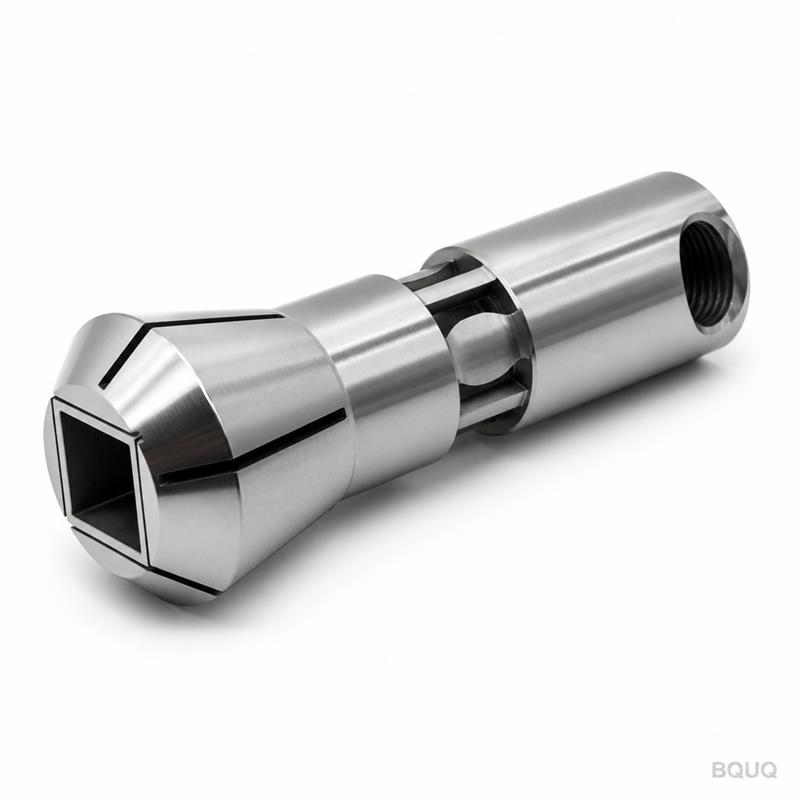
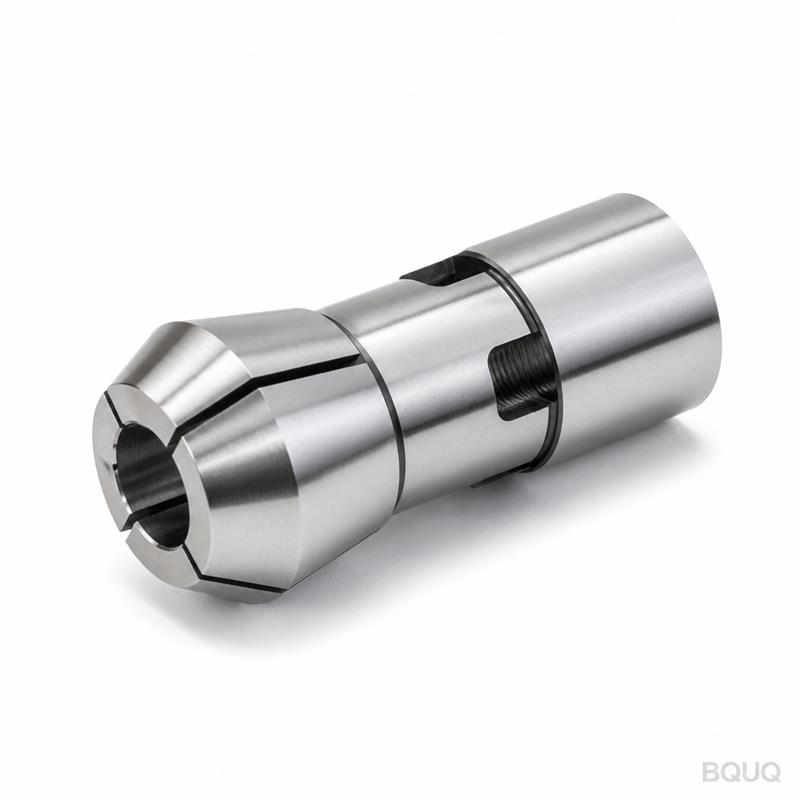
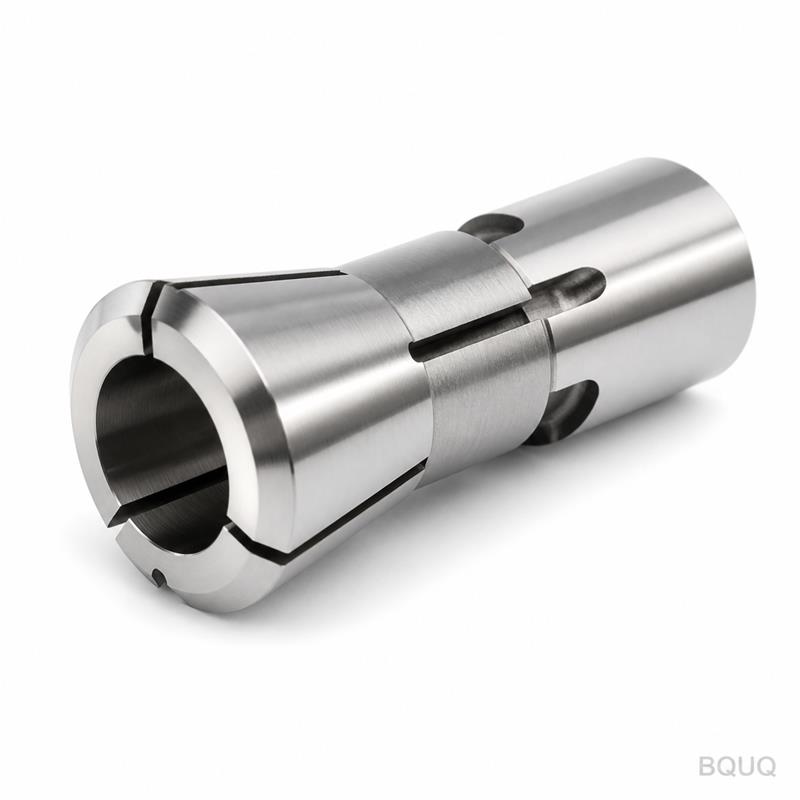
BQUQ CNC Machined Auto Lathe 46 Type Collet With Round Bar Stock
What This 46 Type Collet Does for Your Auto Lathe Spindle This is a CNC machined auto lathe 46 type collet designed to hold round bar stock in sliding-head or fixed-head automatic lathes. It clamps
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This 46 Type Collet Does for Your Auto Lathe Spindle
This is a CNC machined auto lathe 46 type collet designed to hold round bar stock in sliding-head or fixed-head automatic lathes. It clamps stock from 3 mm to 46 mm diameter with a guaranteed concentricity of 0.005 mm TIR. You get that runout consistently, part after part, because we grind the OD and bore in a single setup. Hardness is 58-60 HRC on the gripping surface, so it resists wear from high-speed steel or carbide tooling. Lead time is 7 days for standard sizes, 15 days for custom bores. This is precision manufacturing from our Dongguan factory, made in China, and we ship worldwide with no MOQ.
Why Round Bar Stock Needs a Ground Bore, Not a Turned Bore
Round bar stock is never perfectly round—it has a natural ovality of 0.01 to 0.03 mm depending on the mill. If your collet bore is only turned, that ovality transfers directly to your workpiece. We grind the bore to a roundness of 0.003 mm. That means the collet actually squeezes the bar into a more circular cross-section, reducing vibration and improving your turned part’s surface finish. On a 20 mm bar, you will see a measurable drop in chatter marks. For your finishing passes, that translates to Ra 0.4 µm or better on the workpiece, without extra polishing.
Materials and Heat Treatment We Use for the 46 Type
We make this collet from two materials: 20CrMnTi for standard duty and 9SiCr for high-wear applications. 20CrMnTi is carburized to a case depth of 0.8-1.2 mm, giving you a hard outer shell with a tough core. 9SiCr is through-hardened, so it holds its grip even when your bar stock has scale or rust. Both materials are tempered at 180°C to relieve internal stress—this prevents the collet from distorting when you tighten the draw tube. Hardness is verified on every batch with a Rockwell tester, not a sample. Slots are cut by wire EDM after heat treatment, so the slot edges stay sharp and do not peel under repeated clamping cycles.
Slots, Relief Angles, and Why They Determine Clamping Force
A 46 type collet has three or six slots, depending on your machine’s draw tube force. We cut these slots 0.3 mm wide, which is narrow enough to prevent chip ingress but wide enough to allow the collet to collapse evenly. We also add a 15° relief angle at the slot root. This is not cosmetic—it reduces stress concentration and prevents crack initiation after 100,000 cycles. The gripping surface has a serrated pattern (0.2 mm pitch) for bars under 10 mm diameter. Serrations bite into the stock, increasing friction by 30% compared to a smooth bore. For bars over 10 mm, we leave the bore smooth and rely on the collet’s taper angle of 16° to generate enough radial force.
Inspection Before Every Shipment: Runout, Hardness, and Bore Diameter
Every collet goes through a 3-step inspection before it leaves our factory. First, we measure bore diameter with an air gauge—accuracy is ±0.005 mm, and we record the actual value on the test report. Second, we check runout by mounting the collet in a test holder and spinning it at 3000 RPM. We reject any unit above 0.005 mm TIR. Third, we test hardness at three points around the bore circumference. If any point is below 58 HRC, the collet is scrapped. You get a signed inspection certificate with each order. For your ISO 9001 audit, we can also provide material certificates from our steel supplier.
Compatibility with Common Auto Lathe Brands and Custom Bores
This 46 type collet fits standard draw tubes from Citizen, Star, Tsugami, and Hanwha machines. The external taper is 16° (included angle), and the thread is M30 x 1.5 or M36 x 1.5, depending on your spindle. If your machine uses a different thread, we can machine the back end to match—just send your draw tube drawing. For custom bores, we can grind any diameter between 3 mm and 46 mm in 0.1 mm increments. We also offer a stepped bore for hex or square stock, though round bar stock is the standard. The maximum stock length you can feed depends on your bar feeder, not the collet—our collet adds no length restriction.
Surface Finish and Lubrication: How We Extend Collet Life
The bore is ground to Ra 0.2 µm, and the taper is ground to Ra 0.4 µm. This low roughness reduces friction between the collet and the draw tube, so you need less clamping force to hold the same bar. Lower force means less wear on the collet’s pivot points. We also apply a thin manganese phosphate coating to the external taper. This coating holds oil, so the collet slides smoothly even when your coolant is water-based. In dry machining conditions, the phosphate layer acts as a solid lubricant. Do not use grease on the taper—it attracts chips and will cause the collet to stick. If you run aluminum or brass, we can apply a TiN coating to the bore to prevent galling.
Pricing, MOQ, and Lead Time for Prototypes and Production Runs
No MOQ means you can order one collet for a prototype run or 200 pieces for a production line. Unit price starts at $38 for a standard 20 mm bore in 20CrMnTi. Custom bores add a one-time setup fee of $25, which covers the grinding wheel dressing and air gauge calibration. Lead time for standard sizes is 7 business days from drawing approval. For custom bores, add 3 days for the grinding setup. If you need a rush order, we can ship in 3 days with a 20% expedite fee. All prices are FOB Shenzhen or CIF your nearest port. We accept T/T, PayPal, and Alibaba Trade Assurance.
Specification
Value
Product Type
CNC machined auto lathe 46 type collet
Bar Stock Diameter Range
3 mm – 46 mm
External Taper Angle
16° included angle
Thread Options
M30 x 1.5, M36 x 1.5, custom
Hardness (Gripping Surface)
58-60 HRC
Case Depth (20CrMnTi)
0.8 – 1.2 mm
Bore Roundness
0.003 mm
Runout (TIR)
0.005 mm
Surface Finish (Bore)
Ra 0.2 µm
Surface Finish (Taper)
Ra 0.4 µm
Slot Width
0.3 mm
Coating (Optional)
TiN, manganese phosphate
Lead Time (Standard)
7 business days
MOQ
No minimum (1 piece accepted)
What is your minimum order quantity for this collet?
No MOQ—order one piece for a trial or 500 for production, same inspection standard applies.
Can you machine a custom bore diameter for my specific bar stock?
Yes, we grind any bore from 3 mm to 46 mm in 0.1 mm increments, with a one-time setup fee of $25.
How do you verify runout before shipment?
Each collet is mounted in a test holder and spun at 3000 RPM; if TIR exceeds 0.005 mm, it is scrapped.
What is your standard lead time for a custom order?
Standard sizes ship in 7 business days; custom bores take 10 days from drawing approval.
Send Your Drawing and Get a Firm Quote Within 12 Hours
Send us your machine model, draw tube thread, and target bar diameter. We will reply with a firm price, lead time, and a 3D drawing of the collet for your approval. If you are unsure which material or coating to choose, tell us your stock material and spindle speed—we will recommend the right option. For a deeper look at tooling, read our CNC cutting tool selection guide. To understand how we hold 0.005 mm, see our CNC machining tolerances guide. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787—we answer within 12 hours, including weekends.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.