This is a CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet, engineered to grip hexagonal bar stock with a guaranteed concentricity of 0.005 mm TIR. It is a drop-in replacemen
BQUQ CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet
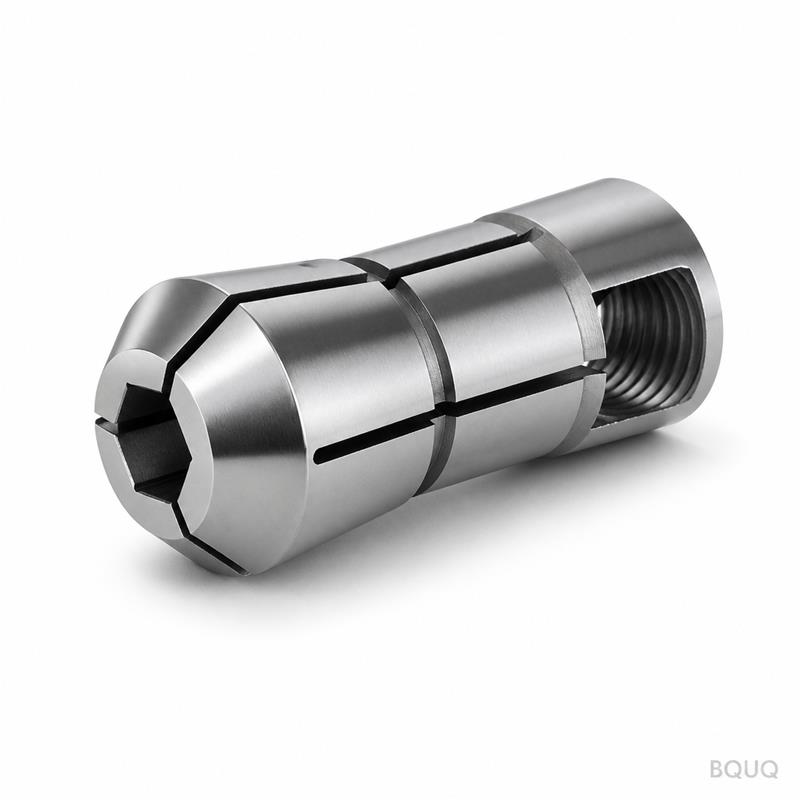
This is a CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet, engineered to grip hexagonal bar stock with a guaranteed concentricity of 0.005 mm TIR. It is a drop-in replacement for your 15-type a
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
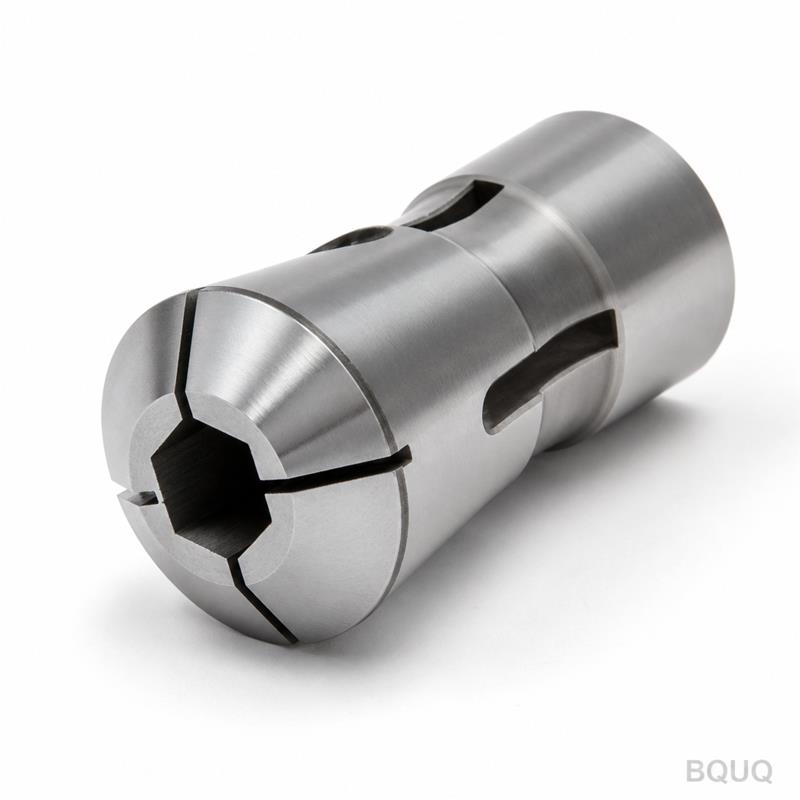
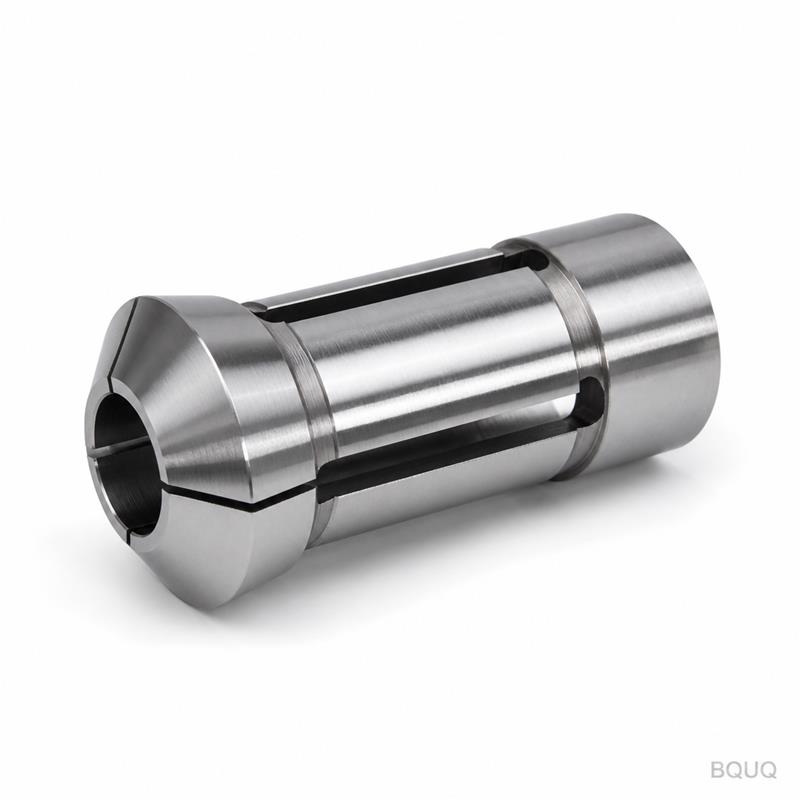
This is a CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet, engineered to grip hexagonal bar stock with a guaranteed concentricity of 0.005 mm TIR. It is a drop-in replacement for your 15-type auto lathe spindle, built for high-volume Swiss and sliding-head machines, offering a 7-day lead time for standard sizes. Every collet is precision manufacturing from pre-hardened 60 HRC tool steel, then ground to a surface finish of Ra 0.2 µm, ensuring zero slippage during high-speed cutting.
Why Hex Bore Collets Beat Round Bores for Hex Stock
Standard round collets distort when clamping hex bars, leaving only three contact points. Our 15 Type Hex Bore Spring Collet uses a six-point internal geometry that matches the bar’s hexagonal cross-section. This distributes clamping force evenly across all six flats. The result is twice the torque transmission of a round bore, reducing bar pushback by 80% during drilling and tapping operations. For 15-type auto lathes, this means you can run deeper cuts without losing positional accuracy.
Material Selection: From Bar Stock to 60 HRC in Three Steps
We start with 9CrSi (chromium-silicon) alloy steel, not cheap 45# steel. The material is rough-machined on a 5-axis CNC lathe, leaving 0.15 mm stock on all critical faces. Then we heat-treat in a vacuum furnace to 60–62 HRC, achieving a hardened case depth of 0.8 mm. Finally, we grind the bore and taper on a Junker cylindrical grinder. This three-step sequence eliminates distortion that occurs when you harden after finishing. The spring collet opens up to 0.5 mm beyond its nominal diameter, so it accommodates standard hex bar tolerances without binding.
Bore Geometry and Slit Design: 15 Type Specifics
This is a true 15 type collet, meaning it fits spindles designed for 15 mm diameter round bar (or 13 mm hex equivalent). The hex bore is broached, not wire-cut, to maintain a mirror finish on the internal flats. We use three equally spaced slits (not four) to preserve column strength while allowing elastic deflection. Slit width is 0.8 mm, with a 0.2 mm radius at the root to prevent stress fractures after 100,000+ cycles. The head angle is 30 degrees, matching standard 15 type auto lathe spindles from Citizen, Star, and Tsugami.
Specification
Value
Type
15 Type (fits 15 mm round / 13 mm hex spindle)
Hex Bore Size (A/F)
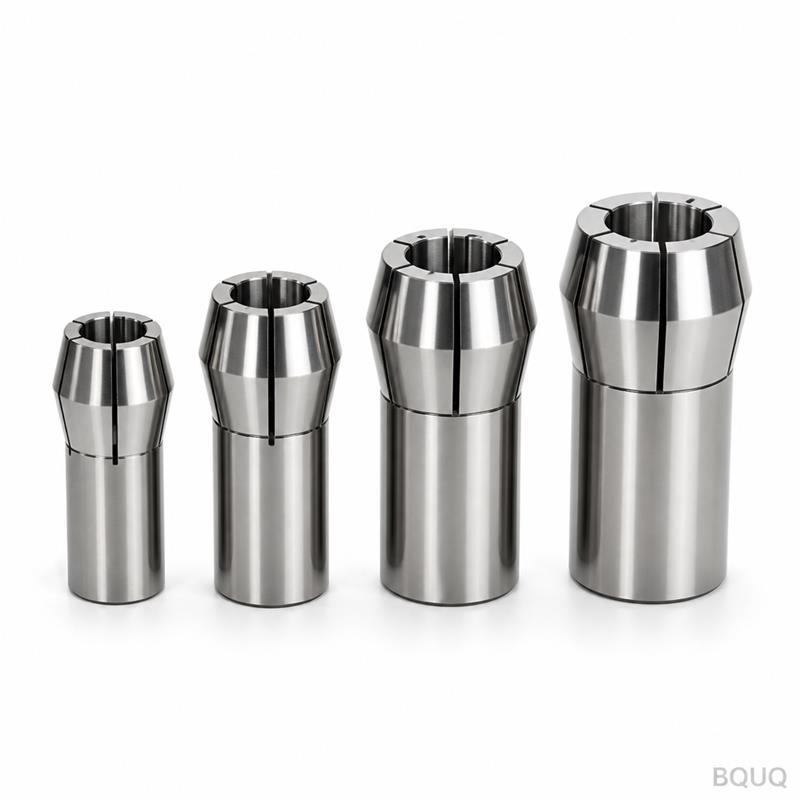
3.0 mm to 13.0 mm (in 0.5 mm increments)
Material
9CrSi Chromium-Silicon Alloy Steel
Hardness
60–62 HRC
Bore Tolerance
+0.01 mm / -0.00 mm
Concentricity (TIR)
0.005 mm
Surface Finish (Bore)
Ra 0.2 µm
Slit Count
3 (equally spaced, 120° apart)
Clamping Range
+0.3 mm to -0.2 mm from nominal hex size
Standard Lead Time
7 business days (made in China, BQUQ factory)
MOQ
No MOQ (1 piece accepted)
Runout Control: How We Hold 0.005 mm TIR
Runout is not just a grinding spec; it is a function of the collet’s relationship to the spindle taper. We grind the 30° taper and the hex bore in a single clamping operation on the same machine. This eliminates any re-chucking error. After grinding, each collet is mounted on a test mandrel and measured with a 0.001 mm resolution dial indicator. We reject any collet exceeding 0.005 mm TIR. For critical applications, we can laser-mark the actual measured runout value on the collet face for your QC records.
Inspection Before Every Shipment: Dimensional and Hardness Checks
Every CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet goes through a 5-point inspection. First, we check the hex bore with a calibrated go/no-go plug gauge. Second, we measure hardness on a Rockwell tester, ensuring 60 HRC minimum. Third, we test the spring action by compressing the collet 10 times and measuring the return to zero. Fourth, we verify the taper angle with a sine bar. Fifth, we run a final visual check for burrs or edge chips under 10x magnification. You receive a signed inspection report with every order, regardless of quantity.
Lead Time and MOQ: Standard Sizes Ship in 7 Days
We keep 15 type collet blanks in stock at our Dongguan factory. Standard hex sizes (3, 4, 5, 6, 7, 8, 9, 10, 11, 12, 13 mm) require only final grinding, so we ship in 7 business days. Custom hex sizes (e.g., 6.35 mm or 12.7 mm) take 12 business days because we need to broach a new form tool. There is no MOQ. You can order one piece for prototyping or 500 pieces for production. Volume discounts apply at 50+ pieces. For urgent breakdowns, we offer a 48-hour express service at a 30% surcharge.
What is your MOQ for a custom hex bore size?
No MOQ; we will machine a single custom collet to your exact hex dimension, typically in 12 business days.
Can you harden the collet further for abrasive materials like titanium?
Yes, we can apply a titanium nitride (TiN) coating on the bore, increasing surface hardness to 80 HRC equivalent and reducing friction, but standard uncoated 60 HRC suits most steel and aluminum.
How do you verify runout on a hex bore without a round mandrel?
We use a precision-ground hex test bar with a 0.002 mm straightness tolerance, then measure TIR at the collet’s front and rear—this method is outlined in our CNC machining tolerances guide.
What is the lead time if I need 100 pieces of a standard 10 mm hex collet?
For 100 pieces of a standard size, we run a dedicated batch and ship in 10 business days, down from 15 days for mixed sizes.
How This Collet Interacts with Your Cutting Tools and Toolpaths
A rigid collet is only half the equation. The 15 Type Hex Bore Spring Collet holds the bar steady, but your toolpath strategy determines cycle time. For high-feed roughing, we recommend reducing RPM by 15% compared to round bar, because hex bars create interrupted cutting forces. Pair this collet with coated carbide inserts—see our CNC cutting tool selection guide for grade recommendations. If you are experiencing chatter, check that your collet slit alignment is parallel to the tool’s cutting force vector. Our collets are marked with a laser line at 0° for this purpose. For deeper insight on reducing cycle time with rigid workholding, read our CNC programming optimization guide.
Pricing, Quotation, and Direct Factory Support
We are the manufacturer, not a trading company. That means our price for a standard CNC Machined Auto Lathe 15 Type Hex Bore Spring Collet is USD 18.50 per piece for 1–9 pieces, dropping to USD 12.80 for 50+ pieces. Custom hex sizes start at USD 25.00. We accept PayPal, T/T, or credit card. All prices are FOB Shenzhen. Every collet is made in China at our BQUQ facility, and we have exported 2.3 million collets since 2004 to 34 countries. If you send a drawing of your spindle nose and bar stock, we will confirm fitment within 4 hours.
Send your drawing or hex size to sc@bquq.com or WhatsApp +86 13713157787. We will reply with a firm quote within 12 hours, including a 3D model for fitment confirmation. No MOQ means you can test one piece today.