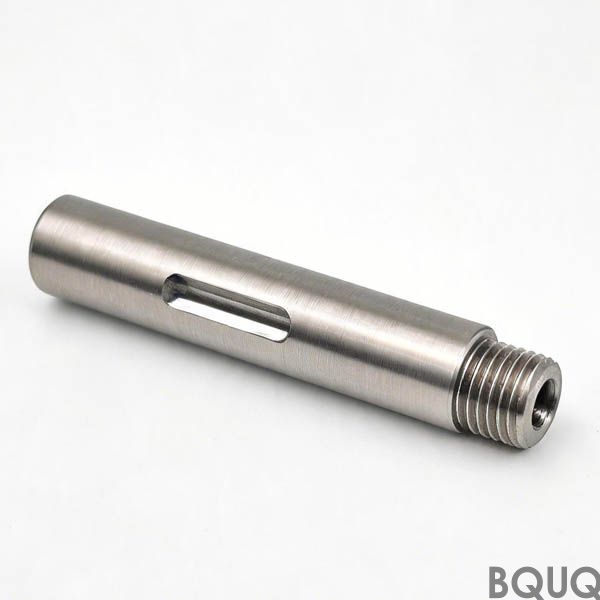
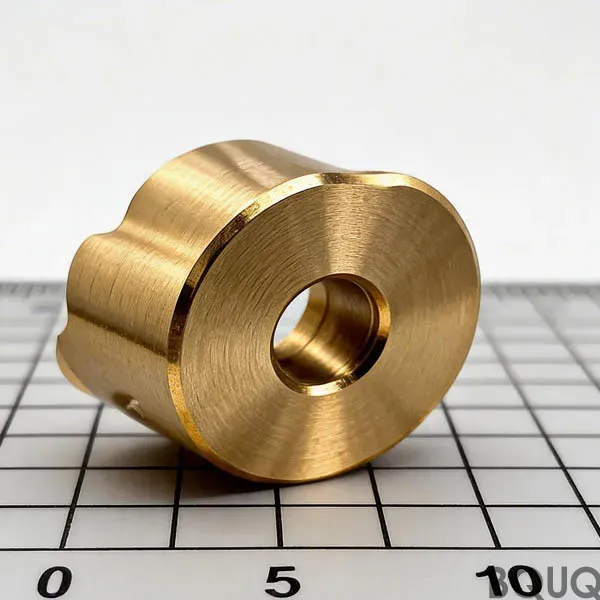
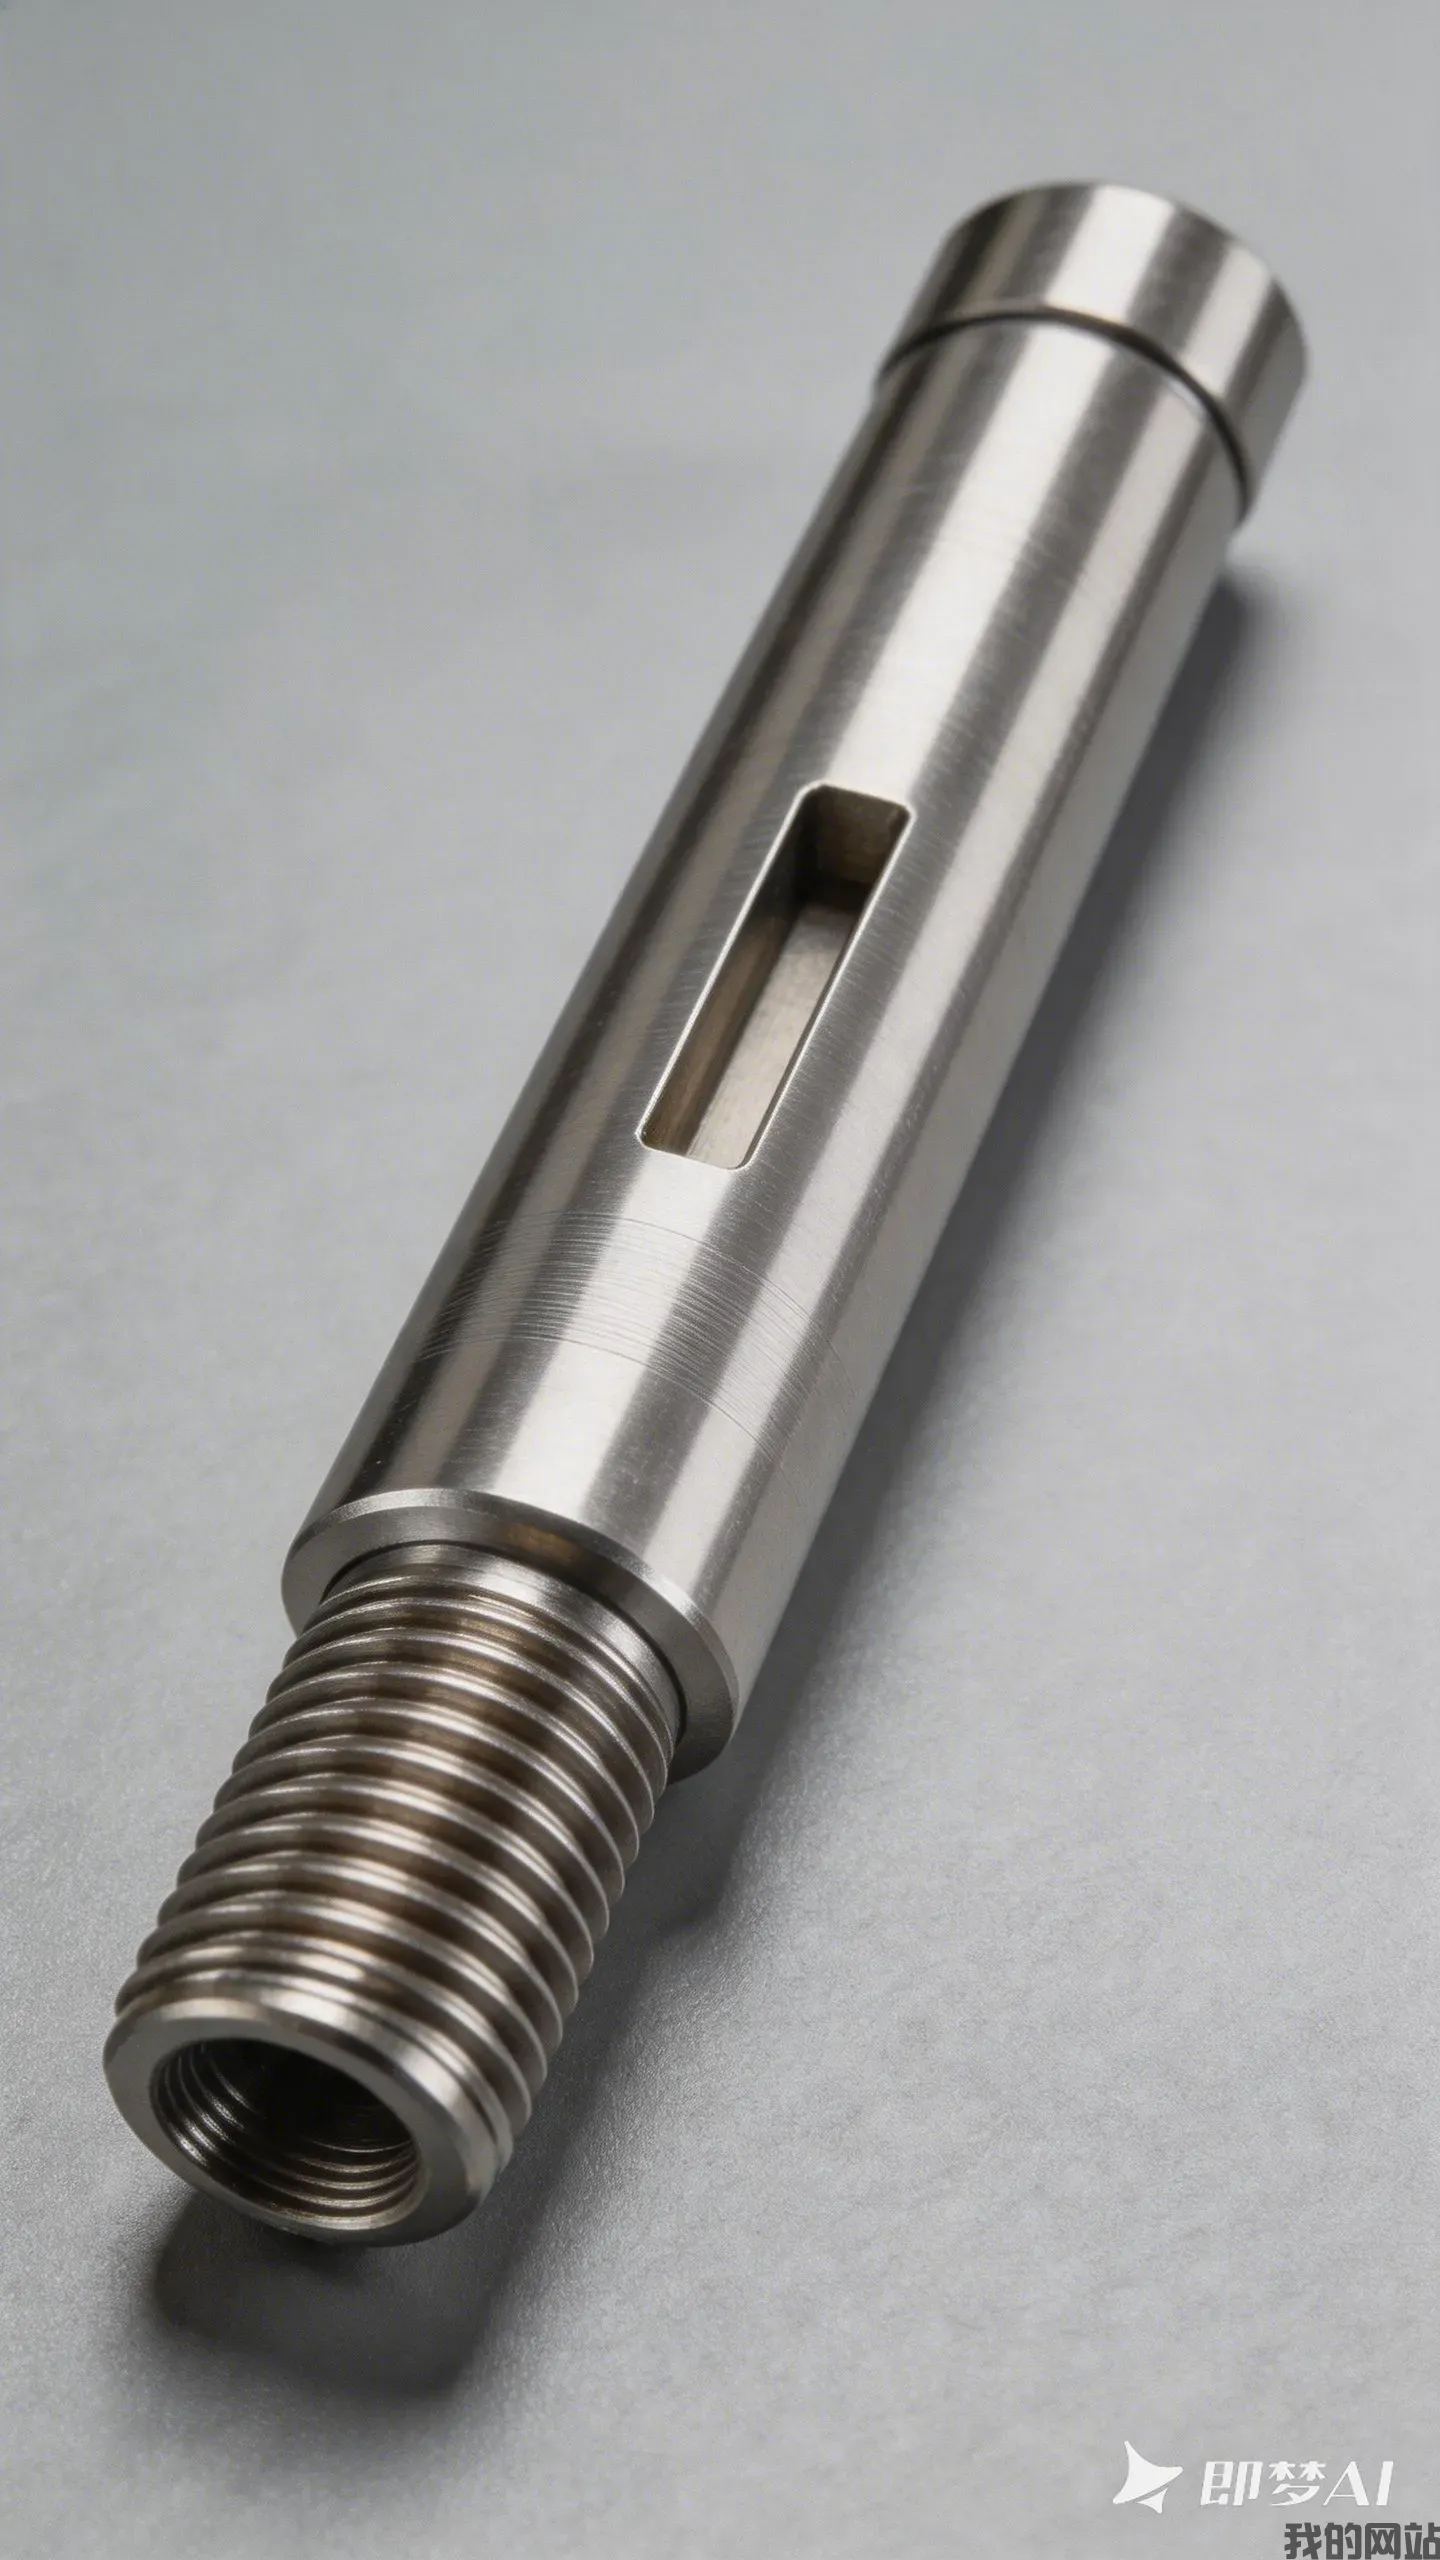
鏁版帶鍔犲伐缂栫鎶€鏈: Steel 4140 / 4340, tolerance 0.005 mm, surface hard chrome plate 0.025 mm, lead time 15 working days, MOQ 500 pcs. Capacity for automotive. Drawing review and first-article report included.
CNC machining programming technology
Key Takeaway
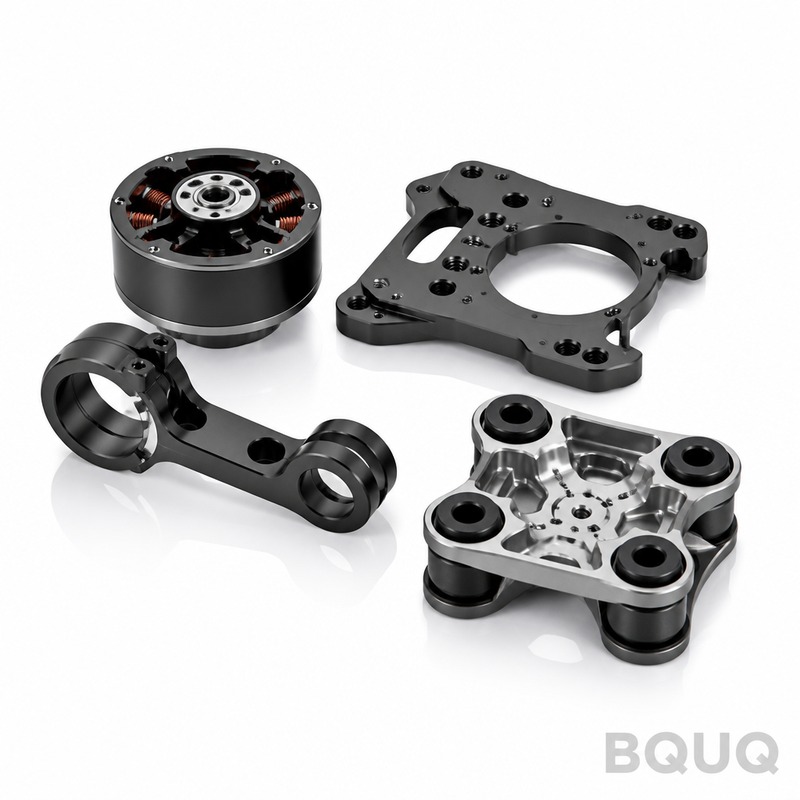
CNC machining programming technology defines the process window before the machine: material condition and tooling geometry are fixed first, then capability is proven at production speed. For robotics parts in 4140/4340 steel, the envelope reaches 400 x 300 x 200 mm, tolerances hold ±0.002 mm on request, bore finish reaches Ra 0.4, and production lead time is 10 working days.
Key Takeaway
CNC machining programming technology defines the process window before the machine: material condition and tooling geometry are fixed first, then capability is proven at production speed. For robotics parts in 4140/4340 steel, the envelope reaches 400 x 300 x 200 mm, tolerances hold ±0.002 mm on request, bore finish reaches Ra 0.4, and production lead time is 10 working days.
Most buyers start with a drawing and a target price. We start with 鏁版帶鍔犲伐缂栫▼鎶€鏈 and ask what the part actually has to survive: load cycling, thermal swing, or a corrosive environment in robotics.
Related reading: Essential Stamping Die Maintenance Tips for Long Life.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | Steel 4140 / 4340 |
| tolerance_standard | ±0.002 mm on request |
| Surface finish | Ra 0.4 on bore, Ra 0.8 external |
| roughness_ra | Ra 0.2 |
| Size range | 400 x 300 x 200 mm envelope |
| Lead time (production) | 10 working days |
Market and Technical Context
Consolidation among robotics buyers means fewer, larger programs. That rewards suppliers who can document process capability at rather than those who win on a single sample.
See also: BQUQ China Dongguan Stamping Manufacturer Supplier Shrapnel Parts.
Tariff and logistics uncertainty has made regional qualification a priority in robotics. Buyers increasingly ask for a second qualified source, which changes how 鏁版帶鍔犲伐缂栫▼鎶€鏈 is specified and how tolerances are documented.
How We Manufacture It
The route for 鏁版帶鍔犲伐缂栫▼鎶€鏈 starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.002 mm on request is held at production speed rather than on a single slow part.
In production, 鏁版帶鍔犲伐缂栫▼鎶€鏈 runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.002 mm on request.
Learn more about Custom CNC Collet Chuck TG100 Precision Tool Holder Made in China.
Final inspection for 鏁版帶鍔犲伐缂栫▼鎶€鏈 is sampling-based for general dimensions and 100% for critical features. The split is agreed before tooling, because moving a feature from general to critical changes cost and 10 working days.
Material and Surface Finish
Surface specification for 鏁版帶鍔犲伐缂栫▼鎶€鏈 is Ra 0.4 on bore, Ra 0.8 external, chosen for the service environment in robotics. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Where 鏁版帶鍔犲伐缂栫▼鎶€鏈 sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Recycled content and RoHS/REACH declarations are available for 鏁版帶鍔犲伐缂栫▼鎶€鏈 on request. If your robotics customer audits material origin, ask for the mill certificate at quote stage, not at delivery.
Tolerance and Inspection
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so 鏁版帶鍔犲伐缂栫▼鎶€鏈 drawings state how each critical dimension is verified.
Traceability is kept by heat lot and production date. If a field issue ever appears with 鏁版帶鍔犲伐缂栫▼鎶€鏈, we can identify which batch, which tooling set, and which inspection record applies.
Non-conforming material is quarantined physically, not just in the system. For 鏁版帶鍔犲伐缂栫▼鎶€鏈, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
Service environment drives more redesigns than load does. 鏁版帶鍔犲伐缂栫▼鎶€鏈 in outdoor or washdown service needs Ra 0.4 on bore, Ra 0.8 external and sealing considered at design stage, not added later.
Maintenance access matters. Where 鏁版帶鍔犲伐缂栫▼鎶€鏈 is a wear item, we recommend specifying it as a spare with its own part number so reorder does not require a full drawing review.
Further technical detail: CNC Machined Jewelry Clasps Hooks.
What to Confirm Before Ordering
Define critical features at quote stage. Moving a feature from general ±0.002 mm on request to critical after tooling adds cost and extends 10 working days, which is the most avoidable delay in custom sourcing.
Compare quotes on the same basis: material grade, Ra 0.4 on bore, Ra 0.8 external, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
FAQ: Your Questions Before Ordering
What is the minimum order quantity for 鏁版帶鍔犲伐缂栫▼鎶€鏈?
General dimensions are held to ±0.002 mm on request. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
How long does production take for 鏁版帶鍔犲伐缂栫▼鎶€鏈?
Standard lead time for 鏁版帶鍔犲伐缂栫▼鎶€鏈 is 10 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Can you work from our existing drawing?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.002 mm on request would require an extra operation, so you can decide before tooling.
Do you provide material and inspection certificates?
Ra 0.4 on bore, Ra 0.8 external is standard for 鏁版帶鍔犲伐缂栫▼鎶€鏈. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
What surface finishes are available for 鏁版帶鍔犲伐缂栫▼鎶€鏈?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of 鏁版帶鍔犲伐缂栫▼鎶€鏈 remains usable.
Send the drawing and the annual volume. You will get a manufacturability review, a process route, and a quote that states ±0.002 mm on request, 10 working days, and 1000 pcs explicitly rather than by implication.
Recommended reading: What Are the Thermal Effects of Anodizing and Coating on Heat Sinks?.
Compare it with How Is Robotics Industry Growth Driving Precision Manufacturing Demand?.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Steel 4140 / 4340 |
| Tolerance | ±0.002 mm on request |
| Lead time | 10 working days (production) |
| MOQ | Not specified in excerpt; confirm with supplier |
| Capacity | 400 x 300 x 200 mm envelope |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Tight tolerance programming (±0.002 mm) | Robotics parts with load cycling or thermal swing | Requires in-process checks at fixed intervals and slower cycle discipline |
| Standard tolerance programming | Non-critical features and roughing passes | Less documentation of process capability at production speed |
| Bore finish Ra 0.4 | Bores needing low friction or sealing | Adds finishing time and tooling cost |
| External finish Ra 0.8 | General external surfaces | Coarser than bore finish; may need secondary operation for Ra 0.2 |
| Regional second-source qualification | Buyers facing tariff and logistics uncertainty | Duplicates documentation and process capability evidence |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Process window definition | Fix material condition and tooling geometry before machining | Process window sheet |
| Programming | Set feeds, speeds, and toolpaths for production speed | CNC program and setup sheet |
| In-process checks | Measure at fixed intervals during production | In-process inspection log |
| Tolerance verification | Confirm ±0.002 mm on request at production speed, not single slow part | Capability data |
| Surface finish verification | Check Ra 0.4 bore and Ra 0.8 external | Surface finish report |
Related reading: Improve the production process and make every effort to improve the quality of stamping terminal products.
Frequently Asked Questions
What is CNC machining programming technology?
It is the process of defining the machining window before cutting metal: material condition, tooling geometry, feeds, speeds, and toolpaths. For robotics parts, it must hold ±0.002 mm on request at production speed, not just on a single slow sample, with in-process checks at fixed intervals.
What tolerances can CNC machining programming hold?
The article specifies ±0.002 mm on request. That tolerance is confirmed at production speed rather than on a single slow part. For a 400 x 300 x 200 mm envelope in 4140/4340 steel, this requires fixed in-process checks and documented process capability.
What surface finish can be achieved on bores and external surfaces?
Bore finish reaches Ra 0.4, external surfaces reach Ra 0.8, and roughness can go to Ra 0.2 where specified. These values are tied to the programming window, so finishing passes and tooling geometry must be fixed before production.
What lead time should I expect for production?
Production lead time is 10 working days. That assumes the process window is fixed and in-process checks are scheduled at fixed intervals. If ±0.002 mm on request is required across a 400 x 300 x 200 mm envelope, confirm capacity before releasing the order.
See also: Stamping Aluminum Sheet: Alloys, Limits and Anodizing After Stamping.
Why does regional qualification matter for CNC machining programming?
Tariff and logistics uncertainty has made regional qualification a priority in robotics. Buyers increasingly ask for a second qualified source, which changes how programming technology is specified and how tolerances are documented. That means capability evidence must travel with the process, not just the sample.
How do you prove process capability at production speed?
We fix material condition and tooling geometry first, then run in-process checks at fixed intervals. The target is ±0.002 mm on request at production speed, not on a single slow part. Records include the process window sheet, CNC program, and in-process inspection log.
What should I confirm before ordering CNC machined parts?
Confirm material grade 4140 or 4340, tolerance ±0.002 mm on request, bore finish Ra 0.4, external Ra 0.8, and the 400 x 300 x 200 mm envelope. Also confirm lead time of 10 working days and whether a second qualified source is required for regional qualification.
Learn more about Precision numerical control machining aluminum linear guide support block - custom metal fixture bracket.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Steel 4140 / 4340 |
| Tolerance | ±0.002 mm on request |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | 400 x 300 x 200 mm envelope |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| 4140 steel | Robotics parts needing load cycling resistance | Lower hardenability than 4340 |
| 4340 steel | Robotics parts needing thermal swing resistance | Higher cost and tighter processing window |
| ±0.002 mm tolerance | Critical mating features in robotics | Requires proven process capability at production speed |
| Ra 0.4 bore finish | Bore surfaces in robotics assemblies | Adds finishing time and inspection cost |
| 10 working days lead time | Production programs with regional qualification | Depends on material condition and tooling readiness |
Frequently Asked Questions
What is CNC machining programming technology?
CNC machining programming technology defines the process window before the machine: material condition and tooling geometry are fixed first, then capability is proven at production speed. For robotics parts in 4140/4340 steel, it supports a 400 x 300 x 200 mm envelope, ±0.002 mm tolerances on request, and Ra 0.4 bore finish.
Further technical detail: How to Calculate Heat Sink Size for Your Application: A Step-by-Step Engineering Guide.
What tolerances can you hold for robotics parts?
We hold ±0.002 mm on request for robotics parts in 4140/4340 steel. The 400 x 300 x 200 mm envelope and Ra 0.4 bore finish are supported when material condition and tooling geometry are fixed first and capability is proven at production speed.
Recommended reading: Custom CNC Machined Watch Bracelet Links.
What surface finish can you achieve on bores?
Bore finish reaches Ra 0.4, with Ra 0.8 external and Ra 0.2 listed in the article. These finishes apply to robotics parts in 4140/4340 steel within the 400 x 300 x 200 mm envelope and ±0.002 mm tolerance on request.
What is the production lead time?
Production lead time is 10 working days for robotics parts in 4140/4340 steel. This assumes material condition and tooling geometry are fixed first, tolerances of ±0.002 mm on request, Ra 0.4 bore finish, and capability proven at production speed.
What materials do you machine for robotics parts?
We machine Steel 4140 / 4340 for robotics parts. The process window covers a 400 x 300 x 200 mm envelope, ±0.002 mm tolerance on request, Ra 0.4 bore finish, Ra 0.8 external, Ra 0.2, and 10 working days production lead time.
What should I confirm before ordering CNC machined robotics parts?
Confirm material condition, tooling geometry, and whether the part must survive load cycling, thermal swing, or a corrosive environment in robotics. Also confirm the 400 x 300 x 200 mm envelope, ±0.002 mm tolerance on request, Ra 0.4 bore finish, and 10 working days lead time.
Compare it with Custom Heat Sinks Made in China.
Why does regional qualification matter for robotics buyers?
Tariff and logistics uncertainty has made regional qualification a priority in robotics. Buyers increasingly ask for a second qualified source. Suppliers must document process capability at production speed, with 4140/4340 steel, ±0.002 mm tolerance on request, Ra 0.4 bore finish, and 10 working days lead time.