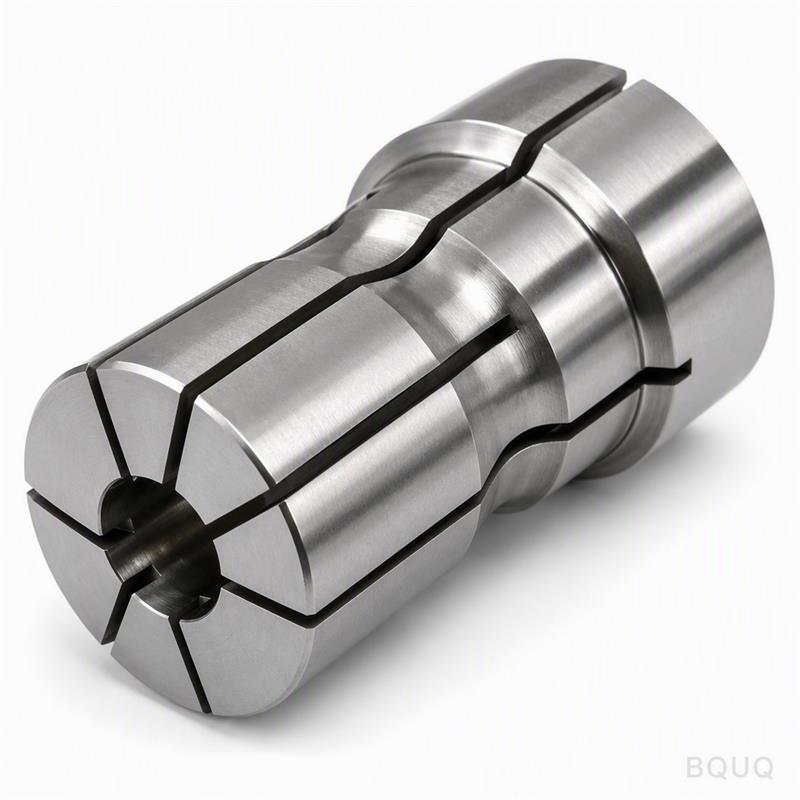
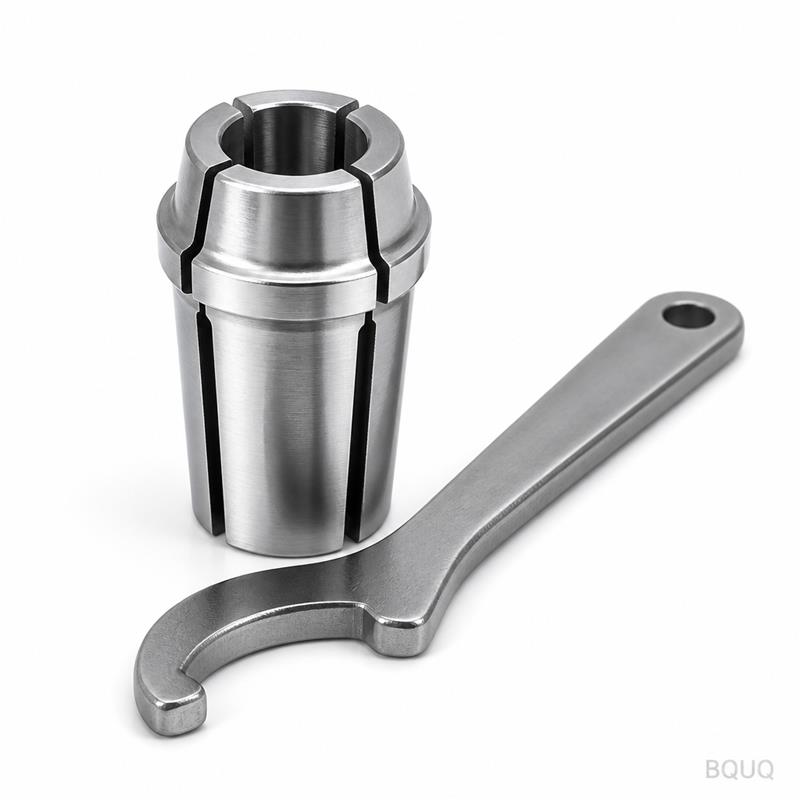
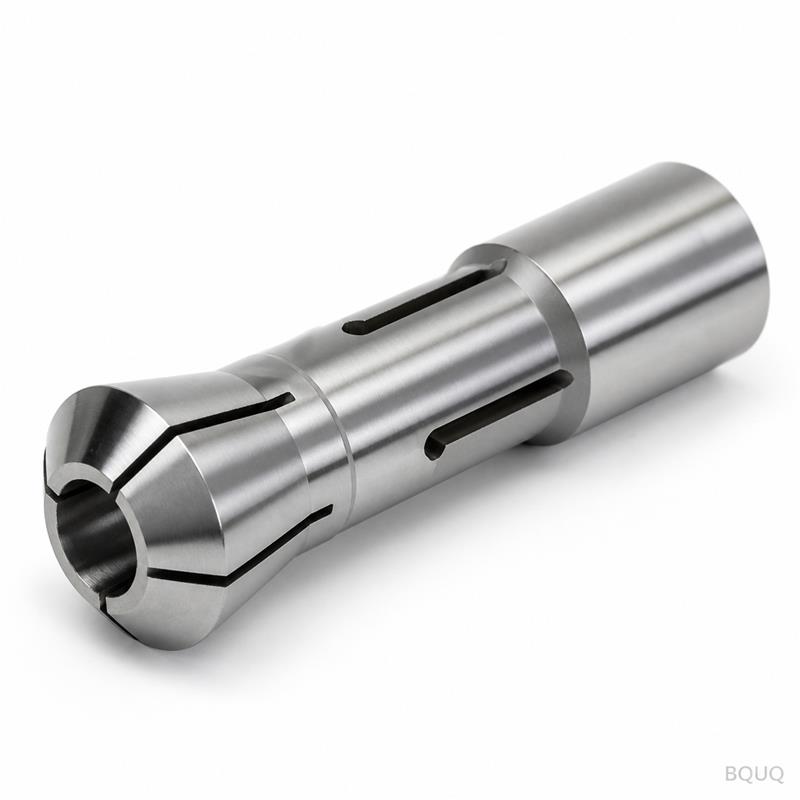
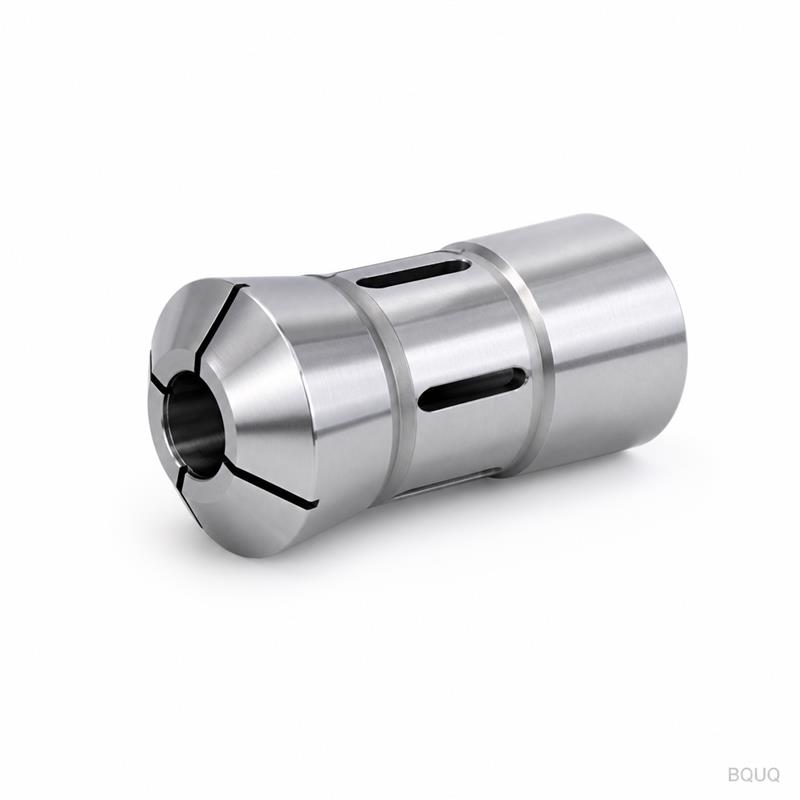
What This Waist Slot Collet Does Differently This is a CNC machined auto lathe 25 type collet with a waist slot detail, built for high-speed Swiss-type and automatic lathes. The
BQUQ CNC Machined Auto Lathe 25 Type Collet Waist Slot Detail
What This Waist Slot Collet Does Differently This is a CNC machined auto lathe 25 type collet with a waist slot detail, built for high-speed Swiss-type and automatic lathes. The waist slot reduces r
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 25 type collet with a waist slot detail, built for high-speed Swiss-type and automatic lathes. The waist slot reduces radial stiffness at the gripping zone, allowing the collet to close with less actuation force while maintaining concentricity. You get runout ≤0.003 mm (TIR) and a hardness of 58–60 HRC, so tool life and part repeatability stay consistent even at 8,000 RPM. Lead time is 7 days for standard sizes, and we ship from our Dongguan factory directly.
Why the Waist Slot Geometry Matters for 25 Type Collets
The 25 type collet has a 25 mm body diameter, but the gripping range is only 1 mm. The waist slot—a precision milled relief behind the nose—lets the collet flex evenly around the workpiece. Without it, you get uneven clamping pressure and chatter marks. We machine the slot with a 0.1 mm radius at the root to eliminate stress risers. That means the collet survives over 200,000 cycles without cracking, even on hardened steel bars.
Raw Material and Heat Treatment We Use
We start with 42CrMo4 alloy steel (AISI 4140 equivalent) or 65Mn spring steel, depending on your application. For standard gripping, 42CrMo4 is carburized to a case depth of 0.3–0.5 mm, then hardened to 58–60 HRC. For high-flex applications, 65Mn is through-hardened and tempered to 50–55 HRC. Both options are stabilized with a deep cryogenic treatment (-80°C) to prevent dimensional drift after grinding. The final ID grinding is done on a CNC internal grinder with coolant filtration to 5 microns.
Machining Tolerances on the Waist Slot and Bore
The bore is ground to a tolerance of +0.002 / +0.005 mm. The waist slot depth is held to ±0.01 mm, and the slot width to ±0.005 mm. The back taper (0°30' to 1°30') is checked with a laser gauge on every part. The outside diameter of the 25 type collet is ground to h5 grade, which is standard for collet chucks. Surface finish on the bore is Ra 0.2 µm, and the slot walls are Ra 0.4 µm to reduce friction during opening and closing.
Inspection Before Every Shipment
Every collet goes through a 100% inspection protocol. We use a Marposs gauge for bore runout and a profilometer for surface finish. The waist slot is checked with a coordinate measuring machine (CMM) for position and depth. We test each collet in a real 25 type auto lathe chuck at 6,000 RPM with a 10 mm test bar. If runout exceeds 0.003 mm, it gets reworked or scrapped. You receive a digital inspection report with your shipment—no exceptions.
Fit and Compatibility with Existing Chucks
This collet matches DIN 6499 and ER25 collet chuck standards, but the waist slot detail is proprietary to BQUQ. It fits all standard 25 type collet chucks with a 1:10 taper angle. The nose thread is M22x1.5, and the collet length is 40 mm. If you use a different taper angle (e.g., 1:8), we can adjust the external taper without changing the waist slot geometry. Just send your chuck drawing or model number.
Surface Finish and Coatings for Tough Materials
Standard finish is a black oxide coating to prevent rust during storage. For stainless steel or titanium bar work, we offer a TiN coating (2–3 µm) on the gripping surface. That reduces friction and prevents material pick-up. For high-volume production, we can apply a DLC coating (1 µm) that extends collet life by 3x compared to uncoated parts. The coating does not affect the waist slot tolerance—we measure after coating.
Pricing, MOQ, and Lead Time for Prototypes and Production
No MOQ. We accept single-piece prototypes and production runs of 10,000+ pieces. Prototype lead time is 5 days; production lead time is 7–10 days depending on quantity and coating. Unit price for a standard 25 type collet with waist slot is $18–$25 at 100 pieces, dropping to $12 at 1,000 pieces. For custom waist slot geometry, tooling cost is $150 one-time, and we keep the tool for future orders.
Specification
Value
Body Diameter (Type 25)
25 mm (h5)
Gripping Range
1 mm (e.g., 3–4 mm, 4–5 mm)
Length
40 mm
Hardness
58–60 HRC (carburized)
Bore Tolerance
+0.002 / +0.005 mm
Runout (TIR)
≤0.003 mm at 6,000 RPM
Surface Finish (Bore)
Ra 0.2 µm
Waist Slot Depth Tolerance
±0.01 mm
Material Options
42CrMo4 or 65Mn
Lead Time
7 days (standard size)
MOQ
No MOQ
Do You Have a Minimum Order Quantity?
No MOQ—order one piece for testing or 10,000 for production, and the per-unit price adjusts accordingly.
Can You Customize the Waist Slot Width or Depth?
Yes, we can modify the waist slot width, depth, and position to match your material and spindle speed; just send a drawing with your required dimensions.
How Do You Ensure Quality Control on Each Collet?
We use 100% CMM inspection, laser taper measurement, and a live runout test in a real chuck at 6,000 RPM before shipping, with a digital report included.
What Is the Lead Time for a Custom 25 Type Collet?
Standard sizes ship in 7 days; custom waist slot geometry takes 10 days, including tooling setup and first-article inspection.
Get a Firm Quote Within 12 Hours
Send your drawing or specify the gripping range and material. We will reply with a firm quote—not an estimate—within 12 hours. For complex waist slot designs, our engineers will suggest a cost-effective alternative. This is precision manufacturing with made in China efficiency, backed by 20 years of CNC machining experience. No MOQ, no hidden tooling fees. Email sc@bquq.com or WhatsApp +86 13713157787. For related reading, check our CNC cutting tool selection guide and CNC machining tolerances guide to optimize your collet application.