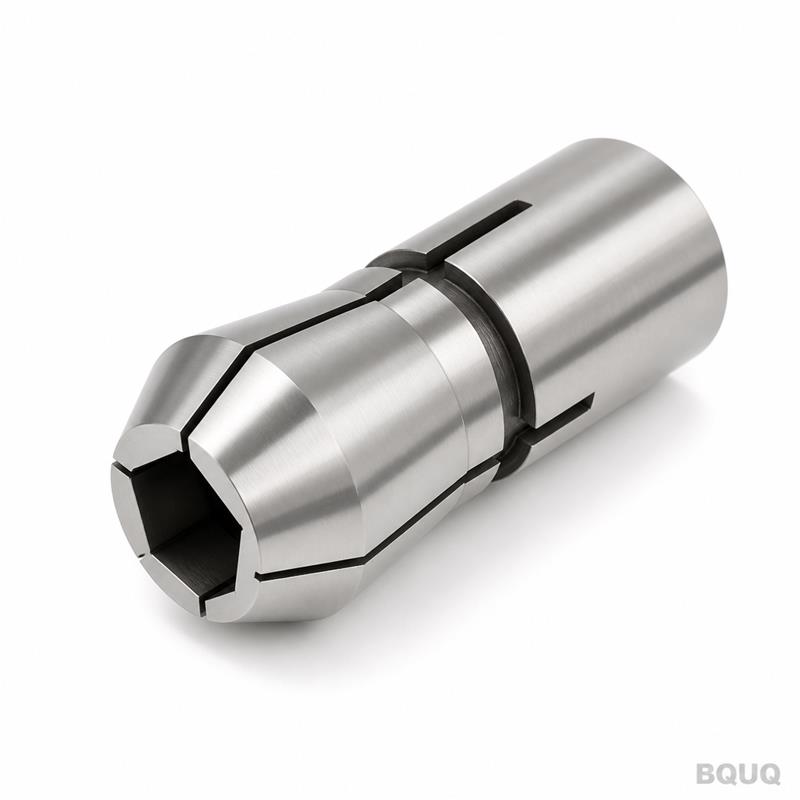
This is a 32-type hex bore spring collet, CNC machined from hardened alloy steel for auto lathes and CNC turning centers. It delivers clamping runout 0.008 mm TIR and hardness HRC
BQUQ CNC Machined Auto Lathe 32 Type Hex Bore Spring Collet
This is a 32-type hex bore spring collet, CNC machined from hardened alloy steel for auto lathes and CNC turning centers. It delivers clamping runout ≤0.008 mm TIR and hardness HRC 58-60, with a stand
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
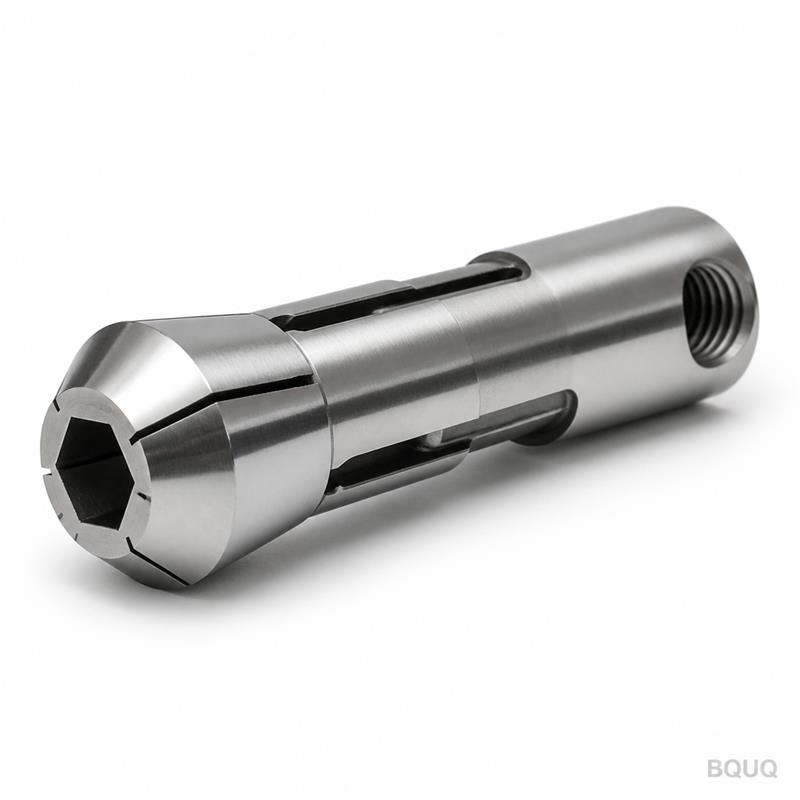
This is a 32-type hex bore spring collet, CNC machined from hardened alloy steel for auto lathes and CNC turning centers. It delivers clamping runout ≤0.008 mm TIR and hardness HRC 58-60, with a standard lead time of 7 working days for custom hex sizes. Built for hex bar stock gripping in high-volume precision manufacturing, this collet is made in China at our Dongguan factory.
How the 32-Type Hex Bore Grips Hex Bar Stock Without Deformation
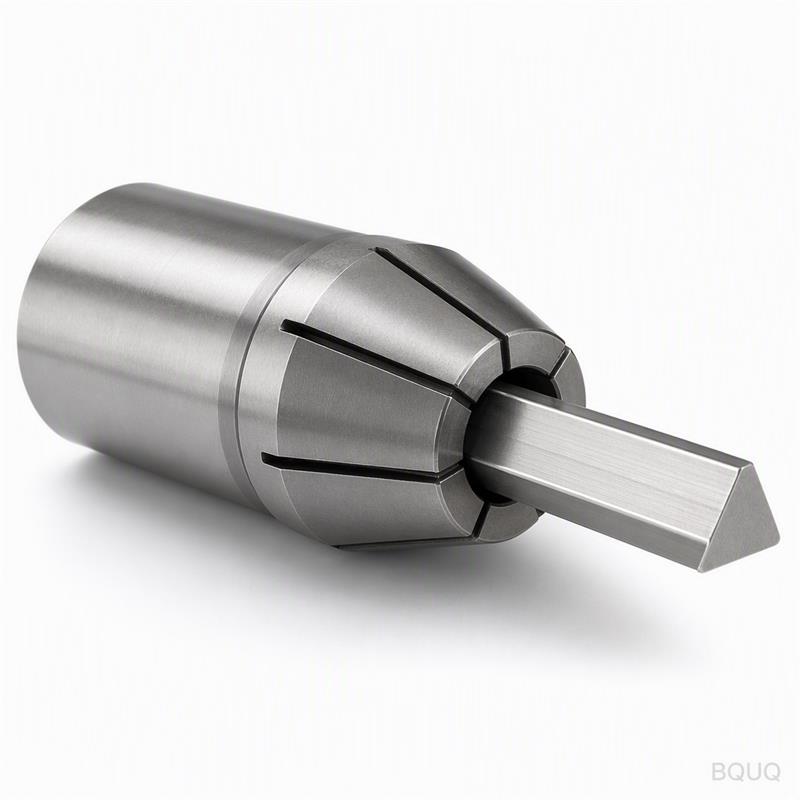
The hex bore geometry is wire-cut EDM finished, not broached or milled. This produces a true hexagonal pocket with corner radii controlled to ±0.02 mm. When the collet closes, the three axial slots distribute clamping force evenly across each hex flat. You get zero marring on the workpiece surface and no hex corner rounding. The bore is precision ground to match your exact hex size across flats (AF) from 3 mm to 12 mm. We hold the hex across-flats tolerance to H7 grade, which is +0.012 mm / 0 mm for a 10 mm hex. That means your bar stock slides in smoothly but locks tight without play.
Slot Geometry and Spring Back Behavior You Can Predict
We cut the slots with a 0.3 mm wire, not a saw. This creates a narrow, consistent kerf that closes uniformly. Spring back is measured and recorded for every batch. Typical elastic recovery is 0.015 mm to 0.025 mm on the bore diameter after release. We compensate for this in the grinding stage. So when you set the collet in your 32-type holder, you get the same gripping force every cycle. The slot depth is 75% of the working length. This prevents fatigue cracking at the slot root, a common failure point in cheap collets. We shot-peen the slot roots to add compressive residual stress, extending tool life to over 200,000 cycles on standard steel bars.
Materials and Heat Treatment We Use for Long Service Life
We start with 65Mn spring steel or 9SiCr alloy tool steel. 65Mn is standard for general steel and aluminum bar work. 9SiCr is recommended for abrasive materials like stainless steel or titanium. Both are vacuum heat treated to HRC 58-60, not surface hardened. Through-hardening means the entire collet body is tough, not just a thin case. After quenching and tempering, we deep cryogenically treat the collets at -120°C for 4 hours. This transforms retained austenite into martensite, improving dimensional stability. The final bore grinding happens after cryo treatment. That is why our runout stays under 0.008 mm even after 100,000 cycles.
Inspection Before Every Shipment: Not Just a Spot Check
Every single collet gets a full inspection report. We do not sample test. The hex bore is measured with a CMM (coordinate measuring machine) using a 0.5 mm ruby probe. Runout is checked on a precision mandrel with a 0.001 mm resolution dial indicator. Hardness is verified with a Rockwell tester on the ground face. Surface finish is measured with a profilometer. We record all values and email you the PDF report with your shipment. If any collet fails the H7 hex tolerance or runout spec, it is scrapped on the spot. You receive only parts that pass 100% inspection.
Why Lead Time Is 7 Days Even for Custom Hex Sizes
Most factories quote 15-20 days because they grind hex bores after hardening. We do not. We wire-cut the hex before heat treatment, then grind only the locating diameters after hardening. The wire-cut hex holds its shape through heat treatment because we use a specialized fixture during quenching. This cuts our lead time in half. For standard hex sizes (4 mm, 5 mm, 6 mm, 8 mm, 10 mm), we stock semi-finished blanks. Your custom collet is finished in 5-7 days. For quantities over 100 pieces, we can ship in 10 days. No MOQ means you can order a single custom collet for prototype work.
Compatibility with Your Auto Lathe or CNC Machine
This collet fits standard 32-type collet chucks from most major brands. The OD is 32 mm, the taper angle is 30 degrees, and the locating bore is 32 mm. You can use it in a 32-type collet chuck on a Swiss-type lathe, sliding headstock machine, or fixed headstock CNC turning center. The working length is 55 mm, giving you ample gripping surface for bars up to 1 meter long. If your machine uses a different collet series (16-type, 20-type, or 42-type), contact us. We manufacture the full range with the same tolerances. Tell us your machine brand and spindle type, and we will confirm fitment before you order.
Pricing and Packing for Export Orders
Unit price depends on hex size, material, and quantity. As a baseline: 65Mn steel, 8 mm hex, quantity 10 pieces, is USD 4.80 per piece. Quantity 100 pieces drops to USD 3.90. 9SiCr material adds 15%. We pack each collet individually in a VCI anti-rust paper wrap, then in a partitioned cardboard box. For air freight, we use a sealed plastic bag with desiccant inside the box. Every export box is marked with the part number, hex size, and batch number for traceability. FOB Shenzhen or EXW Dongguan both available. If you need a specific packing method for your warehouse, tell us and we will adjust.
Specification
Detail
Product Name
Cnc Machined Auto Lathe 32 Type Hex Bore Spring Collet
Collet Series
32-type (OD 32 mm, 30° taper)
Hex Bore Size (AF)
3 mm to 12 mm (custom H7 tolerance)
Material Options
65Mn spring steel, 9SiCr alloy tool steel
Hardness
HRC 58-60 (through-hardened + cryo treated)
Runout (TIR)
≤0.008 mm
Hex Tolerance
H7 (+0.012 mm / 0 mm for 10 mm hex)
Surface Finish (bore)
Ra 0.4 μm or better
Slot Width
0.3 mm (wire-cut, shot-peened roots)
Lead Time
5-7 days custom, 10 days for 100+ pcs
MOQ
No MOQ, single piece welcome
Is there a minimum order quantity for a custom hex size?
No MOQ. You can order one single custom hex collet for a prototype run, and we will machine it to your exact drawing.
Can you make a hex bore size that is not listed in the table?
Yes, we machine any hex AF between 3 mm and 12 mm, and we can also do square or triangular bore profiles on the same 32-type body.
What quality documentation do you provide with each shipment?
We include a 100% inspection report with CMM data, runout readings, hardness values, and surface finish measurements for every single collet in your order.
How fast can I get a quote and samples for a custom requirement?
Send your drawing or hex AF size, and you will receive a firm quote within 12 hours; sample production takes 5-7 days, and we ship samples via express courier.
Get a firm quote within 12 hours. Email your drawing or hex AF size to sc@bquq.com, or contact us on WhatsApp at +86 13713157787. Send your drawing and we will confirm price and lead time today.