What This Collet Chuck Does and Why It Matters This is a CNC machined auto lathe 46 type round bore spring collet chuck, built for high-volume turning of round bar stock. It grip
BQUQ CNC Machined Auto Lathe 46 Type Round Bore Spring Collet Chuck
What This Collet Chuck Does and Why It Matters This is a CNC machined auto lathe 46 type round bore spring collet chuck, built for high-volume turning of round bar stock. It grips workpieces from 3
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
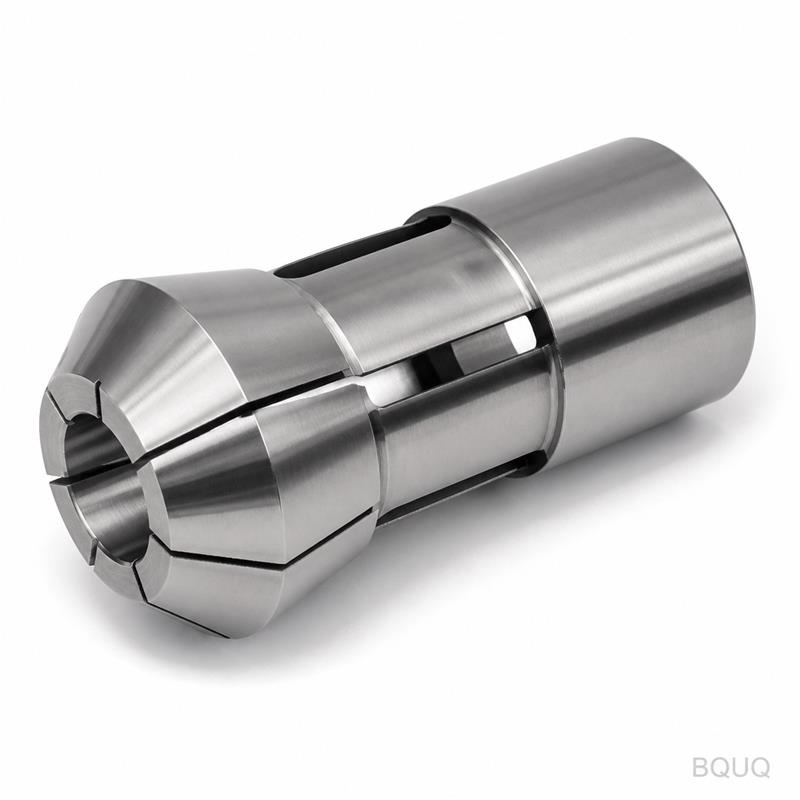
This is a CNC machined auto lathe 46 type round bore spring collet chuck, built for high-volume turning of round bar stock. It grips workpieces from 3 mm to 46 mm bore diameter with 0.005 mm total indicated runout (TIR), which means your finished parts hold concentricity without secondary grinding. We harden the gripping surface to 58–60 HRC, so it resists wear through 100,000+ cycles. Typical lead time is 15 days for standard sizes, and we ship from our Dongguan factory with no MOQ.
How the 46 Type Round Bore Grip Geometry Reduces Runout
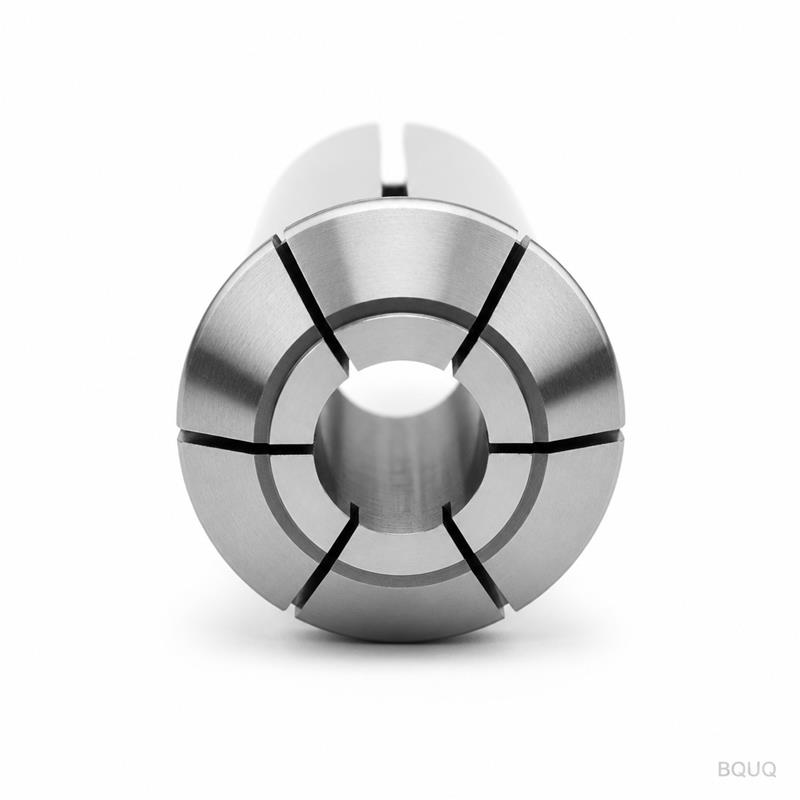
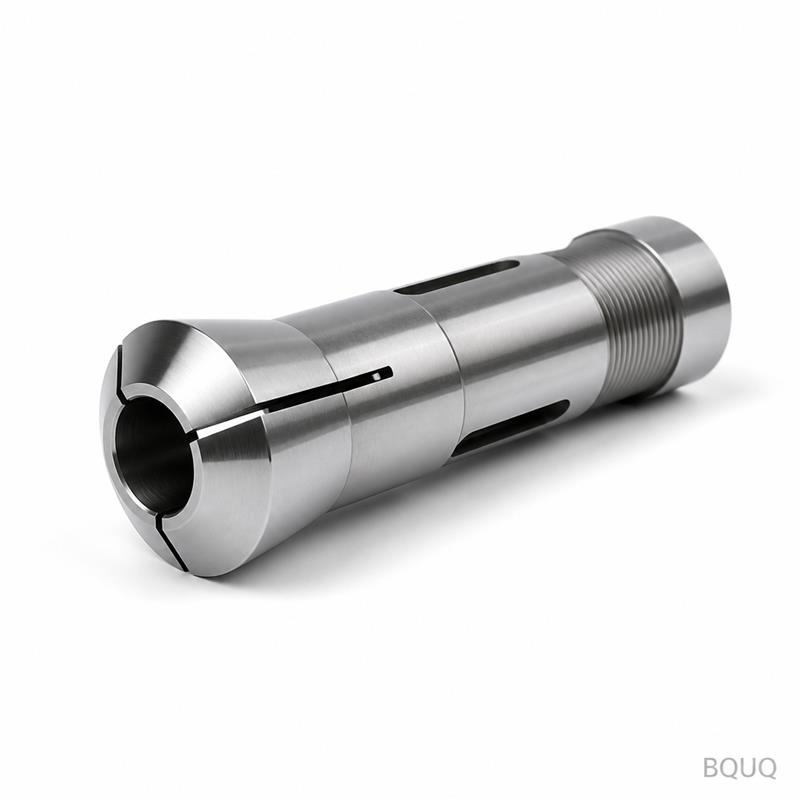
The 46 type designation refers to the DIN 6343 style collet taper, with a 16-degree included angle. Our round bore is ground in a single setup after heat treatment, not before—this is the key to holding 0.005 mm TIR. The spring segment slots are wire-cut with a 0.3 mm kerf, giving even radial collapse across all six slots. Unlike ER collets that use a nut to compress, this spring collet chuck uses a drawbar pull-back action, which centers the bar automatically. You get repeatable gripping force of 40–80 N·m without marking soft aluminum or brass stock.
Materials and Heat Treatment We Use for 60 HRC Longevity
We start with 42CrMo4 (AISI 4140) steel, pre-hardened to 28–32 HRC for machining. After CNC turning and milling, we vacuum harden to 58–60 HRC, then deep-freeze at -80°C for 2 hours to convert retained austenite. This gives a stable microstructure, so the collet won't distort during high-speed spindle runs. The bore and taper are finish-ground with CBN wheels, achieving Ra 0.4 µm surface finish on the gripping area. For corrosive environments, we offer an optional electroless nickel plating of 8–12 µm thickness—but standard delivery is plain ground steel.
Inspection Before Every Shipment: Runout and Hardness Checks
Every collet chuck is 100% inspected, not batch-sampled. We check: (1) TIR at the nose with a test bar inserted, using a 0.001 mm dial indicator; (2) taper angle with a sine bar and gauge blocks; (3) hardness on the gripping surface with a Rockwell tester; (4) slot width and depth with a toolmaker's microscope. You receive a printed inspection report with serial number and actual measured values. If any collet exceeds 0.005 mm TIR, it goes to scrap, not to you. This is why our return rate is under 0.3%.
Specifications for the CNC Machined Auto Lathe 46 Type Round Bore Spring Collet Chuck
Parameter
Value
Collet Type
DIN 6343 / 46 type
Bore Diameter Range
3 mm – 46 mm (round)
Total Indicated Runout (TIR)
0.005 mm max
Gripping Surface Hardness
58–60 HRC
Base Material
42CrMo4 / AISI 4140
Surface Finish (Gripping Area)
Ra 0.4 µm
Taper Angle
16° included
Gripping Force Range
40–80 N·m (drawbar dependent)
Lead Time (Standard Sizes)
15 days
MOQ
No MOQ—single piece accepted
Custom Bore Sizes and Slot Patterns for Special Applications
Standard bores are ground to H7 tolerance, but we can make any bore from 3 mm to 46 mm in 0.1 mm increments. For thin-walled tubing, we offer a 12-slot version instead of the standard 6-slot, which distributes force more evenly and prevents collapse. For square or hex stock, we can wire-cut the bore to match—just send your cross-section drawing. We also adjust slot depth for softer materials like copper or PTFE, reducing grip pressure by up to 30% if you request it. All custom work is still made in China at our Dongguan plant, with the same 15-day lead time for bores under 30 mm.
Compatibility with Common Auto Lathe Spindles
This collet chuck fits most 46 type spindle noses, including Citizen, Star, Tsugami, and Hanwha Swiss-type lathes, as well as fixed-headstock auto lathes from Tornos and Esco. The rear thread is M20 x 1.5 as standard, but we can machine M18, M22, or 3/4-16 UNF on request. The overall length is 68 mm, which clears most guide bushings without modification. If you are unsure about your spindle nose, measure the taper angle and drawbar thread pitch—or send us a photo of your current collet, and we will confirm compatibility within one working day.
Do you accept one-piece orders?
Yes, we have no MOQ—you can order a single collet chuck for testing, and we will ship it with full inspection documents.
Can you customize the bore to my exact bar diameter?
Yes, we grind bores in 0.1 mm increments from 3 mm to 46 mm, and we can also cut square, hex, or splined profiles if you send a drawing.
How do you ensure quality for each batch?
We perform 100% dimensional inspection on every piece, including TIR, hardness, and taper angle, and we include a signed report with each shipment.
What is your typical lead time for a custom size?
Standard bores ship in 15 days; custom profiles or non-standard slot patterns take 20–25 days, depending on complexity.
Get a Firm Quote Within 12 Hours—Send Your Drawing
We reply to all inquiries with a firm, itemized quote within 12 hours, including price, lead time, and freight options. Email us at sc@bquq.com or message us on WhatsApp at +86 13713157787. Attach your 2D drawing or 3D STEP file, and we will confirm the bore size, taper, and thread configuration before quoting. If you are still selecting tooling for your lathe, check our CNC cutting tool selection guide to match the collet chuck with the right inserts and holders. For more on how we hold 0.005 mm TIR, read our CNC machining tolerances guide. This is precision manufacturing, done right—made in China, with no MOQ and a 12-hour response.