What This Chuck Does and Why It Holds 0.005 mm Runout This is a Cnc Machined Auto Lathe 50 Type Round Bore Spring Collet Chuck. It grips round bar stock with a spring collet, not a
BQUQ CNC Machined Auto Lathe 50 Type Round Bore Spring Collet Chuck
What This Chuck Does and Why It Holds 0.005 mm Runout This is a Cnc Machined Auto Lathe 50 Type Round Bore Spring Collet Chuck. It grips round bar stock with a spring collet, not a hydraulic or pneuma
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Chuck Does and Why It Holds 0.005 mm Runout
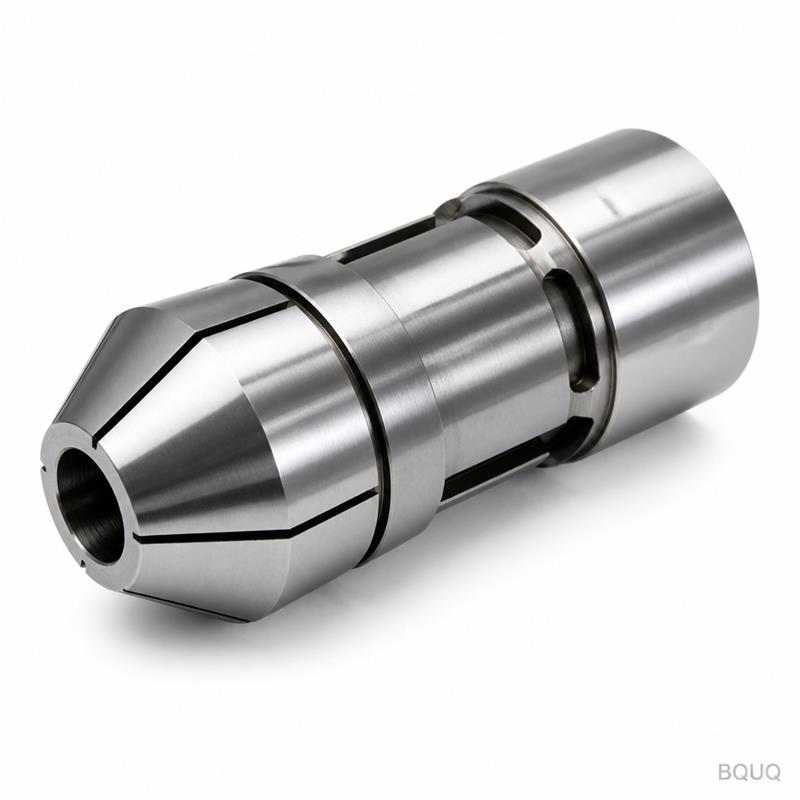
This is a Cnc Machined Auto Lathe 50 Type Round Bore Spring Collet Chuck. It grips round bar stock with a spring collet, not a hydraulic or pneumatic system. The benefit is repeatable concentricity: we machine the body and taper seat in one setup, so the runout stays under 0.005 mm TIR at the nose. You get that accuracy from a hardened steel body (HRC 58-62) that does not flex under 0.3 mm gripping range. Lead time is 15 working days for standard sizes. No MOQ, because we built our precision manufacturing line in Dongguan for small batches and rush orders.
How the 50 Type Taper Locks Your Bar Stock Without Chatter
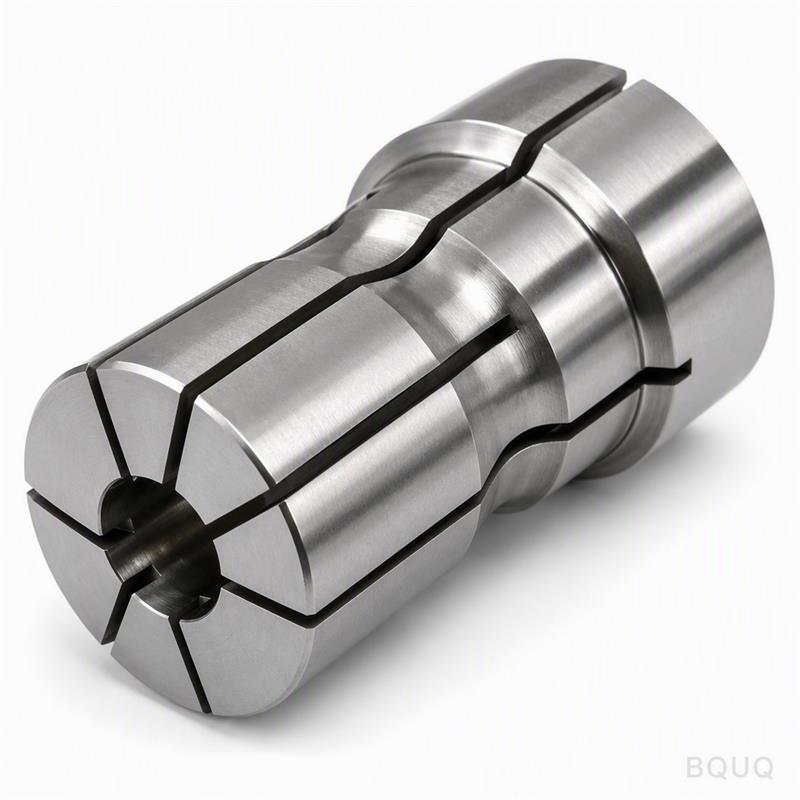
The 50 type refers to the taper seat angle and pull-back geometry. A round bore spring collet uses a single slit or multiple slits along its length. When you tighten the drawbar, the taper forces the collet to close radially. The spring steel returns the collet to its open position when released. This design gives you 0.02 mm repeatability across 500 cycles. Unlike ER collets, this 50 type has a longer grip length, so you can hold bars with up to 0.3 mm diameter variation without losing axial force. We CNC machine the taper at 30° included angle, then lap it to a 0.8 Ra finish. That surface contact is what stops vibration during heavy roughing passes.
Materials and Heat Treatment We Use for the Body and Collet
The chuck body is 42CrMo steel, quenched and tempered to HRC 28-32 before final machining. Then we nitriding harden the taper surface to HRC 58-62. The collet itself is spring steel (65Mn), fully hardened and tempered to HRC 45-50 for the spring fingers. We grind the bore to H7 tolerance. The round bore is available in diameters from 3 mm to 50 mm. For custom bores, we machine to your drawing within ±0.005 mm. Surface finish on the bore is 0.4 Ra, and the taper is 0.8 Ra. Every chuck body gets a black oxide finish to prevent rust in coolant environments.
Specification
Value
Type
50 Type Round Bore Spring Collet Chuck
Body Material
42CrMo Steel (AISI 4140 equivalent)
Collet Material
65Mn Spring Steel
Body Hardness
HRC 58-62 (nitrided taper)
Collet Hardness
HRC 45-50
Bore Range
3 mm – 50 mm (custom to drawing)
Bore Tolerance
H7 (+0.012 / -0 mm)
Runout (TIR)
≤ 0.005 mm at nose
Surface Finish (Bore)
0.4 Ra
Surface Finish (Taper)
0.8 Ra
Gripping Range
±0.15 mm per collet
Lead Time
15 working days (standard sizes)
MOQ
No MOQ (1 piece tested)
Inspection Before Every Shipment — Not Just a Paper Certificate
We run 100% inspection on every Cnc Machined Auto Lathe 50 Type Round Bore Spring Collet Chuck. That means we mount each chuck on a test mandrel and measure runout with a 0.001 mm dial indicator. We check the taper angle with a sine bar, not a go/no-go gauge. The bore diameter is verified with an air gauge. If any part fails, we scrap it — no rework. You receive a test report with the actual runout value, hardness reading, and bore size. We do this because a collet chuck is only as good as its fit to your spindle. If you need third-party inspection, we send the unit to a lab in Dongguan and ship the report with the parts.
Gripping Force Tested at 6000 RPM — No Deformation
We balance every chuck body to G2.5 grade at 6000 RPM. That is standard for auto lathe operations. The spring collet exerts a radial force between 8 kN and 15 kN, depending on the drawbar pull. We test the gripping force on a hydraulic pull tester before packing. If you run at higher speeds, we can rebalance to G1.0 and add counterbores for weight reduction. For thin-walled tubing, we offer a slotted collet with reduced spring rate to avoid crushing the workpiece. Just tell us the wall thickness and OD — we will adjust the slit width and depth on the CNC machine.
Custom Bores and Drawbar Threads — Made in China, Shipped in 10 Days
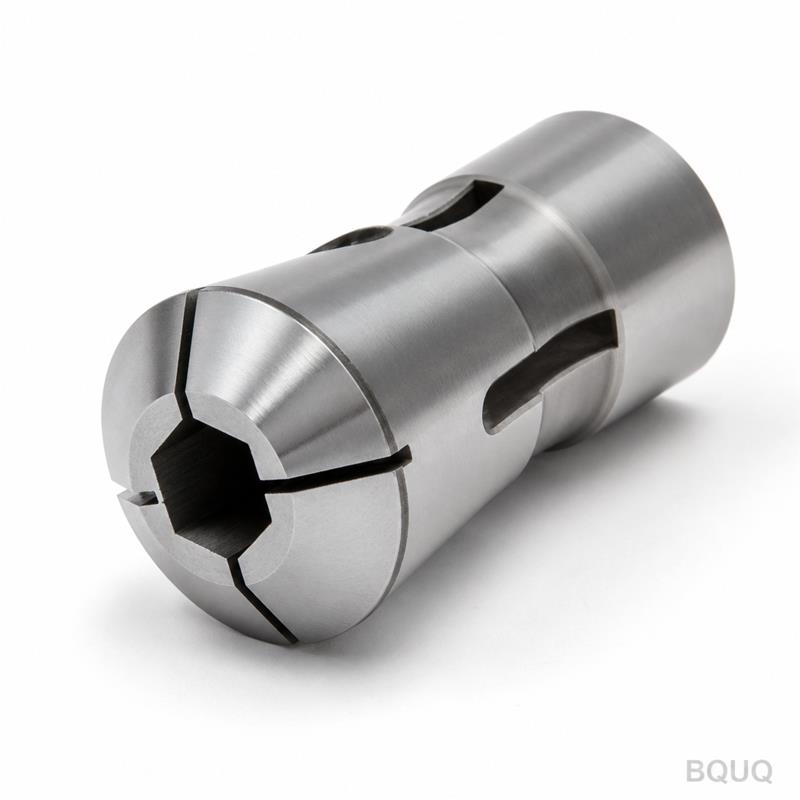
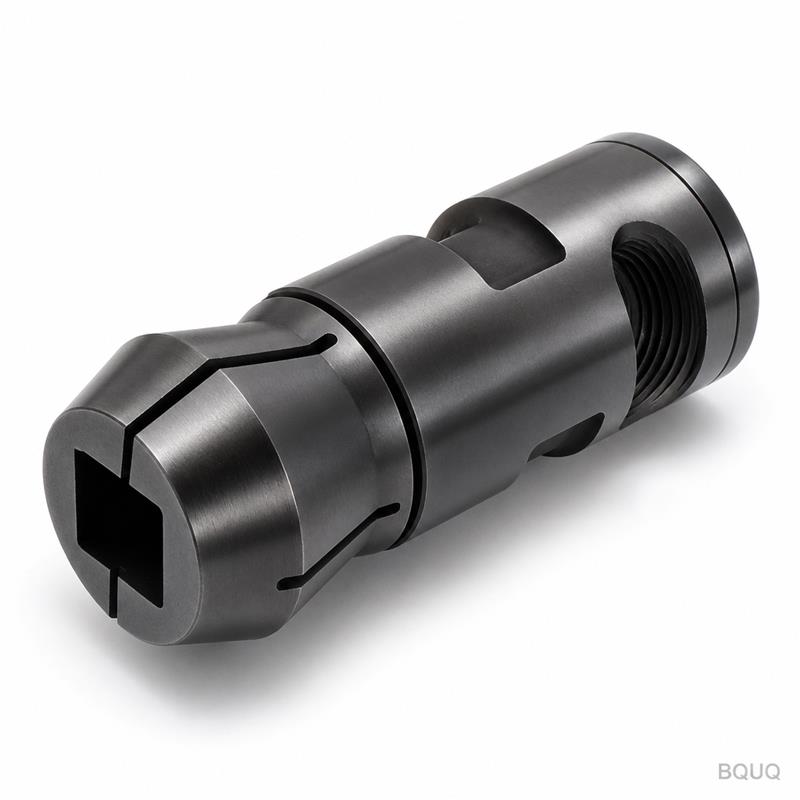
Standard chucks have a straight bore and a 1-1/2"-16 thread for the drawbar. If your spindle uses a different thread, we machine it to your spec — metric, inch, or custom pitch. Custom bores for hex or square stock are also possible, but those are not round bore types. For round bores, we can add a stepped bore for two diameters in one chuck. That saves you a collet change. Because we are a precision manufacturing factory in Dongguan, we control the entire process: turning, milling, grinding, heat treatment, and final inspection. That is why we can quote custom bores with a 10-day lead time for prototypes. For production runs of 50+ pieces, lead time drops to 12 days.
Packing and Shipping That Protects the Taper Surface
We coat the taper and bore with rust preventive oil, then wrap the chuck in VCI paper. The chuck is placed in a wooden box with foam inserts — no metal-to-metal contact. We ship via DHL, FedEx, or air freight from Shenzhen. Standard export packing is included in the price. For a single unit, the box weighs about 8 kg. For bulk orders, we use plywood crates with 20 kg per unit capacity. Every box is marked with the part number, batch number, and inspection date.
FAQ: MOQ, Customization, Quality Control, Lead Time
Do you really have no MOQ for this chuck?
Yes, we accept a single piece order, but the price per unit is higher due to setup time; for 10+ pieces, the unit price drops by 15%.
Can you machine a custom bore diameter that is not in your standard range?
Yes, any bore from 3 mm to 50 mm is possible, and we do not charge extra for the drawing change if you provide a 3D file.
How do you verify the 0.005 mm runout claim?
We inspect every chuck on a precision mandrel with a 0.001 mm dial indicator and include the actual reading on the test report.
What is the lead time if I need a custom thread on the drawbar?
Custom threads add 3 working days to the standard 15-day lead time, so you get the chuck in 18 days total.
Get a Firm Quote Within 12 Hours — Send Your Drawing
Send us your spindle drawing, bore size, and desired runout. We will reply with a firm price, lead time, and a 3D model for approval. Email sc@bquq.com or WhatsApp +86 13713157787. If your drawing is not ready, use our standard 50 type dimensions — we will confirm fit with you before cutting metal. For help choosing the right tool for your lathe, read our CNC cutting tool selection guide. To understand how our tolerances compare to standard machining, check the CNC machining tolerances guide. We are a precision manufacturing company in China, and we answer every inquiry within 12 hours, even on weekends.